

 0086-138 3838 9622
Pig Manure and Mushroom Waste Fertilizer Plant in Canada
RICHI MACHINERY
The Finished Formula Comes Before the Waste Tonnage
This Pig Manure and Mushroom Waste Fertilizer Plant in Canada is designed backward from a saleable fertilizer specification rather than forward from the amount of waste available. The customer is a regional fertilizer producer collecting pig manure, spent mushroom substrate and selected food-processing organics from several suppliers. Each stream has a different moisture, nutrient and biological profile, so the factory treats them as controlled ingredients rather than interchangeable waste.
The main commercial product is a 6 mm microbial organic fertilizer pellet. One FZLH520 mushroom waste pellet machine forms the prepared blend, but pelletizing is only the final forming step. The larger design task is to create a mature, repeatable fertilizer base before the ring die and then apply sensitive microorganisms after the product has cooled.
Finished output is approximately 30,000 T/A. The line is planned around about 3,000 effective mechanical production hours per year, equal to roughly 10 effective hours per day over 300 operating days. Two scheduled shifts provide room around those effective hours for cleaning, die inspection, formula changes, bag changes and routine maintenance rather than assuming every staffed hour becomes saleable production.
The confirmed RICHI machinery and engineering package is about USD 480,000. It covers the main compost-handling interfaces, mature-material preparation, one FZLH520, cooling, screening, microbial post-addition, packing, dust-control interfaces and electrical integration. Land, major civil works, local buildings, roads, provincial utility connection, freight, duties and working capital remain owner-side items unless the final contract explicitly adds them.
10 T/H
finished capacity
USD 480,000
RICHI supply
Canada
location
30,000 T/A
finished output
RICHI MACHINERY
The Collection Radius Has to Work before the Factory Can
The supply model works only if the plant is close enough to the industries that generate its organic inputs. Canada had about 14.0 million hogs on July 1, 2026, with Quebec, Ontario and Manitoba holding the largest provincial inventories. Mushroom production is also concentrated: Ontario accounted for 51.7% of Canadian mushroom output in 2025. Those patterns make a regional manure-and-substrate sourcing network commercially credible without relying on nationwide transport.
This organic fertilizer production project does not assume that every hog farm or mushroom grower becomes a supplier. Contracts are based on collectable solids, moisture, storage method, contamination control and hauling distance. A farm with dilute slurry is a different logistics problem from a farm supplying mechanically separated manure, while fresh wet mushroom substrate behaves differently from material that has already lost part of its moisture.
Canada’s oilseed sector provides another source of selected processing by-products, but the plant does not divert normal high-value feed-grade canola meal simply because it exists. Canadian processors crushed a record 11.6 million tonnes of canola in 2025. The fertilizer project evaluates only off-spec, downgraded or secondary organic fractions whose safety, nutrient value and economics make sense for fertilizer production.
RICHI MACHINERY
Purchasing Is Managed on Usable Dry Matter
The customer buys usable dry matter, not just truck weight. Spent mushroom substrate and brewery-derived residues can carry large amounts of water, while separated manure and some oilseed-derived materials may be much drier. A low gate price can therefore become expensive if the plant is paying to haul and later remove water that contributes little to the finished product.
| Supply Stream | Planning Role | Annual Procurement Basis | Main Control |
|---|---|---|---|
| Separated / stabilized pig manure | Main animal-origin organic fraction | Approx. 24,000–28,000 T/A | Moisture, bedding, contaminants and storage age |
| Spent mushroom substrate | Fibre, organic matter and structure | Approx. 15,000–18,000 T/A | Moisture, fibre length, salts and supplier consistency |
| Brewery-derived organics | Optional wet co-composting stream | Approx. 4,000–6,000 T/A | Water content, transport radius and batch condition |
| Approved oilseed / soy by-products | Controlled nutrient-rich addition | Approx. 5,000–7,000 T/A | Specification, nitrogen load and commercial value |
| Dry structural / formulation materials | Moisture and formula correction | Approx. 5,000–7,000 T/A | Clean source and product compatibility |
The resulting procurement envelope is roughly 55,000–65,000 T/A, but it is not a permanent recipe. Exact wet intake rises when wetter materials dominate and falls when dry solids are higher. The customer records wet weight, moisture or solids, formula additions, biological loss and finished yield so the 30,000-tonne sales target is supported by actual mass balance rather than a fixed wet-input ratio.
RICHI MACHINERY
Four Organic Streams Must First Become One Stable Compost
The compost recipe is managed first as a physical and biological mixture, not as the final fertilizer formula. Pig manure supplies a substantial nitrogen-rich fraction. Spent mushroom substrate brings fibre, residual organic matter and pore space. Brewery material can add readily degradable carbon but can also raise moisture quickly. Oilseed-derived additions are controlled because excessive protein-rich material can intensify heating and ammonia loss.
- Very wet manure or brewery residue is balanced with drier structural material instead of being sent directly to a dryer.
- Spent mushroom substrate is useful for porosity during composting, but excessive long fibre is reduced before pelletizing when it interferes with feeding.
- Oilseed-derived additions are limited by the intended nutrient analysis and by the biological response of the compost mix.
- Plastic, metal, stones, treated wood and other unsuitable contaminants are rejected before the batch enters normal production.
Operators work from measured moisture, texture, temperature response and pile structure instead of one permanent four-material percentage. The aim is to maintain enough water for biological activity without collapsing the pile into an anaerobic mass. When incoming conditions change, the plant corrects the compost recipe and turning strategy before asking the downstream machinery to compensate.
RICHI MACHINERY
Winter and Residence Time Set the Real Site Scale
Composting is the real inventory buffer. With roughly 55,000–65,000 tonnes of annual incoming materials, the plant can receive around 180–220 tonnes on a busy delivery day. Several weeks of active composting and maturation therefore place thousands of tonnes inside the biological section at one time, even though the FZLH520 finishes material at about 10 T/H.
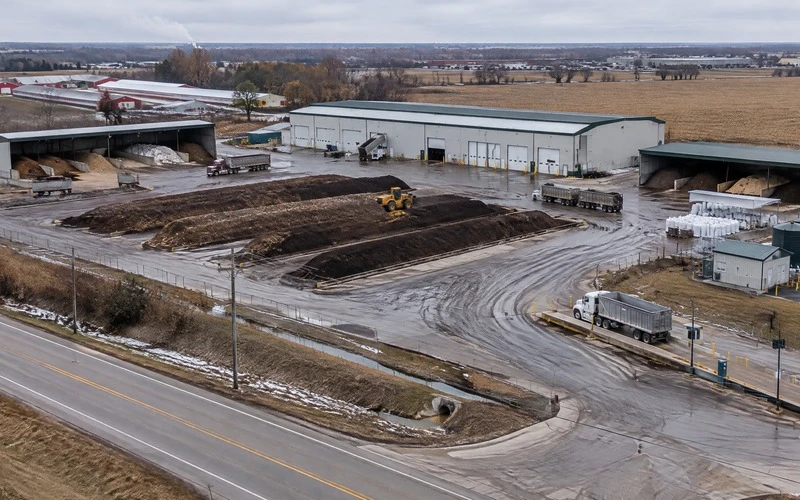
A total site of roughly 16,000–20,000 m² is a more defensible planning basis than sizing land around the pellet mill. About 7,000–9,000 m² can be reserved for wet receiving, active composting, turning lanes and maturation, with the remaining area used for dry preparation, pelletizing, finished storage, utilities, laboratory functions, truck circulation and winter access.
Winter changes the civil design but does not mean the whole compost yard must be heated. Wet receiving, pumps, microbial liquids and critical mechanical equipment need freeze protection. Covered storage keeps finished fertilizer and dry structural material out of snow and rain. Pile mass, covers, drainage, snow removal and delivery scheduling are then adapted to the actual province and winter conditions.
RICHI MACHINERY
Biology Ends before Commercial Formulation Begins
The process changes character only after biological variability has been reduced. Fresh organics stay in the wet side; a commercial fertilizer formula is created from mature compost in the dry side. That boundary prevents the pellet mill from being used as a substitute for stabilization.
- Receive and record each supplier lot, checking moisture, visible contamination and the agreed material specification.
- Blend pig manure, spent mushroom substrate and approved co-materials to establish a compostable physical mixture.
- Run aerobic composting and turning, then hold the material through maturation until temperature trend, odor, moisture and structure support release.
- Reduce mature lumps and excessive fibre only as much as needed for stable feeding and screening.
- Prepare the commercial fertilizer formula in the dry section of the organic fertilizer production line.
- Pelletize the prepared blend through the FZLH520, then cool and screen the 6 mm product.
- Apply the approved microbial treatment only after pellet temperature is suitable for the selected microorganism and registration route.
- Pack qualified product by traceable lot and move it into dry finished storage.
This sequence makes troubleshooting clearer. If a batch remains biologically unstable, the problem belongs in composting. If the formula will not feed consistently, the dry preparation section is checked. If microbial counts fall after packing, coating temperature, carrier, warehouse conditions and shelf life are investigated instead of changing the ring die.
RICHI MACHINERY
One FZLH520 Sits inside a Larger Quality System
The mechanical section is deliberately compact. One 132 kW FZLH520 organic fertilizer pellet making machine is the main forming unit. According to the project machine specification, FZLH520 reference capacity is 9–12 T/H, with a 520 mm ring die and a 4–12 mm pellet-diameter range. The customer starts with a 6 mm product and operates around the 10 T/H annual planning point.
For the Pig Manure and Mushroom Waste Fertilizer Plant in Canada, the 9–12 T/H machine range is treated as a reference, not as a guarantee for every recipe. Sustainable output still depends on bulk density, fibre, moisture, mineral additions and the selected die. Commissioning therefore establishes the stable operating window on the customer’s actual fertilizer blend.
| Mechanical Duty | Main Equipment | Project Configuration |
|---|---|---|
| Mature-compost feed | Buffer hopper and controlled feeder | Stable feed to dry preparation |
| Lump / fibre reduction | Organic fertilizer crushers | 2 staged units where required |
| Screening | Pre-screens | 2 units for oversize and foreign-material control |
| Formula preparation | Horizontal mixer | 1 main unit with controlled dosing |
| Pelletizing | 1 × FZLH520 | 132 kW; 9–12 T/H reference; 6 mm main SKU |
| Cooling | Mechanical fertilizer cooler | Matched to project pellet output |
| Final screening | Pellet screen and fines return | Protects packing quality |
| Microbial finishing | Low-temperature post-addition / coating system | Product- and registration-dependent |
| Packing | 2 quantitative bagging stations | 20–25 kg and 40 kg formats |
| Dust control | Local extraction and bag filtration | Crusher, screen, transfer and packing points |
| Control | PLC/MCC and interlocks | Coordinates finishing and protection logic |
RICHI MACHINERY
Microbial Value Is Added after the Pellet Is Safe to Treat
The physical pellet and the microbial claim are controlled separately. One organic fertilizer pellet mill can create a stable 6 mm product, but compression does not guarantee viable microorganisms. The project therefore cools the pellet first and adds sensitive microbial material afterward when the approved product formulation requires it.
Using a ring-die fertilizer granulator machine gives the customer a denser product for distribution and mechanical spreading. The FZLH520 can use other dies within the 4–12 mm range, but the factory starts with one 6 mm commercial SKU so commissioning, spare-die planning, coating validation and distributor communication are all based on the same reference product.
A later change in pellet size does not automatically require another pig manure pellet machine. It first requires a real customer specification, a compatible die and confirmation that the new pellet geometry still cools, coats and packs within the registered product requirements.
RICHI MACHINERY
The Canadian Product Claim Is a Regulatory Design Input
Canada regulates fertilizers and supplements federally under the Fertilizers Act and Fertilizers Regulations, while manufacturing, environmental management and use can also involve provincial or municipal rules. CFIA evaluates product safety, ingredients and labeling, and registration status depends on how the product is represented in the market. Product identity therefore has to be fixed before the label and microbial system are finalized.
The microbial claim requires particular care. CFIA guidance states that products represented to contain microorganisms as active ingredients generally require registration before importation or sale, subject to specific exemptions for qualifying mixtures. The customer therefore confirms strain identity, carrier, guarantee, label wording, shelf life and registration trigger before the post-coating system is frozen.
This is why the Pig Manure and Mushroom Waste Fertilizer Plant in Canada does not assume that every 6 mm pellet can automatically be sold as a microbial supplement product. The base fertilizer composition, the viable microorganism component and the final market claim are checked against the Canadian regulatory route before commercial release.
RICHI MACHINERY
Utilities and Staffing Follow Two Different Work Rhythms
The plant is mainly electrically driven. The 132 kW FZLH520 is the largest single process motor, followed by crushers, mixers, conveyors, cooler fans, screens, dust collection and packing. A preliminary connected-load class of about 320–420 kW is reasonable before the final motor list is frozen. Annual electricity around 1.0–1.4 GWh provides a useful early planning range for 30,000 T/A.
Canada uses 60 Hz AC power, but site service voltage, transformer size, motor starting and protection still depend on the province, local utility and simultaneous-load schedule. The project does not copy one voltage from another Canadian plant. Space heating for occupied rooms and freeze protection is also separated from the core process-electricity calculation.
Fresh water is used for cleaning, staff, selective compost moisture correction and microbial-coating preparation rather than continuous wet granulation. A planning range of about 1,500–2,500 m³/year is appropriate until the final building and environmental systems are confirmed. Fire-water storage and emergency supply are designed separately.
Around 20–26 direct roles is a practical basis for two-shift finishing with daytime biological handling. Staffing covers receiving, loader and turner work, mature-material preparation, pelletizing, microbial finishing, QC, packing, warehouse and maintenance. Sales, accounting, transport and some laboratory work can remain shared or contracted according to the customer’s organization.
RICHI MACHINERY
Every Bag Has to Trace Back through the Biological Process
Traceability has to cross the biological and mechanical parts of the factory because the raw materials vary and the microbial claim adds another quality layer. Each finished lot links supplier records, compost batch, formulation, pelletizing conditions, post-coating batch and packing date. The customer can then investigate a nutrient, contaminant or viability result without relying on operator memory.
| Quality Point | Typical Control | Commercial Reason |
|---|---|---|
| Incoming organics | Moisture, contamination, supplier identity and agreed analysis | Prevents unsuitable material entering the normal route |
| Mature compost | Temperature trend, odor, moisture, structure and laboratory checks | Confirms readiness for formulation |
| Prepared formula | Batch weights and required nutrient analysis | Keeps fertilizer declaration repeatable |
| Pellet quality | Diameter, fines, breakage, moisture and cooling condition | Protects handling and bag stability |
| Microbial finish | Strain-specific viable-count and application records where claimed | Supports guarantee and shelf-life validation |
| Finished release | Label, lot code and retained sample | Connects saleable product to the production record |
Cold storage is not automatically better for every microbial product. Freeze-thaw exposure, warm warehouse periods and storage duration can affect different strains differently. The customer validates shelf life under the storage conditions stated on the Canadian label instead of publishing one universal viable-count guarantee for every microorganism.
RICHI MACHINERY
Wet-Side and Dry-Side Environmental Controls Stay Separate
Environmental control is concentrated at the material-transition points. Wet receiving and active composting use controlled surfaces, drainage and rapid incorporation into the aerobic process. Clean roof water is kept separate from manure-contact water where practical. Odor control is based first on short wet-residue residence, correct pile structure and aeration rather than on masking agents.
Dust control belongs in the dry workshop. Crushers, screens, transfer points and bagging use local extraction, while clean recoverable fines return only when they remain compatible with the registered formula. Noise is managed through indoor installation, equipment foundations and maintenance. The project does not publish one national odor or runoff limit because environmental approvals are province- and site-specific.
RICHI MACHINERY
Expansion Waits for a Proven Constraint
Execution begins with material characterization and product definition rather than machine fabrication. RICHI Machinery confirms incoming moisture ranges, fibre condition, annual dry matter, 6 mm product requirements, microbial-addition method, packing formats and available utilities before the detailed layout is frozen.
Mechanical manufacture and Canadian civil work can proceed in parallel after interface drawings are approved. Equipment ships from Qingdao, while the Canadian entry port and inland route are selected from the actual province, oversized-cargo plan and freight quotation. The case does not invent Vancouver, Montreal or another port without a confirmed site.
Commissioning starts with mature compost and one reference formula. The team tunes feeding, mixer discharge, FZLH load, pellet formation, cooling, screening and bagging first. Microbial post-addition is validated only after pellet temperature and moisture are stable. This reduces the number of variables introduced at the same time.
If sales exceed 30,000 T/A, expansion follows the first measured bottleneck. A second organic fertilizer granulator machine is justified only if mature-compost supply, dry preparation, cooling, microbial coating, packing and warehouse capacity can all support more pellets. Adding granulation before the biological section is ready would create expensive idle capacity.
For another Pig Manure and Mushroom Waste Fertilizer Plant in Canada, the first design inputs should be collectable pig-manure solids, spent mushroom substrate condition, brewery-residue distance, approved oilseed by-products, winter operating plan, composting land, finished fertilizer guarantee, microbial claim, package sizes and the local regulatory route. Those inputs determine the plant architecture more reliably than starting from a pellet-mill model.
● RICHI MACHINERY
RICHI Service

● Consulting
Customer Consultation
We want to have a deep understanding of your industrial process, to know your exact needs of feed, wood, biomass, fertilizer or other pellet processing.
● Design
fertilizer Pellet Plant Design
Based on your unique situation and industrial process, we will tailor complete pellet plant you need, and inform you of every additional detail that could facilitate operation, minimize total cost.

● Manufacturing
Equipment Manufacturing
The critical components of the of the complete pellet production line equipment are built in our own workshops in Asia. Additional equipment is manufactured by our worldwide network of reliable partners.

● Testing
Quality Inspection & Testing
Before leaving the factory, all equipment will be inspected by the quality inspection department. We can also provide customers with testing services from a single machine to a complete pellet plant system, and provide you with real actual data for “worry-free use.”

● Delivery
Equipment Delivery
In equipment boxing and packaging, we adopt professional packaging and modular solutions to ensure the safe and non-destructive delivery of pellet plant equipment.

● Installation
Installation & Commissioning
Whether you choose your own subcontractor for the erection phase or you want to install everything together with us, a Richi supervisor will be around to make sure everything is mounted in a safe and thorough way.

● Training
Staff Training
We provide comprehensive training for the technicians of each project. We can also continue to provide support for the technicians during latter project operation.

● After-sales
Project Follow-Up
When everything is up and running our Richiers will help you further whenever needed. We are ready to answer your call 24/7.We’ll also visit you regularly to learn about your needs.

Who we are
RICHI Machinery is one of the world’s leading suppliers of technology and services for the animal feed, aqua feed and pet food industries, also the largest pellet production line manufacturer in China.
Since 1995, RICHI’s vision to build a first-class enterprise, to foster first-class employees, and to make first-class contributions to society has never wavered.
In the past three decades, we have expanded our business to a wide range of areas, including animal feed mill equipment, aqua feed equipment, pet feed equipment, biomass pellet equipment, fertilizer equipment, cat litter equipment, municipal solid waste pellets equipment, etc.

1995
RICHI Established

2000+
Serving More Than 2000 Customers

120+
RICHI Employees

140+
Exported To 140 Countries



