 0086-138 3838 9622
2 T/H Wood Shavings Pellet Plant in Ireland
RICHI MACHINERY
Turning Cork Workshop Shavings Into Bagged Fuel
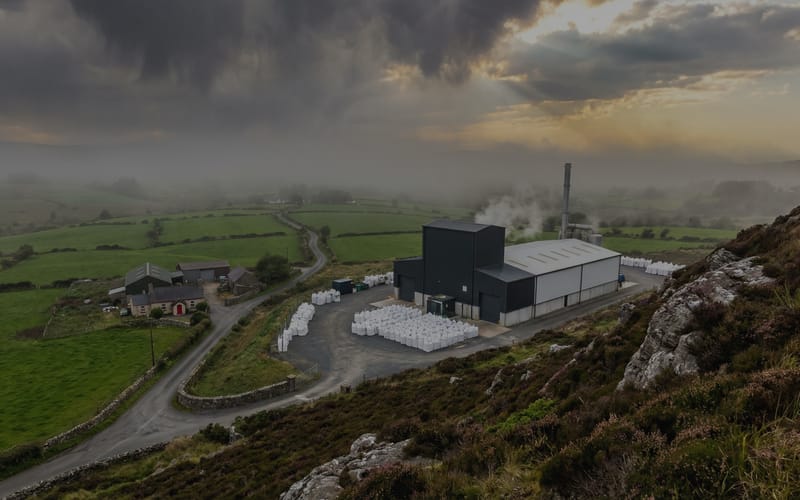
Loose wood shavings occupy valuable workshop space long before they weigh enough to fill a truck. This 2 T/H wood shavings pellet plant in Ireland gives a County Cork agricultural supplier a compact fuel product from clean furniture and sawmill residues. Two parallel presses produce 6 mm or 8 mm pellets, while covered receiving and enclosed feeding address the handling difficulties of light, dusty material.
The biomass pellet plant operates in a rented 1,060 m² ground-floor workshop with six staff. One eight-hour shift over 300 working days provides 2,400 scheduled hours. At the 2 T/H production rate, the schedule accommodates up to 4,800 tonnes before maintenance and cleaning stops. Raw-material deliveries and finished-stock movements are organised around this single-shift operation.
Incoming shavings contain approximately 8–12% moisture and measure roughly 5–20 mm in length. Their dry condition removes the need for a thermal dryer, while fine grinding prepares a consistent feed for the wood pellet mill. The compact route suits a customer adding fuel production inside an existing building without a large wet-material reception yard.
2T/H
capacity
$111,500
fixed investment
Ireland
location
Biofuel
project type
RICHI MACHINERY
A Cork Agricultural Supplier Moves Into Fuel Production
The customer brought fifteen years of agricultural supply experience to the project. That background provided access to local merchants and practical knowledge of seasonal deliveries. Four furniture factories and two sawmills within a 50 km collection radius formed the feedstock network. Turning shavings into bagged fuel added a manufactured product to the business while making use of its regional distribution experience.
Existing grid, municipal water and sewer connections supported installation in the leased building. RICHI arranged the grinding and press-feeding route around the available floor rather than requiring a taller new structure. For a wood pellet production line in Ireland, this approach directs capital towards processing equipment while keeping raw-material access and finished-bag dispatch on the same level. For a similar leased premises, the useful layout drawing shows clear door openings, columns, loading access and the routes used by other occupants. The equipment can then be placed around actual working space. A grinder that fits inside the floor outline still needs room for opening covers, changing screens and removing worn parts; allowing that access at layout stage reduces disruption during production.
The customer’s priority was a compact dry-feed installation: enough receiving space for low-density shavings, stable meal delivery to two presses and practical access for routine service.
Accepted feedstock excludes painted, coated, glued and chemically treated wood. The purchasing budget used US$20–25 per tonne delivered, with US$22 per tonne as the costing basis. Keeping the acceptance rules clear at the supplier reduces rejected loads and protects the finished fuel from contamination that grinding cannot remove.
RICHI sized the receiving, grinding and feed distribution around the two-press arrangement. One press can remain available while the other is serviced, although output then falls. This operating flexibility does not remove the need to stop for common equipment such as the grinder, feeder or extraction fan.
RICHI MACHINERY
A Local Collection Network With Short Stock Turnover
The client set up collection agreements with four furniture factories and two sawmills within a 50km radius.
| Raw Material | Annual purchasing allowance (tonnes) | As-Received Moisture | Cost (USD/ton) | Source |
|---|---|---|---|---|
| Clean wood shavings | 5,001 | 8-12% | $22 | Furniture factories and sawmills |
At US$22 per tonne, the 5,001-tonne purchasing allowance represents US$110,022 of annual material availability. Deliveries arrive loose or in reusable bags. The receiving team manages the volume of each load as well as its weight: light shavings can fill a storage bay quickly, and frequent deliveries leave more floor space for safe handling and bagged product. The 300 m² raw-stock allocation works as a receiving buffer rather than a seasonal store. Operators need access to older bags as well as fresh deliveries, so stock should remain reachable without moving the entire bay. Buyers with the same low-density material benefit from sending both a weighed sample and a bulk-volume measurement when requesting a layout. That information determines hopper and conveyor sizing more usefully than annual tonnage alone.
Production scheduling links accepted deliveries to the hours available on the line. The purchasing allowance provides flexibility for supplier timing, moisture variation and stock carried between periods. Finished-product yield is affected by moisture removal and screening; weighing inbound material and dispatched pellets gives the business a clear basis for stock control and unit-cost management.
RICHI MACHINERY
Omitting Drying Still Requires Moisture Control
A no-dryer shavings pellet plant in Ireland depends on keeping the low-moisture advantage from collection through storage. Rain exposure during loading can invalidate the process choice even when the wood was kiln-dried at the supplier.
Grinding preparation: The wood pellet hammer mill reduces the thin shavings to approximately 3–5 mm meal. Large offcuts are separated at receiving so that the grinder handles material suited to its inlet. Screen condition and consistent feeding help prevent sudden changes in press loading.
Moisture acceptance: Covered deliveries and indoor storage preserve the advantage of dry shavings. Wet bags are kept separate from the production supply. Operators adjust feeding to the accepted material and monitor pellet condition when a new supplier’s shavings enter the blend. A new supplier can change more than moisture: shaving thickness, wood species and the proportion of fine dust also influence feeding. Keeping those changes visible at receiving helps the operator make a controlled adjustment. Mixing an unfamiliar load into the whole stockpile removes that opportunity and can make a short feeding problem harder to trace.
The wood crusher and wood dryer are omitted from the dry-feed arrangement. Their absence reduces purchased equipment and eliminates dryer heat demand; it does not eliminate grinding electricity, extraction, cooling, moisture testing or the cost of protecting stock from rain.
RICHI MACHINERY
Two 90 kW Presses With a Common Grinding Stage
| Equipment | Quantity | Power | Function |
|---|---|---|---|
| Belt conveyor | 4 | 1.5kW each | Material transfer |
| Hammer mill | 1 | 75kW | Fine grinding to 3-5mm |
| Pellet mill bin – (enclosed) | 1 | — | Material holding |
| Biomass pellet mills – 90 kW each | 2 | 90kW each | Approximately 1 T/H per press on approved shavings |
| Screw feeder | 1 | 2.2kW | Material transfer to mills |
| Cyclone separator | 1 | 3.7kW | Pre-dust collection |
| Baghouse filter | 1 | 5.5kW | Final dust collection |
| Exhaust stack | 15m | — | Treated air discharge |
The equipment package cost US$95,000 on an ex-works basis. The customer’s investment also covered delivery and installation. Keeping those costs visible helps buyers compare machinery offers with the local work needed to put equipment into service inside an existing workshop.
A locally supplied loader handled receiving duties. Locating material handling support close to the customer simplifies servicing and leaves RICHI’s equipment scope focused on the grinding, pressing and extraction route.
Two 40-foot containers carried the equipment, departing on 15 September 2023 and arriving at Cork on 28 October 2023. Sea and inland transport accounted for US$4,500. Container unloading and workshop access were coordinated with the installation sequence to keep stored components clear of the production floor.
RICHI MACHINERY
Ground-Floor Storage Has to Match Light Shavings
The 1,060 m² leased floor is allocated between production and two storage zones. The 600 m² production allocation needs to include service clearance, extraction access and packing space. Raw and finished stocks should remain physically separate; loose dust should not be carried into the finished-product packing area. The finished-stock bay is close to dispatch so sealed bags have a short handling route. Pallets need a dry floor and space for inspection before loading. When evaluating another 2 T/H workshop, RICHI can compare loose receiving with bagged receiving and show how each choice changes labour, dust collection and the amount of usable storage left in the building.
| Area | Size (m²) | Function |
|---|---|---|
| Production area | ~600 | Hammer mill, pellet mills, bagging |
| Raw material storage | ~300 | Shavings storage – bagged |
| Finished goods storage | ~160 | Bagged pellets |
RICHI MACHINERY
A Short Route From Shavings to Dispatch
The shavings pellet production line in Ireland follows a short material route, with quality checks at receiving, grinding and product release. Shortening the route reduces handling stages but does not justify bypassing temperature or moisture control.
Receiving and Feeding
Workers open bags under extraction or unload accepted loose shavings into the receiving zone. Packaging and foreign objects are removed before the grinder. Even feed delivery limits motor-load surges and keeps both presses supplied.
Fine Grinding
The 75 kW hammer mill reduces shavings to approximately 3–5 mm meal. Routine sieve checks, hammer inspection and airflow maintenance keep particle preparation consistent as supplier material changes.
Ring-Die Pelleting
An enclosed buffer supplies two 90 kW units. Each wood pellet press handles approximately 1 T/H of accepted shavings, giving the installation its 2 T/H capacity. Separate dies provide the 6 mm and 8 mm product sizes.
Friction and pressure help the prepared wood form durable pellets. Operators use feed rate, motor load and pellet condition together when adjusting the machine. This gives the small team a practical way to keep the two presses balanced without relying on appearance alone. When one press begins drawing more current than the other on the same meal, the operator has a useful comparison point for checking feed distribution and wear. Common preparation makes that comparison easier. It also means that grinder maintenance should be scheduled before material quality drifts far enough to affect both machines.
Product Handling and Bagging
Temperature, moisture and fines determine when pellets are ready for 15 kg bags. Product handling gives heat time to dissipate before sealing, and packing staff separate loose fines from saleable product. For a comparable new installation, RICHI can specify dedicated cooling and screening to suit the packing duty.
RICHI MACHINERY
Where the Operating Budget Is Spent
Grinding and pressing account for the largest electrical duties. The equipment schedule contains 272.4 kW of connected motors across pressing, grinding, conveying, feeding and extraction. Energy cost follows running hours and load; material purchasing, six-person staffing, packaging and wear parts complete the day-to-day production budget.
| Cost Category | Basis | Cost driver | Operating consideration |
|---|---|---|---|
| Wood shavings | 5,001 tonnes/year allowance | US$110,022/year at US$22/tonne | Purchasing ceiling; actual use follows production |
| Electricity | Production energy in kWh | Supply tariff and running load | Grinding and pressing dominate motor demand |
| Labor (6 people) | Six-person operating team | Wages and employer costs | Receiving, production, packing and service coverage |
| Maintenance & spares | Wear parts and routine service | Wear rate and service intervals | Dies, rollers, screens, bearings and filters |
| Building lease | 1,060 m² rented floor | Rent and service charges | Keep access and storage space available |
| Cost per saleable tonne | Materials, energy, labour and site costs | Include packaging and delivered-product handling |
Product and sales planning:
| Product | Output basis | Price basis | Sales channel |
|---|---|---|---|
| 6 mm or 8 mm wood fuel pellets | Below 4,800 tonnes/year at 2 T/H | Bag format and delivery terms | Regional fuel distributors and merchants |
The customer’s unit-cost advantage comes from short local collection routes, dry feedstock and use of a rented building. Die life, consistent feeding and clean stock handling still affect the margin on every bag. For another small producer, these operating details are as important as the purchase price of the pellet presses. A practical production-cost record uses bags or tonnes released for sale as its denominator. Material waiting in a bin, hot pellets awaiting handling and fines returning to the process occupy equipment without yet becoming a dispatched product. Tracking these movements helps the small team identify whether a slow day starts at receiving, pressing or packing.
The project funding package totalled US$145,000: US$95,000 for machinery, US$4,500 for logistics, US$12,000 for installation and US$33,500 for working capital. Equipment, delivery and installation account for US$111,500 of fixed expenditure. Working capital supported materials and operating needs as production and customer deliveries built up.
RICHI MACHINERY
Matching Pellets to Irish Heating Buyers
A wood fuel pellet plant in Ireland needs product specifications agreed with the intended sales channel. Relevant buyer groups include:
- Local fuel distributors needing consistent bag weight and seasonal deliveries.
- Hardware and agricultural merchants needing durable bags and traceable batches.
- Commercial boiler operators specifying diameter, moisture, ash and fines.
- Household-fuel channels requiring documented product quality and suitable handling.
The Cork location suits regional replenishment, with delivery frequency adjusted to merchant storage and seasonal heating demand. The distribution programme includes:
- Distributor replenishment and covered pallet transport.
- Merchant deliveries matched to storage and order frequency.
- Direct retail deliveries with a clear product specification.
Expansion would require another check of grinding, extraction, power, cooling and packing capacity. A third press alone would not demonstrate a 3 T/H saleable line, and export planning needs a destination-specific product and delivery assessment. When planning a larger programme, compare the number of bags leaving the workshop with the press-room rate. Receiving access and a full finished-stock bay can stop production even while machinery remains available. RICHI can use a simple daily material schedule to compare an extra press with faster handling or additional storage, helping the customer put capital into the part of the workshop that will actually increase dispatch.
RICHI MACHINERY
Two Presses Give the Small Team Operating Flexibility
Splitting pressing duty between two machines lets the customer service one press while the other remains available. The shared grinder and feeding route keep the layout compact, and routine maintenance is scheduled around the common equipment.
Useful features:
- Dry accepted feedstock avoids a thermal dryer and its fuel system.
- Two presses allow partial production during a single-press service stop.
- A cyclone followed by a bag filter separates coarse particles from finer dust.
Daily production priorities:
- Packing capacity: 2 T/H in 15 kg bags requires about 134 filled bags per hour, plus sealing and stacking.
- Receiving moisture: measure representative samples and segregate wet deliveries.
- Feeder extraction: inspect hoods, joints, pressure drop and cleanout access.
RICHI MACHINERY
RICHI Scope and Site Interfaces
RICHI’s work on this biomass pellet project connected the customer’s dry feedstock with a compact two-press arrangement. The principal services covered:
- Process layout: a common grinding stage feeding two pellet presses.
- Equipment integration: conveyors, grinder, buffer, presses and extraction.
- Installation support: machinery alignment, feed distribution and safe access.
- Operator instruction: die service, feed adjustment, lockout and documented quality checks.
- Spares planning: dies, wear parts, bearings, belts and filter media matched to the actual machines.
RICHI MACHINERY
Specify the Shavings Before Pricing the Line
For a biomass pellet project using wood shavings in Ireland, an equipment quotation becomes useful when the input data resolves four practical questions:
- What are the lowest and highest measured moisture levels across deliveries?
- How much shavings volume can the covered storage hold at measured bulk density?
- Which pellet diameter, ash limit, fines limit and packing format do buyers require?
- How many productive hours are available after maintenance, cleaning and changeovers?
Send representative shavings samples, annual available tonnage, building dimensions and supply details. Include the intended heating application so that grinding, pressing, cooling and packing can be sized as one production system. For a replacement machine within an existing workshop, also include the conveyor discharge height, available motor supply and the condition of the downstream equipment. These details allow the proposed press to fit the process already in use and help keep the quotation focused on the work the customer actually needs.
Send RICHI your shavings samples and workshop drawing for a line matched to your material and dispatch target. The quotation can set out machinery, delivery, installation and operating-stock requirements so that the full cash commitment is clear.
● RICHI MACHINERY
RICHI Service
● Consulting
Customer Consultation
We want to have a deep understanding of your industrial process, to know your exact needs of feed, wood, biomass, fertilizer or other pellet processing.

● Design
biomass Pellet Plant Design
Based on your unique situation and industrial process, we will tailor complete pellet plant you need, and inform you of every additional detail that could facilitate operation, minimize total cost.
● Manufacturing
Equipment Manufacturing
The critical components of the of the complete pellet production line equipment are built in our own workshops in Asia. Additional equipment is manufactured by our worldwide network of reliable partners.
● Testing
Quality Inspection & Testing
Before leaving the factory, all equipment will be inspected by the quality inspection department. We can also provide customers with testing services from a single machine to a complete pellet plant system, and provide you with real actual data for “worry-free use.”
● Delivery
Equipment Delivery
In equipment boxing and packaging, we adopt professional packaging and modular solutions to ensure the safe and non-destructive delivery of pellet plant equipment.
● Installation
Installation & Commissioning
Whether you choose your own subcontractor for the erection phase or you want to install everything together with us, a Richi supervisor will be around to make sure everything is mounted in a safe and thorough way.
● Training
Staff Training
We provide comprehensive training for the technicians of each project. We can also continue to provide support for the technicians during latter project operation.
● After-sales
Project Follow-Up
When everything is up and running our Richiers will help you further whenever needed. We are ready to answer your call 24/7.We’ll also visit you regularly to learn about your needs.
Who we are
RICHI Machinery is one of the world’s leading suppliers of technology and services for the animal feed, aqua feed and pet food industries, also the largest pellet production line manufacturer in China.
Since 1995, RICHI’s vision to build a first-class enterprise, to foster first-class employees, and to make first-class contributions to society has never wavered.
In the past three decades, we have expanded our business to a wide range of areas, including animal feed mill equipment, aqua feed equipment, pet feed equipment, biomass pellet equipment, fertilizer equipment, cat litter equipment, municipal solid waste pellets equipment, etc.

1995
RICHI Established

2000+
Serving More Than 2000 Customers

120+
RICHI Employees

140+
Exported To 140 Countries