

 0086-138 3838 9622
5–6 T/H Wood Pellet Factory in Canada
A British Columbia project converting high-moisture sawmill residues into 8 mm industrial pellets with extended dryer operation and three MZLH520 pellet mills.
RICHI MACHINERY
Wet Fibre Makes the Dryer the Real Capacity Setter
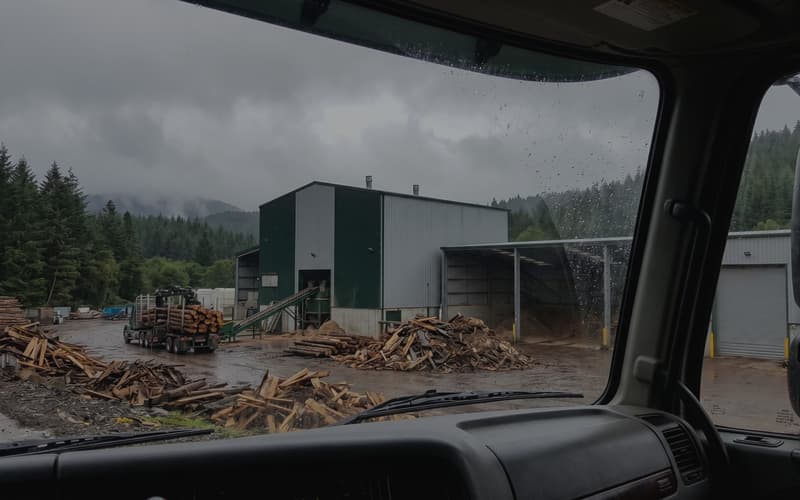
This 5–6 T/H wood pellet factory in Canada was built in the British Columbia interior for a sawmill operator with access to wet spruce, pine and fir residues. The plant is not sized from the dry pellet mills alone. Incoming chips, sawdust and offcuts arrive at roughly 38–42% moisture, so the first capacity question is how many wet tons can be dried every day without starving the pellet section.
The factory receives about 20,100 T/Y of wet wood residue. After moisture removal and normal screening loss, practical gross pellet output is about 13,800 T/Y. Around 600 T/Y is reused as biomass-furnace fuel, leaving roughly 13,200 T/Y of saleable 8 mm industrial pellets. The pellet section runs one 8-hour shift for about 300 days, while the dryer operates for a longer daily window to build a dry-material buffer ahead of the presses.
Three MZLH520 pellet mills, each rated at about 1.5–2.0 T/H with a 132 kW main motor, provide approximately 4.5–6.0 T/H of installed capacity. That range fits the corrected dry-ton balance far better than treating 20,100 wet tons as if they could become 15,000 saleable tons after drying. The completed fixed investment remains about US$530,000.
5–6 T/H
capacity
$530,000
investment
Canada
location
Biofuel
project type
RICHI MACHINERY
The Project Began With 40% Moisture Not With a Pellet Mill
The client had operated a British Columbia sawmill for years and already understood fibre quality. The opportunity came from residues that were difficult to monetize in wet form: sawdust, chips and clean offcuts from local mills. Moisture around 38–42% made transport inefficient and ruled out direct pelleting.
The 3,385 m² industrial site already had buildings, grid electricity, municipal water and enough yard access for trucks. Reusing that property kept civil work limited and allowed more of the US$530,000 fixed investment to go into drying, size reduction, dust control and the three-press pellet section.
The engineering question was whether a wood pellet production line in Canada could accept wet sawmill residues without turning the dryer into a permanent bottleneck.
Material samples contained clean spruce, pine and fir with no paint or adhesive contamination. The wood species were suitable for fuel pellets, but the moisture range made a dryer mandatory and required a different operating schedule from the pellet section.
The final answer was a wood pellet plant in British Columbia that runs the rotary dryer longer than the eight-hour pelleting shift. Dry material is buffered before pelleting, allowing three MZLH520 presses to work near a stable 5–6 T/H range even though the wet-fibre intake is much higher on a mass basis.
RICHI MACHINERY
Six Sawmill Contracts Matter More Than a Large Storage Yard
The customer arranged supply from six sawmills within roughly 100 km. That sourcing network reduces dependence on one mill, but it also means moisture and particle form can change between deliveries. Each incoming lot is therefore checked before it joins the wet-fibre stock.
| Raw Material | Annual Input (tons) | As-Received Moisture | Cost (USD/ton) | Source |
|---|---|---|---|---|
| Wood processing waste – chips, sawdust, offcuts | 20,100 | 38-42% | $25 | Six sawmills |
The delivered price basis is about US$25 per wet ton. For a sawdust pellet plant in Canada, the low purchase price only remains attractive if the dryer and storage system can handle seasonal moisture without excessive fuel use or frozen material blocking the feed system.
The mass balance is based on dry matter rather than a simple wet-input-to-pellet ratio. Around 20,100 tons of wet residue at roughly 38–42% moisture yields about 13,800 tons of gross pellets after drying to the normal pelleting and storage range:
- Water removed in drying: approximately 5,700–6,100 T/Y depending on the incoming moisture mix
- Screened fines and normal process loss: controlled and recycled where suitable rather than counted as a separate 500-ton waste stream
About 600 T/Y of the gross output is reserved for the wood chip dryer furnace. The remaining volume—about 13,200 T/Y on the design basis—is available for sale, so internal heat demand is visible in the production plan instead of being added on top of finished output.
RICHI MACHINERY
The Dryer Runs Longer Than the Pellet Shift
Wood residue at 38–42% moisture cannot feed a stable ring-die process. The target after drying is normally about 12–14%, giving the pellet mills enough moisture for compression while avoiding steam, cracking and storage condensation.
The plant uses one 6 T/H wet-input rotary drum dryer with a biomass furnace. To process the annual wet-fibre volume, the dryer operates roughly 11–12 hours on scheduled production days, while the pellet section works its normal 8-hour shift from the accumulated dry buffer.
Dryer operating basis:
- Type: Rotary drum with direct hot-air heating
- Capacity: approximately 6 T/H wet input
- Inlet moisture: typically 38–42%
- Outlet moisture: normally 12–14%
- Retention time: approximately 25–30 minutes, adjusted by actual moisture
- Furnace fuel: about 600 T/Y of self-produced pellets on the project basis
The dryer is the largest single process constraint in this 5–6 T/H wood pellet factory in Canada. Its furnace, ducting, cyclones and controls are included within the US$410,000 equipment package; the project does not treat the dryer alone as costing more than the entire equipment contract.
RICHI MACHINERY
Three MZLH520 Presses Match the Dry-Ton Balance
| Equipment | Quantity | Power | Function |
|---|---|---|---|
| Wood chipper machine | 1 | 110 kW | Primary reduction of offcuts and large chips |
| Wood pellet hammer mill | 1 | 160 kW | Fine grinding to about 4–5 mm |
| Rotary dryer | 1 | 45 kW + furnace | Reduce wet residue to about 12–14% moisture |
| Wood pellet mill | 3 × MZLH520 | 132 kW each | Approx. 1.5–2.0 T/H per press |
| Cyclones | 2 | 7.5 kW each | Primary separation on dryer and pneumatic air |
| Baghouse filters | 2 | 15 kW each | Fine dust collection |
| Exhaust stack | 15 m | — | Treated air discharge |
| Counterflow cooler + screener | 1 set | Project matched | Cool pellets and remove fines before packing |
| Septic system | 1 | — | Staff sewage |
Equipment package (EXW basis): approximately US$410,000
Shipping: Twelve 40-foot containers left Qingdao in September 2023 and arrived at Port of Vancouver, Canada in late October. The project basis includes about US$24,000 for ocean freight and about US$6,000 for onward transport to the British Columbia interior.
RICHI MACHINERY
The 3,385 m² Site Separates Wet Fibre From Finished Pellets
The 3,385 m² site reuses existing industrial buildings, but wet raw material and finished pellets are kept physically separated. This reduces moisture migration into bagged product and keeps the dryer/furnace zone away from finished-goods traffic. The 630 m² raw-material warehouse acts as a weather buffer rather than a long-term fibre yard: incoming residue is rotated by moisture condition, and frozen or snow-covered material cannot simply be pushed into the dryer at the same feed rate as summer sawdust. The 384 m² finished-goods area, by contrast, is reserved for cooled pellets and dispatch preparation, so wet-fibre forklifts do not cross the clean storage zone.
| Area | Size (m²) | Function |
|---|---|---|
| Steel-framed production building | 560 | Chipping, grinding, drying, cooling and wood pellet extruder machine area |
| Raw material warehouse | 630 | Wet wood residue buffering before drying |
| Finished goods warehouse | 384 | Dry 8 mm pellets for bagging and dispatch |
| Office | Existing | Administration, QC records and logistics |
RICHI MACHINERY
Wet Intake and Dry Pelleting Run on Different Clocks
The wood pellet production line in Canada is organized around a dry-material buffer between thermal drying and pelleting. That buffer prevents short dryer fluctuations from immediately changing pellet-mill feed.
Step 1 – Chipping
Large wet offcuts and oversize residue are reduced to roughly 20–30 mm chips before fine grinding.
Step 2 – Grinding
Prepared wood passes through the hammer mill to a typical 4–5 mm pellet-feed particle size. Fine sawdust can bypass unnecessary primary chipping when it already meets the feed requirement.
Step 3 – Drying
Wet material passes through the rotary dryer from roughly 38–42% toward 12–14% moisture. The dryer runs a longer daily schedule than the pellet presses and fills a dry buffer before the 8-hour pelleting shift.
Step 4 – Pelleting
Dried material feeds three wood pellet presses configured as MZLH520 units. Aggregate installed capacity is about 4.5–6.0 T/H, matching the corrected gross output of roughly 13,800 T/Y. The standard die produces 8 mm industrial pellets.
Step 5 – Cooling and screening
Fresh pellets enter a counterflow cooler before screening. Recoverable fines return to the process so hot pellets are not sent directly into bags or bulk storage.
Step 6 – Bagging and export
Finished pellets can be packed in smaller bags or bulk bags according to the customer order. Internal furnace fuel is deducted from saleable output before export planning.
RICHI MACHINERY
British Columbia Offers Fibre but Supply Security Cannot Be Assumed
Canada has an established wood-pellet industry and British Columbia has long supplied pellets from forest and sawmill residuals. For a new industrial wood pellet plant in Canada, however, the current planning issue is not simply “abundant fibre”; it is securing enough consistent residue from operating mills.
- Long-term sawmill contracts are more important than relying on spot residue availability
- Port of Vancouver provides an established route for export-oriented biomass products
- Domestic industrial and heating users provide an alternative to a single export destination
- Environmental permitting, dust control and fibre traceability need to be addressed at project level rather than assumed from a general incentive program
The project therefore treats export as one sales route, not as a guarantee of margin. Feedstock security, drying cost, shipping contracts and customer specification all affect whether a British Columbia wood pellet factory remains competitive. Pellet diameter, ash, moisture, durability and traceability still have to match the receiving customer’s specification, and the business needs enough dry storage to hold production when vessel or rail schedules move. For a plant of this scale, a delayed shipment can tie up a large share of finished-goods space long before it creates a mechanical production problem.
RICHI MACHINERY
Three Operating Lessons Came From the First Winter
Early operation confirmed that wet-fibre management is more important than chasing the top pellet-mill rating. The main lessons were practical. Winter residue can arrive colder, wetter and more variable than summer fibre; dryer settings that work in August are not automatically suitable in January. The operator therefore records receiving moisture, dryer inlet/outlet condition, dry-buffer level, MZLH520 motor load and cooler discharge temperature as linked production variables rather than separate machine readings.
What proved important:
- The dryer schedule has to stay ahead of the pellet shift so the presses receive stable dry material rather than alternating wet batches.
- Three MZLH520 presses give maintenance flexibility; one press can be stopped while the others keep limited output available.
- Wet-fibre storage and snow or freeze protection need as much planning attention as the production building.
Future expansion checks:
- Dryer hours and buffer volume must be increased before adding pellet-mill capacity.
- Covered raw-material storage should expand if winter inventory days increase.
- Export documentation and inland transport should be managed as a dedicated logistics function once annual sales grow.
RICHI MACHINERY
RICHI Scope Was Built Around Wet-Fibre Conversion
For this 5–6 T/H wood pellet factory project in Canada, the supplied scope focused on turning variable wet residue into a stable dry feed for pelleting. That includes the interfaces between wet-fibre storage, coarse size reduction, the long-running dryer, dry buffering, three parallel presses and downstream cooling. On a project where the thermal section works more hours per day than pelleting, controls and bin capacity are part of throughput planning: the customer needs enough dry material in reserve to start the pellet shift without waiting for the dryer, but not so much that warm or overdried fibre sits unnecessarily before compression.
- Process design – Complete wood pellet production line with extended dryer scheduling and dry-material buffering.
- Equipment package – Chipper, hammer mill, rotary dryer, three wood granulator machines, cooling, cyclones and baghouses.
- Installation supervision – Site support for equipment alignment, hot-air ducting, dust extraction and startup.
- Operator training – Moisture measurement, dryer control, MZLH520 loading, cooling and maintenance routines.
- Spare parts kit – Ring dies, rollers, hammer-mill wear parts, bearings, belts and filter bags for initial operation.
RICHI MACHINERY
Size a Canadian Pellet Factory From Dry Tons Not Wet Tons
If you are evaluating a wood pellet factory in Canada with wet sawmill residue, calculate the dry-matter balance before choosing a pellet mill. A 20,000-ton wet-fibre supply can support a much smaller finished-pellet volume once water and internal furnace fuel are removed. The same calculation should be repeated for the wettest month, not only for the annual average. If the feedstock moves from 38% toward 45% moisture, the dryer sees more water per ton of dry wood, fuel demand rises, and the hourly wet-input rate may need to fall even though the three MZLH520 presses are mechanically unchanged.
- Dryer capacity must be matched to wet-ton input. A 6 T/H wet-input dryer can support this project only because it operates longer each day than the pellet section.
- Internal furnace fuel belongs in the product balance. Pellets burned for drying are operating fuel, not saleable output.
- Fibre contracts matter more than generic market size. A biomass pellet plant in Canada needs secure mill residues before export orders can be treated as dependable capacity.
- Cooling and dust control should be sized as production equipment. They protect storage quality and plant housekeeping at the same time.
The project is therefore a 5–6 T/H dry-pellet factory supported by a longer-running wet-fibre drying section, not a 6 T/H wet-input line that magically turns every incoming ton into product.
For a similar wood pellet plant construction project, provide annual wet feedstock tonnage, moisture by season, dry-fibre storage days, pellet diameter, operating shifts and target customers. Those values determine the dryer, buffer and pellet-mill combination more reliably than one nominal T/H figure.
● RICHI MACHINERY
RICHI Service

● Consulting
Customer Consultation
We want to have a deep understanding of your industrial process, to know your exact needs of feed, wood, biomass, fertilizer or other pellet processing.
● Design
biomass Pellet Plant Design
Based on your unique situation and industrial process, we will tailor complete pellet plant you need, and inform you of every additional detail that could facilitate operation, minimize total cost.

● Manufacturing
Equipment Manufacturing
The critical components of the of the complete pellet production line equipment are built in our own workshops in Asia. Additional equipment is manufactured by our worldwide network of reliable partners.

● Testing
Quality Inspection & Testing
Before leaving the factory, all equipment will be inspected by the quality inspection department. We can also provide customers with testing services from a single machine to a complete pellet plant system, and provide you with real actual data for “worry-free use.”

● Delivery
Equipment Delivery
In equipment boxing and packaging, we adopt professional packaging and modular solutions to ensure the safe and non-destructive delivery of pellet plant equipment.

● Installation
Installation & Commissioning
Whether you choose your own subcontractor for the erection phase or you want to install everything together with us, a Richi supervisor will be around to make sure everything is mounted in a safe and thorough way.

● Training
Staff Training
We provide comprehensive training for the technicians of each project. We can also continue to provide support for the technicians during latter project operation.

● After-sales
Project Follow-Up
When everything is up and running our Richiers will help you further whenever needed. We are ready to answer your call 24/7.We’ll also visit you regularly to learn about your needs.

Who we are
RICHI Machinery is one of the world’s leading suppliers of technology and services for the animal feed, aqua feed and pet food industries, also the largest pellet production line manufacturer in China.
Since 1995, RICHI’s vision to build a first-class enterprise, to foster first-class employees, and to make first-class contributions to society has never wavered.
In the past three decades, we have expanded our business to a wide range of areas, including animal feed mill equipment, aqua feed equipment, pet feed equipment, biomass pellet equipment, fertilizer equipment, cat litter equipment, municipal solid waste pellets equipment, etc.

1995
RICHI Established

2000+
Serving More Than 2000 Customers

120+
RICHI Employees

140+
Exported To 140 Countries



