

 0086-138 3838 9622
Biosolids and Cattle Manure Feedstock Plant in Brazil
RICHI MACHINERY
The Gatekeeping Rule Comes before the Mixer
The first design decision in this biosolids and cattle manure feedstock plant in Brazil is what the factory refuses to accept. The customer is an organic-waste recycling company supplying conditioned material to commercial vermicomposting operators. Its value does not come from receiving any wet municipal residue that arrives at the gate.
It comes from converting approved biosolids and mechanically manageable cattle manure into a traceable, more uniform loose feedstock that downstream earthworm facilities can evaluate and use within their own biological process.
The plant prepares about 30,000 T/A and operates a 10–15 T/H receiving and mixing route. At roughly 300 operating days and one eight-hour preparation shift, the annual target requires an average of about 12.5 T/H during scheduled mechanical hours. That puts the project near the middle of its commercial capacity range and leaves room for truck timing, batch checks, washdown, mixer cleaning and short interruptions without turning the facility into a continuous 24-hour waste-handling site.
There is no pelletizer, rotary dryer or process boiler in the first phase. The output is not finished vermicompost and is not marketed as bagged fertilizer. The factory stops at controlled feedstock preparation, after which the material is dispatched to separate vermiculture sites for further stabilization and earthworm processing. This boundary is central to the engineering scope because it keeps an industrial receiving-and-mixing operation from being confused with a land-intensive biological production system.
RICHI supplies approximately USD 280,000 of material-handling, dosing, mixing, conveying, odor-control interfaces and electrical/PLC equipment for this phase. Land, local buildings, utility connection, transport fleet and the downstream vermicomposting beds are outside that equipment-and-engineering figure. The page therefore does not convert a machinery package into a false total-project investment.
10–15 T/H
preparation capacity
USD 280,000
RICHI supply
Brazil
location
30,000 T/A
prepared feedstock
RICHI MACHINERY
Daily Throughput Is a Logistics Calculation
For this customer, capacity begins with a daily logistics question: can about 100 tonnes of acceptable material move through the gate, be checked, mixed and leave again without creating a wet stockpile? The 30,000 T/A target corresponds to about 100 tonnes per operating day. The line can process more than that during a strong hour, but daily output is deliberately governed by approved supplier deliveries and confirmed downstream demand rather than by keeping mixers full regardless of where the material will go.
| Operating Layer | Project Basis | What Controls It |
|---|---|---|
| Annual prepared output | Approx. 30,000 T/A | Supply contracts and downstream vermicomposting demand |
| Mechanical preparation | 10–15 T/H | Hopper feeding, mixer duty and wet-material flow |
| Scheduled mechanical time | Approx. 2,400 h/year | One main 8 h shift × about 300 days |
| Average required output | Approx. 12.5 T/H | 30,000 tonnes divided by scheduled hours |
| Normal inventory | Short operating buffer | Truck sequence rather than long-term sludge storage |
| Finished form | Loose conditioned feedstock | Dispatched before vermicomposting |
That operating model is why the organic fertilizer production project uses fast turnover rather than a large warehouse. Incoming biosolids are not treated like dry grain that can remain on site for months. The commercial rhythm is approve → unload → dose → mix → release → dispatch. If downstream beds slow down, inbound deliveries must be rescheduled before the preparation plant becomes a storage facility for wet organic waste.
RICHI MACHINERY
Biosolids Must Arrive with Their Compliance History
Municipal biosolids are the most tightly controlled incoming stream. Brazil’s CONAMA Resolution 498/2020 distinguishes treated biosolids by quality and requires management of pathogen reduction, vector-attraction reduction, chemical substances and microbiological quality for biosolids destined to soil use. Mixing cattle manure into a biosolids cake does not replace those supplier-side controls.
The preparation plant therefore requires documentation and lot identification before material enters the normal production route.
The receiving specification focuses on origin, solids or moisture condition, treatment history, microbiological status, relevant chemical characterization and consistency between deliveries. Industrial sludge, unidentified mixed sludge and loads that do not match the approved supply profile are excluded. A loader can physically move a rejected material and a mixer can physically blend it, but neither machine can make an unsuitable biosolids stream compliant or biologically appropriate for downstream vermiculture.
| Incoming Stream | Role in the Blend | Acceptance Focus | Handling Route |
|---|---|---|---|
| Qualified municipal biosolids | Main moist organic base | Origin, treatment, lot records, microbiological and chemical quality | Covered receiving and controlled dosing |
| Cattle manure | Structure and organic co-feedstock | Moisture, bedding, soil, foreign matter and supplier consistency | Separate buffer and metered addition |
| Approved microbial or process additive | Optional process support | Documented product and validated use | Small-dose controlled addition |
| Rejected foreign material | No production role | Plastic, metal, stones or unapproved contaminants | Segregated disposal route |
Brazil’s cattle sector also makes manure sourcing commercially plausible without requiring one exceptional farm. The customer can qualify dairy and cattle operations, collection contractors or agricultural-waste processors within a practical hauling radius. What matters is that the manure is shovelable or otherwise mechanically manageable.
Dilute slurry is avoided because transport cost rises rapidly when the payload is mostly water and because the preparation line is designed for wet solids, not tanker-fed liquid manure.
RICHI MACHINERY
Cattle Manure Changes the Blend Rather Than the Legal Status
Cattle manure is not included as a cosmetic “natural” ingredient. It changes the physical character of the blend. Dewatered biosolids can be dense, sticky and difficult to distribute evenly, while manure with suitable fiber or bedding can improve structure and handling. The project therefore adjusts the blend from actual incoming condition rather than publishing one permanent biosolids-to-manure percentage that would become wrong as soon as a supplier changes dewatering performance.
- Moisture determines whether the blend remains loadable and suitable for the downstream vermiculture route.
- Bedding and fiber affect porosity, mixer behavior and the physical structure delivered to the worm-bed operator.
- Visible contamination and soil content influence both equipment wear and the acceptability of the resulting feedstock.
- Supplier consistency affects how often the customer has to change dosing settings and downstream quality checks.
Microbial additives are optional rather than automatic. They are used only when the customer’s downstream biological program has a defined reason for them and when the product is appropriate for the intended process. The line therefore includes controlled small-dose capability without claiming that an inoculant can compensate for poor-quality biosolids, unsuitable manure or inadequate vermicomposting conditions.
RICHI MACHINERY
Six Operations Take the Material from Truck to Dispatch
The production sequence is intentionally short because every extra transfer of sticky wet material creates another cleaning and odor-control point. The line does not grind the entire stream into powder, does not thermally dry it and does not try to complete biological stabilization in a few minutes. Its job is to standardize physical handling and batch composition before transport.
- Verify the incoming truck against the approved supplier and batch documents before unloading.
- Unload biosolids and cattle manure into separate covered short-term receiving areas so the operator can control each main stream independently.
- Remove obvious foreign objects and meter the two bulk materials through loader-fed hoppers or controlled feeders.
- Blend the batch in heavy-duty organic-material mixers, adding only approved small-dose materials required by the customer’s process.
- Check moisture, consistency and batch identity, then move the accepted blend to a short dispatch buffer.
- Load covered vehicles and transfer the prepared feedstock to the downstream vermicomposting site.
This route is shorter than a conventional organic fertilizer production line because there is no compost-finishing, granulation, cooling, screening or bagging stage in phase one. The shorter route is not a missing section. It reflects the product boundary: the plant sells conditioned biological feedstock, while the downstream operator supplies the residence time, worm-bed management and final vermicompost harvesting.
RICHI MACHINERY
Equipment Is Chosen for Sticky Wet Solids
Equipment is selected for wet, variable-density material rather than copied from a dry fertilizer or animal-feed plant. Receiving hoppers have to accept loader-fed material without creating inaccessible corners. Feeders must control discharge from sticky solids. Mixers need torque, open access and a discharge geometry that can clear cohesive material. Belt or other low-impact conveyors are preferred where they reduce smearing and buildup compared with unnecessarily complex transfer systems.
| Mechanical Duty | Main Equipment | Typical Qty. | Selection Reason |
|---|---|---|---|
| Biosolids receiving | Loader-fed receiving hopper | 1 | Controlled wet-material intake |
| Manure receiving | Separate buffer hopper | 1 | Independent manure dosing |
| Foreign-object control | Coarse separator and inspection point | 1 set | Protects mixers and conveyors |
| Bulk dosing | Variable feeding systems | 2 sets | Adjusts major-material ratio by batch |
| Wet mixing | Heavy-duty organic-material mixers | 2 | Parallel duty, cleaning access and production continuity |
| Small-dose addition | Controlled additive unit | 1 | Only for approved process additions |
| Transfer | Belt conveyors and loading interfaces | As required | Moves sticky material with fewer enclosed dead zones |
| Odor control | Local extraction and treatment interface | 1 set | Targets receiving and mixing sources |
| Drainage | Contact-water sump and pumps | 1 set | Keeps contaminated water out of clean stormwater |
| Electrical control | MCC and PLC system | 1 set | Interlocks feeders, mixers and conveyors |
Two parallel mixers are useful because this process is driven by batch consistency and cleanout rather than one enormous continuous mixing chamber. One unit can be inspected or washed while the other remains available for limited production. The layout also reduces the temptation to overload a single mixer simply to chase a theoretical hourly number. Sustainable 10–15 T/H output has to include loading, mixing, discharge and cleaning—not only the few minutes when paddles are turning.
RICHI MACHINERY
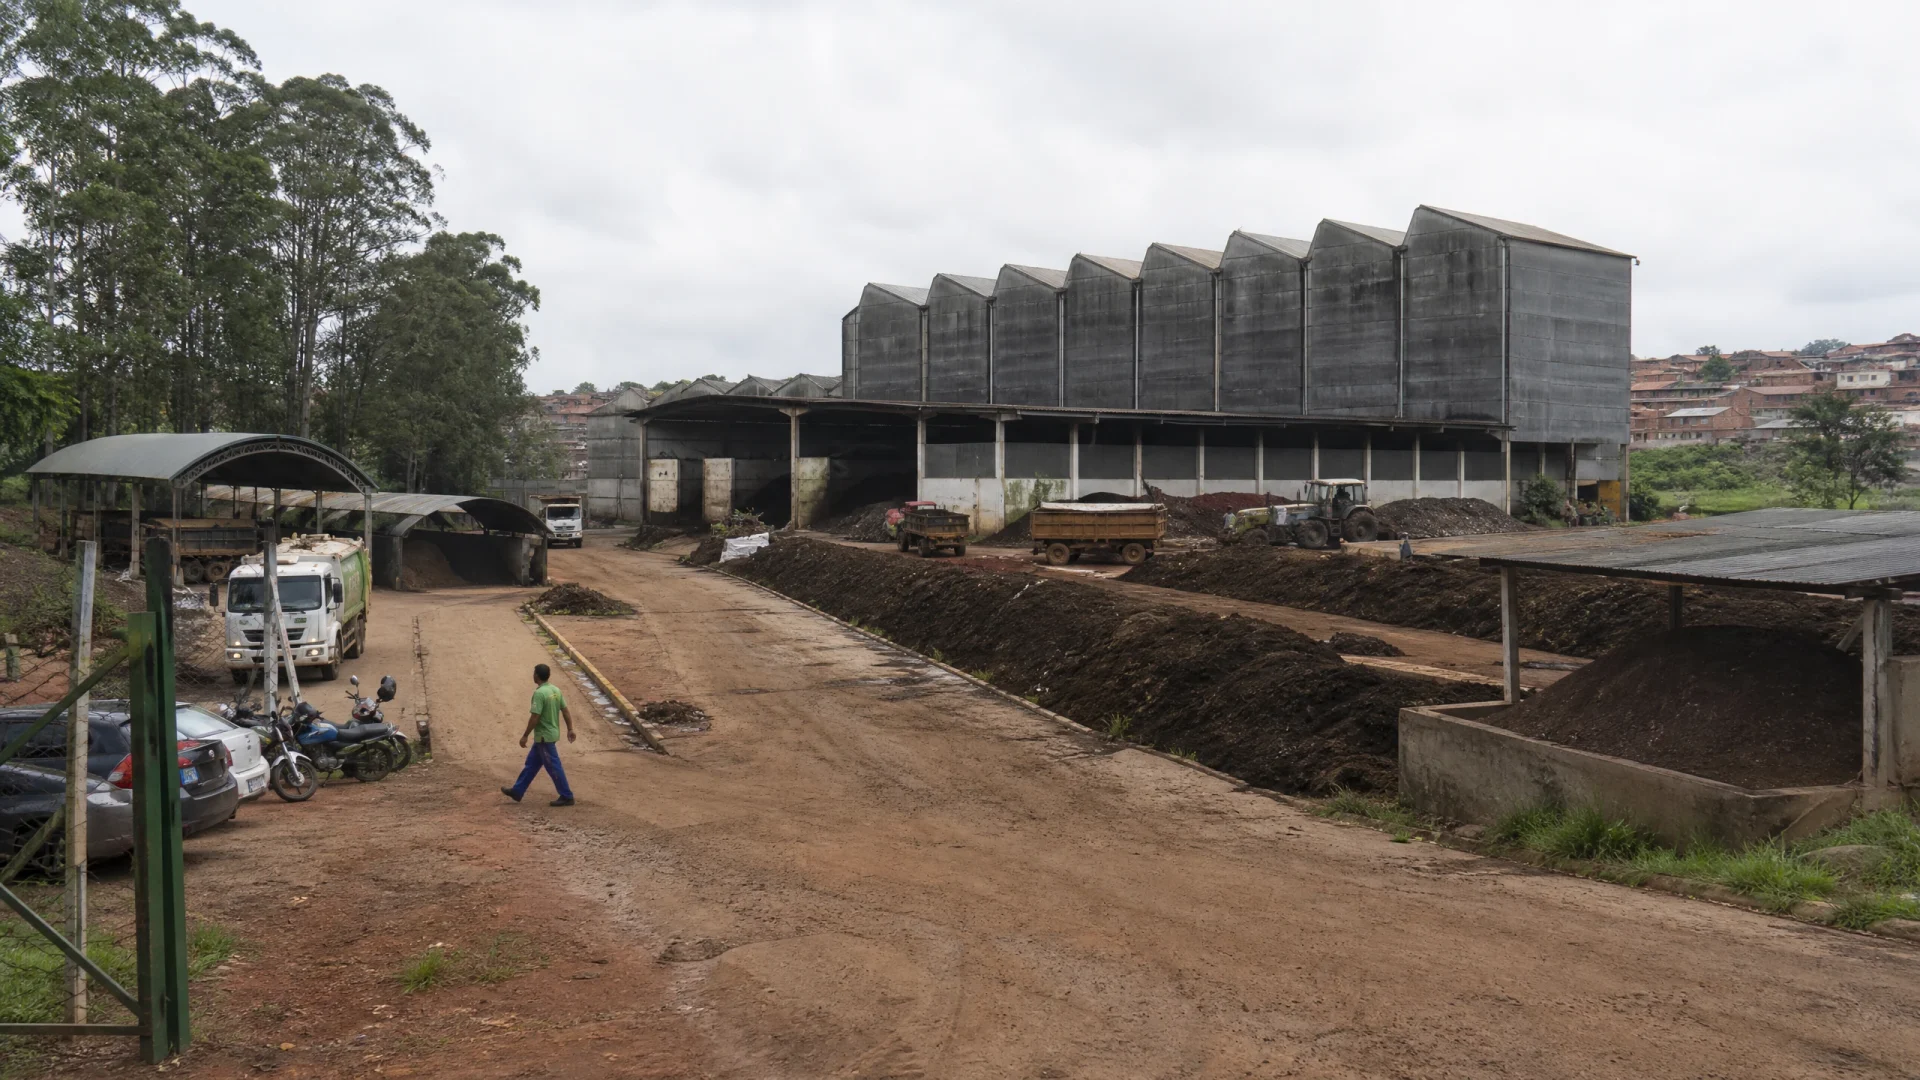
The Site Works Like a Controlled Transfer Station
The site is designed around truck paths and contact-water control. Wet receiving sits near the inbound side so biosolids do not cross the whole property before unloading. The mixing workshop sits between the two raw-material buffers and the dispatch zone. Prepared feedstock leaves through a covered loading area that can operate without blocking incoming vehicles. Where the owner’s commercial settlement requires verified tonnage, a weighbridge can be added to the traffic loop.
| Functional Zone | Planning Area | Site Logic |
|---|---|---|
| Covered biosolids receiving | 500–700 m² | Fast unloading, impermeable floor and controlled drainage |
| Cattle-manure buffer | 400–600 m² | Separate supplier lots and dosing control |
| Dosing and mixing workshop | 700–900 m² | Two mixers, feeders, conveyors and maintenance access |
| Prepared-feedstock buffer | 500–700 m² | Short residence before truck loading |
| Loading and dispatch | 500–700 m² | Covered vehicle interface and traffic separation |
| Utilities, maintenance and QC | 250–350 m² | Electrical, samples, tools and staff support |
| Roads, drainage and circulation | Remaining land | Truck turning, fire access and clean/dirty water separation |
A total site of about 4,000–5,500 m² is therefore reasonable for this preparation-only business. It is much smaller than an integrated vermicomposting estate because worm beds are elsewhere, but larger than a simple mixer shed because wet receiving, traffic, drainage, quality-control space and short-term buffers all need room. Rainfall affects civil design more than process heat: roof runoff should stay separate from areas where water contacts biosolids or manure.
RICHI MACHINERY
Utilities Stay Mechanical and One Shift Keeps Labor Lean
There is no production boiler. Electricity drives mixers, feeders, conveyors, pumps, ventilation and controls, while fuel combustion would add cost and permitting work without serving a process step. A reasonable simultaneous mechanical load is about 110–160 kW once the final mixer drives, conveying lengths and odor-control equipment are fixed. Because not every motor runs at full load during every scheduled hour, annual electricity is planned from duty cycles rather than from connected load alone.
A working annual electricity range of roughly 250,000–400,000 kWh is appropriate for early utility planning, but the final figure must follow the confirmed motor list and measured utilization. Brazil operates a 60 Hz electrical system, while site voltage and transformer requirements vary by local distribution network. The project therefore specifies motor frequency and protection correctly but confirms service voltage against the actual utility connection instead of copying one voltage from another Brazilian state.
Water demand is comparatively low but not zero. The process does not add water as a bulk ingredient, yet the facility still needs cleaning, wheel-wash where required, staff water, maintenance and possibly an odor-control spray or scrubber. About 500–900 m³/year is a practical non-fire planning range for a clean, well-managed site. Fire-water storage and emergency supply are designed separately and are not hidden inside ordinary process consumption.
A direct workforce of about 12–16 people fits one-shift preparation: operations coordination, receiving/QC, loader operation, mixing and feeding, dispatch, maintenance and environmental/safety support. Laboratory testing, trucking or specialized maintenance can remain contracted if the customer’s business model already uses external providers. The staffing number is therefore linked to which services stay in-house rather than to a generic headcount per tonne.
RICHI MACHINERY
Traceability Continues after the Truck Leaves
Quality control protects the downstream earthworm operation before it protects the machine. Every batch links an approved supplier to an incoming lot, a blend record and a dispatch destination. The customer retains the treatment and characterization documentation required for the biosolids stream and adds its own receiving observations for moisture, physical condition and contamination.
Cattle manure is also recorded by source because an unexpected change in bedding, soil or moisture can alter the blend even when the biosolids lot stays constant.
CONAMA Resolution 498/2020 requires biosolids management to address pathogen reduction, vector attraction, chemical substances and microbiological quality for biosolids intended for soil use. It also classifies biosolids into Class A and Class B with different use restrictions. The preparation plant therefore does not describe mixing as a treatment shortcut.
Only biosolids accepted through the applicable licensed and documented route enter the normal process, and the downstream operator remains responsible for the additional vermicomposting stage and its own permitted use.
If the downstream business later sells vermicompost as a fertilizer, soil conditioner or related agricultural input, that commercial product falls under Brazil’s MAPA fertilizer framework rather than becoming automatically marketable because earthworms processed the feedstock. Establishment registration, product requirements, analytical documentation and labeling depend on the final commercial category.
Keeping that boundary clear protects both the recycling company and its customers from calling an intermediate material a finished registered fertilizer.
RICHI MACHINERY
Odor Drainage and Storage Are Managed at the Wet End
Environmental control is concentrated where the material is wettest. Receiving and mixing use impermeable floors, managed contact-water collection and rapid housekeeping. Roof water and clean stormwater are diverted away from wet-material areas. Local ventilation or odor extraction is applied where the building configuration requires it, and the plant keeps raw-material residence short so odor control does not depend on masking a large stockpile.
Foreign objects removed at the receiving gate leave through a separate waste route rather than being returned to the blend.
The project does not claim that odor can be eliminated by landscaping or by adding microbes. The practical hierarchy is supplier control, fast turnover, covered unloading, clean floors, controlled drainage, ventilation and treatment where necessary. The same logic applies to spills: containment and recovery are designed into the wet zone so a truck or mixer problem does not automatically become a stormwater incident.
Prepared feedstock is stored only long enough to organize transport. It leaves loose in covered vehicles because bagging would add cost without helping the downstream worm-bed operator. If the receiver needs a different moisture or pre-stabilization condition, that becomes part of the commercial specification and the operating route is adjusted before dispatch. The plant’s job is repeatable preparation and logistics, not long-term wet-product warehousing.
RICHI MACHINERY
The First Investment Stops before Vermicompost Finishing
The USD 280,000 RICHI scope is concentrated on the mechanical bottleneck: receiving, metered feeding, two wet-material mixers, transfer, dispatch interfaces, drainage-related equipment, local odor-control interfaces and electrical/PLC integration. A dryer, boiler, cooler and packing line are absent because the phase-one product does not require them. Spending on equipment that does not change feedstock quality or throughput would only make the first investment harder to recover.
Execution begins with supplier and downstream-route confirmation before fabrication. The customer needs approved biosolids sources, a defined manure network and real vermicomposting capacity before a 15 T/H mechanical package creates value. RICHI then freezes the receiving geometry, mixer duty, conveyor arrangement, clean/dirty drainage interfaces and electrical load.
Equipment ships from Qingdao, while the Brazilian seaport and inland transport route are selected for the plant’s actual state and road distance instead of being guessed from the country name alone.
Commissioning uses approved project materials. Operators first test hopper discharge and mixer behavior at moderate loading, then adjust feed rates, batch size, mixing time, additive dosing, discharge sequence and conveyor speed. Throughput is increased only after the prepared feedstock is physically consistent and the line can cleanly complete repeated batches. This is more useful than proving an unloaded mixer can turn fast enough to display a high nominal capacity.
A later integrated vermicompost business can add screening, moisture adjustment, formulation and an organic fertilizer pellet mill only after enough mature worm castings exist to support that investment. Wet feedstock preparation capacity and dry fertilizer pellet capacity are not the same number. The future pellet line must be sized from mature vermicompost tonnage, moisture and commercial product demand rather than from the 10–15 T/H wet receiving rate.
For another biosolids and cattle manure feedstock plant in Brazil, RICHI Machinery needs the biosolids treatment status, annual wet tonnage, solids content, cattle-manure source, downstream vermicomposting method, daily transport plan, site dimensions and local power conditions before fixing equipment. Those inputs determine whether a short preparation plant is commercially sensible or whether the customer actually needs a larger integrated composting, vermicomposting and fertilizer-finishing project.
● RICHI MACHINERY
RICHI Service

● Consulting
Customer Consultation
We want to have a deep understanding of your industrial process, to know your exact needs of feed, wood, biomass, fertilizer or other pellet processing.
● Design
fertilizer Pellet Plant Design
Based on your unique situation and industrial process, we will tailor complete pellet plant you need, and inform you of every additional detail that could facilitate operation, minimize total cost.

● Manufacturing
Equipment Manufacturing
The critical components of the of the complete pellet production line equipment are built in our own workshops in Asia. Additional equipment is manufactured by our worldwide network of reliable partners.

● Testing
Quality Inspection & Testing
Before leaving the factory, all equipment will be inspected by the quality inspection department. We can also provide customers with testing services from a single machine to a complete pellet plant system, and provide you with real actual data for “worry-free use.”

● Delivery
Equipment Delivery
In equipment boxing and packaging, we adopt professional packaging and modular solutions to ensure the safe and non-destructive delivery of pellet plant equipment.

● Installation
Installation & Commissioning
Whether you choose your own subcontractor for the erection phase or you want to install everything together with us, a Richi supervisor will be around to make sure everything is mounted in a safe and thorough way.

● Training
Staff Training
We provide comprehensive training for the technicians of each project. We can also continue to provide support for the technicians during latter project operation.

● After-sales
Project Follow-Up
When everything is up and running our Richiers will help you further whenever needed. We are ready to answer your call 24/7.We’ll also visit you regularly to learn about your needs.

Who we are
RICHI Machinery is one of the world’s leading suppliers of technology and services for the animal feed, aqua feed and pet food industries, also the largest pellet production line manufacturer in China.
Since 1995, RICHI’s vision to build a first-class enterprise, to foster first-class employees, and to make first-class contributions to society has never wavered.
In the past three decades, we have expanded our business to a wide range of areas, including animal feed mill equipment, aqua feed equipment, pet feed equipment, biomass pellet equipment, fertilizer equipment, cat litter equipment, municipal solid waste pellets equipment, etc.

1995
RICHI Established

2000+
Serving More Than 2000 Customers

120+
RICHI Employees

140+
Exported To 140 Countries



