

 0086-138 3838 9622
Biomass Bedding Plant for Combined Biomass Resources in Austria
RICHI MACHINERY
Project Overview
An Upper Austrian entrepreneur developed this Biomass Bedding Plant for Combined Biomass Resources in Austria to convert local straw, sawdust and clean untreated wood residues into animal bedding pellets for dairy farms, horse stables and poultry houses. The project was designed as a bedding business from the start, so product cleanliness, low loose dust, storage efficiency and break-down after wetting matter more than fuel-pellet density or combustion performance.
Annual finished output is 9,000 T/A. The plant operates two 8-hour shifts for about 330 days, giving 5,280 scheduled production hours and an average required output of about 1.70 T/H. One MZLH520 biomass ring-die pellet mill, rated at 1.5–2 T/H with a 132 kW main motor, is therefore a realistic production core for the project.
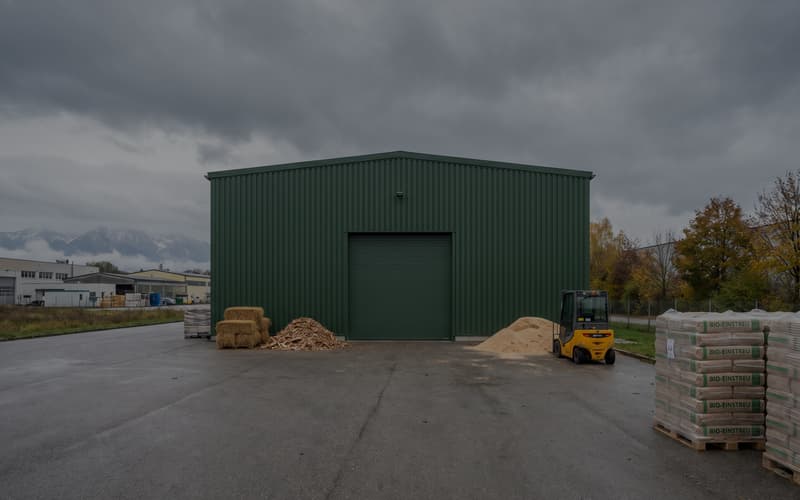
The project occupies about 2,000 m² within an existing industrial complex roughly 50 km southwest of Linz. Around 1,400–1,450 m² is covered production, storage and service space; the balance is used for truck access, short-term unloading, fire clearance and circulation. The single-story steel building has about 8 m clear height.
The fixed completed-project investment is USD 168,000, including a USD 112,000 RICHI equipment package. The corrected scope includes material-specific pre-processing, grinding, magnetic protection, metering, MZLH520 pelleting, mechanical cooling, screening, dust collection and semi-automatic packing. About 8–10 employees cover two-shift production, warehouse handling, packing, maintenance and administration.
1.5–2T/H
capacity
$168,000
investment
Austria
location
Bedding
project type
RICHI MACHINERY
Why Austria Has a Practical Market for Bedding Pellets
Austria gives this project two advantages at the same time: a large livestock base and a mature forest and wood-processing economy. Statistics Austria recorded about 1.79 million cattle on 1 June 2026, including more than 524,000 in Upper Austria, while the average chicken population in 2025 exceeded 21 million. That creates a substantial animal-housing market without assuming that every farm will switch to pellet bedding.
Austria’s forests also provide a strong raw-material context. Official 2025 timber-harvest data show about 19.56 million solid cubic metres of wood harvested nationally, feeding sawmills and other wood-processing industries that generate sawdust, shavings and clean solid-wood residues. Only chemically untreated and traceable material is accepted for bedding production.
| Customer Segment | Why Pellet Bedding Can Fit | Main Product Priority |
|---|---|---|
| Dairy farms | Compact storage and controlled handling | Absorbency, cleanliness and practical bulk/FIBC supply |
| Horse stables | Dust control and convenient retail handling | Clean wood-rich low-fines grade |
| Poultry farms | Dry litter management and easy storage | Clean absorbent bedding with manageable particle form |
| Agricultural distributors | Multiple pack sizes and repeatable batches | Stable bag weight and traceable material origin |
EU organic livestock rules require comfortable, clean and dry resting areas with ample dry bedding such as straw or another suitable natural material. They do not specifically require pellet bedding, so this project markets pellets as one practical bedding option rather than as a mandatory compliance product.
RICHI MACHINERY
Raw Materials: Straw Sawdust and Clean Wood Residues
The raw-material strategy is built around three streams with different preparation needs. Straw contributes absorbency and a softer bedding structure; sawdust is already fine and can bypass primary crushing; clean solid-wood offcuts add fiber and pellet strength after chipping and grinding.
| Raw Material | Annual Planning Volume | Typical Receiving Condition | Preparation Route |
|---|---|---|---|
| Clean sawdust / shavings | Approx. 4,200 T/A | 8–12% moisture | Screen/magnet → buffer; grinding only if needed |
| Clean untreated wood offcuts | Approx. 3,300 T/A | 8–15% moisture | Chipping → hammer milling → buffer |
| Wheat/barley straw | Approx. 2,000 T/A | 10–15% moisture | Bale opening/chopping → hammer milling → buffer |
| Gross annual intake | Approx. 9,500 T/A | Before rejects and moisture variation | Supports about 9,000 T/A finished bedding pellets |
- MDF, particleboard, OSB, painted timber, preservative-treated wood and demolition wood are excluded.
- Furniture-factory material is accepted only when it is verified clean solid wood without coatings or engineered-board contamination.
- Straw is checked for mold, excess soil and storage damage.
- Moisture is checked at receiving and again before pelletizing.
- Metal protection is used to protect high-speed equipment; metal is not expected to represent several percent of incoming biomass.
A main dryer is not installed because incoming moisture is controlled by purchasing specifications. Loads that arrive too wet are segregated, rejected or dried off-site instead of forcing the full 9,000 T/A through a thermal drying stage.
RICHI MACHINERY
The Existing Building Is Used as a Compact Bedding-Pellet Factory
The corrected layout separates land area from covered building area. About 1,400–1,450 m² is enclosed, leaving enough space within the 2,000 m² site for truck access, short-term unloading, fire clearance and external circulation.
| Zone | Approx. Area | Function |
|---|---|---|
| Raw-material storage | 320 m² | Separate straw, sawdust and clean wood residues |
| Preparation area | 350 m² | Bale opening/chipping, magnetic protection and grinding |
| Pelletizing/cooling/screening | 420 m² | MZLH520, cooler, screen and fines return |
| Finished-product storage | 250 m² | Retail bags and FIBC orders |
| Maintenance/electrical | 60 m² | Spare parts and service |
| Office/staff | 50 m² | Administration and welfare |
An 8 m clear height is adequate for elevators, buffer bins and the counterflow cooler when platforms are coordinated with the existing roof structure. Straw and sawdust are stored away from ignition sources, and preparation areas use localized dust extraction and regular housekeeping.
RICHI MACHINERY
Equipment Configuration
The line is designed around one 1.5–2 T/H production train. Large wood needs primary chipping, straw needs bale opening/chopping, and sawdust can bypass both when particle size is already suitable.
| Equipment | Qty | Project Specification | Function |
|---|---|---|---|
| Wood chipper machine | 1 | 45–55 kW class | Reduces clean wood offcuts before fine grinding |
| Bale opener / straw cutter | 1 set | Matched to straw campaign | Opens and shortens straw |
| Wood pellet hammer mill | 1 | 45–55 kW class | Final 2–5 mm grinding where required |
| Magnetic protection | 1 system | Project-specific | Ferrous protection before high-speed equipment |
| Prepared-material buffers / metering | Multiple | Separate wood/straw streams | Controls blend ratio |
| Wood pellet mill | 1 × MZLH520 | 132 kW; 1.5–2 T/H | Main bedding-pellet forming machine |
| Counterflow cooler | 1 | Matched to 2 T/H | Mechanical cooling and stabilization |
| Pellet screener / fines return | 1 | Matched to line | Removes loose fines and broken product |
| Semi-automatic bagging / FIBC route | 1 system | 15–25 kg bags + FIBC | Commercial packing |
| Dust collection | 1 system | Preparation and transfer points | Dust control |
The fixed RICHI equipment package is USD 112,000. This corrected figure includes the properly sized MZLH520, mechanical cooling, screening, controlled metering, dust collection and practical packing rather than relying on floor cooling and shovel filling.
Die compression, feed moisture and roller setting are confirmed with the actual straw/wood formulation during commissioning. Bedding pellets do not use one universal compression ratio.
RICHI MACHINERY
Process Flow
The process is designed around bedding performance rather than fuel-pellet density. Each raw material follows only the preparation steps it actually needs.
Step 1: Receiving and Segregation
Sawdust, straw bales and clean untreated wood are received in separate zones. Wet, moldy or chemically treated material is rejected.
Step 2: Material-Specific Pre-Processing
Wood offcuts pass through the chipper. Straw passes through a bale opener/cutter. Sawdust bypasses both stages.
Step 3: Magnetic Protection and Fine Grinding
Prepared wood and straw pass through magnetic protection before the hammer mill. Final feed is generally controlled in a 2–5 mm range; suitable fine sawdust can bypass intensive grinding.
Step 4: Buffering and Blending
Separate prepared-material buffers keep straw and wood streams controllable. Metering conveyors create the scheduled bedding grade rather than relying on one permanent blend.
Step 5: Pelletizing
The blend enters the wood pellet extruder machine section, configured here as the MZLH520 ring-die pellet mill. Feed moisture, throughput and die/roller settings are adjusted so pellets survive handling but still break down appropriately in use.
Step 6: Mechanical Cooling
Hot pellets enter a counterflow cooler. Floor spreading has been removed from the final design because it would occupy warehouse space, increase labor and complicate cleanliness at 9,000 T/A.
Step 7: Screening and Fines Return
Loose fines and broken pellets are removed before packing. Clean fines can be returned in a controlled amount to the pelleting route.
Step 8: Packing and Dispatch
Horse and retail customers can receive 15–25 kg bags, while dairy and poultry farms can use FIBC or larger farm-delivery formats. Semi-automatic weighing and sewing reduce labor and improve bag-weight consistency.
RICHI MACHINERY
Utilities and Consumption
The original utility section contained conflicting figures. With one 132 kW MZLH520 plus intermittent chipping, hammer milling, aspiration, cooling, screening and conveying, annual electricity is planned at approximately 760,000–820,000 kWh.
| Utility | Completed-Project Planning Value | Engineering Basis |
|---|---|---|
| Electricity | Approx. 790,000 kWh/year | About 88 kWh/t at 9,000 T/A |
| Electrical service | Approx. 400–500 kVA | 132 kW pellet mill plus preparation and auxiliaries |
| Water | Approx. 200–300 m³/year | Domestic use and limited cleaning |
| Process heat/steam | None | No dryer or steam-conditioning system |
| Mobile-equipment fuel | Tracked separately | Forklift/loader use depends on supplier delivery form |
Energy intensity changes with the material mix. A sawdust-rich campaign uses less preparation power because fine material can bypass chipping and sometimes grinding, while straw and wood-offcut campaigns place more load on the preparation section.
RICHI MACHINERY
How RICHI Customized the Line for Bedding Rather Than Fuel
The engineering difference between bedding and fuel pellets begins with end use. Bedding needs cleanliness, low loose fines, storage efficiency, absorbency after wetting and an appropriate break-down rate in the stall rather than maximum combustion density.
- The die and roller setup is selected for the actual straw/wood blend rather than copied from a fuel-pellet recipe.
- Raw-material streams remain separate so premium wood bedding and mixed agricultural grades can be produced with traceability.
- The MZLH520 provides enough installed output for the 9,000 T/A target without multiple undersized pellet mills.
- Mechanical cooling and screening are included because they directly affect loose fines and packing quality.
- Semi-automatic packing controls bag weight and reduces labor.
- No main dryer is installed because incoming moisture is controlled by purchasing specifications.
The plant operates with about 8–10 employees rather than six people covering an unrealistic 24-hour schedule. Training covers raw-material acceptance, die/roller adjustment, screen changes, cooler operation, dust housekeeping, packing calibration and safe lockout.
RICHI MACHINERY
Product Specifications Depend on the Bedding Grade
Bedding quality cannot be reduced to one guaranteed absorbency or PDI value. Straw, softwood sawdust and mixed clean wood have different fiber structure, bulk density and water uptake, so the plant releases products by physical grade and buyer requirement.
| Property | Commercial Target | Control Logic |
|---|---|---|
| Pellet diameter | Mainly 6–8 mm | Suitable for farm and stable bedding handling |
| Length | Typically 10–25 mm | Controlled by cutter and screening |
| Finished moisture | Usually 8–12% | Supports storage stability |
| Loose fines | Kept low through cooling and screening | Important for horse/stable and poultry users |
| Pellet strength | Enough for transport, not unnecessarily hard | Adjusted through die, moisture and blend |
| Absorbency | Verified by internal/buyer test method | Not guaranteed from raw-material name alone |
| Contamination | Clean untreated natural biomass only | No coated/treated engineered wood |
Premium wood-rich bedding is positioned for horse stables and buyers prioritizing cleanliness and low loose dust. Straw/wood blends are aimed at dairy and poultry users where economics and absorbency are more important than uniform pale-wood appearance.
The plant does not claim one universal Austrian statutory bedding-pellet standard. Suitability is documented through material origin, physical testing, cleanliness controls and customer requirements.
RICHI MACHINERY
Market Outlook Is Strongest in Dairy Horse and Poultry Applications
Austria’s livestock figures support a meaningful bedding market without relying on invented producer counts or fixed retail prices. In June 2026 the country had about 1.79 million cattle, with Upper Austria alone holding more than 524,000 head. The national average chicken population in 2025 exceeded 21 million.
Those numbers do not mean every farm will replace straw or sawdust. Pellet bedding competes where storage volume, handling time, dust control, manure-management practice or premium stable conditions justify the processing cost.
| Market Factor | How the Project Responds |
|---|---|
| Large dairy base | FIBC and farm-volume grades |
| Horse/stable market | Wood-rich low-fines retail bedding |
| Poultry production | Clean absorbent litter product |
| Strong wood-processing economy | Contracted clean sawdust and untreated residues |
| Cross-border proximity to Bavaria | Optional regional sales after domestic demand is secured |
EU organic-livestock rules require a comfortable, clean and dry rest area with ample dry bedding such as straw or another suitable natural material. They do not require pellets specifically. The project therefore sells performance and traceable raw-material quality rather than a false compliance claim.
Operating margin, product price and payback are not fixed in the case copy because Austrian electricity, straw, sawdust, packaging and transport costs move. The completed-project investment remains fixed; ongoing economics are evaluated against current local bedding alternatives.
RICHI MACHINERY
Why a Combined Biomass Bedding Plant Can Work in Upper Austria
This project works because its feedstock and customer bases overlap geographically. Upper Austria combines a large cattle population with access to forestry and wood-processing residues, while regional grain production supplies straw. Shorter inbound and outbound logistics matter because bedding is a relatively bulky agricultural product.
The plant also gains flexibility by not locking itself into one permanent formula. When clean sawdust is abundant, the customer can increase wood-rich production. When straw prices are favorable, a controlled mixed grade can serve dairy or poultry users.
Equipment leaves Qingdao for the Port of Koper and then moves by rail/road through Central Europe to Upper Austria. Koper is a practical gateway for Austrian cargo because of its established Central European rail connections; final routing is selected from freight availability and inland cost at shipment time.
For another Biomass Bedding Plant for Combined Biomass Resources in Austria, RICHI Machinery would first confirm untreated raw-material origin, moisture by season, straw bale format, wood particle size, target animal sector, bag format, dust expectations, annual tonnage and electrical capacity. Those inputs determine whether a project needs chipping, bale opening, drying, one or multiple pellet mills and what degree of packing automation is justified.
RICHI scope covers process engineering, equipment manufacture, factory inspection, export packing, control-system preparation, installation guidance, commissioning and operator training. A practical implementation window for an existing-building project of this scale is about 4–6 months when utilities, local modifications and import logistics are prepared in parallel.
● RICHI MACHINERY
RICHI Service

● Consulting
Customer Consultation
We want to have a deep understanding of your industrial process, to know your exact needs of feed, wood, biomass, fertilizer or other pellet processing.
● Design
biomass Pellet Plant Design
Based on your unique situation and industrial process, we will tailor complete pellet plant you need, and inform you of every additional detail that could facilitate operation, minimize total cost.

● Manufacturing
Equipment Manufacturing
The critical components of the of the complete pellet production line equipment are built in our own workshops in Asia. Additional equipment is manufactured by our worldwide network of reliable partners.

● Testing
Quality Inspection & Testing
Before leaving the factory, all equipment will be inspected by the quality inspection department. We can also provide customers with testing services from a single machine to a complete pellet plant system, and provide you with real actual data for “worry-free use.”

● Delivery
Equipment Delivery
In equipment boxing and packaging, we adopt professional packaging and modular solutions to ensure the safe and non-destructive delivery of pellet plant equipment.

● Installation
Installation & Commissioning
Whether you choose your own subcontractor for the erection phase or you want to install everything together with us, a Richi supervisor will be around to make sure everything is mounted in a safe and thorough way.

● Training
Staff Training
We provide comprehensive training for the technicians of each project. We can also continue to provide support for the technicians during latter project operation.

● After-sales
Project Follow-Up
When everything is up and running our Richiers will help you further whenever needed. We are ready to answer your call 24/7.We’ll also visit you regularly to learn about your needs.

Who we are
RICHI Machinery is one of the world’s leading suppliers of technology and services for the animal feed, aqua feed and pet food industries, also the largest pellet production line manufacturer in China.
Since 1995, RICHI’s vision to build a first-class enterprise, to foster first-class employees, and to make first-class contributions to society has never wavered.
In the past three decades, we have expanded our business to a wide range of areas, including animal feed mill equipment, aqua feed equipment, pet feed equipment, biomass pellet equipment, fertilizer equipment, cat litter equipment, municipal solid waste pellets equipment, etc.

1995
RICHI Established

2000+
Serving More Than 2000 Customers

120+
RICHI Employees

140+
Exported To 140 Countries



