

 0086-138 3838 9622
Wood Straw Pellet Production Line in South Africa
Commissioned in early 2025 for an agricultural enterprise in the Free State, this wood straw pellet production line in South Africa turns maize stalks, wheat straw and clean wood residues into industrial fuel. One ring-die press forms the 2 T/H line; bale preparation, feeding and cooling support that single production duty.
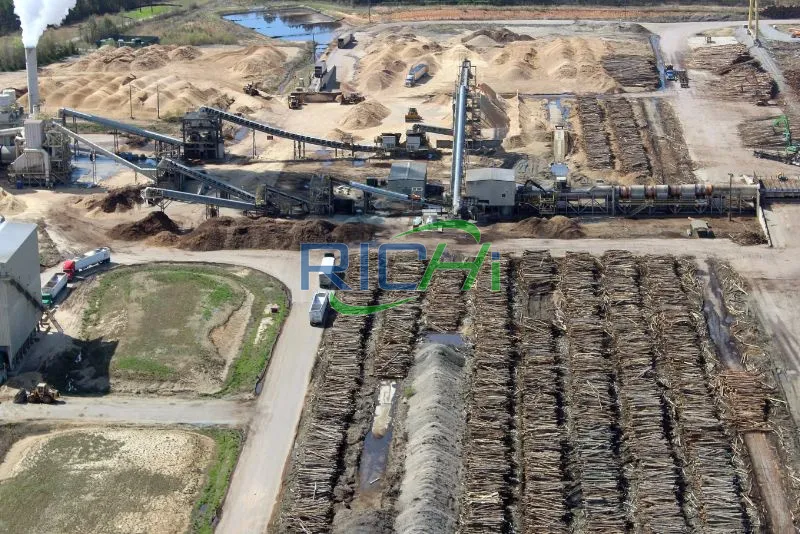
RICHI MACHINERY
Crop residues set the direction of this installation
Maize stalks and wheat straw occupy most of the raw-material programme at this Free State facility. Their low bulk density, long fibres and seasonal availability shaped the machinery selection more than the smaller wood stream. The customer already worked with agricultural residues and timber-related materials. It needed a processing route that converted those supplies into a consistent fuel product, with an operating team able to manage preparation, pressing and dispatch locally.
RICHI supplied the wood straw pellet production line in South Africa around one biomass pellet mill. The nominal output is 2 T/H, and annual design capacity is 9,000 tons over 4,500 productive hours. The plant operates on a 3,000 m² site with 14 employees. Its product is an 8 mm pellet for compatible industrial and commercial biomass combustion equipment, packed in manageable bags for regional distribution.
The commercial straw pellet plant in South Africa combines a cutter, hammer mill, controlled press feeding, mechanical cooling, screening and bagging. Supplier-side air drying keeps the incoming material suitable for a process without a thermal dryer. RICHI also supplies separate bedding-pellet systems for clean straw and wood under the relevant product specifications.
2 T/H
capacity
US$340,000
investment
South Africa
location
Industrial fuel
project type
RICHI MACHINERY
What the Free State customer brought to the project
The agricultural enterprise handles maize and wheat residues from farming activities in the Free State. Collection is seasonal, while pellet buyers need deliveries across the operating year. That creates a storage and scheduling task before the machinery starts: identify the available surplus, keep bales dry and arrange transport so the plant receives prepared material in regular loads.
Wood forms a supplementary stream in this biomass pellet project in South Africa. Clean sawdust and prepared pine or eucalyptus offcuts enter through timber-processing channels linked to the customer’s forestry activities. Preparation takes place through that supply channel before factory delivery. Receiving checks cover moisture, the largest particle and the treatment history of the timber.
Initial consultations took place in late 2023. Equipment procurement was finalised in mid-2024, followed by installation and commissioning in early 2025. RICHI’s role covered the machinery package, process matching, installation guidance and operator training. The customer organised the site, local connections, material collection and finished-fuel distribution.
Four operating requirements shaped the work between the customer and RICHI:
- Prepare long fibres: open the incoming bales, remove bindings and cut stalks before fine grinding, keeping stringy material away from the press feeder.
- Keep one press properly supplied: match preparation and buffer feeding to the production duty, with access for cleaning and routine maintenance.
- Make a defined industrial fuel: control the raw-material blend and finished pellet handling around buyers whose combustion systems accept agricultural biomass.
- Maintain a practical stock cycle: retain seasonal material at collection points and replenish the factory’s covered buffer through planned truck deliveries.
RICHI MACHINERY
One press and a clearly defined supply package
The equipment scope centres on a single production train. Material opening and grinding prepare the blend; the press makes pellets; cooling, screening and packing finish the product. Those shared stages are sized around the required output. Routine service is supported by access space and replaceable wear parts.
- Nominal line duty: 2 T/H of finished industrial biomass pellets on the specified prepared blend.
- Annual design capacity: 9,000 tons, calculated from 4,500 productive hours at the nominal hourly duty.
- Press arrangement: one MZLH520 biomass pellet mill, with no additional standby press in the machinery package.
- Site footprint: 3,000 m² allocated to processing, covered stock, packing, service access and vehicle movement.
- Operating organisation: 14 employees serving two shifts, with maintenance and management support shared across the working day.
The package price and use of the available site are set out together below. Floor allocations include working access around the equipment:
| Item | Project specification |
|---|---|
| Complete equipment package | US$120,000 |
| Production bay | 500 m² |
| Covered raw-material buffer | 600 m² |
| Finished-pellet store | 200 m² |
| Maintenance and staff facilities | 50 m² |
| Vehicle access and open circulation | 1,650 m² |
| Total site footprint | 3,000 m² |
For buyers comparing biomass pellet plant cost in South Africa, the package boundary matters. The equipment price covers the prepared-feed route through bagging, including drives and controls. The fixed project investment also covers site preparation, local electrical work, installation and related implementation. Raw-material purchases and operating inventory remain working-capital requirements. No thermal drying system is included in this process.
RICHI MACHINERY
Bales determine the storage and preparation plan
A crop-heavy collection programme
Half of annual collection is maize stalk material, wheat straw contributes three tenths and wood residues supply the balance. For maize stalk pellet production in South Africa, the stalk condition at pickup is a practical purchasing specification: bale moisture, soil contamination, binding materials and stalk length all affect unloading and preparation. The customer maintains separate material streams until each is ready for controlled blending.
Annual collection and seasonal stock positions
Annual quantities are recorded at collection before final air drying and intake cleaning. The stock limits below cover the collection and supply network, with seasonal reserves held upstream of the factory’s short-term buffer:
| Material | Collection channel | Annual collection (t) | Seasonal storage location | Supply-network stock limit (t) |
|---|---|---|---|---|
| Maize stalks | Free State crop farms | 5,000 | Covered bales at farm collection points | 500 |
| Wheat straw | Grain-farming supply network | 3,000 | Dry bale stores at collection points | 300 |
| Wood residues | Clean pine and eucalyptus processing residues | 2,000 | Covered stock at wood-processing suppliers | 200 |
The collection programme totals 10,000 tons annually. Its material balance uses 17% average collection moisture and 10% finished-pellet moisture: 9,000 tons become packaged product, 250 tons are non-reusable sorting rejects and 750 tons are water removed across supplier air drying and plant processing. The reject stream is balanced at 20% moisture. Reusable process fines remain inside the production circuit. Material arrives for milling below 15% moisture.
Getting prepared material to the press
- The crop-residue collection agreements support scheduled farm deliveries. Buyers considering a wheat straw pellet plant in South Africa should distinguish seasonal collection capacity from the quantity that fits inside the processing site’s bale store.
- Wood residue pellet production in South Africa also requires a size specification. Sawdust enters after inspection; offcuts are pre-chipped through the timber supply channel. Painted wood, preservative-treated timber and glued panels are excluded from this fuel blend.
- Air drying takes place before material enters long-term covered storage and the milling route. At the factory, moisture checks identify unsuitable loads before unloading into the production stock. Storage prevents rain rewetting; placing wet bales under a roof is not a substitute for drying.
RICHI MACHINERY
Equipment selected around the two-tonne duty
The wood straw pellet production line in South Africa uses material-specific preparation ahead of one MZLH520. The machinery table shows the operating role of each assembly. Auxiliary capacities refer to light biomass duty, since a grain-grinding capacity figure alone does not describe how a hammer mill handles straw.
| No. | Equipment | Specification | Quantity | Duty in this installation |
|---|---|---|---|---|
| 1 | Bale-opening and straw-cutting assembly | 3 T/H preparation duty | 1 set | Removes bindings and reduces long stalks before milling |
| 2 | Biomass hammer mill | SFSP series with 3–5 mm screens | 1 | 3 T/H preparation duty with matched aspiration |
| 3 | Ring-die Wood Pellet mill | MZLH520; 132 kW | 1 | Biomass range 1.5–2 T/H; nominal project duty 2 T/H |
| 4 | Control and motor-protection cabinet | Matched drives and feeder controls | 1 set | Coordinates starting, stopping and equipment interlocks |
| 5 | Counterflow cooling and screening assembly | At least 2 T/H combined handling duty | 1 set | Cools pellets and returns separated clean fines |
| 6 | Milling-air and fines-recovery assembly | Cyclone, filtration and matched fan | 1 set | Supports pneumatic separation and clean material recovery |
| 7 | Weighing and bag-closing station | 20 kg and 25 kg bags | 1 set | 100 bags/hour at 20 kg or 80 bags/hour at 25 kg |
This 2 t/h biomass pellet line in South Africa makes 8 mm industrial fuel pellets. With a single press, daily attention goes to an even feed, usable die area and roller adjustment. Spare dies, roller components, screens and bearings support the service plan. Cooler discharge and bagging remain accessible during those checks.
RICHI MACHINERY
Power provision for a mechanical processing route
Electricity, water and cooling air
- Freshwater provision is 200 m³/year for staff facilities and routine sanitation. Pellet cooling uses ambient air, so cooling performance is controlled through airflow, bed depth and discharge rate.
- The annual electricity design allowance is 900,000 kWh, equivalent to 100 kWh per ton of the annual design output. It covers cutting, grinding, pressing, conveying, cooling and packing; the pellet-mill main motor is rated at 132 kW.
- No thermal dryer or steam boiler is included. The process relies on suitable incoming moisture and heat generated during mechanical preparation and pressing. The electrical interface is matched to the local three-phase supply and the actual simultaneous motor duty.
Make the daily operating inputs visible
- Operators check incoming moisture, prepared material level and press motor load together. Those readings distinguish an empty feeder, difficult material and an excessive feed setting before output is interrupted.
- Control settings remain available to the local operating team. Screen changes, die inspections and bearing lubrication are scheduled around the daily production window, with critical replacement parts identified during training.
RICHI MACHINERY
Keeping light straw moving through the line
Open the bale before asking the feeder to meter it
- Long fibres bridge across narrow openings and wind around rotating components. The opening and cutting stage breaks up the bale before the material reaches fine grinding, with bindings and foreign pieces removed at receiving.
- Material flow through the prepared-feed buffer stays visible to the operator. An uneven bin discharge is addressed at the feed point; increasing the press feeder setting cannot make an upstream blockage disappear.
Use motor load to control the feed
- The feeder supplies the MZLH520 at a controlled rate. Material composition, moisture and die condition are checked when load changes, preventing the press from becoming the only place where an upstream problem is noticed.
- Grinding is managed by the coarse fraction and fibre condition, with 3–5 mm screen selection. Excessive grinding creates unnecessary recirculation and handling, while long uncut fibres disturb flow and compaction.
- Prepared material provides a short process buffer between milling and pressing. Its purpose is to smooth brief interruptions, with a discharge arrangement suited to low-density biomass.
Keep wear parts accessible
- Die and roller access, screen replacement and motor servicing have clear working space. The single-press arrangement makes planned care and a usable spares list central to production availability.
- Clean fines from final screening return through a controlled route. Contaminated material stays outside that circuit, preventing a recovery conveyor from bringing foreign matter back to the press.
RICHI matched the preparation route and operating interfaces to the customer’s crop-heavy blend. The local team has separate duties for bale opening, milling, pressing and final handling. Clear access, visible material levels and coordinated controls make those equipment interfaces part of the daily operating routine.
RICHI MACHINERY
Six operations from opened bale to packed fuel
The material route through the factory
- Bale opening and cutting: dry maize stalks and wheat straw are released from their bindings and reduced to manageable fibres. Wood arrives as sawdust or prepared chips. Receiving inspection keeps stones, metal and unsuitable timber outside the milling stream. The cutter feeds steadily instead of pushing whole bundles into the next machine.
- Fine grinding: the SFSP hammer mill processes cut crop residues and the wood fraction requiring further reduction. Suitable sawdust bypasses unnecessary size reduction. Matched aspiration clears material from the grinding chamber, and screening controls the coarse tail. The prepared blend maintains the project’s maize, wheat-straw and wood proportions before pressing.
- Pellet pressing: metered material enters the straw pellet machine and is compressed through the ring die into 8 mm pellets. Roller setting, die condition and feeding determine the press duty alongside the material itself. The line uses one MZLH520, with its control interface coordinated with the upstream feed and downstream handling.
- Mechanical cooling: pellets move into the counterflow cooler while airflow removes heat and assists moisture release. The discharge maintains a working bed and feeds the next stage at a controlled rate. Pellets leave cooling before entering sealed bags, protecting the packed product from retained heat and condensation.
- Final screening: undersize fines are separated from the cooled pellets and returned to processing. Screening checks the fraction that reaches the bagging station and avoids sending loose fines out with the fuel. Long pieces are controlled at the press discharge cutter, with screen selection matched to the finished product.
- Weighing and bagging: the station fills 20 kg or 25 kg bags, followed by closing and transfer into finished stock. The required bagging rate is modest enough for one matched station. Manual bag handling, pallet movement and dispatch access are included in the layout and staff allocation.
Two preparation entries join one finishing route
Dry crop bales → opening and cutting → fine grinding; clean wood → inspection and size reduction where required → controlled blending → one ring-die press → counterflow cooling → screening and fines return → weighing → bag closing → finished stock.
RICHI MACHINERY
A fourteen-person team over two shifts
- The workforce totals 14: six production and handling staff on each shift, plus two shared maintenance and management positions. Operating duties cover preparation, press control, packing, stock movement and routine product checks.
- The calendar comprises 300 working days and two 8-hour shifts, giving 4,800 scheduled hours. Annual design output uses 4,500 productive hours at nominal duty, leaving 300 hours for planned interruptions across the year.
- Shift handovers cover material identity, moisture checks, prepared-stock level, equipment condition and outstanding maintenance. The next team takes over the operating state of the line as well as the production count.
RICHI Machinery provided operator training during installation. Instruction covered equipment starting and stopping, feed adjustment, cooling discharge, bagging, lubrication and access for routine service. The training connected machine controls with visible material behaviour so the local team could manage the complete route.
RICHI MACHINERY
What the installation added to the customer’s operation
A product with a defined release check
- Finished product is identified as an 8 mm industrial biomass fuel pellet. Product diameter, moisture, strength and fines are checked together before dispatch.
- The raw-material programme identifies maize stalks, wheat straw and clean wood separately. That gives operators a way to trace a change in pressing behaviour back to the incoming material.
- The bagging station supplies consistent handling units, while finished stock is organised for planned regional deliveries. Pack size, batch identification and storage condition form part of release.
- Material recovered during screening returns through the process route. Rejects and unsuitable incoming material stay separate from usable fines.
A manageable workflow for the local team
- Operators work with one press and a connected preparation route, keeping attention on material supply and product finishing at the required scale.
- Maintenance access and the wear-parts list support local servicing. A press stoppage is addressed through the service plan and identified spares.
- The site separates bale reception from packed-pellet dispatch, giving truck and forklift movements a defined place outside the main processing bay.
A stock plan that reflects harvest timing
- Seasonal reserves remain at farm and timber-processing collection points, while the factory receives scheduled replenishment. The processing site’s covered buffer carries working stock between those deliveries.
- Crop availability is checked after other committed uses, including feed, bedding and necessary field retention. Annual procurement planning concerns the collectable surplus and its delivered condition.
RICHI MACHINERY
Fuel handling determines the customer fit
Industrial biomass pellets in South Africa serve users whose boilers or furnaces accept the actual fuel characteristics. With crop residues making up most of this blend, ash behaviour and ash-removal capacity matter alongside pellet size and moisture. The project is directed toward suitable commercial and industrial heating duties, with the fuel specification checked against the receiving equipment.
Three buyer-side conditions shape the product and delivery discussion:
- Combustion equipment must suit agricultural biomass and its ash characteristics, with the fuel feed and grate arrangement matched to the product.
- Receiving space and delivery frequency must suit bagged fuel. Warehouse conditions and handling methods affect how many days of stock the buyer can hold.
- Purchasing decisions need product measurements and delivered-fuel terms. A bag label or pellet diameter alone is insufficient to define a boiler fuel.
Regional supply is the practical commercial focus of this installation. The customer has a defined product, a working collection network and a packing route suited to manageable deliveries. Market discussion centres on compatible fuel users and transport, with capacity tied to the available material programme.
RICHI MACHINERY
Specify your line around the material arriving at the gate
This Free State installation starts with the crop-residue supply and carries that decision through bale handling, fine grinding, a single press and cooled-product packing. Its layout reserves substantial space for stock and vehicle movement because those activities support a small continuous processing line throughout the working day.
When choosing a biomass pellet equipment supplier for South Africa, give the manufacturer separate information for stalks, straw, sawdust and wood pieces. Their moisture, shape and bulk density determine preparation duty, feed arrangements and storage provision. A single list headed biomass is insufficient for selecting those stages.
For a wood straw pellet plant in South Africa, send RICHI the annual quantity of each material, collection moisture, moisture at the factory, bale dimensions, largest wood piece and target pellet specification. Include the available building, electrical supply, working calendar and buyer’s combustion application. Those inputs define the machinery scope and the work required at the site.
We configure the biomass pellet production line around those operating inputs, with preparation and downstream equipment matched to the selected press. The quotation identifies supply responsibilities, installation interfaces, operating support and the equipment needed for the agreed material route.
● RICHI MACHINERY
RICHI Service

● Consulting
Customer Consultation
We want to have a deep understanding of your industrial process, to know your exact needs of feed, wood, biomass, fertilizer or other pellet processing.

● Design
biomass Pellet Plant Design
Based on your unique situation and industrial process, we will tailor complete pellet plant you need, and inform you of every additional detail that could facilitate operation, minimize total cost.

● Manufacturing
Equipment Manufacturing
The critical components of the of the complete pellet production line equipment are built in our own workshops in Asia. Additional equipment is manufactured by our worldwide network of reliable partners.

● Testing
Quality Inspection & Testing
Before leaving the factory, all equipment will be inspected by the quality inspection department. We can also provide customers with testing services from a single machine to a complete pellet plant system, and provide you with real actual data for “worry-free use.”

● Delivery
Equipment Delivery
In equipment boxing and packaging, we adopt professional packaging and modular solutions to ensure the safe and non-destructive delivery of pellet plant equipment.

● Installation
Installation & Commissioning
Whether you choose your own subcontractor for the erection phase or you want to install everything together with us, a Richi supervisor will be around to make sure everything is mounted in a safe and thorough way.

● Training
Staff Training
We provide comprehensive training for the technicians of each project. We can also continue to provide support for the technicians during latter project operation.

● After-sales
Project Follow-Up
When everything is up and running our Richiers will help you further whenever needed. We are ready to answer your call 24/7.We’ll also visit you regularly to learn about your needs.

Who we are
RICHI Machinery is one of the world’s leading suppliers of technology and services for the animal feed, aqua feed and pet food industries, also the largest pellet production line manufacturer in China.
Since 1995, RICHI’s vision to build a first-class enterprise, to foster first-class employees, and to make first-class contributions to society has never wavered.
In the past three decades, we have expanded our business to a wide range of areas, including animal feed mill equipment, aqua feed equipment, pet feed equipment, biomass pellet equipment, fertilizer equipment, cat litter equipment, municipal solid waste pellets equipment, etc.

1995
RICHI Established

2000+
Serving More Than 2000 Customers

120+
RICHI Employees

140+
Exported To 140 Countries



