

 0086-138 3838 9622
Straw pellet production line in Germany
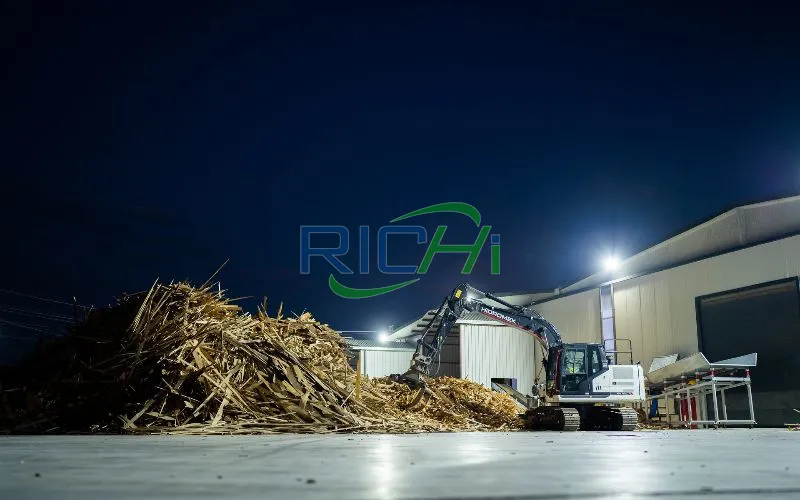
This straw pellet production line in Germany connects two different receiving streams: relatively dry farm straw and wetter untreated wood residues. RICHI configured separate preparation routes ahead of one MZLH768 press. The completed installation serves an agricultural and timber-processing business in Bavaria, with an annual design programme of 18,000 tons of industrial fuel pellets.
RICHI MACHINERY
One production train for two material conditions
The installation occupies approximately 6,667 m² in a Bavarian industrial location. The allocated building area is 5,450 m², including processing, ingredient storage, finished stock and support rooms. Production follows two eight-hour shifts on 300 working days annually. A nominal finished-pellet rate of 4 T/H supports an 18,000-ton annual design programme, leaving scheduled time for servicing, material changes and operating interruptions. The programme describes design production rather than audited annual deliveries.
The property allocation connects four working areas. For clean straw intended for animal bedding, RICHI supplies a separate product route with its own material and quality requirements; the mixed fuel recipe here serves industrial heating.
- Production workshop: 2,800 m² for material reduction, the wet-wood drying route, pressing, cooling, screening and packing, with maintenance access around the machinery.
- Warehouse allocation: 2,000 m² shared between identified incoming ingredients and finished-product stock. Their operating boundaries keep wet wood handling away from dry straw and packed fuel.
- Office and support building: 580 m² for administration, quality checks, staff facilities and production coordination. These rooms serve the wider operation rather than adding processing capacity.
- Auxiliary rooms: 70 m² for electrical and site support functions. Buildings total 5,450 m², leaving approximately 1,217 m² for external access and circulation.
4 T/H
capacity
One MZLH768
press configuration
Germany
location
Industrial fuel
project type
RICHI organised the equipment for this biomass pellet project around the receiving condition of each material:
- One biomass-fired hot-air furnace supplies the wood-drying branch. Its separately recorded fuel supply is additional to the ingredients allocated to pellet production.
- A straw-opening and cutting section prepares long fibres; an SFSP-series hammer-milling section controls the coarse fraction entering the press feed system.
- A rotary drum dryer handles the wetter wood stream. Accepted dry straw uses a separate route so it does not receive unnecessary thermal treatment.
- One ring-die straw pellet machine, model MZLH768, uses a 315 kW main motor for the selected 4 T/H nominal production duty.
- A counterflow pellet cooler and product screen finish the press discharge before weighing, packing or transfer to finished stock.
- Belt and screw conveyors connect the preparation branches, controlled feed buffer and finishing section according to material behaviour.
- Process aspiration collects recoverable clean fines at the milling and transfer points, with a defined return path into production.
- The dryer heat system includes matched hot-air delivery, temperature control and downstream particle separation appropriate to its selected fuel and duty.
The straw pellet plant has a 30-person staffing allocation across two operating shifts and shared support functions. The receiving team identifies materials before assigning them to the straw or wood route. Operators coordinate drying, preparation and press supply, while packing and dispatch work follow the finished-stock schedule. The arrangement requires communication between the material yard and the process operators when a supplier lot or recipe changes.
This single-press biomass pellet system in Germany has a nominal calendar ceiling of 19,200 tons: 4 T/H multiplied by 4,800 scheduled hours. The annual target requires 4,500 productive hours at that rate, leaving 300 hours within the calendar. Maintaining that allowance depends on prepared-stock availability and routine maintenance; it is not a guarantee of uninterrupted operation. No parallel small presses are needed for the stated production programme.
RICHI MACHINERY
A customer with both farm and timber supply channels
Client operations and the production brief
The customer is a mid-sized agro-industrial business in Bavaria with grain cultivation, timber-processing and straw-collection activities. Its operations also extend into Austria. The pellet project brings those supply capabilities into one manufacturing route, but their materials cannot share every preparation step. Straw arrives as a fibrous agricultural residue; wood may arrive as sawdust or chips with substantially more water. RICHI treated this difference as a layout and heat-duty question from the beginning.
The business needed fuel pellets in a controlled handling form for its own compatible heating duties and selected commercial outlets. It also needed to retain flexibility when the relative availability of straw and wood changed. That flexibility rests on controlled ingredient preparation and a defined recipe. An unrestricted mixture of incoming residues would make dryer loading, mill feeding and product checks difficult to repeat.
Fuel composition determined the customer route
For this agricultural biomass pellet plant in Germany, the intended product is a declared straw-and-wood industrial fuel. Straw changes ash composition and combustion behaviour relative to clean wood alone. The receiving installation therefore needs approval for the actual agricultural biomass blend. The project does not assume that pellets become interchangeable with household wood fuel merely because they have the same diameter or a smooth surface.
The commercial brief concentrates on three defined receiving applications:
- Compatible internal heating equipment, where the customer can coordinate fuel storage, feeding settings and the heating schedule directly.
- Qualified local heating operators, following review of the declared recipe, representative product and relevant fuel-test results.
- Industrial thermal users, with material-handling and combustion equipment suited to the pellet composition and delivery format.
Buyer qualification starts before a routine dispatch programme is agreed. A representative lot provides material for checks of moisture, fines, ash, heating value and handling behaviour. The relevant results accompany the fuel description. When the recipe changes substantially, the receiving operator reviews the change rather than relying on a standing batch designation. The project serves identified fuel duties without making a national demand forecast or assuming a guaranteed sales volume.
The operating objectives
Four decisions shaped this straw pellet production line in Germany:
- Separate preparation duties: Dry fibrous straw and wet wood take suitable routes before joining the controlled blend feeding the press.
- Match the annual programme: One machine supplies the selected duty within the two-shift calendar, with downstream equipment sized for its discharge.
- Define the input boundary: The annual process plan allocates 24,000 tons of received ingredients, with furnace fuel counted separately.
- Keep batches traceable: Ingredient identity, preparation condition and product checks stay connected through production, packing and dispatch records.
The biomass pellet plant combines the customer’s supply organisation with RICHI’s machinery configuration. Farm collection, supplier qualification, local works and finished-fuel distribution remain customer operating responsibilities. RICHI’s role connects material preparation, drying duty, the selected press, cooling and packing. Reviewing those interfaces gives the customer a clearer scope than choosing a pellet mill from hourly output alone.
RICHI MACHINERY
Incoming moisture decides the preparation route
Straw and untreated wood supplies
The straw and wood pellet plant in Germany accepts the following identified ingredients:
- Wheat straw, barley straw and maize stalks are collected from farms within a 50 km radius. Collection condition, bindings and soil contamination are checked before release to working stock.
- Clean sawdust and wood chips come from selected sawmills and untreated-timber processors. Painted wood, preservative-treated material and unknown demolition timber are excluded.
- Wood fines and limited bark-bearing material require a defined ingredient specification. Changes in bark content trigger a review of the fuel recipe and relevant product properties.
The annual material-balance basis is 24,000 tons of received ingredients: 12,000 tons of straw at 12% moisture and 12,000 tons of untreated wood residues at 48% moisture. Their weighted average moisture is 30%. These are intake-planning conditions, not a requirement that every load has the same water content. Actual receiving weights and moisture checks determine the preparation setting for each lot.
From received weight to usable press feed
- Moisture routing: Accepted straw at up to 20% moisture bypasses the thermal dryer; the wetter wood stream is dried separately. After blending, press feed is controlled within 10–14%, using 12% for the balance calculation.
- Material balance: The annual outputs comprise 18,000 tons of finished pellets containing 10% moisture, a 750-ton sorting stream containing 20% moisture, and water evaporation of 5,250 tons. Incoming dry matter totals 16,800 tons; product and sorting material contain 16,200 and 600 tons respectively.
- Handling density: Loose straw, sawdust and chips occupy different volumes per ton. Storage planning uses the actual ingredient form and stacking arrangement; finished-pellet bulk density is measured separately and is not inferred from individual-pellet density.
Electrical and thermal planning are separate
- Site water: The annual allowance is 720 m³ for staff and site services. The product route has no continuous water-washing stage and no steam-conditioning demand in this configuration.
- Electricity: The annual design allocation is 2,700,000 kWh, equivalent to 150 kWh per ton of planned product. It covers pressing, size reduction, drying fans, cooling, conveying, aspiration and site auxiliaries.
- Dryer heat: A separate allowance of 1,500 tons of dry furnace fuel at 15 MJ/kg provides 22.5 TJ of fuel energy annually. At a 70% useful-heat planning efficiency, approximately 15.75 TJ reaches the drying duty. Furnace fuel is additional to the 24,000-ton ingredient input.
RICHI MACHINERY
The process follows two branches into one press
In this straw pellet processing plant in Germany, receiving checks decide the next equipment step. The press is supplied from a controlled buffer after fibre reduction, wood drying where needed and recipe preparation. Finished pellets then pass through cooling, screening and measured packing. The operating sequence keeps drying control distinct from press loading, allowing each operator to identify the cause of a feed or product change.
- Receiving and allocation
Loads are weighed, identified and checked before entering ingredient stock. Straw, sawdust and chips retain separate positions so the team can select a repeatable batch. Wet wood does not enter the dry-straw store. The receiving record follows the load into preparation and distinguishes accepted ingredient weight from rejected foreign material. - Fibre and particle preparation
Straw is opened and cut before hammer milling. Oversized wood chips receive primary reduction suited to their dimensions, while suitable sawdust can bypass that step. The mill controls the coarse fraction entering the press feed system. Operators check remaining long fibres and coarse pieces as well as screen condition; a nominal screen opening alone does not describe every particle leaving the mill. - Selective wood drying
The rotary dryer handles wood that arrives above the accepted moisture condition. Its feed rate follows incoming water content and available useful heat. Dry straw bypasses this branch and joins the blend downstream. On the annual balance, about 4,841 tons of water leave before press feeding, followed by approximately 409 tons during pressing and cooling. The two stages together account for the 5,250-ton evaporation allowance. - Recipe preparation and buffering
The prepared ingredients are proportioned into the approved blend and checked for moisture before pressing. The feed buffer absorbs short preparation interruptions without becoming a long-term storage bin. Its discharge must move the fibrous blend consistently. There is no routine addition of steam or hot water in this process definition; the ingredient preparation establishes the required condition. - Ring-die pressing
Metered blend enters the wood pellet mill selected for the project: one MZLH768 with a 315 kW main motor. The rated biomass range is 3–4 T/H, with 4 T/H used as this programme’s nominal duty. Die selection, roller adjustment and feed condition govern the achievable rate. The product diameter is selected within 6–8 mm to match the receiving customer’s agreed specification. - Cooling and fines separation
The counterflow cooler accepts hot press discharge and removes heat before finished-stock transfer. Operators check product temperature, airflow and discharge behaviour as part of routine running. Screening separates loose fines for a controlled return to the process. Reusable clean fines remain inside the production circuit and are not counted again as received material or saleable output. - Packing and dispatch stock
Cooled pellets pass to weighing and filling for the agreed industrial delivery format. Packing records identify the recipe and finished lot. Filled bags are stored away from incoming wet ingredients, and loading follows the order schedule. Bag size, unloading equipment and the buyer’s available storage are agreed together; a household-sized bag does not change the intended industrial fuel application.
RICHI MACHINERY
The equipment scope follows the limiting duties
The MZLH768 straw pellet line in Germany uses one production train. Upstream equipment is checked against ingredient condition and the required prepared-feed rate; downstream equipment is checked against press discharge. The key assemblies have different duties:
- SFSP-series hammer milling controls prepared fibre size. Straw cutting ahead of milling reduces the burden of long fibres; wood preparation follows incoming chip dimensions. Final mill selection follows material trials and the required feed rate.
- Rotary drying with a biomass furnace serves the wet-wood branch. The annual basis corresponds to about 1.08 T/H of water evaporation over 4,500 productive hours; selection allows for the intended peak wet-load condition and drying trials.
- One MZLH768 pellet mill provides the 3–4 T/H biomass duty with a 315 kW main motor. This power is the press main-motor rating; it excludes its auxiliaries and every other process assembly.
- Counterflow cooling and screening match the nominal 4 T/H pellet discharge. They include controlled fines return so the packing section receives cooled product with loose material removed.
- Weighing and bagging follow the selected delivery format. Capacity is checked against net packed output and the time needed to change bags, identify lots and move filled units.
- Process aspiration serves milling and transfer points, keeping clean recovered material on an identified return route. Inspection access is provided for filters, ducts and discharge devices.
- Control and interlocks coordinate conveyor availability, dryer conditions, feed supply and finishing. Operators retain access to temperature, motor-load and stop indications relevant to their assigned section.
RICHI MACHINERY
Daily checks at the equipment interfaces
Receiving to preparation
- Before feeding, operators check the ingredient record, moisture result and condition of the selected stock. A damp bale or changed wood delivery is assessed before it can alter the prepared-feed supply.
- Preparation checks include cutting performance, screen wear, magnetic separation and transfer clearance. Persistent bridging is addressed at the material or equipment setting rather than by forcing a higher feed command.
Drying to the blend buffer
- Dryer control follows inlet moisture, discharge condition, temperature and airflow. A wetter lot requires an adjusted feed setting within the available heat and evaporation duty.
- Blend release follows the selected ingredient proportions and press-feed moisture check. Prepared material is kept separate from unprocessed wet stock until it meets the feed condition.
Press to finishing
- Motor-load trends, feeding continuity and pellet formation are observed together. When loose fines increase, the operator checks preparation and press settings before simply increasing the recirculation rate.
Packing to dispatch
- Each released lot has an identity linked to its recipe and checks. Product remains out of dispatch stock until cooling and the required quality checks are complete.
- Dispatch records connect the delivered quantity, lot reference and agreed delivery format. The next shift receives any outstanding product or equipment observations in its handover.
RICHI MACHINERY
The buildings must support working stock and access
- Ingredient storage occupies designated positions within the warehouse allocation. Straw deliveries are scheduled against covered capacity instead of assuming the site can hold the entire annual harvest.
- The process workshop contains both preparation branches and their common press route. Its floor area includes service access, working clearances and material buffers as well as machine footprints.
- Finished stock remains near the dispatch route. Lot rotation and packing schedules limit unnecessary handling and keep the warehouse from becoming a buffer for unsuitable warm product.
- Office and support rooms house the shared administrative, quality and staff functions, leaving process operating positions close to the equipment they serve.
- External circulation uses the approximately 1,217 m² outside the building allocation. Delivery appointments, vehicle dimensions and the actual site plan govern access; an area total alone does not prove truck-turning clearance.
For this biomass fuel pellet factory in Germany, storage capacity is a logistics calculation rather than a conversion from floor area alone. Usable aisles, bale size, chip-bin arrangement, stacking limits and product format all affect inventory. The receiving schedule therefore supports a working-stock system. Dimensions and vehicle movements are checked on the site layout before confirming the final unloading and loading arrangements.
RICHI MACHINERY
Staffing the straw fuel pellet production project in Germany
- Working calendar: Two eight-hour shifts over 300 days provide 4,800 scheduled hours. At 4 T/H, 18,000 tons require 4,500 productive hours, leaving 300 scheduled hours for interruptions and maintenance.
- Staff allocation: Thirty people include 20 production and logistics workers across the shifts, five maintenance personnel, three administrative staff and two quality and stock-control staff. Shared functions do not imply 30 people present on each shift.
- Quality records: Incoming moisture and lot identity accompany batch recipes. Finished-product checks cover agreed dimensions, moisture, fines, durability and fuel properties relevant to the receiving installation.
- Maintenance planning: Daily inspections cover lubrication, screens, conveying and wear components. Planned interventions are included in the operating allowance, with major work coordinated against the annual production calendar.
RICHI MACHINERY
Dispatch planning follows qualified fuel demand
The industrial straw pellet project in Germany connects production with buyers through four practical arrangements:
- An agreed fuel description identifies the agricultural and wood ingredients. Buyers review the relevant product results against their equipment requirements before accepting routine deliveries.
- A manageable order pattern balances production batches, finished-store space and the customer’s available inventory. Delivery intervals remain part of the supply discussion.
- A local collection plan coordinates the straw harvest and wood deliveries within the working-stock system. Moisture checks help keep purchasing weight separate from useful dry matter.
- A defined response to changes covers supplier substitutions, recipe adjustments and product observations. Significant changes are reviewed before another routine shipment is released.
The annual dispatch programme targets 18,000 tons of finished fuel, equivalent to 60 tons per working day on average. That figure helps coordinate packing and loading, but does not establish the number of trucks required: vehicle payload, bag format and delivery appointments determine actual movements. The 4 T/H straw pellet plant in Germany therefore uses the production calendar together with its storage and transport plan.
RICHI MACHINERY
A single press within a complete preparation system
RICHI configured this straw pellet production line in Germany around a specific relationship between raw materials and annual output. Dry straw avoids unnecessary thermal treatment, wetter untreated wood receives a dedicated drying route, and the prepared blend feeds one appropriately sized press. Cooling, screening and packing complete the manufacturing route. The customer receives a connected operating scope with four clear priorities:
- Identified ingredient streams with separate moisture-dependent preparation routes.
- One MZLH768 press matched to the annual programme and two-shift calendar.
- Separate accounting for ingredient weight, furnace fuel, electricity and finished output.
- Recorded production lots supplied to compatible industrial fuel users.
● RICHI MACHINERY
RICHI Service

● Consulting
Customer Consultation
We want to have a deep understanding of your industrial process, to know your exact needs of feed, wood, biomass, fertilizer or other pellet processing.

● Design
biomass Pellet Plant Design
Based on your unique situation and industrial process, we will tailor complete pellet plant you need, and inform you of every additional detail that could facilitate operation, minimize total cost.

● Manufacturing
Equipment Manufacturing
The critical components of the of the complete pellet production line equipment are built in our own workshops in Asia. Additional equipment is manufactured by our worldwide network of reliable partners.

● Testing
Quality Inspection & Testing
Before leaving the factory, all equipment will be inspected by the quality inspection department. We can also provide customers with testing services from a single machine to a complete pellet plant system, and provide you with real actual data for “worry-free use.”

● Delivery
Equipment Delivery
In equipment boxing and packaging, we adopt professional packaging and modular solutions to ensure the safe and non-destructive delivery of pellet plant equipment.

● Installation
Installation & Commissioning
Whether you choose your own subcontractor for the erection phase or you want to install everything together with us, a Richi supervisor will be around to make sure everything is mounted in a safe and thorough way.

● Training
Staff Training
We provide comprehensive training for the technicians of each project. We can also continue to provide support for the technicians during latter project operation.

● After-sales
Project Follow-Up
When everything is up and running our Richiers will help you further whenever needed. We are ready to answer your call 24/7.We’ll also visit you regularly to learn about your needs.

Who we are
RICHI Machinery is one of the world’s leading suppliers of technology and services for the animal feed, aqua feed and pet food industries, also the largest pellet production line manufacturer in China.
Since 1995, RICHI’s vision to build a first-class enterprise, to foster first-class employees, and to make first-class contributions to society has never wavered.
In the past three decades, we have expanded our business to a wide range of areas, including animal feed mill equipment, aqua feed equipment, pet feed equipment, biomass pellet equipment, fertilizer equipment, cat litter equipment, municipal solid waste pellets equipment, etc.

1995
RICHI Established

2000+
Serving More Than 2000 Customers

120+
RICHI Employees

140+
Exported To 140 Countries



