

 0086-138 3838 9622
Crop Residue Pellet Manufacturing System for Energy in Slovenia
RICHI MACHINERY
Project Overview
A biomass entrepreneur in the Savinja Statistical Region developed this Crop Residue Pellet Manufacturing System for Energy in Slovenia to produce industrial solid fuel from dry wood-processing residues and selected agricultural by-products. The project serves district-heating operators, industrial boilers and fuel traders rather than treating every pellet as a residential-stove product.
The design target is 20,000 T/A. At 300 operating days and about 8 effective hours per day, the line must average roughly 8.33 T/H. Three MZLH678 biomass pellet mills, each rated at 2.5–3 T/H with a 200 kW main motor, provide 7.5–9 T/H installed pelletizing capacity. That is a realistic match for the annual target when the plant is operated near the upper part of its range; in years with about 250 operating days, output of roughly 15,000–16,000 tons is consistent with the same equipment.
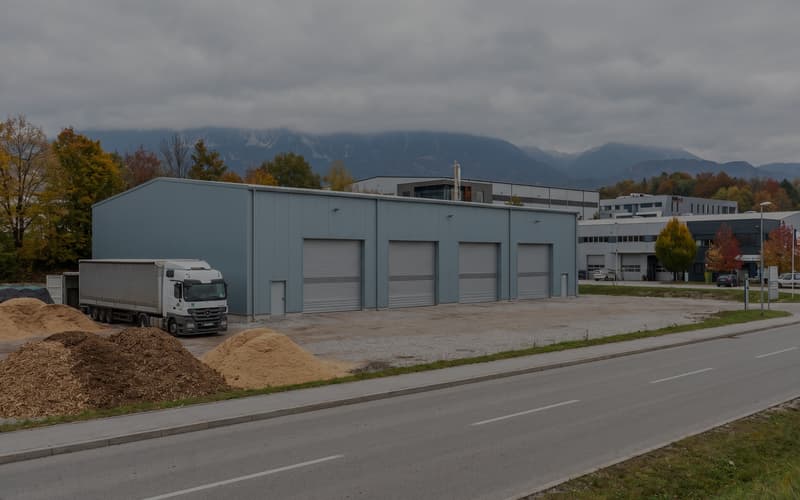
The project is a retrofit of an existing biomass line rather than a greenfield factory. The finished configuration uses a larger practical site of about 6,000 m² with approximately 3,000 m² of covered production and storage space. This corrects the impossible earlier combination of a 2,500 m² site and a 3,000 m² building.
Total completed-project investment is fixed at USD 365,000. The upgraded scope includes controlled receiving, screening, grinding, magnetic protection, three correctly sized MZLH678 pellet mills, a counterflow cooler, finished-pellet screening, dust extraction, enclosed conveying and semi-automatic bagging. RICHI also redesigned the aspiration system so the retrofit addresses dust at source instead of relying on one small filter and a stack alone.
7.5–9T/H
capacity
$365,000
investment
Slovenia
location
Biofuel
project type
RICHI MACHINERY
Why Slovenia?
Slovenia is a logical location for this project because it combines a forest-based manufacturing economy, Central European road and rail access, and an established market for solid biomass heating. The business case is strongest when the plant uses locally or regionally available residues instead of importing low-value bulk biomass over long distances.
| Project Driver | Practical Meaning |
|---|---|
| Wood-processing base | Sawdust, shavings and clean untreated residues can form the main feedstock stream. |
| District and industrial heat users | Higher-ash non-wood pellets can be sold where boiler design allows them. |
| Access to Austria and Italy | Pure wood pellets and industrial biomass fuels can move into nearby markets when specifications and certification match the buyer. |
| Port and rail connectivity | Koper links Slovenia with Central European freight corridors and provides a practical route for imported machinery. |
The page does not use fixed pellet-market volumes, guaranteed margins or old carbon-tax figures as selling points. Those values change with energy prices, contracts and policy. Instead, the project is built around controllable factors: raw-material cost, ash behavior, pellet durability, delivered logistics cost and buyer boiler compatibility.
Residential sales require much tighter fuel-quality control than industrial sales. Pure woody pellets may be marketed under a wood-pellet quality scheme if the producer and product actually meet its requirements. Crop-residue or mixed rice-husk pellets are treated separately for industrial users and are not presented as equivalent residential fuel.
RICHI MACHINERY
Raw Materials: Wood Chips, Bamboo Dust, and Rice Husks
The feedstock basket requires careful separation because the three materials behave very differently. Local wood-processing residues are the preferred base material. Rice husk can be sourced regionally when freight is economical, but it raises ash and silica. Bamboo dust is not treated as a base-load imported commodity from Asia; it is accepted only when available from a nearby processor or trader at a delivered cost that still makes sense.
| Raw Material | Annual Planning Role | Typical Receiving Moisture | Process / Product Logic |
|---|---|---|---|
| Clean sawdust and dry wood residues | Approx. 12,000–14,000 T/A | 8–12% | Main feedstock for low-ash wood pellet grades; screening and grinding as needed. |
| Rice husk | Approx. 3,000–4,000 T/A | 9–13% | Industrial-grade formulas only; higher ash/silica must match the buyer boiler. |
| Bamboo dust or similar dry fibrous fines | Up to 1,000–2,000 T/A when locally available | 8–12% | Optional blend component after contamination and ash checks. |
| Gross annual input | Approx. 20,600–21,200 T/A | Weighted by material mix | Supports about 20,000 T/A finished pellets after screening, handling and moisture loss. |
Chemically treated wood, demolition wood, MDF, particleboard, painted timber and contaminated furniture board are excluded. For ENplus-certified wood pellets, only permitted woody raw materials can be used; rice husk and other non-woody biomass must remain outside that certified product stream.
- Every truck or bulk load is checked for moisture and visible contamination.
- Magnetic separation protects the hammer mill and pellet mills from ferrous material.
- Dry sawdust can bypass intensive grinding when particle size is already suitable.
- Rice husk is stored separately and metered only into industrial formulas.
- Wet material outside the procurement moisture window is isolated rather than forced through the no-dryer line.
The plant keeps a no-main-dryer configuration only because procurement is based on dry residues. If future suppliers deliver green chips, wet straw or high-moisture crop residues, a mechanical drying section would become necessary.
RICHI MACHINERY
The Site and Building
The facility is located in the Celje/Savinja industrial corridor. The corrected site plan uses about 6,000 m² of land with approximately 3,000 m² of covered production and storage area, leaving enough external space for truck circulation, fire access, loading and short-term raw-material handling.
| Area | Approx. Size | Use |
|---|---|---|
| Raw-material warehouse | 1,200 m² | Separated dry sawdust, wood residues and non-wood biomass. |
| Production hall | 1,050 m² | Screening, grinding, buffering, pelleting, cooling and screening. |
| Finished-product warehouse | 550 m² | Bagged and FIBC pellets; short-term bulk dispatch staging. |
| Maintenance / electrical / dust system | 120 m² | Service access, filters, compressor and electrical equipment. |
| Office / welfare | 80 m² | Administration and staff facilities. |
An 8 m clear height is adequate for buffer bins, elevators, the cooler and aspiration ducting when platforms are coordinated with the existing steel structure. Dust-prone equipment is kept within enclosed or locally extracted areas, while hot pellets are no longer spread over the warehouse floor for cooling.
RICHI MACHINERY
Equipment Configuration
The retrofit is centered on three MZLH678 biomass pellet mills. This replaces the earlier claim that four 132 kW machines could each produce 2–2.5 T/H; the authoritative MZLH520 rating is only 1.5–2 T/H, while MZLH678 is the correct 200 kW model for approximately 2.5–3 T/H.
| Equipment | Qty | Key Specification | Function |
|---|---|---|---|
| Receiving / screening system | 1 system | 7.5–9 T/H duty | Removes oversize and routes already-fine material around unnecessary grinding. |
| Magnetic separators | Multiple | Before grinding and pelleting | Protects high-speed equipment. |
| Hammer mill | 1–2 sets | Sized to material and 7.5–9 T/H line demand | Reduces wood/crop residues to typical 2–5 mm feed size. |
| Prepared-material bins / metering | Multiple | Separate woody and non-wood streams | Controls blend and prevents uncontrolled ash variation. |
| Biomass pellet press | 3 × MZLH678 | 200 kW each; 2.5–3 T/H each | 7.5–9 T/H installed pellet capacity. |
| Counterflow cooler | 1 system | Matched to line capacity | Mechanical pellet cooling before storage. |
| Pellet screener / fines return | 1 system | Matched to line capacity | Controls fines and returns clean rework. |
| Dust collection | 1 centralized + local pickups | Grinding, transfer, cooling and screening points | Controls airborne particulate at source. |
| Semi-automatic packing / FIBC route | 1 system | Retail, commercial and bulk handling | Reduces manual handling. |
The biomass fuel pellet machine section is designed for multiple industrial fuel grades, but raw-material streams remain identifiable. Pure wood production and crop-residue-rich production are scheduled in campaigns so quality control and cleaning are manageable.
The completed project investment remains USD 365,000. That figure covers the production system and retrofit scope as a whole; the earlier USD 28,500 dust-only figure is not used as the total equipment value because it cannot represent a line with three pellet mills, cooling, screening, aspiration and packing.
RICHI MACHINERY
Process Flow
This biomass pellet plant uses a no-main-dryer process, but it is no longer described as a minimal line. At 20,000 T/A, mechanical cooling, screening, enclosed conveying and controlled dust extraction are necessary for stable commercial operation.
Step 1: Receiving and Raw-Material Separation
Dry sawdust, clean wood residues and non-wood biomass are received into separate storage zones. Moisture, contamination and ash-sensitive materials are checked before release. Rice husk and optional bamboo dust are never blended into residential wood-pellet production by default.
Step 2: Screening Magnetic Protection and Grinding
Already-fine sawdust passes screening and magnets before moving to prepared-material bins. Oversize wood particles and fibrous crop residues are routed to the hammer mill. Final pellet-feed size is generally kept around 2–5 mm, adjusted to the actual material rather than fixed at one 6 mm screen rule.
Step 3: Metering and Formula Control
Separate buffers allow the operator to run pure wood campaigns or controlled industrial blends. Rice-husk inclusion is limited by the buyer’s ash tolerance and slagging behavior. The plant does not assume that every available residue can be blended at the same percentage.
Step 4: Pelletizing
Prepared material is distributed to three biomass granulators configured as MZLH678 ring-die pellet mills. Each unit provides about 2.5–3 T/H on suitable biomass. Main pellet diameter is 6–8 mm; die compression and feed moisture are tuned by formula during commissioning.
Step 5: Mechanical Cooling
Hot pellets enter a counterflow cooler immediately after pelleting. Floor spreading is removed from the final design because 20,000 T/A production would create contamination, dust, forklift traffic and warehouse-capacity problems. Cooling brings the product close to ambient conditions before screening and storage.
Step 6: Screening and Fines Return
A finished-pellet screen removes loose fines and broken pellets. Clean fines are returned in a controlled proportion. Product destined for retail wood-pellet channels receives tighter fines and durability control than higher-ash industrial biomass grades.
Step 7: Packing and Bulk Dispatch
Retail or distributor orders can use smaller bags, while industrial customers can receive FIBC or bulk truck shipments. Semi-automatic weighing and sewing are used instead of hanging scales and manual floor handling.
Utilities and Consumption
| Utility | Planning Value | Engineering Basis |
|---|---|---|
| Electricity | Approx. 2.2–2.6 million kWh/year | Three 200 kW pellet mills plus grinding, cooling, dust extraction, conveying and packing. |
| Electrical service | Approx. 1.0–1.25 MVA | Allows simultaneous pelletizing and auxiliaries with operating margin. |
| Water | Approx. 250–400 m³/year | Domestic use and housekeeping; no steam conditioning or wet process. |
| Process heat | None in base configuration | No main dryer when incoming raw material meets moisture specification. |
Electricity demand is material-dependent. Dry sawdust requires less preparation power than fibrous crop residues, while all three MZLH678 pellet mills represent the dominant electrical load when running together.
RICHI MACHINERY
How RICHI Customized This Line for the Retrofit
The retrofit focused on three real operating problems: incorrect line sizing, missing mechanical cooling, and insufficient dust control around grinding and transfer points. RICHI therefore treated the project as a process retrofit rather than a filter-only add-on.
- The pelletizing section was standardized around three MZLH678 units so installed capacity matches the 20,000 T/A target.
- A counterflow cooler and pellet screener were added to replace floor cooling and manual rehandling.
- Local extraction points were placed at grinding, transfer, screening and cooling rather than relying on one remote pickup.
- Woody and non-woody raw materials were separated in storage and metering so ENplus-eligible wood production cannot be mixed with rice-husk or other crop-residue batches.
- The control logic was revised so the line can run one, two or three pellet mills depending on order volume and maintenance requirements.
- Packing was upgraded to semi-automatic weighing for repeatable bag weight and cleaner warehouse operation.
Dust performance is verified against the actual filter design, airflow, pressure drop and permit conditions. The case does not publish an unsupported universal 99% collection figure, a fixed 1.56 mg/m³ stack result or a generic 50 mg/m³ legal limit without the project’s test report and permit basis.
The line continues to operate without a main dryer only because dry material procurement is enforced. That design choice saves capital and heat energy, but it also makes incoming moisture control a critical commercial requirement.
RICHI scope covers process review, retrofit engineering, equipment manufacture, factory inspection, export packing, installation guidance, commissioning and operator training. Training is competency-based and covers raw-material acceptance, die/roller adjustment, magnet checks, filter inspection, cooler operation and safe lockout.
RICHI MACHINERY
Product Specifications
The plant makes more than one fuel grade. Pure woody pellets and crop-residue-rich industrial pellets cannot be described under the same certification or ash specification. ENplus certification applies only to wood pellets, so rice-husk or other non-woody blends are sold under buyer-specific industrial specifications instead.
| Property | Pure Wood Pellet Grade | Crop-Residue / Industrial Grade |
|---|---|---|
| Diameter | Mainly 6–8 mm | Mainly 6–8 mm |
| Finished moisture | Usually ≤10% target | Usually 8–12% depending buyer |
| Ash | Controlled to the chosen wood-pellet quality class | Higher and formula-dependent; rice husk can raise ash substantially |
| Mechanical durability | Verified against buyer/certification requirement | Verified against transport and boiler-handling requirement |
| Bulk density | Checked by batch | Checked by batch |
| Raw-material eligibility | Permitted woody biomass only for ENplus-certified production | May include rice husk or other approved non-wood residues |
| Main use | Residential/commercial wood-pellet users if certified and compliant | Industrial boilers and district-energy systems designed for higher-ash fuel |
A mixed rice-husk or bamboo-containing product is therefore not advertised as ENplus A2. The ENplus scheme is specifically for wood pellets and excludes non-woody biomass from certification. Pure woody campaigns can pursue certification only when the company, raw material and finished pellets meet the scheme requirements.
The case also avoids fixed historical retail prices and a claim of zero carbon emissions. Delivered fuel value depends on current energy markets, moisture, ash, transport distance and the user’s combustion system. Biomass can have biogenic carbon accounting benefits under specific frameworks, but it is not physically emission-free.
RICHI MACHINERY
Market Outlook for Crop Residue Pellets in Slovenia
The most defensible opportunity is industrial heat, not a blanket claim that all Slovenian pellet users will accept mixed crop-residue fuel. Wood pellets have an established residential and commercial market, while rice-husk and other agricultural-residue pellets need boilers that can tolerate higher ash, silica and different slagging behavior.
| Market Route | Product Fit | Key Buyer Check |
|---|---|---|
| Slovenian industrial boilers | Wood or approved crop-residue pellets | Ash limit, grate design, fuel feeding and emissions permit. |
| District-energy operators | Usually standardized industrial biomass fuels | Contract specification and ash-handling capacity. |
| Residential pellet heating | Pure wood grade only where appliance and certification requirements are met | ENplus status, fines, ash and appliance warranty conditions. |
| Austria / Italy export | Product-specific opportunity | Certification, customs/logistics, delivered price and buyer specification. |
Slovenia’s location supports both domestic and regional sales. Port of Koper has regular rail connections through Ljubljana, Celje and Maribor and frequent links to Austria, so imported equipment and export-oriented freight can use established intermodal corridors.
The plant manages supply risk by prioritizing several local wood-processing suppliers and keeping non-wood residues as flexible industrial ingredients rather than depending on imported bamboo dust as a permanent base feedstock. That materially reduces freight exposure and keeps the project tied to the regional resource base.
RICHI MACHINERY
Why a Crop Residue Pellet Line Makes Sense in Slovenia
The project makes sense when the plant is treated as a flexible biomass-fuel factory rather than a single-grade residential pellet mill. Local dry wood-processing residues provide the stable core volume, while selected agricultural by-products create additional industrial products when buyer specifications and ash behavior allow them.
The no-dryer design is an advantage only under controlled procurement. Dry sawdust and pre-dried residues can move directly through screening, grinding and pelleting, but wet green biomass would change the entire energy balance and require a dryer, fuel system, additional dust control and more floor area.
Equipment ships from Qingdao to the Port of Koper, then moves inland toward Celje/Savinja by road or rail. Koper publishes regular domestic rail services through Ljubljana–Celje–Maribor and frequent links to Austria, making it a practical gateway for both machinery import and regional freight.
For another crop residue pellet manufacturing system, RICHI Machinery would first confirm raw-material origin, monthly tonnage, moisture, particle size, ash and silica, target fuel grade, buyer boiler type, packaging route and electrical capacity. Those inputs decide whether the correct design needs a dryer, how many pellet mills are required, and whether separate woody and non-woody production campaigns are necessary.
A complete biomass pellet project for this scale typically requires coordinated building adaptation, utilities, dust control, installation and commissioning. For an existing-building retrofit, a practical implementation window is about 5–7 months when civil work, electrical upgrades and import logistics are prepared in parallel.
● RICHI MACHINERY
RICHI Service

● Consulting
Customer Consultation
We want to have a deep understanding of your industrial process, to know your exact needs of feed, wood, biomass, fertilizer or other pellet processing.
● Design
biomass Pellet Plant Design
Based on your unique situation and industrial process, we will tailor complete pellet plant you need, and inform you of every additional detail that could facilitate operation, minimize total cost.

● Manufacturing
Equipment Manufacturing
The critical components of the of the complete pellet production line equipment are built in our own workshops in Asia. Additional equipment is manufactured by our worldwide network of reliable partners.

● Testing
Quality Inspection & Testing
Before leaving the factory, all equipment will be inspected by the quality inspection department. We can also provide customers with testing services from a single machine to a complete pellet plant system, and provide you with real actual data for “worry-free use.”

● Delivery
Equipment Delivery
In equipment boxing and packaging, we adopt professional packaging and modular solutions to ensure the safe and non-destructive delivery of pellet plant equipment.

● Installation
Installation & Commissioning
Whether you choose your own subcontractor for the erection phase or you want to install everything together with us, a Richi supervisor will be around to make sure everything is mounted in a safe and thorough way.

● Training
Staff Training
We provide comprehensive training for the technicians of each project. We can also continue to provide support for the technicians during latter project operation.

● After-sales
Project Follow-Up
When everything is up and running our Richiers will help you further whenever needed. We are ready to answer your call 24/7.We’ll also visit you regularly to learn about your needs.

Who we are
RICHI Machinery is one of the world’s leading suppliers of technology and services for the animal feed, aqua feed and pet food industries, also the largest pellet production line manufacturer in China.
Since 1995, RICHI’s vision to build a first-class enterprise, to foster first-class employees, and to make first-class contributions to society has never wavered.
In the past three decades, we have expanded our business to a wide range of areas, including animal feed mill equipment, aqua feed equipment, pet feed equipment, biomass pellet equipment, fertilizer equipment, cat litter equipment, municipal solid waste pellets equipment, etc.

1995
RICHI Established

2000+
Serving More Than 2000 Customers

120+
RICHI Employees

140+
Exported To 140 Countries



