 0086-138 3838 9622
Biomass Residue Pellet Production System for Fuel in Ireland
RICHI MACHINERY
Project Overview
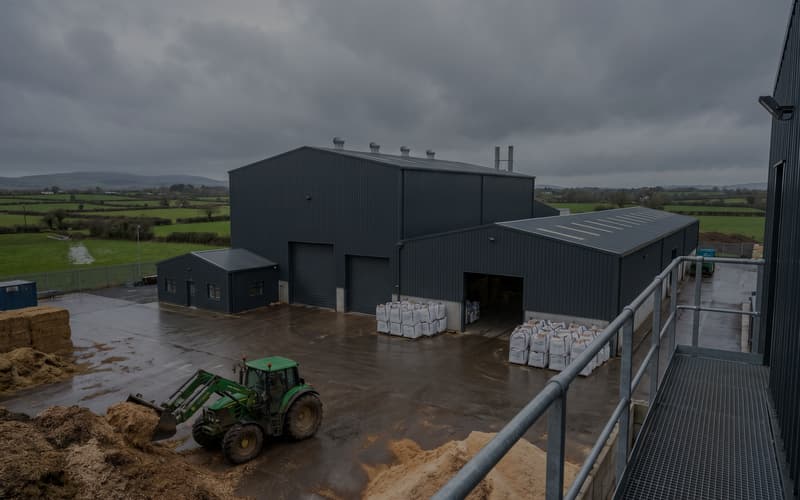
An agricultural-logistics entrepreneur in County Cork developed this Biomass Residue Pellet Production System for Fuel in Ireland to convert locally available cereal straw and clean wood-processing residues into two clearly separated fuel products: pure wood pellets and non-woody or blended industrial biomass pellets. The project uses the same receiving, grinding, drying and pelletizing infrastructure, but production campaigns are separated because residential wood-pellet specifications and straw-pellet combustion behavior are not interchangeable.
Annual finished output is 30,000 T/A. With 250 operating days and two 8-hour shifts, the calculated average requirement is 7,500 kg/h, so the installed pelletizing section is sized above the minimum at 9–12 T/H. Three MZLH768 biomass pellet mills, each 315 kW and rated at 3–4 T/H, provide enough margin for die changes, maintenance, dryer fluctuations and the lower throughput that can occur with fibrous straw formulations.
The line receives roughly 35,000 T/A of wet biomass: about 23,000 tons of clean sawdust and shavings plus about 12,000 tons of wheat, barley and oat straw. Field-dry straw can often bypass thermal drying, while wetter sawdust or rain-affected straw uses a biomass-fired drying route. After moisture removal, screening loss and fines recycle, the plant produces about 18,000 T/A of pure wood pellets and 12,000 T/A of straw or wood-straw industrial pellets.
The completed project represents a fixed total investment of USD 760,000, including a USD 485,000 RICHI equipment package. The project uses a 3,000 m² production building, a 2,800 m² warehouse and a 200 m² office within an approximately 9,000 m² industrial site, leaving space for truck circulation, fire access, unloading and outdoor service areas.
9-12T/H
capacity
$760,000
investment
Ireland
location
Biofuel
project type
RICHI MACHINERY
Why Ireland?
Ireland has a credible feedstock base for a mixed biomass project. The Central Statistics Office reported 2.31 million tonnes of wheat, barley and oats in 2025, including about 1.37 million tonnes of barley, 664,000 tonnes of wheat and 282,000 tonnes of oats. Those crops generate substantial straw volumes, although not every ton is available for energy because bedding, feed, soil management and other farm uses compete for the same material.
Wood residues are the second supply pillar. Ireland continues to expand and mobilize its forest resource, and County Cork recorded the largest area of new forest established in 2024. Sawmills, pallet producers and solid-wood processors therefore provide a more realistic woody feedstock stream than mixed furniture or demolition waste.
| Market / Customer | Suitable Product | Why the Separation Matters |
|---|---|---|
| Residential and small commercial pellet users | Pure wood pellets | These buyers need low-ash wood fuel and compatible appliances |
| Food, dairy and process-heat users | Wood pellets or approved industrial biomass pellets | Larger boilers may accept a wider fuel specification |
| Industrial boilers designed for agricultural biomass | Straw or wood-straw pellets | Ash, chlorine and slagging behavior must match the combustion system |
| Regional distributors / export customers | Product-specific batches | Wood and non-woody pellets require different declarations and buyer specifications |
Ireland’s current renewable-heat support is the Support Scheme for Renewable Heat, not the older RHI language often used in legacy market descriptions. The SSRH provides an operational tariff for eligible biomass and biogas heating systems for up to 15 years, supporting non-domestic heat users rather than directly subsidizing this pellet factory.
The carbon tax reached €71 per tonne of CO₂ for non-auto fuels from 1 May 2026, which strengthens the long-term pressure to reduce fossil-fuel heat use. Even so, pellet economics still depend on delivered fuel price, boiler efficiency, moisture, ash and the customer’s eligibility for support; the project does not assume a guaranteed margin or fixed import-substitution volume.
RICHI MACHINERY
Raw Materials: Crop Residues and Wood Waste
The production plan uses cereal straw and clean pre-consumer wood residues from farms, sawmills and solid-wood processors. The feedstock mix is managed by product campaign so pure wood pellets are not contaminated with straw when a customer requires a wood-only specification.
| Raw Material | Approx. Annual Intake | Typical Receiving Moisture | Preparation Route |
|---|---|---|---|
| Clean sawdust / wood shavings | 23,000 T/A | About 20–28% for mixed sawmill supply | Screen, magnet, dry as required, fine grind if needed |
| Wheat / barley / oat straw | 12,000 T/A | About 14–20% when baled and covered | Bale opening, cutting, hammer milling; dryer only when required |
| Gross intake | Approx. 35,000 T/A | Supply-dependent | Supports about 30,000 T/A finished pellets after moisture and process losses |
Only untreated wood is accepted. Painted timber, preservative-treated wood, MDF, particleboard, OSB, adhesive-rich panel waste and demolition wood are excluded from the normal pellet route. This protects combustion quality and is essential if the client sells a certified or premium wood-pellet grade.
- Straw suppliers are contracted within an economical collection radius, with part of the seasonal inventory remaining in covered farm or contractor storage.
- Wood suppliers are approved by residue type and moisture rather than being treated as one generic sawdust source.
- Incoming lots are checked for moisture, stones, metal, soil and visible mold before processing.
- Dry straw can bypass the dryer; green sawdust and rain-affected material are dried before pelletizing.
- Wood and straw campaigns use separate bins, cleaning sequences and batch records to limit cross-contamination.
A 2,800 m² warehouse cannot economically hold six months of loose or baled straw for this output. The plant therefore keeps a shorter on-site buffer and relies on contracted off-site bale storage and scheduled deliveries through the year.
RICHI MACHINERY
The Site and Building
The factory is located in an industrial area in County Cork. The approximately 9,000 m² site combines 6,000 m² of covered buildings with truck movement, fire separation and loading space. The distinction between building area and total site area prevents the layout from becoming unrealistically dense.
| Building / Area | Approx. Size | Use |
|---|---|---|
| Production building | 3,000 m² | Bale opening, grinding, drying, pelletizing, cooling, screening and packing |
| Raw / finished warehouse | 2,800 m² | Divided between short-term feedstock buffer and packaged product |
| Office / welfare / QC | 200 m² | Administration, records, sampling and staff facilities |
| Outdoor unloading / circulation | Balance of approx. 9,000 m² site | Truck turning, unloading, fire access and service routes |
The 8 m production-building height supports a mainly horizontal line with bucket elevators and conveyors at selected transfer points. Straw preparation is separated from the cleaner wood-pellet route so fibrous dust, soil and agricultural residues can be controlled before the line changes to premium wood production.
The dryer, burner and exhaust-treatment section is fire-separated from dry pellet storage. The three pellet mills are arranged in parallel with independent feed screws and maintenance clearance so one machine can be serviced without stopping the entire plant.
Finished pellets are stored under cover on a dry floor. Pure wood grades and industrial straw/mixed grades remain physically identified by batch because they are sold to different boiler markets.
RICHI MACHINERY
Equipment Configuration
The client selected a complete biomass pellet production line with flexible bypasses for dry straw and fine sawdust. Three MZLH768 units are used because the project must sustain 30,000 T/A within 4,000 annual production hours while leaving maintenance and material-variation margin.
| Process Section | Main Equipment | Project Configuration |
|---|---|---|
| Straw receiving | Bale breaker / straw cutter | 8–10 T/H class; used only for baled crop residues |
| Coarse wood preparation | Chipper / crusher where required | Handles oversize clean wood residues |
| Fine grinding | 2 hammer mills + magnets + aspiration | 9–12 T/H combined preparation duty |
| Drying | Biomass-fired dryer with bypass and exhaust cleaning | Used mainly for wet sawdust and rain-affected straw |
| Pelletizing | 3 × MZLH768 biomass pellet mill | 315 kW each; 3–4 T/H each; 9–12 T/H installed capacity |
| Pellet press reference | Biomass pellet press | Same ring-die MZLH route; separate dies/settings by product campaign |
| Cooling | Counterflow cooler | Matched to 9–12 T/H line |
| Screening | Pellet screener + fines return | Removes loose fines before storage |
| Dust / dryer exhaust | Bag filters plus dryer particulate/wet polishing as permit requires | Separate dry dust from hot exhaust treatment |
| Packing | 2 weighing / bagging stations | 25 kg bags, FIBC and bulk dispatch |
The fixed RICHI equipment package is USD 485,000. The USD 760,000 completed-project investment also covers local foundations, electrical connection, burner and exhaust works, warehouse modifications, internal handling, installation, commissioning and initial working capital.
The dryer heat source is clean biomass residue or process fuel suitable for the burner, not an assumption that electricity will evaporate several thousand tonnes of water economically. Thermal duty is controlled by actual inlet moisture, and sufficiently dry straw bypasses the dryer.
RICHI MACHINERY
Process Flow
This biomass pellet plant uses two related but distinct production campaigns. Wood-pellet campaigns keep the feed stream woody; straw or wood-straw campaigns accept higher-ash agricultural biomass and are sold to compatible industrial boilers.
Step 1: Receiving and Product-Campaign Segregation
Straw bales, sawdust and other approved wood residues are unloaded into defined storage zones. The production schedule specifies whether the next campaign is pure wood or non-woody/blended fuel so bins, conveyors and fines return can be cleaned appropriately.
Step 2: Bale Opening and Coarse Size Reduction
Baled straw is mechanically opened and cut before fine grinding. Oversize clean wood pieces are chipped or crushed separately. Fine sawdust bypasses coarse size reduction.
Step 3: Fine Grinding
Prepared biomass passes through two wood pellet hammer mill units. Screen selection is adjusted to raw material and die behavior, typically producing a few-millimeter feed rather than forcing one fixed screen size on every straw/wood recipe.
Step 4: Moisture Control and Drying
Moisture is measured before drying. Material above the pelletizing window is dried to roughly 10–14%, while sufficiently dry straw bypasses the thermal stage. The biomass burner and dryer controls are sized around evaporation load, not a fixed temperature and retention time for every season.
Dryer exhaust first removes entrained particles through appropriate separation equipment. A wet polishing stage can be used where the approved air-emissions design requires it, with make-up water and blowdown handled separately from stormwater.
Step 5: Pelletizing
Prepared material enters three biomass fuel pellet machine units in the MZLH768 configuration. Product diameter is normally 6–8 mm. Die compression and roller settings are established during commissioning because straw, spruce/pine sawdust and mixed biomass do not require the same compression conditions.
Step 6: Mechanical Cooling
Hot pellets discharge to a counterflow cooler. Mechanical cooling brings pellet temperature close to ambient before screening and storage; conveyor-only natural cooling is not used as the main cooling method for a 30,000 T/A plant.
Step 7: Screening and Fines Return
Cooled pellets pass through a final screen. Clean fines return to the same product campaign. Fines from a straw batch are not automatically returned into a subsequent premium wood batch.
Step 8: Packing and Dispatch
Wood pellets can be packed in 15–25 kg bags, FIBC or bulk depending on buyer requirements; industrial straw/mixed pellets are mainly dispatched in bulk or larger bags. Batch identification records raw-material category, production date and quality results.
RICHI MACHINERY
Utilities and Consumption
The electrical load is dominated by three 315 kW pellet mills, two hammer mills, aspiration, cooling, conveying and packing. The dryer adds fan and feed-system power but receives most of its thermal energy from a biomass burner rather than electric resistance heating.
| Utility | Practical Annual Planning Range | Engineering Basis |
|---|---|---|
| Electricity | Approx. 3.2–4.0 million kWh/year | About 105–135 kWh per ton depending on grinding, drying and product mix |
| Electrical service | Approx. 1.6–2.0 MVA | Three MZLH768 units plus preparation and auxiliaries |
| Biomass dryer fuel | Approx. 1,800–2,500 T/A | Depends on incoming sawdust moisture, straw bypass rate and burner efficiency |
| Dryer scrubber / cooling make-up water | Approx. 800–1,200 m³/year | Only where wet polishing is used |
| Domestic / cleaning water | Approx. 300–500 m³/year | About 20 staff plus housekeeping |
| Fire-water reserve | Separate engineered storage | Sized by approved fire-protection design |
The plant operates 16 production hours per day over about 250 days per year. The remaining daily hours provide maintenance time for die and roller inspection, hammer-mill screen changes, dryer cleaning and dust-system checks.
Electrical capacity is verified against simultaneous motor starts and transformer loading. If standby generation is installed, it is sized for selected critical loads or reduced production; a small generator is not represented as capable of operating the entire 9–12 T/H pellet line.
About 20 employees cover two production shifts, warehouse, quality control, maintenance, supervision and administration. Front-end loader staffing varies with delivery schedule rather than requiring three loaders to operate continuously.
RICHI MACHINERY
How RICHI Customized This Line for Biomass Residues
The main engineering issue is not simply that straw is fibrous and sawdust is powdery. The two materials lead to different preparation, drying, ash, certification and end-use requirements, so the factory has to protect product identity as carefully as it protects throughput.
- Three MZLH768 pellet mills provide 9–12 T/H installed capacity, giving the 30,000 T/A project operating margin above its 7,500 kg/h calculated average requirement.
- A bale-opening route handles cereal straw, while fine sawdust can bypass coarse size reduction.
- Moisture-based dryer bypass prevents field-dry straw from consuming unnecessary thermal energy.
- Pure wood and straw/mixed campaigns use separate production scheduling, die settings and batch identification.
- Counterflow cooling and screening replace conveyor-only cooling and keep packaged fines under control.
- Dry-grinding dust and dryer exhaust are treated as separate emission streams instead of being routed through one generic collector.
For straw campaigns, the existing straw pellet machine anchor refers to the same biomass ring-die platform configured for fibrous agricultural residues. RICHI selects die geometry and operating parameters from the actual straw species, moisture and required industrial fuel specification rather than publishing one universal compression ratio.
Operator training covers product changeover, bale handling, moisture decisions, hammer-mill screens, MZLH die/roller service, dryer balance, cooler operation, dust housekeeping and fire-response procedures. Competence is checked through supervised operation instead of a fixed two-week proficiency claim.
The line also leaves physical and electrical space for a fourth production module or additional storage only if future feedstock and off-take contracts justify expansion; capacity is not added without reviewing dryer, cooler and transformer bottlenecks.
RICHI MACHINERY
Product Specifications
The factory sells wood and agricultural-biomass pellets under separate specifications. Only pellets made from woody biomass can be ENplus certified, so straw pellets and intentional wood-straw blends are not presented as ENplus A1 or A2. Non-woody and mixed pellets can instead be specified against industrial buyer requirements and, where appropriate, ISO 17225-6:2021 for graded non-woody pellets.
| Property | Pure Wood Pellet Grade | Straw / Wood-Straw Industrial Grade |
|---|---|---|
| Diameter | 6–8 mm | Typically 8 mm |
| Length | Typically 10–40 mm | Typically 10–40 mm |
| Finished moisture | Usually 8–10% | Usually 8–12% |
| Ash | Controlled to selected wood-pellet class / buyer specification | Higher and raw-material dependent; commonly several percent |
| Calorific value | Generally about 16.5–18 MJ/kg | Generally about 15–17 MJ/kg depending straw/wood ratio |
| Ash melting / slagging | Checked where relevant | Important buyer parameter for straw-rich fuel |
| Mechanical durability / fines | Tested for commercial grade | Tested for handling and boiler-feed requirements |
If the customer pursues ENplus certification, the certification applies only to the qualifying wood-pellet stream and requires the company’s production, quality and bagging system to meet the current scheme rules. Simply achieving one ash or moisture number does not make a pellet ENplus certified.
Straw-rich pellets are targeted to boilers designed for agricultural biomass because ash quantity, alkali/chlorine content and ash-melting behavior can differ materially from clean wood. Residential wood-pellet stoves should not be assumed to accept straw pellets.
The case does not embed fixed 2025 selling prices. Irish and UK fuel prices, exchange rates, bags and freight change, so quotations should use current contracts and the exact certified or industrial product grade.
RICHI MACHINERY
Market Outlook for Biomass Pellets in Ireland
Ireland’s 2025 cereal crop provides a substantial agricultural-residue base: wheat, barley and oats together reached about 2.31 million tonnes. The Department of Agriculture also reports continuing forest expansion and expects timber and wood mobilisation to increase, supporting a second long-term source of clean processing residues.
On the demand side, the Support Scheme for Renewable Heat remains active in 2026. Eligible commercial, industrial, agricultural, district-heating and public-sector users can receive an operational tariff for biomass or biogas heat for up to 15 years. That creates a more defensible non-domestic market driver than the outdated claim that homeowners receive an RHI pellet-stove subsidy.
| Commercial Challenge | Project Response |
|---|---|
| Straw has higher ash / slagging risk | Sell to compatible industrial boilers and declare the fuel grade |
| Straw supply is seasonal | Use contracted farm storage plus a shorter on-site buffer |
| Wet sawdust raises drying cost | Buy by moisture class and maximize dryer bypass |
| Wood-pellet certification must remain clean | Separate wood-only campaigns from agricultural biomass |
| Island logistics | Use Cork’s container / RoRo network for imported equipment and regional exports |
| Energy prices change | Quote delivered fuel and useful heat value instead of claiming a fixed margin |
Ireland’s carbon tax is €71 per tonne of CO₂ for relevant non-auto fuels from May 2026, increasing the policy pressure on fossil heat. Biomass still has to meet sustainability, air-emissions and boiler-efficiency requirements; it is not automatically the lowest-cost solution for every site.
The project does not rely on claims that Ireland imports a fixed volume of pellets, that only a few competitors exist, or that a 20–25% operating margin is guaranteed. Expansion decisions are tied to wood/straw contracts, certified product demand and industrial off-take.
RICHI MACHINERY
Why a Biomass Residue Pellet Plant Makes Sense in Ireland
This project makes sense because County Cork gives the client access to both sides of the feedstock equation: cereal-farming residues from southern Ireland and clean sawmill/wood-processing residues from a forestry sector that is still expanding. The two feedstocks are processed on common equipment but sold as distinct fuels.
The 9–12 T/H installed capacity is deliberately higher than the minimum annual average. It leaves room for maintenance and for straw batches that pellet more slowly than uniform sawdust, making the 30,000 T/A target more realistic within a 250-day, two-shift schedule.
For equipment delivery, a practical route is Qingdao to a major north-European transshipment hub such as Rotterdam or Antwerp, then feeder service to Cork Container Terminal at Ringaskiddy and road delivery to the County Cork site. The Port of Cork currently operates container links with Rotterdam, Antwerp, Bremerhaven and Southampton and handles project cargo at Ringaskiddy.
Regional pellet sales can also use Cork’s maritime links, while domestic Irish customers move by road. Shipments to Great Britain require the relevant post-Brexit customs and product documentation; the page does not describe UK trade as customs-free.
For another biomass pellet project, RICHI would first confirm annual tonnage by product, wood-versus-straw split, monthly feedstock moisture, certification target, industrial boiler requirements, warehouse days, power connection and dryer fuel. These inputs determine the correct MZLH quantity, dryer duty, cooler size and storage plan.
RICHI scope covers process engineering, equipment manufacture, factory inspection, export packing, control-system preparation, installation guidance, commissioning and operator training. A practical implementation window for an existing industrial site of this scale is about 6–8 months when building adaptation, transformer work and equipment manufacture proceed in parallel.
● RICHI MACHINERY
RICHI Service
● Consulting
Customer Consultation
We want to have a deep understanding of your industrial process, to know your exact needs of feed, wood, biomass, fertilizer or other pellet processing.
● Design
biomass Pellet Plant Design
Based on your unique situation and industrial process, we will tailor complete pellet plant you need, and inform you of every additional detail that could facilitate operation, minimize total cost.
● Manufacturing
Equipment Manufacturing
The critical components of the of the complete pellet production line equipment are built in our own workshops in Asia. Additional equipment is manufactured by our worldwide network of reliable partners.
● Testing
Quality Inspection & Testing
Before leaving the factory, all equipment will be inspected by the quality inspection department. We can also provide customers with testing services from a single machine to a complete pellet plant system, and provide you with real actual data for “worry-free use.”
● Delivery
Equipment Delivery
In equipment boxing and packaging, we adopt professional packaging and modular solutions to ensure the safe and non-destructive delivery of pellet plant equipment.
● Installation
Installation & Commissioning
Whether you choose your own subcontractor for the erection phase or you want to install everything together with us, a Richi supervisor will be around to make sure everything is mounted in a safe and thorough way.
● Training
Staff Training
We provide comprehensive training for the technicians of each project. We can also continue to provide support for the technicians during latter project operation.
● After-sales
Project Follow-Up
When everything is up and running our Richiers will help you further whenever needed. We are ready to answer your call 24/7.We’ll also visit you regularly to learn about your needs.
Who we are
RICHI Machinery is one of the world’s leading suppliers of technology and services for the animal feed, aqua feed and pet food industries, also the largest pellet production line manufacturer in China.
Since 1995, RICHI’s vision to build a first-class enterprise, to foster first-class employees, and to make first-class contributions to society has never wavered.
In the past three decades, we have expanded our business to a wide range of areas, including animal feed mill equipment, aqua feed equipment, pet feed equipment, biomass pellet equipment, fertilizer equipment, cat litter equipment, municipal solid waste pellets equipment, etc.

1995
RICHI Established

2000+
Serving More Than 2000 Customers

120+
RICHI Employees

140+
Exported To 140 Countries