

 0086-138 3838 9622
Hardwood Bedding Pellet Line for Poultry Houses in Malaysia
RICHI MACHINERY
Project Overview
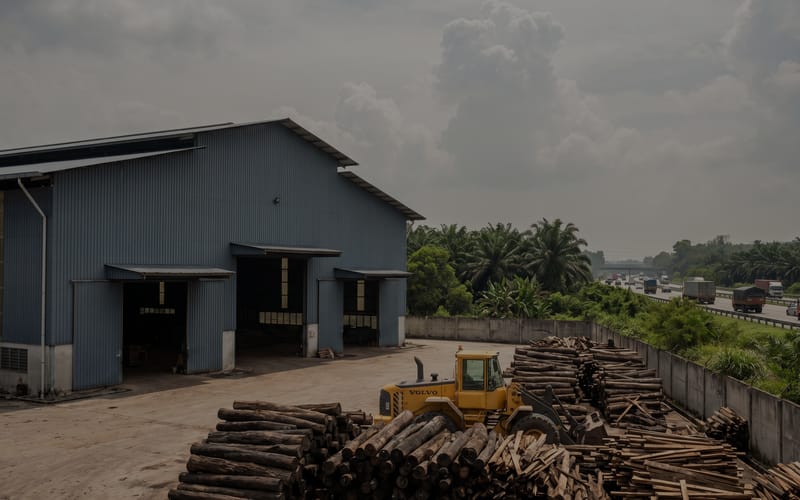
A wood-recycling business in Klang, Selangor developed this Hardwood Bedding Pellet Line for Poultry Houses in Malaysia to convert clean solid-hardwood residues into a compact poultry bedding product. The project serves broiler, breeder and layer operations that need consistent, low-fines litter material while giving nearby furniture processors a controlled outlet for suitable dry residues.
Finished capacity is planned at 15,000 T/A. With 261 operating days and one 8-hour production shift, average required output is about 7.18 T/H. The installed pelletizing section therefore uses three MZLH678 biomass pellet mills, each 200 kW and rated at 2.5–3 T/H, providing 7.5–9 T/H total capacity and enough operating margin for material variation, die service and normal downtime.
The project is deliberately based on pre-consumer solid-wood residues rather than mixed demolition or household furniture waste. Kiln-dried hardwood offcuts, blocks, shavings and sawdust from furniture and joinery factories are accepted after inspection. Painted wood, varnished pieces, MDF, particleboard, plywood, laminates, preservative-treated timber and mixed post-consumer furniture are excluded because poultry bedding requires much tighter contamination control than ordinary fuel pellets.
The plant uses an existing 3,000 m² covered building within an approximately 5,000 m² industrial site. Total completed-project investment is USD 420,000, including a USD 285,000 RICHI machinery package. The line includes receiving and sorting, primary size reduction, hammer milling, magnetic protection, three pellet mills, counterflow cooling, screening, fines return, dust collection and bagging.
8T/H
capacity
$420,000
investment
Malaysia
location
Bedding
project type
RICHI MACHINERY
Why Malaysia?
Malaysia gives this project two practical conditions at the same time: a large commercial poultry sector and an established furniture/timber-processing base. Department of Statistics Malaysia data for 2024 reported about 327.3 million chickens and approximately 1.83 million tonnes of chicken meat production. Johor, Selangor and Perak are among the main poultry-producing states, so a Klang-based bedding supplier can reach several intensive production areas by road.
The opportunity is not that every farm must replace rice husk with pellets. Rice husk remains widely available and cost-sensitive farms may continue to use it. Hardwood bedding pellets target farms that value predictable moisture, controlled fines, compact storage and the ability of pellets to swell and break down into a litter layer after placement and moisture exposure.
| Buyer Segment | What Matters to the Buyer | Project Response |
|---|---|---|
| Large broiler farms | Fast spreading, litter moisture control, predictable deliveries | Bulk or large-bag hardwood bedding pellets |
| Breeder farms | Clean material, low loose fines, reliable lot quality | Tighter raw-material acceptance and screening |
| Layer / pullet operations | Dry bedding where litter systems are used | Controlled moisture and batch identification |
| Distributors / integrators | Storage density and repeatable specifications | Bagged and bulk dispatch options |
Bedding performance depends on house ventilation, drinker management, stocking density, litter depth and reuse practice as well as the bedding material itself. The page therefore does not claim a fixed ammonia reduction, mortality reduction or universal absorbency percentage. Commercial trials should compare the product with the farm’s current litter under the same operating conditions.
For a 15,000 T/A plant, the strongest sales territory is domestic Peninsular Malaysia. Export can be considered for nearby buyers, but it is not required to justify the project because Selangor is already connected to major poultry, logistics and manufacturing markets.
RICHI MACHINERY
Raw Materials: Clean Hardwood Waste
The feedstock is clean hardwood residue generated during furniture, joinery and solid-timber processing. Pre-consumer material gives the plant better traceability than mixed municipal wood because the factory can identify timber type, treatment history and storage condition before the material reaches the pellet line.
| Material Form | Typical Receiving Condition | Preparation Route |
|---|---|---|
| Kiln-dried offcuts / blocks | Dry, clean solid wood; large pieces | Chipping then hammer milling |
| Wood shavings | Usually dry and low density | Screening and controlled grinding as needed |
| Sawdust | Fine, dry, variable bulk density | Magnetic protection and buffer; may bypass coarse chipping |
| Short solid-wood trim | Dry but irregular in size | Primary size reduction before milling |
Annual gross intake is planned at roughly 15,700–16,300 tons to support 15,000 tons of finished bedding pellets after screening rejects, handling losses, moisture adjustment and fines management. Procurement contracts are spread across several factories so the line is not dependent on one furniture producer’s production schedule.
- Accepted wood must be untreated solid timber with a known industrial origin.
- Painted, coated, varnished, preservative-treated or chemically treated timber is rejected.
- MDF, particleboard, OSB, plywood, laminates and glued composite panels are excluded.
- Metal fasteners are controlled by visual sorting and magnetic protection; magnets do not replace incoming inspection.
- Wet or mold-affected loads are segregated because poultry bedding must remain clean and storage-stable.
The installed line does not include a wood chip dryer. This is viable because the purchasing program is centered on kiln-dried furniture residues and incoming moisture is controlled, generally around 8–12% for direct processing. Loads above the agreed moisture window are rejected, segregated for off-site drying or held outside the normal production plan rather than being forced through a no-dryer line.
RICHI MACHINERY
The Site and Building (3,000m² Total)
The 3,000 m² figure represents the covered operating building, not the entire land parcel. The industrial site is approximately 5,000 m² so trucks can unload safely and the plant can maintain circulation, fire access, outdoor maneuvering space and separation between incoming wood and finished bedding pellets.
| Zone | Approx. Covered Area | Use |
|---|---|---|
| Raw-material receiving / storage | 900 m² | Segregated offcuts, shavings and sawdust |
| Chipping / grinding | 450 m² | Primary size reduction, hammer milling and dust extraction |
| Pelletizing / cooling / screening | 850 m² | Three MZLH678 mills, cooler and pellet screen |
| Finished product / packing | 550 m² | Bagging, palletizing and dispatch stock |
| Electrical / maintenance / office | 250 m² | Controls, spare parts, workshop and administration |
The building has a concrete floor and about 8 m clear height. A single-story arrangement is practical at this scale, but conveyors and elevators are positioned to keep the line compact and to preserve maintenance access around grinders, pellet mills, the cooler and dust filters.
Malaysia’s humid climate makes warehouse management important even when the raw wood arrives dry. Finished pellets are kept off the floor where practical, protected from rain splash and condensation, and managed on a first-in/first-out basis so long storage does not undo the moisture control achieved during production.
RICHI MACHINERY
Equipment Configuration
The wood pellet production line is configured as an animal-bedding system rather than a fuel-pellet line with a different bag label. Capacity is carried by three MZLH678 pellet mills, while preparation, cooling and screening are sized to the full 8 T/H project duty.
| Process Section | Main Equipment | Qty / Specification | Function |
|---|---|---|---|
| Primary size reduction | Wood chipper machine | 1, sized to offcut dimensions | Turns solid offcuts into manageable chips |
| Fine grinding | Wood pellet hammer mill | 2 parallel units | Produces consistent pellet-mill feed |
| Pelletizing | Wood pellet mill / wood granulator machine | 3 × MZLH678; 200 kW each; 2.5–3 T/H each | 7.5–9 T/H installed bedding-pellet capacity |
| Cooling | Counterflow cooler | 1 × 8–10 T/H class | Reduces pellet temperature before screening and storage |
| Screening | Pellet screener + fines return | 1 set | Controls loose fines and recycles clean material |
| Dust control | Bag filters / aspiration network | By emission point | Grinding, transfer and screening dust control |
| Packing | Bagging conveyor and scale | 25 kg / project-specific bags | Farm and distributor dispatch |
| Pneumatics / controls | Air compressor + PLC controls | Project-specific | Gates, monitoring and interlocks |
Three MZLH678 units are used because 15,000 T/A over 261 eight-hour days requires an average of about 7.18 T/H. A two-machine 6–8 T/H arrangement would leave too little operating margin once die changes, maintenance and hardwood variability are considered.
The USD 285,000 RICHI machinery package includes the core preparation, pelletizing, cooling, screening, conveying, aspiration, electrical-control and packing equipment. The USD 420,000 completed-project investment also covers local building adaptation, foundations, power connection, installation work and initial operating capital.
RICHI MACHINERY
Process Flow
The process is designed around one principle: only clean, dry solid-wood residues enter the bedding stream. The line does not try to make contaminated furniture waste acceptable through grinding. Sorting and material approval come before mechanical processing.
Step 1: Receiving Sorting and Magnetic Protection
Factory residues are unloaded by material form and supplier lot. Operators check coatings, composite wood, metal, plastic, mold and excessive moisture. Sawdust and shavings are kept separate from large offcuts so each fraction can take the shortest practical processing route.
Step 2: Chipping for Large Solid Wood
Large offcuts enter the wood chipper. Sawdust and suitable small shavings bypass this step. Chipping capacity is matched to the share of large material rather than forcing the entire 8 T/H stream through a high-power chipper.
Step 3: Hammer Milling
Chips and coarse residues pass through parallel hammer mills to reach a consistent particle size suitable for ring-die pelletizing. Screen selection is confirmed during commissioning because hardwood species, shaving content and target pellet behavior affect both throughput and fines generation.
Step 4: Buffering and Pelletizing
Prepared wood is buffered ahead of three MZLH678 pellet mills. Bedding pellets are commonly produced in the 6–8 mm diameter range. Die compression, roller setting and feed moisture are tuned so the pellets survive conveying and delivery but still open readily when used as litter; one fixed compression ratio is not applied to every hardwood blend.
Step 5: Counterflow Cooling
Hot pellets enter a counterflow cooler immediately after pelleting. Mechanical cooling is used because an 8 T/H bedding line cannot rely on spreading hot pellets across the warehouse floor. The cooler stabilizes product temperature, reduces condensation risk in bags and keeps finished-product handling continuous.
Step 6: Screening and Fines Return
Cooled pellets pass through a dedicated screen. Loose fines are separated before packing and clean fines return through a controlled recycle path. Low loose-fines content comes from cooling and screening performance plus careful handling, not from an unsupported universal dust guarantee.
Step 7: Packing and Dispatch
Finished poultry house bedding pellets are packed mainly in 25 kg bags, with larger packaging or bulk supply available for integrated farms that have suitable receiving and storage. Batch identification links the product to the wood-supply lot and production date.
The line contains no routine thermal dryer. Incoming moisture control therefore remains an operating rule throughout the year, especially during Malaysia’s wetter periods and after long storage at supplier sites.
RICHI MACHINERY
Utilities and Consumption
Electrical demand is dominated by three 200 kW pellet mills plus chipping, hammer milling, cooling, aspiration and conveying. The plant does not consume process steam, and there is no dryer heat load in the normal production route.
| Utility | Practical Planning Range | Engineering Basis |
|---|---|---|
| Electricity | Approx. 1.8–2.3 million kWh/year | Depends on chipping share, hardwood type and actual motor loading |
| Electrical service | Approx. 1,000–1,250 kVA | Three pellet mills plus preparation and auxiliaries |
| Process water | Minimal | No washing, steam conditioning or wet processing |
| Domestic / cleaning water | Approx. 300–500 m³/year | Staff welfare and housekeeping |
| Compressed air | Project-specific | Pneumatic gates, bagging and filter cleaning where used |
Dust extraction is one of the main utility-related design considerations. Airflow is calculated from hood geometry, duct losses, pickup velocity and filter area at the chipper, hammer mills, transfers and screening points; the plant does not publish a single oversized airflow number without the duct design that supports it.
Because the process handles dry wood dust, electrical protection, housekeeping, bearing monitoring, spark and metal control, and isolation around dust collectors are part of the operating plan. Local fire and workplace requirements are incorporated during detailed engineering and installation.
RICHI MACHINERY
How RICHI Customized This Line for Hardwood Bedding Pellets
The engineering choices were driven by the end use inside poultry houses, not by fuel-pellet practice. A bedding product must arrive clean, store without condensation, generate limited loose fines during spreading and break down into a workable litter layer after exposure to moisture and bird traffic.
- The raw-material acceptance plan prioritizes traceable pre-consumer solid hardwood and excludes engineered, coated and treated wood.
- The no-dryer process is paired with a strict receiving-moisture limit rather than assuming every furniture residue is dry enough year-round.
- Three MZLH678 pellet mills provide the throughput needed for 15,000 T/A while leaving operating margin for maintenance.
- Die geometry and roller settings are tuned for bedding behavior instead of using a universal fuel-pellet compression ratio.
- A counterflow cooler replaces floor cooling so product flow, bagging and warehouse hygiene remain continuous.
- Screening and controlled fines return improve delivered cleanliness without making unsupported health claims.
Automation is sized for a small industrial team rather than an unrealistic two-person plant. Around 10–12 employees can cover receiving and forklift work, control-room operation, packing, warehouse duties, maintenance, quality checks and administration across the normal one-shift schedule.
Commissioning includes raw-material trials, pellet-mill loading, die/roller adjustment, cooler settings, screen performance and packing checks. Operator training focuses on safe startup and shutdown, magnet and screen inspection, lubrication, die changes, blockage response, dust housekeeping and lockout procedures.
RICHI MACHINERY
Product Specifications (Hardwood Bedding Pellets)
There is no single universal Malaysian standard that makes one fixed set of numbers mandatory for poultry bedding pellets. The commercial specification is therefore built around clean material, moisture control, physical integrity, low loose fines and farm validation rather than an invented certification claim.
| Property | Practical Project Target | Buyer Relevance |
|---|---|---|
| Pellet diameter | 6–8 mm | Easy spreading and handling in poultry houses |
| Pellet length | Approx. 10–25 mm | Avoids excessive long pieces while limiting breakage |
| Finished moisture | Usually 8–12% | Storage stability and litter performance |
| Loose fines | Controlled by cooling and screening | Reduces dust during handling and spreading |
| Durability | Moderate, test-defined | Must survive transport but still open under use |
| Bulk density | Measured by production lot | Warehouse and truck-volume planning |
| Absorbency | Verified by agreed test method | Allows comparison with the farm’s existing bedding |
| Wood cleanliness | Untreated solid hardwood only | Critical for poultry-house suitability |
Numbers such as 250–300% absorbency, less than 0.5% dust or a fixed 92–94% durability are not presented as automatic product guarantees. These values depend on test method, wood species, particle size, pellet density and conditioning. Commercial samples should be tested using the same method that the buyer will use for acceptance.
The product is intended to swell and gradually break down after placement. That behavior is different from a high-density heating pellet, where maximum mechanical durability is often the priority. Bedding trials therefore look at spreading, moisture uptake, caking, litter friability and ease of removal as a combined performance package.
RICHI MACHINERY
Market Outlook for Hardwood Bedding Pellets in Malaysia
Malaysia’s poultry scale gives the project a credible customer base, but the market case does not depend on claims that almost no competitors exist. Official 2024 statistics reported roughly 327.3 million chickens and 1.83 million tonnes of chicken meat production, showing the scale of poultry activity without converting that figure into an unsupported bedding-demand estimate.
Selangor is a useful production location because it sits close to a large industrial base and road network, while Johor and Perak are also major poultry states. The plant can therefore build sales with integrators, contract growers, breeder operations and farm-supply distributors rather than relying on one poultry group.
| Market Issue | Commercial Response |
|---|---|
| Rice husk is inexpensive and familiar | Position pellets where cleanliness, storage density and consistency justify the premium |
| Farm results depend on management | Use controlled farm trials instead of universal ammonia or mortality claims |
| Furniture residues vary by factory | Approve suppliers and segregate material forms |
| Malaysia is humid | Use covered storage, moisture checks and FIFO inventory |
| Large farms need dependable deliveries | Maintain finished-stock buffers and bulk/large-bag options |
The strongest conversion argument is operational consistency: a farm can receive a compact standardized product with documented moisture and low loose fines, while the producer creates value from clean timber residues. Pricing and payback are kept out of the case because raw-material contracts, electricity tariffs, packaging and delivery distances change.
RICHI MACHINERY
Why a Hardwood Bedding Pellet Line Makes Sense in Malaysia
The project works when three conditions are present together: traceable dry hardwood residues, enough poultry customers within economical delivery distance, and a production line configured specifically for bedding rather than fuel. Klang can satisfy that combination because it sits inside Malaysia’s main industrial and logistics corridor.
The no-dryer route also keeps the process compact, but it only remains economical if supplier moisture is controlled. A buyer with wetter sawmill residues would need a different plant architecture that includes drying, additional thermal energy and a larger raw-material buffer.
Equipment can ship from Qingdao to Port Klang and move by road to the Klang/Selangor site. The project schedule is typically about 5–7 months when building adaptation, electrical work and foundations are prepared in parallel with equipment manufacture. RICHI scope covers process engineering, manufacturing, factory inspection, export packing, installation guidance, commissioning and operator training.
For another biomass pellet project focused on animal bedding, the first design inputs should be wood origin, moisture range, percentage of sawdust versus offcuts, contamination risk, target annual output, farm packaging, storage days and buyer testing requirements. Those details determine whether a dryer is needed, how many grinding stages are justified and what pellet-mill capacity provides enough operating margin.
RICHI Machinery can configure hardwood, softwood or other suitable clean biomass bedding lines, but the material approval rules remain product-specific. For poultry applications, the engineering priority is a clean and consistent bedding product that can be produced, cooled, screened, packed and delivered repeatably.
● RICHI MACHINERY
RICHI Service

● Consulting
Customer Consultation
We want to have a deep understanding of your industrial process, to know your exact needs of feed, wood, biomass, fertilizer or other pellet processing.
● Design
biomass Pellet Plant Design
Based on your unique situation and industrial process, we will tailor complete pellet plant you need, and inform you of every additional detail that could facilitate operation, minimize total cost.

● Manufacturing
Equipment Manufacturing
The critical components of the of the complete pellet production line equipment are built in our own workshops in Asia. Additional equipment is manufactured by our worldwide network of reliable partners.

● Testing
Quality Inspection & Testing
Before leaving the factory, all equipment will be inspected by the quality inspection department. We can also provide customers with testing services from a single machine to a complete pellet plant system, and provide you with real actual data for “worry-free use.”

● Delivery
Equipment Delivery
In equipment boxing and packaging, we adopt professional packaging and modular solutions to ensure the safe and non-destructive delivery of pellet plant equipment.

● Installation
Installation & Commissioning
Whether you choose your own subcontractor for the erection phase or you want to install everything together with us, a Richi supervisor will be around to make sure everything is mounted in a safe and thorough way.

● Training
Staff Training
We provide comprehensive training for the technicians of each project. We can also continue to provide support for the technicians during latter project operation.

● After-sales
Project Follow-Up
When everything is up and running our Richiers will help you further whenever needed. We are ready to answer your call 24/7.We’ll also visit you regularly to learn about your needs.

Who we are
RICHI Machinery is one of the world’s leading suppliers of technology and services for the animal feed, aqua feed and pet food industries, also the largest pellet production line manufacturer in China.
Since 1995, RICHI’s vision to build a first-class enterprise, to foster first-class employees, and to make first-class contributions to society has never wavered.
In the past three decades, we have expanded our business to a wide range of areas, including animal feed mill equipment, aqua feed equipment, pet feed equipment, biomass pellet equipment, fertilizer equipment, cat litter equipment, municipal solid waste pellets equipment, etc.

1995
RICHI Established

2000+
Serving More Than 2000 Customers

120+
RICHI Employees

140+
Exported To 140 Countries



