

 0086-138 3838 9622
Wood pellet production line in Bangladesh
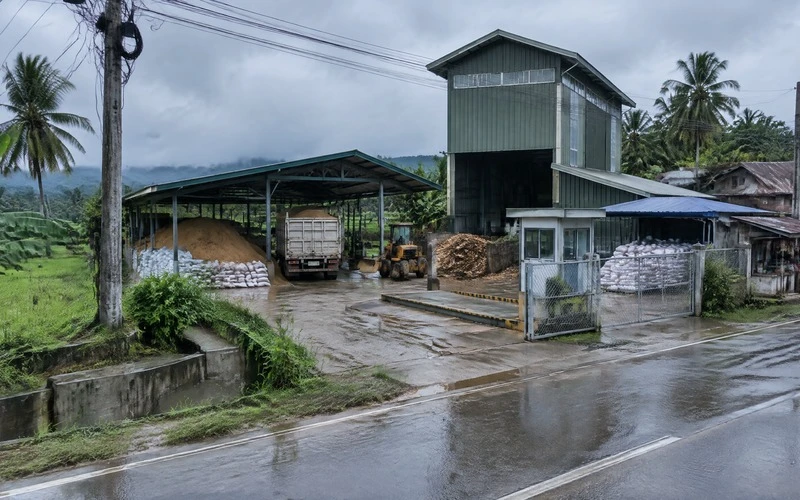
Wet sawdust, rather than a lack of wood, is the starting challenge for this wood pellet production line in Bangladesh. A family-owned timber business in Chittagong wanted to turn residues from its sawmill and furniture workshop into wood fuel pellets. The target was 2–2.5 T/H, but the proposal also had to account for rainy-season moisture, grit in the incoming material and the quantity of sawdust the business could actually supply.

RICHI MACHINERY
A sawmill supply with a seasonal water problem
The customer works with mixed wood, including rubber wood and mango wood, and already has a collection stream from its own processing operations. That gives the project a clear starting supply. It does not make every tonne ready for the press: a wet load contains water, and floor-collected sawdust may also carry sand, stones or metal.
The business wanted a line that its team could operate without an elaborate production organisation. The useful way to simplify it is to keep the material route understandable and the handling manageable. Removing a necessary dryer or relying on hand packing that cannot keep up would only move the problem to another part of the factory.
RICHI’s planning task was to connect three different quantities: wet wood arriving at the site, dry prepared material feeding the press and cooled pellets leaving in bags. Keeping those quantities separate matters here because the stated raw-material moisture can change considerably between dry weather and the rainy season.
Following the first enquiry in July 2023, the customer signed the equipment contract on March 11, 2024. This wood pellet production line in Bangladesh is described here around its material supply and a practical 2–2.5 T/H engineering duty. The FOB equipment contract is not a complete installed-site budget; the drying system, heat source and final supply schedule need to be priced against the agreed wet-feed conditions.
2–2.5 T/H
target finished output
$91,120
FOB equipment contract
Bangladesh
location
Fuel
project type
RICHI MACHINERY
Own sawdust is the base supply rather than a full-shift guarantee
The company’s sawmill is reported to generate 150–200 tonnes of sawdust per month. That can support a useful pellet programme, but it should not be confused with enough material to run a 2–2.5 T/H press continuously. Before buying extra equipment, the owner needs to know how many of those tonnes are suitable wood and how much water they contain.
- Measure usable sawdust separately from the total workshop collection.
- Check monthly wood supply against the intended pellet-running hours.
- Define the buyer’s pellet size, moisture and fuel requirements.
- Add outside sawmills only after checking their wood and contamination levels.
The first email arrived on July 3, 2023, asking about machine capacity, price and a complete wood pellet line. For this customer, the best answer starts with a material sample and a supply record. A larger press does not help if the available sawdust is too wet or the prepared-wood store empties halfway through the shift.
RICHI MACHINERY
Rubber wood and mango wood need consistent preparation
This mixed wood pellet plant in Bangladesh uses rubber wood, mango wood and other sawmill residues. The proportions can vary with timber orders, so the line should be assessed with representative mixed samples. Bark content, particle size and contamination are more useful design information than a fixed species percentage that may not hold through the year.
Check the material before it enters storage
| Receiving item | Practical decision |
|---|---|
| Mixed rubber and mango wood | Sample the actual mixture |
| Sawing residues | Check for grit and metal |
| Furniture residues | Exclude painted wood and unsuitable boards |
| Bark | Control the share and check fuel suitability |
| Moisture | Measure each incoming supply lot |
A shed keeps rain out but does not replace a dryer
The incoming sawdust is described at roughly 25–30% moisture in drier periods and up to 45% in the rainy season. Both conditions need drying before this pellet route. Sheltered storage can prevent further soaking and make handling easier, but it cannot be credited with reaching the required pressing moisture within a fixed number of hours.
- Keep wet incoming wood apart from dried material.
- Use a drained receiving area instead of collecting wood from muddy ground.
- Measure moisture inside the load as well as at its surface.
RICHI MACHINERY
Dry the wood before asking the pellet press to shape it
The wet sawdust pellet line in Bangladesh follows this route: receiving → screening and metal separation → suitable grit removal → size preparation where needed → drying → final grinding if required → prepared-wood holding → pelleting → cooling → screening → packing. The heat supply and dryer are part of making this wet feed usable, not optional accessories to the press.
Remove grit with equipment suited to the material
At the inlet of the wood biomass pellet production line, coarse screening and magnetic separation do different jobs. Magnets can remove suitable ferrous pieces, but they do not remove sand or every type of metal. Grit separation needs equipment selected for the wood’s particle size and moisture; a fan motor rating alone does not establish that separation will work.
| Task | Equipment function | Limit to remember |
|---|---|---|
| Coarse screening | Separate oversize pieces and debris | Select aperture from actual feed |
| Magnetic separation | Remove suitable ferrous contamination | Does not remove sand |
| Grit removal | Separate heavy mineral contamination | Wet fine wood needs appropriate equipment |
Size the dryer by water removal as well as feed weight
The example below starts with clean wet wood after foreign material has been removed. It assumes a target of 2.5 T/H of pellets at 10% moisture, a dryer outlet at 12%, and no external loss of dry wood. Those are engineering calculation assumptions, not measurements from an operating trial. All moisture figures are on a wet basis: water divided by total material weight.
| Illustrative flow | At 30% inlet moisture | At 45% inlet moisture |
|---|---|---|
| Clean wet wood entering | 3.214 T/H | 4.091 T/H |
| Dry wood in every stage | 2.250 T/H | 2.250 T/H |
| Dryer outlet at 12% moisture | 2.557 T/H | 2.557 T/H |
| Water removed in dryer | 0.657 T/H | 1.534 T/H |
| Pellets at 10% moisture | 2.500 T/H | 2.500 T/H |
Cool, grade and pack the actual finished quantity
At the rainy-season example condition, the dryer removes about 1.53 tonnes of water each hour. A further 0.057 T/H leaves between the prepared-wood stage and the finished pellets. That second change is allowed for in the press-and-cooler balance; it does not justify sending 45%-moisture wood directly into the press.
- Cool pellets before closing bags, using the actual intake-air conditions.
- Screen the cooled product and return clean fines to a compatible wood batch.
- Keep cooling, screening and bagging connected during a sustained run.
RICHI MACHINERY
Keep other biomass out of the first wood-fuel recipe
Rice husk, bagasse and jute residues may be available to the business, but none is a direct substitute for clean sawdust. Each changes preparation, wear, ash behaviour or the finished-fuel specification. The first production programme is easier to learn when it starts with a defined wood mixture instead of several untested materials.
| Potential material | What changes |
|---|---|
| Rice husk | Ash, abrasion and buyer acceptance |
| Sugarcane bagasse | Fibre preparation and drying load |
| Jute residues | Cutting, grinding and fuel testing |
| Coconut shell | Hard-material preparation; not automatic charcoal production |
Water-rich aquatic plants are especially unsuitable as an easy rainy-season cost-saving ingredient: they bring another drying load and a new fuel composition. Adding used cooking oil is not a substitute for controlling wood moisture either. The wood-fuel programme should remain a known mixture until any additional material has been separately assessed with the intended buyer.
RICHI MACHINERY
Use one press with enough capacity for the target
An MZLH678 is the appropriate starting size for the requested output: a single press driven by a 200 kW main motor, with a 2.5–3 T/H reference range for wood. To use that capacity, the site has to keep dry, prepared material flowing into it. The dryer and wet-wood handling therefore deserve as much attention as the press.
| Duty | Engineering selection |
|---|---|
| Receiving and cleaning | Screening, magnets and suitable grit separation |
| Drying | Dryer with matched heat source |
| Final size reduction | Wood grinder matched to dry prepared feed |
| wood pellet mill | One MZLH678; 200 kW main motor |
| Cooling and screening | Matched load including internal circulation |
| Packing | Complete bagging and handling route |
The site arrangement should make rainy-weather handling straightforward:
- Set machine levels from the drainage and floor survey, rather than a fixed plinth height.
- Use suitable motor enclosures and keep their cooling paths open.
- Leave access to remove collected grit, inspect screens and replace wear parts.
RICHI MACHINERY
Put the monthly sawdust figure into a production plan
To show what the reported 150–200 tonnes per month could mean, take an illustrative incoming moisture of 30% and finished pellets at 10%. With no dry-wood loss, every tonne received becomes about 0.778 tonnes of pellets. Dirt, unsuitable pieces and actual process losses would reduce that result further.
| Monthly example at 30% moisture | 150 tonnes received | 200 tonnes received |
|---|---|---|
| Dry wood available | 105.0 tonnes | 140.0 tonnes |
| Pellets at 10% moisture | 116.7 tonnes | 155.6 tonnes |
| Productive hours at 2.5 T/H | 46.7 hours | 62.2 hours |
At a net finished rate of 2.5 T/H, that monthly example represents roughly 47–62 productive hours. Start-up, cleaning and maintenance take additional time. The owner can schedule campaigns around that supply or buy more qualified wood; the monthly total alone does not support an assumption of continuous full-shift production.
Outside supply should be agreed by both quantity and material condition. Two trucks of equal weight may bring different amounts of dry wood when one load has absorbed rain. Recording received weight and moisture gives the business a better purchasing basis and helps avoid planning pellet orders around water rather than wood.
RICHI MACHINERY
Make packing the same size job as production
The bagging station needs a repeating cycle: position the bag, weigh the pellets, close it and move it clear before the next one arrives. Manual bag placement can remain part of the arrangement, but weighing, closing, lifting and removal need to work together. A low purchase price for a scale does not establish the output of a complete packing station.
- Keep bag storage and the packing area away from wet incoming material.
- Provide covered storage for finished bags before dispatch.
- Agree how pallets or bag stacks will be removed while packing continues.
| Complete packing duty | At 2 T/H | At 2.5 T/H |
|---|---|---|
| 25 kg bags | 80 bags/hour | 100 bags/hour |
| 50 kg bags | 40 bags/hour | 50 bags/hour |
The daily production target should stop at what the full line can handle. If the bag station falls behind, a buffer buys time but eventually fills. The useful trial is therefore a sustained run through cooling, screening and packing, rather than a short measurement at the press outlet.
RICHI MACHINERY
From first enquiry to the March contract
| Date | Project step |
|---|---|
| July 3, 2023 | First email enquiry |
| September 2023 | Customer representative visited RICHI |
| January 2024 | Purchase financing arranged |
| March 11, 2024 | Equipment contract signed |
The enquiry-to-contract period allowed the customer to examine the equipment and arrange the purchase. It does not establish a later operating rate, a particular fuel test result or the number of staff needed on site. Those figures should come from trials and the final handling arrangement.
What to establish during a representative trial
- Use a representative mixed-wood batch with its incoming moisture recorded.
- Measure dryer inlet, outlet and water-removal duty.
- Weigh accepted cooled pellets and identify returned fines separately.
- Run packing long enough to expose a bag-handling bottleneck.
For a wood pellet production line in Bangladesh using wet sawdust, send RICHI the monthly supply, seasonal moisture range, wood samples and required pellet size. Add the available heat source, electrical supply and preferred bag weight. Those details determine a workable drying duty and a realistic production schedule.
This Chittagong project is most useful to another timber business facing the same question: how much bagged fuel can its own wet residues support? Answer that first, then match the dryer, one suitable press and the packing arrangement to the result.
● RICHI MACHINERY
RICHI Service

● Consulting
Customer Consultation
We want to have a deep understanding of your industrial process, to know your exact needs of feed, wood, biomass, fertilizer or other pellet processing.
● Design
biomass Pellet Plant Design
Based on your unique situation and industrial process, we will tailor complete wood pellet plant you need, and inform you of every additional detail that could facilitate operation, minimize total cost.

● Manufacturing
Equipment Manufacturing
The critical components of the of the complete wood pellet manufacturing equipment are built in our own workshops in Asia. Additional equipment is manufactured by our worldwide network of reliable partners.

● Testing
Quality Inspection & Testing
Before leaving the factory, all equipment will be inspected by the quality inspection department. We can also provide customers with testing services from a single machine to a complete wood pellet processing plant system, and provide you with real actual data for “worry-free use.”

● Delivery
Equipment Delivery
In equipment boxing and packaging, we adopt professional packaging and modular solutions to ensure the safe and non-destructive delivery of wood pellet processing equipment.

● Installation
Installation & Commissioning
Whether you choose your own subcontractor for the erection phase or you want to install everything together with us, a Richi supervisor will be around to make sure everything is mounted in a safe and thorough way.

● Training
Staff Training
We provide comprehensive training for the technicians of each wood pellet production line in Bangladesh project. We can also continue to provide support for the technicians during latter project operation.

● After-sales
Project Follow-Up
When everything is up and running our Richiers will help you further whenever needed. We are ready to answer your call 24/7.We’ll also visit you regularly to learn about your needs.

Who we are
RICHI Machinery is one of the world’s leading suppliers of technology and services for the animal feed, aqua feed and pet food industries, also the largest pellet production line manufacturer in China.
Since 1995, RICHI’s vision to build a first-class enterprise, to foster first-class employees, and to make first-class contributions to society has never wavered.
In the past three decades, we have expanded our business to a wide range of areas, including animal feed mill equipment, aqua feed equipment, pet feed equipment, biomass pellet equipment, fertilizer equipment, cat litter equipment, municipal solid waste pellets equipment, etc.

1995
RICHI Established

2000+
Serving More Than 2000 Customers

120+
RICHI Employees

140+
Exported To 140 Countries



