

 0086-138 3838 9622
3–4 T/H Wood Pellet Processing Plant in Luxembourg
A compact Diekirch project converting dry clean sawdust and wood residues into about 7,800 T/Y of heating pellets with distributed dust collection.
RICHI MACHINERY
Project Overview
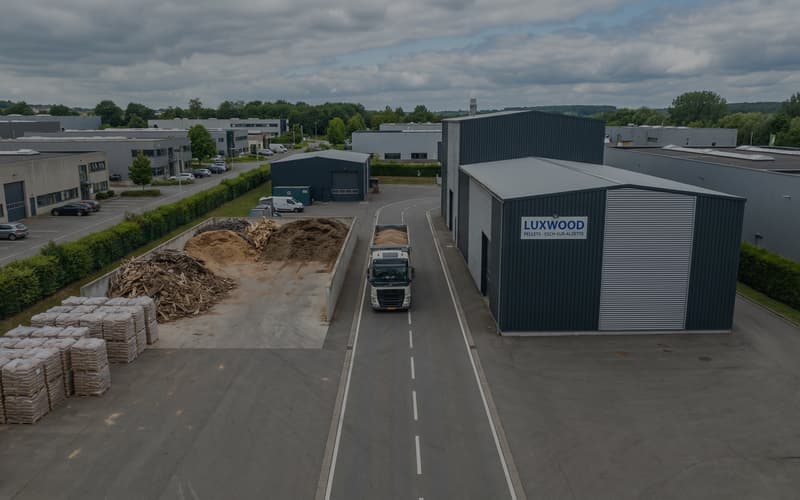
This 3–4 T/H wood pellet processing plant in Luxembourg was commissioned for a customer in the Diekirch area using clean, kiln-dried furniture and sawmill residues from the Luxembourg–Germany–Belgium border region. The site processes about 8,020 T/Y of accepted wood feedstock into approximately 7,800 T/Y of saleable heating pellets. Because the project is small, the commercial advantage does not come from bulk port export. It comes from short collection routes, a compact existing building and road access to several nearby heating-fuel markets. That combination makes the project closer to a regional wood waste pellet plant in Luxembourg than to a large export-oriented forestry complex.
The complete wood pellet plant operates one 8-hour shift per day for about 300 days, giving 2,400 scheduled production hours. At roughly 7,800 T/Y, the required average output is about 3.25 T/H, which fits two MZLH520 biomass pellet mills rated at approximately 1.5–2.0 T/H each. The completed fixed investment remains about US$168,000. The two-press arrangement also gives the operator a practical maintenance option: one press can be stopped for a die or roller check while the second continues limited production. Full annual output still depends on both presses being available for most scheduled production hours.
The distinctive feature is the dust-control architecture. Instead of routing every machine into one oversized central collector, the grinder and pellet section use local or equipment-level collection where practical, while a smaller central baghouse serves transfer points. That distributed arrangement reduces long duct runs and limits the number of process areas affected when one collector is stopped for maintenance. For a 400 m² production workshop, long shared duct runs would also consume valuable overhead clearance and create more balancing points. The distributed concept keeps extraction closer to the dust source, but it requires a disciplined inspection routine so several smaller filters do not become several overlooked maintenance points.
The line has no thermal dryer. That makes feedstock acceptance critical: material is sourced from kiln-dried or indoor-stored wood, and lots above the working moisture range must be held, blended or dried outside the main process before pelleting. Moisture control therefore begins at purchasing rather than after grinding. This is one of the main limits on the biomass pellet plant in Luxembourg: the factory cannot correct a truckload of wet sawdust after it reaches the production floor. Supplier specifications, covered transport and indoor storage therefore act as part of the process system.
3–4 T/H
capacity
$168,000
investment
Luxembourg
location
Biofuel
project type
RICHI MACHINERY
The Customer Prioritized Redundancy Over One Large Dust System
The customer came from a construction background and already controlled an idle 1,200 m² industrial building with grid electricity, municipal water and sewer access. The commercial opportunity came from clean sawdust and wood residues generated by nearby furniture factories and sawmills. Reusing this building kept the civil scope small and allowed more of the available capital to be directed toward pelleting, cooling, electrical interfaces and dust control. It also meant the process had to fit the existing doorways, internal traffic paths and storage divisions instead of starting with a blank greenfield layout.
The design question was whether a wood pellet processing plant in Luxembourg could run with distributed dust collection instead of depending on one central baghouse for every grinder, pellet mill and cooler.
The final answer uses two MZLH520 presses and multiple local collection points. The extra collectors add some equipment and maintenance points, but they shorten ductwork and let one section be isolated without automatically shutting every other machine. For a small plant, that operating resilience was more important to the customer than minimizing the number of filters. The tradeoff is that maintenance staff have several collectors, pressure drops and filter sets to inspect. The design therefore improves isolation, not maintenance-free operation.
RICHI MACHINERY
Dry Feedstock Makes the No-Dryer Route Possible
The customer arranged supply from five furniture factories and three sawmills within roughly 40 km. The sourcing radius is small enough for frequent deliveries, which is useful because the plant does not have a thermal dryer or a large outdoor wet-wood yard. Deliveries are scheduled around storage turnover so the 600 m² raw-material area functions as a working buffer rather than a seasonal stockpile. This also reduces the risk that dry sawdust absorbs moisture during prolonged storage.
| Raw Material | Annual Input (tons) | As-Received Moisture | Cost (USD/ton) | Source |
|---|---|---|---|---|
| Clean wood residue and sawdust | About 8,020 | Normally accepted around 9–12% | Approx. $15 project basis | Furniture factories and sawmills |
The material must be clean and untreated. Painted panels, MDF, plywood, glued composites and preservative-treated wood are excluded from the fuel stream. The preferred feedstock is kiln-dried solid-wood residue or dry sawdust stored indoors. This exclusion is important for both product quality and combustion use: composite boards can introduce adhesives, coatings and mineral contaminants that do not belong in a clean-wood heating pellet. Receiving staff therefore check supplier category as well as moisture and particle form.
Starting with about 8,020 tons of accepted dry wood, the project produces roughly 7,800 tons of saleable pellets after moisture adjustment, screening and normal process loss. This balance is more realistic for a no-dryer plant than assuming only 20 tons disappear from the annual input. Suitable fines are recycled where possible rather than counted immediately as waste. The difference between incoming and saleable tonnage is mainly moisture equalization and unavoidable handling loss, not a large rejected-waste stream. That is why the incoming moisture window has to stay narrow.
RICHI MACHINERY
Two MZLH520 Presses Match the 3.25 T/H Average
| Equipment | Quantity | Power | Function |
|---|---|---|---|
| Multifunctional wood grinder | 1 | 75 kW | Size reduction to a controlled pellet-feed fraction |
| Wood pellet extruder machine | 2 × MZLH520 | 132 kW each | Main pelleting, about 1.5–2.0 T/H per press |
| Low-voltage starters | 2 | — | Pellet mill controls |
| Local cooling / dust unit | 1 | 5.5 kW | Hot-pellet cooling and local dust capture |
| Second cooling / dust unit | 1 | 5.5 kW | Parallel cooling and local collection duty |
| Central baghouse | 1 | 7.5 kW | Transfer-point dust collection |
Equipment price (EXW Qingdao port): approximately US$115,000
The customer sourced the grinder locally in Luxembourg, while the imported package focused on the pelleting, cooling, collection and control equipment that defined the final line performance. Local procurement reduced international freight for a standard size-reduction machine and made routine service easier. The imported pellet section remained the part that needed to match the user’s confirmed MZLH model library and annual dry-ton balance.
Shipping: Two 40-foot containers departed Qingdao and arrived through the Port of Antwerp before road delivery to the Diekirch area. Luxembourg is landlocked, so the final inland leg is part of the project logistics plan. The source project basis includes about US$4,500 sea freight and US$1,200 for onward trucking.
RICHI MACHINERY
The 1,200 m² Building Is Mostly Storage
| Area | Size (m²) | Function |
|---|---|---|
| Production workshop | 400 | Grinding, two MZLH520 presses, cooling and dust collection |
| Raw material storage | 600 | Dry clean wood residue and sawdust |
| Finished goods | 180 | Bagged heating pellets awaiting dispatch |
| Office | 20 | Administration and production records |
RICHI MACHINERY
The Process Stays Short Because Drying Happens Before Delivery
The 3–4 T/H wood pellet production line in Luxembourg has only four core production stages because accepted feedstock is already dry enough for pelleting. There is no chip dryer, furnace or wet-material buffer in the normal route. That saves floor space and thermal energy, but it shifts more responsibility to supplier quality control and covered storage. The plant also avoids the extra fire zone, exhaust stack and fuel-handling system that a dryer would require. Those savings are real only while the incoming moisture stays within the accepted window; if suppliers begin delivering wetter residues, the process boundary has to be reviewed rather than pushing wet material through the same line.
Step 1 – Grinding
Clean wood chips, offcuts and sawdust are reduced to a controlled pellet-feed size. The grinder uses local dust extraction so fines are captured close to the source instead of moving through long shared ductwork.
Step 2 – Pelleting
Ground material is conveyed to two wood pellet makers configured as MZLH520 units. Each contributes about 1.5–2.0 T/H, giving 3–4 T/H of installed capacity. The standard heating product is normally 6–8 mm, with final die specification selected by customer requirement. The presses normally share the production load so neither unit is forced to operate at its upper rating for every batch. Feed rate, die condition and wood density still influence instantaneous output, so the 3–4 T/H range is treated as installed plant capability rather than a guaranteed value for every residue mix.
Step 3 – Cooling
Fresh pellets are cooled before bagging so retained heat and surface moisture do not migrate into storage. The distributed cooling/collection arrangement also keeps dust capture close to the hot-product handling points. Cooling is not used to correct wet raw material; its job is to remove process heat after compression and stabilize the pellet before storage. Finished-product temperature and fines level are checked before bags are stacked in the 180 m² warehouse.
Step 4 – Transfer dust collection
Conveyors and other transfer points connect to the central baghouse. Suitable recovered wood fines return to the process, while filter inspection can be carried out without dismantling the entire production route.
Step 5 – Bagging
Saleable pellets are packed after cooling and screening. Manual or semi-manual packing matches the current 7,800 T/Y scale, while a future automatic bagging upgrade can be added without changing the two-press pelleting section.
RICHI MACHINERY
A Small Domestic Market Connects Directly to Germany and Belgium
Luxembourg is a small heating-pellet market, so the commercial logic of this heating pellet plant in Luxembourg includes cross-border distribution as well as domestic sales. The Diekirch location gives practical road access to customers in neighboring Germany and Belgium. For a plant of roughly 7,800 T/Y, this regional sales model is more credible than depending on deep-sea export. Trucks can serve several customer groups while finished-product storage remains sized as a turnover buffer rather than a large export warehouse.
- Heating demand supports a market for densified wood fuel where boilers and stoves are already compatible
- Renewable-heating support can influence demand, but subsidy rules should be checked at the time of sale
- Short cross-border road distances widen the customer base without requiring seaport export logistics
- Quality-sensitive buyers require documented moisture, ash, durability and source control rather than one generic “premium” claim
The project can serve several sales channels rather than relying on one buyer. For a plant of this size, customer concentration matters: losing one large distributor can change monthly production planning quickly, while several regional buyers allow the factory to schedule smaller but more regular dispatches:
- Local distributors and heating-fuel dealers in Luxembourg
- Nearby German customers reached by road
- Belgian customers within the wider cross-border market
RICHI MACHINERY
Distributed Collection Changes the Maintenance Strategy
The first months of operation confirmed that the dust-control concept has both advantages and responsibilities. Operators can isolate one collector or press for service, but they also have to monitor several filter units, local pickup points and transfer zones. Preventive maintenance is therefore distributed across the plant in the same way as the dust collection itself. Differential pressure, fan condition, filter cleaning and dust discharge all need routine checks. Redundancy only improves uptime when the spare capacity and isolation valves are actually maintained.
What worked well:
- Local collectors allow one production area to be isolated for filter service without automatically shutting every dust pickup point.
- Shorter duct runs simplify inspection and reduce the number of long shared branches that need balancing.
- Two MZLH520 presses provide maintenance flexibility; reduced production can continue on one press during short service work.
Future improvements:
- Automatic bagging would reduce manual handling if retail volumes increase.
- Cooling and insulation should be reviewed before adding more pelleting hours or larger bags.
- Each pellet mill should have its own critical spare-die and roller plan rather than sharing one emergency set.
RICHI MACHINERY
RICHI Scope Centered on Pelleting and Dust-Control Integration
For this 3–4 T/H sawdust pellet plant in Luxembourg, the project scope included the process areas that determine stable operation on dry feedstock. The imported package focused on the pelleting and collection sections, while locally sourced equipment and existing building utilities were integrated into the final layout:
- Process design – Dry-feedstock route with distributed dust collection and no thermal dryer.
- Equipment package – Two wood granulator machines, cooling/collection units and the central transfer-point baghouse.
- Installation supervision – Site support for alignment, conveying interfaces, dust extraction and startup.
- Operator training – Die changes, moisture acceptance, collector maintenance and safe shutdown procedures.
- Spare parts kit – Initial die, bearing, belt and filter-bag items for early operation.
RICHI MACHINERY
A No-Dryer Pellet Plant Needs Tight Feedstock Specifications
If you are evaluating a 3–4 T/H wood pellet plant in Luxembourg or another Western European market, the first question is whether the wood residue is consistently dry and clean enough to bypass thermal drying. That decision controls the entire biomass pellet project cost and layout. A buyer with 15–20% moisture residue needs a different project from this case, even if the desired pellet capacity is identical. Dryer duty, furnace fuel, fire protection, electrical load and floor area would all change.
- Use distributed dust collection when uptime and simple isolation matter. The tradeoff is more individual filters to inspect and maintain.
- Do not oversell a no-dryer route. Lots above the working moisture range need separate drying or holding before they reach the pellet presses.
- Quality claims need test data and certification where applicable. Do not treat one market price or “premium” label as permanent.
- Cross-border sales expand the addressable market. Road access to Germany and Belgium is useful for a small landlocked producer.
The project works because the customer combines dry clean feedstock, a compact 1,200 m² building and a 7,800 T/Y sales target that fits two MZLH520 presses. It should not be copied as a universal small wood pellet plant. Its no-dryer route is viable only because the incoming residue is already dry, clean and locally sourced.
For a similar wood pellet production line, provide annual dry wood tonnage, moisture range, contamination risk, operating hours and target pellet diameter before selecting the final press and dust-control layout. For Luxembourg and neighboring Western European markets, also define the intended heating customer, packaging format and any certification target before the final quality-control plan is issued.
● RICHI MACHINERY
RICHI Service

● Consulting
Customer Consultation
We want to have a deep understanding of your industrial process, to know your exact needs of feed, wood, biomass, fertilizer or other pellet processing.
● Design
biomass Pellet Plant Design
Based on your unique situation and industrial process, we will tailor complete pellet plant you need, and inform you of every additional detail that could facilitate operation, minimize total cost.

● Manufacturing
Equipment Manufacturing
The critical components of the of the complete pellet production line equipment are built in our own workshops in Asia. Additional equipment is manufactured by our worldwide network of reliable partners.

● Testing
Quality Inspection & Testing
Before leaving the factory, all equipment will be inspected by the quality inspection department. We can also provide customers with testing services from a single machine to a complete pellet plant system, and provide you with real actual data for “worry-free use.”

● Delivery
Equipment Delivery
In equipment boxing and packaging, we adopt professional packaging and modular solutions to ensure the safe and non-destructive delivery of pellet plant equipment.

● Installation
Installation & Commissioning
Whether you choose your own subcontractor for the erection phase or you want to install everything together with us, a Richi supervisor will be around to make sure everything is mounted in a safe and thorough way.

● Training
Staff Training
We provide comprehensive training for the technicians of each project. We can also continue to provide support for the technicians during latter project operation.

● After-sales
Project Follow-Up
When everything is up and running our Richiers will help you further whenever needed. We are ready to answer your call 24/7.We’ll also visit you regularly to learn about your needs.

Who we are
RICHI Machinery is one of the world’s leading suppliers of technology and services for the animal feed, aqua feed and pet food industries, also the largest pellet production line manufacturer in China.
Since 1995, RICHI’s vision to build a first-class enterprise, to foster first-class employees, and to make first-class contributions to society has never wavered.
In the past three decades, we have expanded our business to a wide range of areas, including animal feed mill equipment, aqua feed equipment, pet feed equipment, biomass pellet equipment, fertilizer equipment, cat litter equipment, municipal solid waste pellets equipment, etc.

1995
RICHI Established

2000+
Serving More Than 2000 Customers

120+
RICHI Employees

140+
Exported To 140 Countries



