

 0086-138 3838 9622
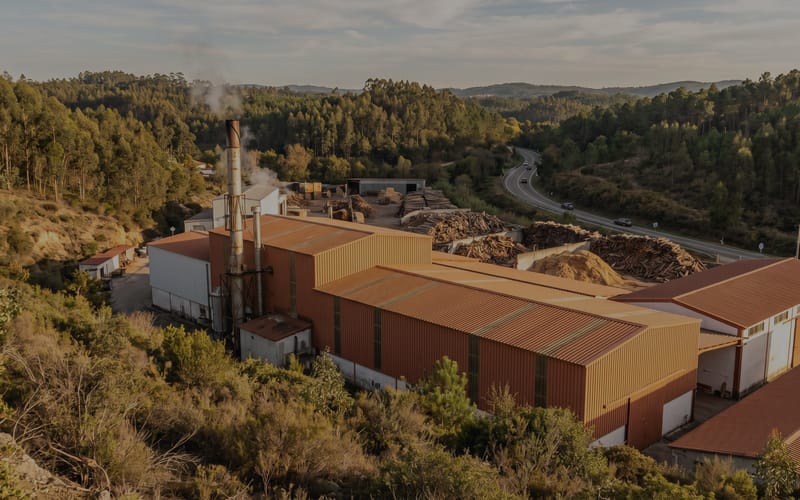
3 T/H Wood Pellet Plant in Portugal
A Leiria-region project converting dry pine and eucalyptus furniture residues into industrial and heating pellets without a thermal dryer.
RICHI MACHINERY
Dry Furniture Residue Sets the Whole Process
This 3 T/H wood pellet plant in Portugal was developed for a timber trader in the Leiria District using clean pine and eucalyptus offcuts, shavings and sawdust from nearby furniture factories. The project does not depend on green sawmill residue: accepted material normally arrives around 8–12% moisture, allowing the line to avoid a thermal dryer. This sourcing pattern also keeps the buyer’s main decision visible: the plant is a dry-residue conversion unit, not a green-wood dryer-and-pellet complex. Incoming moisture, contamination and daily supply volume are checked before production planning, because those three factors decide whether the MZLH678 can hold a stable load.
The wood pellet manufacturing plant operates two 10-hour shifts per day for about 300 days per year, giving roughly 6,000 scheduled hours. With one MZLH678 biomass pellet mill rated at about 2.5–3.0 T/H, the practical annual gross output is around 17,000–18,000 tons rather than treating the full 20,000 T/Y feedstock purchasing plan as finished product. Completed fixed investment is approximately US$145,000. The 6,000-hour calendar gives enough room for maintenance and short stoppages without forcing the press above its rated biomass range. Five operators can cover the compact line only because raw-material receiving and finished-product handling are simple and mobile equipment is sourced locally.
The project’s commercial advantage is not a claim that every waste-wood ton becomes premium pellets. It is the combination of dry indoor feedstock, a short 50 km sourcing radius, simple preprocessing and access to Portuguese heating and industrial pellet buyers. Material acceptance excludes paint, laminates, glue-rich panels and preservative-treated wood.
Because the raw material is already dry, the line concentrates investment on size reduction, pelleting, cooling, screening and dust control. That makes this wood pellet production line in Portugal fundamentally different from a green-sawdust plant where drying energy dominates operating cost.
3 T/H
capacity
$145,000
investment
Portugal
location
Biofuel
project type
RICHI MACHINERY
The Feedstock Specification Removed the Dryer
The customer had spent more than a decade trading timber and knew the Leiria furniture cluster well. The project started when he secured several regular sources of kiln-dried offcuts and dust that were clean enough for fuel-pellet production but too fragmented for higher-value woodworking.
An existing 2,000 m² industrial building already provided concrete floors, grid electricity, water and truck access. That made a compact no-dryer layout more useful than a larger greenfield design.
The first engineering question was whether a 3 T/H sawdust pellet plant in Portugal could remain stable without thermal drying. Moisture tests on repeated samples answered that question: accepted furniture residues were consistently around 8–12%.
The second question was contamination. Only clean solid wood and uncontaminated sawdust are accepted. Painted pieces, MDF, laminated panels and adhesive-rich boards are excluded before they reach the chipper or hammer mill.
The final wood pellet making line therefore uses one MZLH678 press, forced cooling and screening, while supplier moisture control replaces a thermal dryer.
RICHI MACHINERY
20,000 Tons of Dry Residue Are the Purchasing Ceiling
The customer maintains supply agreements with several furniture and wood-processing factories within roughly 50 km of Leiria. The annual purchasing ceiling is about 20,000 tons, but actual production is scheduled against accepted moisture, contamination and finished-pellet orders.
| Raw Material | Annual Input (tons) | As-Received Moisture | Cost (USD/ton) | Source |
|---|---|---|---|---|
| Clean pine/eucalyptus offcuts, shavings and sawdust | Up to 20,000 | 8–12% | Project-specific | Furniture and wood-processing factories |
The incoming material is not accepted simply because it is “waste wood.” Loads are checked for coatings, glue, plastic, metal and moisture. This keeps the industrial wood pellet plant in Portugal tied to a defined clean-wood feedstock rather than a mixed construction-waste stream. The customer also separates suppliers by residue type so one delivery of dusty sanding fines does not change the bulk density of an entire day’s feed. This matters for hopper flow, hammer-mill load and pellet-mill amperage even when the moisture reading looks acceptable.
At the scheduled operating time and the 2.5–3.0 T/H MZLH678 range, annual gross pellet output is planned around 17,000–18,000 tons. The difference between available residue and saleable pellets covers unused purchasing headroom, screening rejects, moisture variation, maintenance and inventory carryover.
RICHI MACHINERY
No Dryer Means Moisture Control Moves to Receiving
A no-dryer route is only economical when moisture is controlled before material enters the plant. This project does not assume that all Portuguese sawdust is dry; it buys specifically from factories processing kiln-dried timber.
The customer therefore spends more effort on supplier qualification and covered storage instead of on thermal drying.
The operating rules are simple:
- Accept only clean residues from factories using kiln-dried solid wood
- Check incoming moisture and segregate material above the plant’s normal 8–12% window
- Keep raw material and finished pellets under cover so Atlantic weather does not add moisture back into the process
The trade-off is that the plant depends on a disciplined dry-feedstock network. If suppliers begin delivering wetter sawdust, the project would need either off-site drying, longer natural conditioning or a future dryer investment. Covered storage is therefore part of the process design. If dry offcuts are left exposed to rain or coastal humidity, the project can lose the very advantage that justified removing the dryer. A no-dryer line needs stricter receiving discipline than a plant with spare thermal capacity.
That is the real value of the no-dryer design: lower process complexity only because feedstock quality is controlled upstream.
RICHI MACHINERY
One MZLH678 Matches the 3 T/H Line
| Equipment | Quantity | Power | Function |
|---|---|---|---|
| Wood chipper machine | 1 | 45 kW | Primary size reduction for large offcuts |
| Wood pellet hammer mill | 1 | 55 kW | Fine grinding to a pellet-ready fraction |
| Wood pellet mills | 1 × MZLH678 | 200 kW | Main pelleting, about 2.5–3.0 T/H |
| Counterflow cooler + screener | 1 set | Project matched | Cool hot pellets and recover fines |
| Forklift | 2 | Diesel | Finished goods handling |
| Pulse dust collection system | 1 | 7.5 kW | Dust control at size reduction and transfer |
Equipment price (EXW Qingdao port): approximately US$85,000
The client bought the wheel loader and forklifts locally in Portugal – cheaper than importing, and local service is available.
Shipping: Four 40-foot containers. Departed Qingdao September 15, 2023. Arrived Port of Leixões, Portugal (near Porto) on October 28, 2023. Sea freight: $6,200 USD. Inland trucking to Leiria (about 150km) added $1,200 USD.
RICHI MACHINERY
A 2,000 m² Building Favors a Horizontal Flow
The client’s building was already standing – a former warehouse on a 2,000m² plot. Total built area 2,000m². We divided it into zones.
| Area | Size (m²) | Function |
|---|---|---|
| Production area | ~1,500 | Crusher, hammer mill, pellet mills |
| Raw material storage | ~300 | Waste wood storage |
| Finished goods storage | ~200 | Bagged pellets for export |
RICHI MACHINERY
Five Stages From Dry Offcut to Finished Pellet
The process stays short because drying is removed, not because cooling or contamination control are optional. Material movement is kept in one direction through coarse preparation, fine grinding, pelleting, cooling and packing. The compact route reduces recirculation and makes it easier for operators to identify where a moisture, particle-size or fines problem entered the product.
Step 1 – Coarse size reduction
Large clean offcuts are chipped to a manageable intermediate size. Fine sawdust and shavings can bypass this stage when they already meet the downstream feed requirement.
Step 2 – Fine grinding
The hammer mill reduces prepared wood to a consistent particle range before the MZLH678. Screen selection is adjusted to material density and pellet quality rather than fixed by one nominal number.
Step 3 – Pelleting
The MZLH678 wood granulator machine produces about 2.5–3.0 T/H depending on feedstock density and die condition. Standard finished diameters are 6 mm and 8 mm.
Motor load, feed rate and die condition are used to control compression. The line does not rely on unsupported “pressure tonnage” claims as a quality specification.
Step 4 – Cooling and screening
Fresh pellets enter forced cooling before fines are screened and returned to the process where suitable. Hot pellets are not sent directly into retail bags or long-term storage.
Step 5 – Packing and dispatch
Cooled pellets can be supplied in retail bags or bulk packaging according to customer orders. Export and domestic sales are planned from confirmed contracts rather than a fixed 70% export assumption.
RICHI MACHINERY
Dust Control Replaces Dryer Exhaust as the Main Air Issue
With no thermal dryer, the main routine air-emission source is dry wood dust from chipping, grinding and transfer. The pulse bag filter is therefore treated as production equipment, not an optional environmental add-on. Pickup hoods are positioned where material is dropped, crushed or transferred, and filter condition is checked against pressure loss rather than visible dust alone. This is particularly important with dry furniture sawdust because the same low moisture that helps pelleting can increase airborne fines during handling.
System design:
- Collection hoods at dust sources
- Pulse-jet cleaning system
- Collection efficiency: 95% at pickup points
Calculated emissions:
- Total dust generated: very low (material is already dry and clean)
- Fugitive dust settles inside the workshop
The chipper and hammer mill are not fully sealable, so some fugitive dust escapes. The client keeps the workshop doors closed and the dust collection system running at all times. Portuguese inspectors have visited twice – no violations.
RICHI MACHINERY
Quality Specification Comes Before Certification Claims
Where the customer targets residential heating or certified export channels, pellet quality has to be tested against the buyer’s required standard. Certification is not assumed merely because the raw material is clean wood. For buyers targeting heating markets, laboratory data and traceable clean-wood sourcing are more useful than marketing language. The plant can adjust die diameter and packing format, but ash, moisture, durability and fines still have to be demonstrated on the actual production batch.
- Pellets diameter 6mm ±1mm
- Length 3.15-40mm
- Bulk density ≥600 kg/m³
- Durability ≥97.5%
- Fines ≤1%
- Moisture ≤10%
- Ash ≤0.7%
- Net calorific value ≥16.5 MJ/kg
The line is capable of producing 6 mm heating pellets and 8 mm industrial pellets, but any ENplus claim must follow completed certification and laboratory verification. The process therefore focuses first on moisture, fines, durability, ash and contamination control.
Commercial pricing is handled through actual contracts. The page does not assume that a certification label automatically doubles pellet value in Germany or France.
RICHI MACHINERY
Leiria Links Furniture Residues With Heating-Fuel Demand
Portugal already has an established wood-pellet industry, so a small producer is entering a real market rather than creating one from scratch. For this project, the stronger local advantage is the Leiria furniture and wood-processing base combined with road access to domestic customers and Atlantic ports. A 3 T/H producer cannot compete with large export mills on scale alone. Its advantage is a short sourcing radius, lower process complexity and the ability to serve regional orders without holding months of finished inventory. Freight, certification and bagging strategy are therefore treated separately for each customer segment.
- A large furniture industry generating abundant waste wood
- Established export routes to Germany, France, and Italy
- Growing domestic demand for biomass heating
Target customers include pellet distributors, commercial heating users and industrial biomass consumers that can accept the project’s verified specification.
- Regional pellet distributors serving central Portugal
- Industrial and commercial heating users requiring bulk deliveries
- Export traders only where certification, specification and freight terms are confirmed
Expansion should follow secured feedstock and sales rather than an assumed jump to 10 T/H. A second line would require fresh checks on raw-material contracts, transformer capacity, cooling, packing and storage.
RICHI MACHINERY
The Operating Lesson Is Supplier Discipline
Early operation highlighted three decisions that matter more than headline pellet price: Maintenance planning also changed after startup. Screen wear, die condition and moisture drift are logged together so operators do not automatically blame the pellet press when throughput falls. This reduces unnecessary die changes and helps the team distinguish a raw-material problem from a mechanical problem.
What proved useful:
- Buying dry furniture residues removes a major thermal stage, but only while supplier moisture remains controlled
- Separating certified-quality ambitions from ordinary industrial sales keeps product claims aligned with actual testing
What needs continuous attention:
- Packaging speed should be increased only when retail orders justify an automatic scale
- Dust pickup points need periodic balancing as screens and production rates change
- Incoming moisture should be measured routinely instead of relying on supplier declarations
RICHI MACHINERY
RICHI Scope Focused on a No-Dryer Layout
For this 3 T/H wood pellet manufacturing plant in Portugal, the supplied scope centered on dry-feedstock handling and a compact production route:
- Process design – Simple, minimal-equipment layout.
- Equipment package – Crusher, hammer mill, pellet mill, dust collection system.
- Installation supervision – Our engineer spent 12 days in Leiria.
- Operator training – Three days on die changes, gap adjustments, and ENplus quality requirements.
- Spare parts kit – Two spare dies, five sets of hammer mill screens, bearings, belts, and filter bags.
- ENplus consulting – We helped the client understand the certification requirements and adjust his process to meet the standards.
RICHI MACHINERY
When a No-Dryer Pellet Plant Makes Sense in Portugal
A no-dryer biomass pellet plant in Portugal should be selected only after repeated moisture tests confirm that the accepted wood stream can remain inside the pelleting window through the year. Buyers should also compare the value of dry residue against the cost of adding thermal drying. If the dry-material premium becomes too high or suppliers cannot hold moisture through winter, the economics can reverse. The correct plant concept therefore depends on a year-round moisture record, not one dry summer sample.
- Pay for feedstock quality when it removes a process stage. Dry clean offcuts can justify a higher delivered cost if they eliminate continuous thermal drying.
- Treat certification as a verified market requirement. Do not design the commercial case around a label that has not yet been obtained.
- Simple does not mean incomplete. Cooling, screening, dust collection and covered storage remain necessary even when the dryer is removed.
- Keep sourcing radius short. The Leiria furniture cluster is valuable because residue, factory and customers can remain within manageable transport distances.
The project works because feedstock condition, machine capacity and operating hours are matched. It is not a generic export-pellet template.
For a similar wood pellet plant construction project in Portugal, provide monthly clean-wood tonnage, moisture range, largest offcut size, working hours and target pellet specification before the MZLH model is finalized.
● RICHI MACHINERY
RICHI Service

● Consulting
Customer Consultation
We want to have a deep understanding of your industrial process, to know your exact needs of feed, wood, biomass, fertilizer or other pellet processing.
● Design
wood Pellet Plant Design
Based on your unique situation and industrial process, we will tailor complete pellet plant you need, and inform you of every additional detail that could facilitate operation, minimize total cost.

● Manufacturing
Equipment Manufacturing
The critical components of the of the complete pellet production line equipment are built in our own workshops in Asia. Additional equipment is manufactured by our worldwide network of reliable partners.

● Testing
Quality Inspection & Testing
Before leaving the factory, all equipment will be inspected by the quality inspection department. We can also provide customers with testing services from a single machine to a complete pellet plant system, and provide you with real actual data for “worry-free use.”

● Delivery
Equipment Delivery
In equipment boxing and packaging, we adopt professional packaging and modular solutions to ensure the safe and non-destructive delivery of pellet plant equipment.

● Installation
Installation & Commissioning
Whether you choose your own subcontractor for the erection phase or you want to install everything together with us, a Richi supervisor will be around to make sure everything is mounted in a safe and thorough way.

● Training
Staff Training
We provide comprehensive training for the technicians of each project. We can also continue to provide support for the technicians during latter project operation.

● After-sales
Project Follow-Up
When everything is up and running our Richiers will help you further whenever needed. We are ready to answer your call 24/7.We’ll also visit you regularly to learn about your needs.

Who we are
RICHI Machinery is one of the world’s leading suppliers of technology and services for the animal feed, aqua feed and pet food industries, also the largest pellet production line manufacturer in China.
Since 1995, RICHI’s vision to build a first-class enterprise, to foster first-class employees, and to make first-class contributions to society has never wavered.
In the past three decades, we have expanded our business to a wide range of areas, including animal feed mill equipment, aqua feed equipment, pet feed equipment, biomass pellet equipment, fertilizer equipment, cat litter equipment, municipal solid waste pellets equipment, etc.

1995
RICHI Established

2000+
Serving More Than 2000 Customers

120+
RICHI Employees

140+
Exported To 140 Countries



