 0086-138 3838 9622
2 T/H straw pellet production line in Mexico
A completed straw-fuel project in Jalisco connects a crop-processing enterprise’s corn and wheat residues with industrial heat users. The nominal 2 T/H line uses one main press, with a receiving yard, a workshop and two product warehouses supporting preparation and dispatch.

RICHI MACHINERY
A completed fuel-pellet operation in Jalisco
This straw pellet production line in Mexico was completed for an agricultural processing company in Jalisco. The owner had several corn and wheat growing bases and an established source of crop residues. Pellet production added a fuel product suited to the company’s own heat requirements and nearby industrial buyers.
The customer’s crop operations could provide more than 20,000 tonnes of straw annually. That resource base was broader than the pellet line’s own programme. Harvested material still needed collection, receiving and preparation before it could become feed for the forming stage.
Corn residues and wheat straw differed in stem form and feeding behaviour. The preparation route took those differences into account, with incoming length, bulk condition and moisture checked before crushing. Only material suitable for the selected direct-processing route was released to the press.
The product was straw-based fuel pellets for compatible boilers and heating equipment. Buyers needed a fuel that matched their feeding and ash-handling arrangements. Pellet dimensions, moisture, fines and mechanical condition were part of that product specification.
RICHI arranged the straw pellet plant around receiving, size reduction, one biomass press and finished-product handling. The nominal forming duty was 2 T/H. Material supply, productive running and the release of accepted pellets governed the annual output of the completed installation.
2 T/H
nominal capacity
US$63,000
project investment
Mexico
location
Fuel pellets
project type
RICHI MACHINERY
Site functions and storage buildings
The project occupied a 7,000 m² site with one workshop, one office and two product warehouses. Incoming straw was received in a separate yard before preparation. The site arrangement connected bulky crop-residue handling with the smaller, denser product moved into storage for dispatch.
| Site item | Project basis | Function |
|---|---|---|
| Whole project site | 7,000 m² | Overall site allocation |
| Processing workshop | 1 building | Prepare and form pellets |
| Office | 1 building | Work and staff facilities |
| Product warehouses | 2 buildings | Hold accepted pellets |
| Straw receiving yard | Separate receiving area | Hold incoming crop residues |
RICHI MACHINERY
A single forming machine with straw preparation
The straw biomass pellet plant used one main pellet press for the nominal 2 T/H duty. A straw crusher prepared the feed, with the conveyor and fan serving the connected material-handling route. Cooling, weighing and packing completed the product-finishing duties before warehouse entry.
| Equipment or duty | Quantity | Production role |
|---|---|---|
| Straw crusher | 1 unit | Prepare the press-feed particles |
| Biomass Pellet Mill | 1 main press | Nominal 2 T/H forming |
| Conveyor | 1 unit | Transfer material |
| Process fan | 1 unit | Support connected airflow |
| Cooling weighing and packing | Finishing duties | Release accepted pellets |
RICHI MACHINERY
Annual straw provision and product programme
The planning account included 15,000 tonnes of straw provision annually and a 10,000-tonne pellet objective. Those quantities sat within the owner’s wider crop-residue resource. Receiving weight, material released to processing and accepted pellet output were kept as separate quantities in the production account.
| Annual planning quantity | Amount | Scope |
|---|---|---|
| Crop-residue resource | More than 20,000 tonnes | Owner’s growing-base resource |
| Straw provision | 15,000 tonnes | Raw-material planning allowance |
| Pellet programme | 10,000 tonnes | Accepted-product design objective |
The raw-material allowance belongs to procurement planning. Material released from storage, its moisture, net rejected material and accepted pellets form the line balance. Internal returns stay within that circuit, while opening and closing stocks complete the annual material account.
RICHI MACHINERY
Production target and calendar capacity
The operating plan covered sixteen hours daily over 300 days, giving 4,800 scheduled hours. A 2 T/H line can produce at most 9,600 tonnes within that time before interruptions. The 10,000-tonne design objective requires 5,000 productive hours, so achieving it requires more coverage than the basic calendar provides.
| Product and operating measure | Project basis |
|---|---|
| Finished product | Straw-based fuel pellets |
| Nominal forming duty | 2 T/H |
| Annual pellet objective | 10,000 tonnes |
| Scheduled calendar | 4,800 hours |
| Ceiling before interruptions | 9,600 tonnes |
| Productive time for annual objective | 5,000 hours |
| Minimum extra productive coverage | 200 hours |
The basic calendar therefore needs additional effective coverage for the full annual design programme. Two hundred extra productive hours is the minimum at the nominal rate; further time is needed for interruptions. The quantity actually produced follows effective running and accepted finished weight.
RICHI MACHINERY
How the straw pellet production line in Mexico handled crop residues
RICHI matched the preparation and handling route to the customer’s straw and site arrangement. Incoming material was received in the yard, reduced to a suitable press-feed form, compacted through a ring die and cooled before packing. Usable returns re-entered the process without being counted again as new supply.
Receiving and temporary straw holding
Straw entered the receiving yard from the customer’s crop operations. The receiving check covered source, moisture, foreign material and the form presented to the crusher. Compacted loads or long stalks needed opening and suitable preparation before they could be fed evenly.
Size reduction for crop residues
The straw crusher shortened and reduced the incoming material to a particle distribution suited to pressing. Its feeding and size-control arrangement followed the crop residue being handled. Oversized or unsuitable pieces were kept out of the press-feed stream until preparation was complete.
Ring-die forming and product condition
Prepared straw entered the straw pellet machine at a controlled rate. The ring die and rollers compressed it into cylindrical pellets, with the feed condition and die arrangement matched to the required fuel. Consistent withdrawal from preparation helped maintain the forming machine’s supply.
Friction within the die and between particles generated heat during compaction. Moisture, particle size and die condition influenced that interaction. The forming behaviour therefore depended on the actual prepared straw, alongside the machine setting and operating load.
Biomass binding during pressing helped the compressed material retain its shape. Product strength still depended on the material and process conditions. The operating checks covered stable feed, the condition of the forming parts and the quality of the pellets leaving the die.
The cutter set product length for the receiving fuel system. Pellets then moved towards finishing, with conveying and natural cooling ahead of bag closing. Their condition at release to packing mattered because warm or unsuitable product could affect the stock placed in the warehouses.
Weighing packing and warehouse entry
Cooled, acceptable pellets were measured, packed and sealed before warehouse entry. Product checks separated usable material needing reprocessing from accepted stock. Handling after grading was kept controlled, with finished bags protected from rewetting before collection.
RICHI MACHINERY
Water staffing and electrical connections
Well supply and personnel demand
Personnel facilities used well water. For ten staff, the daily planning allowance was 600 litres, based on 60 litres for each worker. Applying the 300-day calendar gave an annual staff allowance of 180 m³. This demand belonged to site services alongside the dry processing operation.
The site well was 60 m deep, with a water-supply capacity figure of 20 m³/h. That capacity described the water source, while the personnel allowance described use. They were separate measures, with no continuous withdrawal implied by the hourly capacity.
| Water measure | Figure | Meaning |
|---|---|---|
| Personnel daily allowance | 600 litres | Ten people at 60 litres |
| Personnel annual allowance | 180 m³ | 300 working days |
| Well depth | 60 m | Water-supply infrastructure |
| Supply capacity figure | 20 m³/h | Water-source capacity |
People and operating coverage
The sixteen-hour figure described the line’s operating day. Staff coverage connected receiving, preparation, press supervision, cooling, packing and warehouse handling. Productive running, maintenance and shift handovers all belonged within the operation’s working arrangement.
Local grid connection
Electricity came from the local grid. The press, crusher, conveyor, fan and finishing duties belonged in the complete load assessment, including starting conditions. Actual energy consumption followed their loading and operating time; supply capacity and annual consumption required their own checks.
RICHI MACHINERY
Why the grower added straw-fuel production
Use the crop bases’ residue stream
Several corn and wheat bases provided the owner with a known residue stream. Pellet production gave qualified straw a defined fuel outlet, with collection and preparation linked to the line’s requirements. Procurement followed the material committed to this operation rather than the total resource estimate.
Serve internal and nearby heat users
The fuel programme included the owner’s boiler heat needs and sales to surrounding businesses. Internal withdrawals and external deliveries were separate movements of accepted product. The annual production objective covered both outlets, without assigning an unsupported split between them.
Maintain quality between incoming lots
A consistent fuel product depended on more than the crop name. Changes between incoming lots could alter stem condition, moisture and feeding behaviour. Keeping those characteristics identifiable helped preparation and forming follow the actual straw being processed.
Match fuel to the receiving equipment
Industrial buyers needed the pellets to suit their storage, fuel feeding and combustion equipment. Acceptance covered the declared crop material, product dimensions and handling quality. The specification followed the particular heat application and its ash-handling requirements.
Assess additional North American outlets
The owner also considered the United States and Canada as additional commercial directions. Those opportunities depended on the buyer’s fuel specification, product acceptance and delivery arrangement. They formed part of commercial planning alongside internal and local industrial heat outlets.
For a straw pellet production line in Mexico, share the crop-residue forms, incoming moisture and collection pattern with RICHI. Include the annual product objective, available operating hours and intended boiler fuel specification. These details define the preparation, main press, storage and finishing duties for the operation.
● RICHI MACHINERY
RICHI Service
● Consulting
Customer Consultation
We want to have a deep understanding of your industrial process, to know your exact needs of feed, wood, biomass, fertilizer or other pellet processing.

● Design
straw Pellet Plant Design
Based on your unique situation and industrial process, we will tailor complete pellet plant you need, and inform you of every additional detail that could facilitate operation, minimize total cost.
● Manufacturing
Equipment Manufacturing
The critical components of the of the complete pellet production line equipment are built in our own workshops in Asia. Additional equipment is manufactured by our worldwide network of reliable partners.
● Testing
Quality Inspection & Testing
Before leaving the factory, all equipment will be inspected by the quality inspection department. We can also provide customers with testing services from a single machine to a complete pellet plant system, and provide you with real actual data for “worry-free use.”
● Delivery
Equipment Delivery
In equipment boxing and packaging, we adopt professional packaging and modular solutions to ensure the safe and non-destructive delivery of pellet plant equipment.
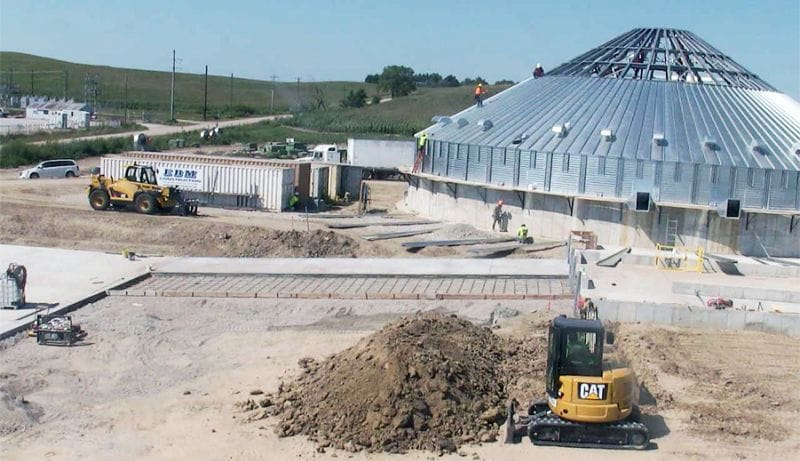
● Installation
Installation & Commissioning
Whether you choose your own subcontractor for the erection phase or you want to install everything together with us, a Richi supervisor will be around to make sure everything is mounted in a safe and thorough way.
● Training
Staff Training
We provide comprehensive training for the technicians of each straw pellet production line in Mexico project. We can also continue to provide support for the technicians during latter project operation.
● After-sales
Project Follow-Up
When everything is up and running our Richiers will help you further whenever needed. We are ready to answer your call 24/7.We’ll also visit you regularly to learn about your needs.
Who we are
RICHI Machinery is one of the world’s leading suppliers of technology and services for the animal feed, aqua feed and pet food industries, also the largest pellet production line manufacturer in China.
Since 1995, RICHI’s vision to build a first-class enterprise, to foster first-class employees, and to make first-class contributions to society has never wavered.
In the past three decades, we have expanded our business to a wide range of areas, including animal feed mill equipment, aqua feed equipment, pet feed equipment, biomass pellet equipment, fertilizer equipment, cat litter equipment, municipal solid waste pellets equipment, etc.

1995
RICHI Established

2000+
Serving More Than 2000 Customers

120+
RICHI Employees

140+
Exported To 140 Countries