

 0086-138 3838 9622
Sawdust to Bedding Pellets Production Line in Mozambique
RICHI MACHINERY
Project Overview
A sawmill operator in Maputo Province developed this Sawdust to Bedding Pellets Production Line in Mozambique to turn clean pine and eucalyptus processing residues into compact animal bedding for dairy farms, cattle units, poultry houses and equestrian customers. The business already generated sawdust and planer shavings, so the project adds value to an existing residue stream instead of depending on purchased logs or mixed waste wood.
The finished-output target is 8,000 T/A. Rather than forcing one MZLH768 pellet mill to operate near its upper limit for only eight hours per day, the factory is planned around one 10-hour production shift for about 300 days per year. This reduces the required average to roughly 2.7 T/H, giving a 3–4 T/H MZLH768 line practical margin for die service, moisture variation, cleaning and softer bedding-pellet settings.
Most feedstock arrives as clean sawdust or shavings and therefore does not need coarse crushing. Dry material is screened, magnetically protected and ground only where particle size requires it. Wetter lots are separated and dried in a small biomass-fired hot-air system before pelletizing. A counterflow cooler and final screener are included because commercial bedding should leave the line cool, stable and with loose fines removed rather than being spread on the warehouse floor.
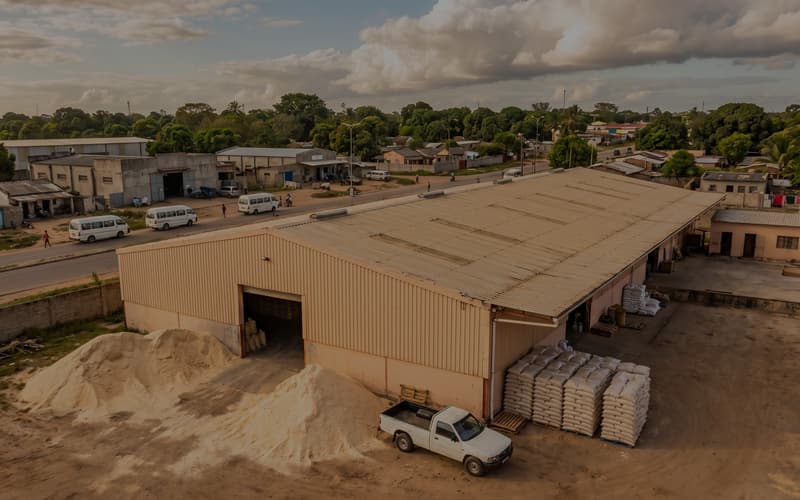
The completed-project investment is USD 238,000, including a USD 158,000 RICHI equipment package. The client uses an existing 2,000 m² warehouse within an approximately 3,500 m² leased industrial site, leaving outdoor space for unloading, truck movement, fire access and utility equipment while keeping raw material, production and finished bedding under cover.
3-4T/H
capacity
$238,000
investment
Mozambique
location
Bedding
project type
RICHI MACHINERY
Why Mozambique?
Mozambique has a substantial livestock base and a clear need for low-cost farm materials that can be produced locally. The country’s 2023/2024 agricultural census estimates about 2.4 million cattle, 4.2 million goats and roughly 16 million local-breed chickens. Those numbers do not translate directly into an 8,000-ton bedding-pellet market, but they show that cattle and poultry applications are large enough to support targeted commercial sales.
For a Maputo Province producer, the immediate opportunity is more specific than the national herd count. Dairy and cattle farms around Maputo and Gaza, poultry operations, horse stables and farm-supply dealers can buy a screened bedding product that takes less storage space than loose shavings and is easier to meter and transport.
| Customer Segment | What They Need | How the Plant Serves Them |
|---|---|---|
| Dairy and cattle farms | Dry resting material with manageable storage volume | 6–8 mm wood bedding pellets supplied in bags or FIBC |
| Poultry houses | Consistent litter with low loose fines | Cooled and screened pellet grade that breaks down after spreading |
| Horse stables | Clean, predictable bedding with good handling | Smaller-bag premium grade made mainly from clean pine residues |
| Farm-supply distributors | Repeatable packaging and batch identification | 25 kg, 50 kg and bulk-bag options |
The project does not rely on fixed claims that pellet bedding is 50–60% cheaper than imports, that no competitor exists, or that every farm will switch from loose sawdust. Raw sawdust and crop residues can remain cheaper where storage and dust are not major concerns. The commercial case is strongest where customers value compact transport, cleaner handling, moisture control and consistent screening.
Maputo Province also has two useful logistics directions. Imported machinery can enter through the Port of Maputo, while regional sales can move west through the EN4/Ressano Garcia corridor toward South Africa. The Ressano Garcia crossing is one of Mozambique’s principal land links with South Africa and is being modernized as a one-stop border facility.
RICHI MACHINERY
Raw Materials: Sawdust from Local Sawmills
The feedstock is clean pre-consumer sawdust and wood shavings from the client’s own sawmill and other approved solid-wood processors. Pine and eucalyptus can both be used, but they are stored by supplier and moisture class so the operator can control drying load and pellet softness rather than treating every delivery as identical.
| Raw Material Stream | Approx. Annual Planning Volume | Typical Receiving Condition | Processing Decision |
|---|---|---|---|
| Client sawmill sawdust / shavings | Approx. 1,000 T/A | Usually 10–16% moisture | Screen, magnet and buffer; grind only if needed |
| Local sawmill residues | Approx. 7,000–7,500 T/A | About 12–20% for covered or air-dried material | Direct route if moisture and size are suitable |
| Seasonal wet sawdust allowance | Approx. 1,000–1,500 T/A within the total supply plan | Can reach 25–35% moisture | Segregate and dry before pelletizing |
| Gross annual intake | Approx. 9,300–9,800 T/A | Supplier-dependent | Supports about 8,000 T/A finished bedding after water removal and process loss |
A gross input above finished output is expected because some delivered sawdust contains more water than the final bedding pellet and a small dry-matter loss occurs through screening, housekeeping and sampling. Clean fines from screening are returned to the process rather than counted as a major waste stream.
- Painted, varnished, preservative-treated or chemically contaminated wood is rejected.
- MDF, particleboard, OSB, laminated boards and adhesive-rich panel waste are excluded from animal-bedding production.
- Magnets and receiving inspection protect the hammer mill and pellet mill from incidental nails, screws and metal fragments.
- Visible mold, plastic, excessive soil and unknown mixed workshop waste are grounds for load rejection or segregation.
- Moisture is checked by lot so already-dry sawdust bypasses the dryer.
The plant therefore buys wood residues as a controlled raw material, not merely as cheap waste. For bedding customers, cleanliness and origin are commercially more important than achieving a fuel-pellet ash value.
RICHI MACHINERY
The Site and Building
The client reuses a 2,000 m² steel-framed warehouse with an 8 m clear height. The covered building does not occupy the entire property: the leased industrial site is approximately 3,500 m², leaving outdoor space for trucks, utilities, fire access and temporary unloading.
| Zone | Approx. Area | Main Function |
|---|---|---|
| Raw-material storage | 600 m² | Dry sawdust, shavings and segregated wetter lots |
| Production area | 900 m² | Screening, grinding, drying interface, MZLH768, cooler and screener |
| Finished-product storage / packing | 400 m² | Bagging, pallet staging and bedding inventory |
| Maintenance / electrical / welfare | 100 m² | Spare parts, controls, staff and routine service |
| Outdoor site area | Approx. 1,500 m² | Truck turning, unloading, fire access and dryer/utility separation |
Material flow runs from receiving toward grinding and moisture control, then to pelletizing, cooling, screening and packing. The route avoids crossing incoming dusty sawdust with finished bagged bedding, and maintenance space is reserved around the hammer mill, ring die, cooler and dust collectors.
The raw-material area uses a dry concrete floor and roof protection because Maputo’s wet season can quickly raise sawdust moisture. Wet deliveries are not mixed into dry stock simply to keep production moving; they are directed to the drying buffer first.
The pellet cooler and finished warehouse are kept away from the dryer hot-air system. This separation reduces fire risk and prevents newly cooled product from taking up moisture or dust from raw-material handling.
RICHI MACHINERY
Equipment Configuration
The line is intentionally simple because the feedstock is already sawdust rather than logs or large chips. The equipment package focuses on screening, final size control, selective drying, one correctly sized biomass pellet mill, mechanical cooling and low-fines finishing.
| Process Section | Main Equipment | Project Configuration |
|---|---|---|
| Receiving / protection | Feed hopper, screen and magnets | Separates foreign material before high-speed equipment |
| Grinding | 1 × wood pellet hammer mill, approx. 55–75 kW class | Used for oversize shavings and inconsistent sawdust; suitable fine material can bypass |
| Moisture control | Small biomass-fired hot-air dryer with bypass | Used only for wet sawdust; dry feedstock bypasses the thermal stage |
| Pelletizing | 1 × MZLH768 biomass pellet mill | 315 kW; 3–4 T/H installed bedding-pellet capacity |
| Cooling | Counterflow cooler | Reduces pellet temperature before screening and storage |
| Screening / recycle | Vibrating pellet screener + fines return | Removes loose fines and recycles clean material |
| Bagging | Semi-automatic weighing / sewing station | 25 kg, 50 kg and FIBC options |
| Dust control | Bag filters at grinding and transfer points | Controls dry wood dust and housekeeping load |
The fixed RICHI equipment package is USD 158,000. Together with building adaptation, electrical work, local installation, dryer hot-air system, foundations, inland transport, commissioning and initial working capital, the completed project investment is USD 238,000.
A 30 kW electric heater is not used as the primary dryer for several tons per hour of wet sawdust. Thermal drying requires far more heat than that rating can provide. The project instead uses a small biomass-fired hot-air system sized for the limited wet fraction, while most dry material bypasses it.
One MZLH768 is enough because the operating schedule is about 10 production hours per day. At 300 days per year, the 8,000-ton target requires about 2.7 T/H average output, leaving reasonable margin inside the machine’s 3–4 T/H biomass range.
RICHI MACHINERY
Process Flow
This biomass pellet plant is adapted to bedding production by controlling moisture, friability, cooling and loose fines rather than maximizing fuel-pellet hardness. The process is short because clean sawdust does not need a log-chipping stage.
Step 1: Receiving and Moisture Classification
Covered trucks deliver sawdust and shavings to the raw-material area. Each lot is checked for moisture, visible contamination and wood origin. Dry material and wetter material are stored separately so the dryer operates only when required.
Step 2: Screening Magnetic Protection and Grinding
Fine, uniform sawdust can move directly through screening and magnetic protection to the process buffer. Fluffy shavings, agglomerated material and oversize particles pass through the hammer mill to create a consistent few-millimeter feed for the ring die.
Screen size is selected from the actual residue rather than fixed at one value. The objective is stable feeder flow and even pellet formation, not unnecessary over-grinding.
Step 3: Drying Wet Lots
Material already within the pelletizing window bypasses the dryer. Wet sawdust is dried to roughly 10–14% moisture using a biomass-fired hot-air system. Dryer temperature, airflow and residence time are adjusted to inlet moisture and particle size rather than one fixed recipe.
Step 4: Pelletizing for Bedding
Prepared sawdust enters one MZLH768 ring-die pellet mill. The main commercial diameter is 6–8 mm. The die, roller gap and feed moisture are tuned during commissioning so pellets remain strong enough for conveyors and bags but break down readily after spreading or wetting.
The line does not use one universal 4:1 compression ratio or one guaranteed operating temperature for every pine/eucalyptus blend. Bedding softness depends on species, fiber, moisture, die geometry and actual farm-use behavior.
Step 5: Counterflow Cooling
Fresh pellets leave the die hot and relatively soft. A counterflow cooler brings them close to ambient temperature before they enter the screener. Floor spreading or several hours of open-bin cooling is avoided because it occupies warehouse space, increases contamination risk and makes cooling inconsistent.
Step 6: Screening and Fines Return
Cooled pellets are screened to remove loose fines and broken pieces. Clean fines return to the process buffer. The aim is a clean packaged bedding product rather than a fixed universal dust percentage that has not been measured by an agreed test method.
Step 7: Packing and Dispatch
Finished bedding is packed in 25 kg or 50 kg bags for dealers and smaller farms, with FIBC available for larger dairy or poultry customers. Batch records identify supplier group, production date and product grade.
RICHI MACHINERY
Utilities and Consumption
Electricity use is dominated by the 315 kW MZLH768 pellet mill, hammer mill, cooler, dust filters and conveying. The dryer uses electrical power for fans and feeding but receives thermal energy from biomass combustion, so annual electricity is much higher than 150,000 kWh yet remains moderate for an 8,000 T/A line.
| Utility | Practical Annual Planning Range | Engineering Basis |
|---|---|---|
| Electricity | Approx. 700,000–900,000 kWh/year | Pellet mill, grinding, cooling, aspiration, conveyors and intermittent dryer fans |
| Electrical service | Approx. 630–800 kVA | Allows the MZLH768 plus preparation and auxiliary loads |
| Biomass dryer fuel | Approx. 250–450 T/A clean wood residue equivalent | Depends on wet-sawdust share and inlet moisture |
| Domestic / cleaning water | Approx. 250–400 m³/year | Staff welfare and dry-cleaning support |
| Process water | Minimal | Dry wood process; no routine water addition required |
| Diesel for handling equipment | Tracked by operating hours | Loader / forklift use depends on delivery format |
The plant runs about 10 production hours per day for roughly 300 days per year. The remaining time is available for die inspection, lubrication, hammer-mill screen service, dust cleaning and bagging-area housekeeping.
The existing Sawdust pellet machine project anchor represents the same MZLH biomass pelletizing platform used here. If backup generation is required, the generator must be sized from the actual critical-load list; a 10 kVA set cannot operate a 315 kW pellet mill.
The operating team is approximately 8–10 people across receiving, production, bagging, warehouse, maintenance and supervision. The simple one-shift schedule keeps staffing lean without pretending the line can run unattended.
RICHI MACHINERY
How RICHI Customized This Line for Sawdust Bedding
The project is designed around a sawmill business that already owns one part of its feedstock stream and wants to manufacture bedding rather than fuel. The engineering choices therefore focus on avoiding unnecessary equipment while still protecting product quality and annual output.
- No log chipper or heavy primary crusher is installed because the routine feedstock is sawdust and shavings.
- The hammer mill is used selectively for oversize shavings and inconsistent residues; suitable fine sawdust can bypass it.
- A bypassable biomass-fired dryer handles the wet fraction instead of imposing thermal cost on every ton of material.
- One MZLH768 provides 3–4 T/H installed capacity, which is sufficient for 8,000 T/A when the plant operates about 10 hours per day.
- Counterflow cooling and screening are retained even in a cost-conscious line because bedding leaves the factory cleaner and more stable than floor-cooled pellets.
- Die and moisture settings are commissioned around controlled friability and farm-use performance rather than copying a hard fuel-pellet recipe.
The equipment package remains compact enough for the existing warehouse while still giving technicians proper access to the ring die, roller assembly, hammer-mill screen, cooler and bag filter. That reduces maintenance downtime and makes spare-parts work possible without dismantling adjacent conveyors.
Training covers moisture checks, raw-material rejection, hammer-mill screens, MZLH die and roller service, cooler adjustment, fines recycle, bagging, dust housekeeping and electrical lockout. Operator capability is confirmed during supervised production rather than by promising full proficiency after a fixed number of days.
The design also leaves room for a second pellet mill or larger bagging system only if residue contracts and bedding sales justify expansion. A capacity increase would require the client to review electrical service, cooling, storage and material supply together.
RICHI MACHINERY
Product Specifications
There is no single universal Mozambique or South African bedding-pellet standard that fixes one density, durability or absorbency number for every cattle, poultry and equestrian customer. The client therefore sells against a practical product specification and buyer testing rather than presenting fuel-pellet limits as mandatory bedding requirements.
| Property | Project Target | Control Logic |
|---|---|---|
| Diameter | 6–8 mm | Suitable for spreading, bagging and breakdown after use |
| Length | Typically 10–25 mm | Controlled to reduce bridging and improve distribution |
| Finished moisture | About 8–12% | Checked before warehouse release |
| Friability / pellet strength | Controlled, not maximized | Must survive handling but soften and break down in bedding use |
| Loose fines | Kept low by cooling and screening | Measured by agreed sampling method when contractually required |
| Absorbency | Verified by agreed test method | Depends on wood species, final moisture and pellet structure |
| Ash / contaminants | Low for clean untreated wood | Used mainly as a cleanliness indicator rather than a fuel target |
| Bulk density | Measured by commercial grade | Used for bag, warehouse and truck planning |
Pine-rich material can produce a softer bedding pellet than some dense hardwood blends, but the project does not promise a fixed 250–300% absorbency or a fixed PDI without laboratory or farm-test data. Eucalyptus content is adjusted where the finished pellet becomes too dense or slow to break down.
For poultry and dairy customers, product performance still depends on ventilation, stocking density, manure load, replacement frequency and floor management. Bedding pellets are a handling and litter-management tool, not a guarantee of animal-health outcomes.
Selling prices are kept out of the technical specification because Mozambican transport, packaging, electricity and raw-material costs change. Commercial quotations should be based on the current bag size, delivery radius and annual contract volume.
RICHI MACHINERY
Market Outlook for Sawdust Bedding Pellets in Mozambique
Mozambique’s 2023/2024 agricultural census provides a stronger market foundation than older estimates: about 2.4 million cattle, 4.2 million goats and roughly 16 million local-breed chickens were recorded nationally. The plant does not need to serve the whole country; an 8,000 T/A line can build its customer base around commercial farms and distributors in southern Mozambique.
Raw sawdust, straw and crop residues will continue to compete on price. Pellet bedding is most attractive where users pay for compact storage, predictable bags, lower loose dust, easier spreading or simplified waste handling. Horse and dairy customers may value those features more than small farms with abundant loose bedding.
| Commercial Challenge | Project Response |
|---|---|
| Wet-season sawdust moisture | Supplier segregation plus bypassable drying |
| Variable wood quality | Approved untreated-solid-wood suppliers and receiving inspection |
| Farmers unfamiliar with pellet bedding | Trial deliveries and on-farm performance checks |
| Power interruptions | Safe shutdown plan and correctly sized backup for defined loads |
| Domestic market still developing | Serve cattle, poultry, equestrian and dealer channels rather than one niche |
| South Africa export logistics | Use the EN4/Ressano Garcia corridor and quote delivered cost by customer |
Regional export is possible because Maputo Province is directly connected with South Africa through Ressano Garcia. In August 2026 Mozambique began construction of a one-stop border facility there to improve freight efficiency on this strategic corridor. That supports logistics potential, but export margins still depend on customs, road freight, buyer specification and exchange rates.
The page does not claim that the client is Mozambique’s only bedding-pellet producer, that the market is already a fixed size, or that payback will occur in fourteen months. Those conclusions require current sales contracts and operating records.
Future expansion should follow repeat demand. If the client adds a second MZLH line, raw-material contracts, transformer capacity, cooler duty, warehouse space and bagging throughput must all be reviewed together.
RICHI MACHINERY
Why a Sawdust Bedding Pellet Line Makes Sense in Mozambique
This project makes sense because the customer starts with an existing sawmill, an existing warehouse and a local residue stream. The factory is therefore not paying to create a new feedstock supply chain from standing timber; it is converting a by-product that already needs handling into a more transportable bedding product.
The 3–4 T/H line is deliberately matched to 8,000 T/A through a roughly 10-hour production day. That operating plan gives one MZLH768 enough margin for normal maintenance while keeping the plant compact and avoiding the capital cost of duplicate pellet mills before the market is established.
Equipment can ship from Qingdao to the Port of Maputo, whose container terminal operates around the clock and has dedicated container-handling infrastructure, followed by a relatively short road leg to the Maputo Province site. This route is more direct than importing through a distant regional port for a plant located near Mozambique’s capital corridor.
Finished bedding can move by road across southern Mozambique or west toward South Africa via Ressano Garcia. Export customers should receive a defined product specification and transport quotation rather than a generic claim that Mozambican pellets are always cheaper than South African supply.
RICHI scope covers process engineering, equipment manufacture, factory inspection, export packing, control preparation, installation guidance, commissioning and operator training. A practical implementation period for an existing-building project of this scale is about 4–6 months when electrical work and building adaptation proceed in parallel with equipment manufacture.
For another sawdust bedding project, the first design inputs should be monthly residue volume, wood species, untreated-wood verification, moisture by season, oversize fraction, target bag size, customer type, operating hours, power capacity and desired expansion plan. Those details determine whether a line needs drying, how much grinding is justified and which MZLH model fits the annual target.
● RICHI MACHINERY
RICHI Service

● Consulting
Customer Consultation
We want to have a deep understanding of your industrial process, to know your exact needs of feed, wood, biomass, fertilizer or other pellet processing.
● Design
biomass Pellet Plant Design
Based on your unique situation and industrial process, we will tailor complete pellet plant you need, and inform you of every additional detail that could facilitate operation, minimize total cost.

● Manufacturing
Equipment Manufacturing
The critical components of the of the complete pellet production line equipment are built in our own workshops in Asia. Additional equipment is manufactured by our worldwide network of reliable partners.

● Testing
Quality Inspection & Testing
Before leaving the factory, all equipment will be inspected by the quality inspection department. We can also provide customers with testing services from a single machine to a complete pellet plant system, and provide you with real actual data for “worry-free use.”

● Delivery
Equipment Delivery
In equipment boxing and packaging, we adopt professional packaging and modular solutions to ensure the safe and non-destructive delivery of pellet plant equipment.

● Installation
Installation & Commissioning
Whether you choose your own subcontractor for the erection phase or you want to install everything together with us, a Richi supervisor will be around to make sure everything is mounted in a safe and thorough way.

● Training
Staff Training
We provide comprehensive training for the technicians of each project. We can also continue to provide support for the technicians during latter project operation.

● After-sales
Project Follow-Up
When everything is up and running our Richiers will help you further whenever needed. We are ready to answer your call 24/7.We’ll also visit you regularly to learn about your needs.

Who we are
RICHI Machinery is one of the world’s leading suppliers of technology and services for the animal feed, aqua feed and pet food industries, also the largest pellet production line manufacturer in China.
Since 1995, RICHI’s vision to build a first-class enterprise, to foster first-class employees, and to make first-class contributions to society has never wavered.
In the past three decades, we have expanded our business to a wide range of areas, including animal feed mill equipment, aqua feed equipment, pet feed equipment, biomass pellet equipment, fertilizer equipment, cat litter equipment, municipal solid waste pellets equipment, etc.

1995
RICHI Established

2000+
Serving More Than 2000 Customers

120+
RICHI Employees

140+
Exported To 140 Countries



