 0086-138 3838 9622
Tofu Cat Litter Manufacturing Plant in Vietnam
RICHI MACHINERY
Local Okara Meets a Retail Litter Business
A distributor with three years of cat litter sales experience established this tofu cat litter manufacturing plant in Vietnam to supply its own plant-based product. The Bình Dương workshop combines soybean residue, corn starch and a binding system through mixing, cold forming, drying, cooling and screening. The equipment fits a low building and supports retail packing for the customer’s distribution network.
The forming section handles a wet-material duty of up to 5 T/H. Drying removes water before the product reaches packing, so finished-litter weight depends on the formula and incoming moisture. The customer produces standard and finer granules using separate die and cutting settings.
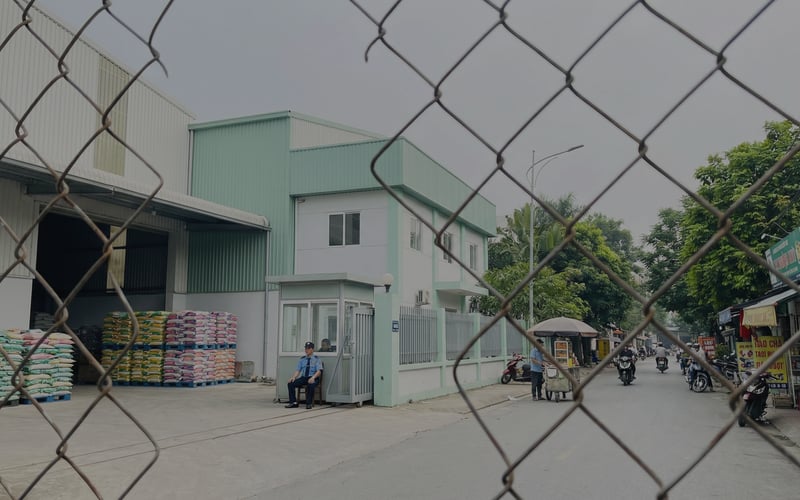
The single-storey workshop has approximately 5 m clearance. Low platforms and conveyors keep the material route within that height, with part of the drying section sheltered under a canopy. The arrangement provides floor-level access for cleaning and servicing wet-material equipment.
The customer’s product priorities are firm clumps, low loose dust and sealed bags that protect litter during distribution. RICHI connected those requirements with controlled ingredient feeding, product sizing and downstream handling inside the 2,000 m² site.
5T/H
wet-forming capacity
$95,000
equipment package
Vietnam
location
Cat Litter
project type
RICHI MACHINERY
A Low Workshop Shapes the Equipment Arrangement
The leased Bình Dương building places manufacturing close to the customer’s southern Vietnam distribution network. Converting an existing garment workshop gave the business covered floor space while the processing layout provided separate routes for wet ingredients, dry powders and finished bags.
The steel building offers approximately 5 m clearance below the beams. Low-level transfers keep the mixer and forming machine accessible, while the drying and cooling route uses more floor length than a tall gravity-fed arrangement.
The single forming route serves both product sizes. Die changes, cleaning access and dryer residence time therefore influence changeover planning as much as the hourly forming rate.
The arrangement uses conveyors where gravity transfer cannot fit.
The buyer had imported cat litter for three years and understood retail packing and distribution. Manufacturing adds material acceptance, formulation control, hygienic handling and finished-product testing to that commercial experience.
Local production gives the distributor control over granule dimensions, packing format and delivery batches. The commercial value lies in matching manufacturing to the retail specification: a durable bag of stable litter supports repeat purchases better than a low wet-material cost alone.
RICHI’s process arrangement connects ingredient moisture, mixing consistency and the amount of water removed after forming. That relationship determines how the product behaves during drying and in the finished bag.
The available height constrains bins and transfer points.
The covered external drying area provides space for the longer thermal section. Weather protection and accessible ducting support cleaning and service, while the wet receiving area remains separated from finished-product storage.
RICHI MACHINERY
Fresh Soybean Residue From a Regional Supplier
The plant links a local tofu-processing residue stream with dry starch and binder supplies. Delivery frequency matters because fresh okara has a short handling window and takes up more transport weight than its dry solids alone.
The okara supply arrangement draws on a tofu processor in the Ho Chi Minh City area. An annual purchasing allowance of 7,500 tonnes corresponds to 25 tonnes per working day over 300 days. Short receiving residence and covered unloading help keep fresh material moving into production.
Fifteen staff cover a ten-hour daily schedule over 300 working days. Duties span receiving, batching, forming, drying, packing, quality checks and maintenance. The wet-material route makes cleaning and stock rotation part of the daily workload.
Pet retailers and distributors are the principal target channels. Their purchasing requirements shape bag size, label information and the balance between standard and finer litter products.
Sealed packing and consistent batch quality support regional distribution. For customers serving additional markets, RICHI can adapt bagging and handling to the required retail format and delivery conditions.
RICHI MACHINERY
Two Granule Sizes for Different Product Positions
The plant produces unscented clumping litter in standard and finer grades. Granule geometry, dust separation and moisture control are managed together so that the product remains stable during packing, transport and use.
| Product | Product positioning | Pellet Size | Key Feature |
|---|---|---|---|
| Tofu cat litter (standard) | Standard retail grade | 3–5 mm | Firm granules for routine clumping litter |
| Tofu cat litter (premium) | Finer retail grade | 2–4 mm | Extra fine, lower dust |
Standard 3–5 mm and finer 2–4 mm granules use different forming and cutting settings. Screening removes loose fines after drying and cooling. Product checks follow the bag through handling, because granules that break in transport can raise dust even when the line discharge looks clean.
RICHI MACHINERY
Separate Wet Ingredients From Dry Powders
Fresh okara enters a short-residence receiving area, while starch and additives remain protected in dry storage. The plant based cat litter production line in Vietnam brings these streams together at batching, keeping wet handling away from packaged ingredients until mixing.
- Okara: 7,500 tonnes/year wet cake at 65–70% moisture, with rapid covered receiving and processing. Spoiled or fermented loads should be rejected rather than treated as normal feed.
- Corn starch: 7,380 tonnes/year purchasing allowance, with measured moisture and a supplier specification.
- Guar gum: a 90-tonne annual purchasing allowance, with small additions controlled at batching.
- Colour ingredient: a 30-tonne annual purchasing allowance, used according to the selected product formula.
The schedule distinguishes wet raw material from packaged supplies:
| Raw Material | Annual purchasing allowance | Form | Source |
|---|---|---|---|
| Okara (soybean residue) | 7,500 | Wet cake; 65–70% received moisture | Tofu factory, HCMC |
| Corn starch | 7,380 | Powder (bagged, 25 kg) | Đồng Nai province |
| Guar gum | 90 | Powder (bagged, 25 kg) | Imported from India |
| Green color additive | 30 | Powder (bagged) | Local supplier |
| Printed packing material | Quantity depends on bag size and actual output | Printed film rolls | Local printer, Bình Dương |
Finished litter is stored in sealed bags on pallets. Stock rotation follows the actual sales programme, with space left for handling and dispatch. Separating this area from fresh okara receiving protects bags from wet traffic and simplifies housekeeping.
RICHI MACHINERY
A Forming Package Connected to Drying and Packing
The cat litter making machine package cost US$95,000. The equipment arrangement links ingredient feeding, mixing, cold forming and finished-product handling. Local building work, transport and electrical installation formed separate parts of the customer’s project expenditure.
| Section | Equipment | Quantity |
| Raw material handling | Feed hopper with grate | 1 unit |
| Pulse dust filter | 7 units | |
| Bucket elevator | 2 units | |
| Mixing | Mixing bin (storage) | 1 unit |
| Pneumatic gate valve | 1 unit | |
| Ribbon mixer (1,500L) | 1 unit | |
| Buffer bin | 1 unit | |
| Screw conveyor | 1 unit | |
| Extrusion | Cold-forming screw extruder – wet-material duty up to 5 T/H | 1 unit |
| Drying | Product drying section | 1 unit |
| Drag chain conveyor | 3 units | |
| Cooling | Counterflow cooler (with fan) | 1 unit |
| Dust collection | Cyclone separator | 1 unit |
| Airlock | 1 unit | |
| Screening | Horizontal reciprocating screener | 1 unit |
| Auxiliary | Electrical control panel | 3 panels |
| Air compressor (screw type) | 1 unit | |
| Packaging | Automatic bagging scale (5–10 kg) | 3 units |
| Arrangement | Integrated handling and processing sections |
The cat litter pellet machine uses cold screw forming to shape the mixed material. Binder distribution and consistent moisture keep feeding smooth, while accessible contact surfaces support cleaning between product batches. Die and cutting adjustments provide the standard and finer granule formats.
Drying is the main thermal duty in this wet-ingredient route. RICHI sizes comparable systems from the water entering with the ingredients and the moisture required in the packed product. This connects the dryer, airflow and heat supply with the actual recipe instead of treating heater motor power as the whole energy requirement.
RICHI MACHINERY
Working Areas Within a 2,000 m² Site
Five-metre headroom keeps the layout low and accessible. The working areas provide room for mixer cleaning, die access, dryer maintenance and packing movements. Conveyors carry material between sections where a taller gravity arrangement would use too much height.
Low-level conveyors are part of the route, with each transfer checked for dust and wet-material build-up.
Raw storage
300 m² separates fresh okara receiving from dry starch and additives. The starch allowance of 7,380 tonnes per year averages 24.6 tonnes per working day, making frequent replenishment important to usable stock space.
Mixing
200 m² accommodates the 1,500 L ribbon mixer, batching access and discharge transfer. Consistent filling, mixing and emptying cycles keep the forming machine supplied.
Forming
150 m², with a clean die-change and maintenance envelope around the cold-forming machine.
Drying
a 400 m² working allocation accommodates the thermal section, partly beneath a canopy. The route preserves access for duct inspection, cleaning and product transfer.
Cooling and screening
250 m², with enough clearance for airflow equipment, screen removal and cleaning.
Packing and finished stock
500 m² accommodates bag filling, sealing, pallet handling and dispatch stock.
Office and staff facilities
200 m² supports administration and the production team. The seven working allocations together account for the 2,000 m² site arrangement.
RICHI MACHINERY
Control Water Addition Before Cold Forming
The tofu litter production line in Vietnam requires batch control from received okara to finished bag. Wet mass, dry solids and evaporation are tracked separately.
Ingredient Receiving
Fresh okara is weighed and checked for moisture and condition before processing. Dry powders enter through a protected hopper with extraction. Covered storage and short wet-material residence help keep batches consistent.
Weighing and Mixing
Starch, okara and binder enter the mixer in controlled proportions. Water addition follows the moisture already present in the ingredients. Even binder distribution supports stable forming and clump performance in the finished litter.
A metered water addition gives the operator a repeatable way to adjust a batch. The complete mixing cycle includes filling and discharge, keeping the transfer to the forming machine coordinated with the next batch.
Cold Forming
The screw-forming section handles up to 5 T/H of wet mixture. Die geometry sets granule diameter, while feed consistency and screw loading influence the smoothness of the formed strands.
The cutter controls strand length separately from diameter. A consistent cut helps product move evenly through drying and screening and gives the retail bag a more uniform appearance.
Product Drying
Controlled hot airflow removes moisture from the formed granules. Air distribution and residence time are balanced across the bed so that the surface and centre dry evenly. Product temperature and moisture guide the operating settings.
Moisture checks continue after drying and cooling. Sampling the full granule helps the operator detect a wetter core before the product enters sealed packaging. Stable packed moisture supports storage and keeps the litter free-flowing.
Excessively rapid surface drying can cause brittle granules or cracks. The drying profile therefore follows the formula and granule geometry, with product strength checked alongside moisture.
Secondary Cooling
Airflow lowers the temperature of dried litter before screening and bagging. Bed depth and local humidity influence residence time, so the operator follows the product leaving the cooler.
Cooling protects the packed product from retained heat and condensation. The final bagging decision combines temperature, moisture and handling condition.
Size Classification
The reciprocating screen separates agglomerates, saleable granules and loose fines. The selected mesh works with the product’s elongated shape and the standard or finer retail grade.
- Oversize and agglomerates: inspect before controlled reprocessing.
- Accepted fraction: test geometry, dust, strength and clumping before packing.
- Fines: return only within a validated formulation limit.
The finer product uses its own forming and screening settings. Keeping those settings together with the batch recipe makes changeovers more repeatable.
Retail Packing
Three bagging stations serve the 5–10 kg packing range. Filling, sealing and pallet handling are balanced with dried output, while weight checks and seal inspection protect the product through distribution.
Clean Rework
Compatible fines return in controlled quantities. The operator keeps batches traceable and excludes spoiled or contaminated wet material from the product route.
RICHI MACHINERY
Water and Energy Follow the Wet-Material Route
The utility arrangement serves mixing, thermal drying, motors and staff facilities. Keeping these duties distinct makes it easier to control daily consumption and understand where a recipe change affects the operating cost.
| Utility | Point of use | Control method | Operating purpose |
|---|---|---|---|
| Water (mixing) | Batch mixer | Metered addition by recipe | Adjust forming moisture |
| Water (staff) | Washing and staff facilities | Separate domestic supply | Hygiene and daily site use |
| Electricity | Drives, fans and control panels | Section-level operating management | Keep electrical demand separate from dryer heat duty |
Drying exhaust carries moisture removed from the litter, while powder-handling extraction collects entrained solids. Wet receiving and cleaning have their own drainage route. Keeping these flows separate helps the team manage housekeeping without bringing wet traffic into the packing area.
RICHI MACHINERY
Keep Fresh Material and Dust Under Control
Fresh organic material, dry powders and warm exhaust require different housekeeping measures. The plant separates these functions so that wet residues are cleared promptly and dry dust does not accumulate at transfer points.
The control arrangement includes:
- Pulse filters at identified powder transfer and packing points, with suitable cleaning access.
- Dryer exhaust separation sized for moisture and entrained solids; a cyclone alone may not control fine particles.
- Enclosed transfers where appropriate, with cleanout access and guarded drives.
Accessible filters and transfer points make routine cleaning practical. The operating team checks dust build-up, collection performance and wet-material residence as part of daily production management.
RICHI MACHINERY
Commissioning Focused on Product Consistency
Commissioning connected wet-material handling with stable forming, drying and packing. The work focused on batch consistency and product condition through the complete route.
Wet-contact surfaces
accessible equipment supports cleaning and reduces retained material between batches. The team inspects the screw, seals and discharge points during routine maintenance.
Electrical operation
motors and fans start in sequence, with protective devices and controls serving each process section.
Packing accuracy
test weights and regular fill checks keep the retail pack within its specified weight range.
Cooling maintenance
cleanout access allows the team to remove accumulated fines and maintain clear airflow paths.
Operators follow material moisture, batch weight, product temperature and bag quality together. This makes troubleshooting specific to the stage affecting the product rather than relying on the final appearance alone.
RICHI MACHINERY
Fifteen Staff Across Wet Handling and Retail Packing
The fifteen-person team covers receiving, mixing, forming, drying, quality, packing and maintenance. Training addresses the duties most important to this formula:
- Mixing: representative moisture checks and calculated water dosing.
- Forming: feed consistency, torque monitoring and safe die changes.
- Drying: airflow, temperature profile, moisture sampling and cleanout.
- Screening: mesh condition, geometry checks and controlled rework.
- Maintenance: isolation, lubrication, filter checks and weighing calibration.
Repeated checks at the mixer, dryer and packing station give the team a consistent routine across shifts and product changes.
RICHI MACHINERY
Equipment and Local Project Expenditure
| Item | Cost (USD) | Notes |
|---|---|---|
| Equipment package | $95,000 | Process machinery |
| Sea freight + insurance | $12,500 | Qingdao to Cát Lái |
| Taxes and duty budget | $14,250 | Import-related allowance |
| Local transport (Cát Lái to Bình Dương) | $1,500 | Truck rental |
| First-year building lease | $36,000 | US$3,000 per month |
| Building modifications (wall cutout, canopy, flooring) | $25,000 | Local contractor |
| Electrical installation | $18,000 | Panels, wiring, lighting, breaker |
| Installation supervision (our team, 10 days) | $15,000 | Flights, hotel, per diem |
| Operating training | Included in supervision | Operator instruction and handover |
| Raw materials (first batch: 100 tons okara, 100 tons starch) | $22,000 | Startup stock |
| Packaging (first 100,000 bags) | $8,000 | Printed with their logo |
| Contingency provision | Held separately | Reserve for additional local works |
| Equipment and delivery subtotal | US$109,000 | Machinery, sea freight and inland delivery |
Machinery, sea freight and inland delivery total US$109,000. Building modifications, electrical installation and supervision add US$58,000, giving US$167,000 across these fixed-work categories before tax treatment. The first-year lease, raw-material stock and packaging stock remain separate operating-funding items. This separation helps a buyer compare the manufacturing installation with the cash needed to launch retail supply.
RICHI MACHINERY
Product Development Starts With Repeatable Batches
The customer can develop additional litter grades around the established material route. The most useful changes focus on:
- Granule strength suited to the handling and packing format.
- Ingredient moisture and dry-solids proportions that keep forming consistent.
- Foreign-object control and clean wet-material handling.
- Dust separation at screening and retail packing.
For a tofu cat litter production line in Vietnam, an additional product grade should fit the mixer, forming equipment and dryer together. RICHI can compare die size, cut length and drying settings using the customer’s intended formula and sample bags.
RICHI MACHINERY
Manufacturing Around the Distributor’s Retail Specification
The Bình Dương customer combined manufacturing with its experience in selling cat litter. Local production allows packing batches and product dimensions to follow the distribution programme more closely.
Fresh okara delivery is managed by moisture and dry-solids contribution, making the recipe repeatable when the wet ingredient changes.
The fifteen-person operating team supports ingredient handling, product quality and retail pack preparation within the same site.
Clump strength, dust level, moisture stability and bag performance connect production quality with repeat retail demand.
For additional distribution markets, pack size, language and disposal guidance can be adapted to the destination while retaining the same controlled production route.
RICHI MACHINERY
Send a Dry-Solids Formula With the Inquiry
For a tofu cat litter manufacturing plant in Vietnam, begin with the formula and fresh ingredient condition.
Provide wet and dry material data together.
List okara moisture, daily delivery quantity, starch moisture, gum inclusion and target final moisture. Specify whether the hourly target means wet forming or finished dry product.
Include product diameter, cut length, dust and clumping test requirements. These define die, drying, screening and packing duties.
A reusable equipment proposal needs the building drawing, power rating, available heat source, permitted outdoor space and wastewater route. Support and spare-parts arrangements should be defined in the proposal.
RICHI can compare dewatering, heat-source and drying options for the actual formula, then provide a layout and scope separating machinery, installation and startup funding.
● RICHI MACHINERY
RICHI Service
● Consulting
Customer Consultation
We want to have a deep understanding of your industrial process, to know your exact needs of feed, wood, biomass, fertilizer or other pellet processing.

● Design
cat litter Pellet Plant Design
Based on your unique situation and industrial process, we will tailor complete pellet plant you need, and inform you of every additional detail that could facilitate operation, minimize total cost.
● Manufacturing
Equipment Manufacturing
The critical components of the of the complete pellet production line equipment are built in our own workshops in Asia. Additional equipment is manufactured by our worldwide network of reliable partners.
● Testing
Quality Inspection & Testing
Before leaving the factory, all equipment will be inspected by the quality inspection department. We can also provide customers with testing services from a single machine to a complete pellet plant system, and provide you with real actual data for “worry-free use.”
● Delivery
Equipment Delivery
In equipment boxing and packaging, we adopt professional packaging and modular solutions to ensure the safe and non-destructive delivery of pellet plant equipment.
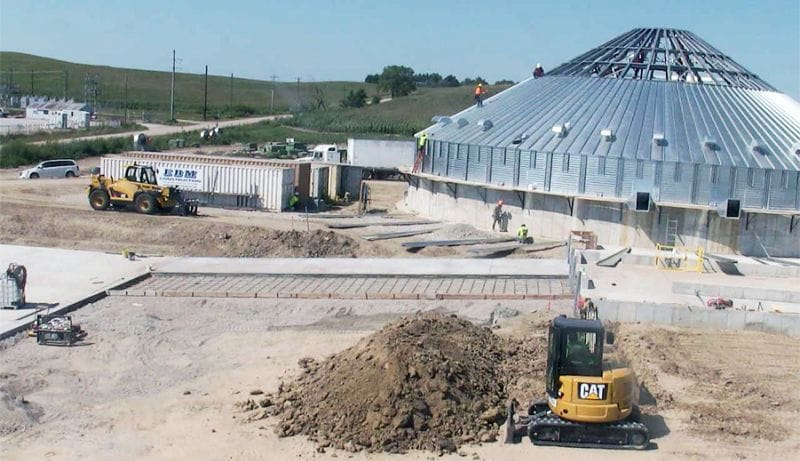
● Installation
Installation & Commissioning
Whether you choose your own subcontractor for the erection phase or you want to install everything together with us, a Richi supervisor will be around to make sure everything is mounted in a safe and thorough way.
● Training
Staff Training
We provide comprehensive training for the technicians of each project. We can also continue to provide support for the technicians during latter project operation.
● After-sales
Project Follow-Up
When everything is up and running our Richiers will help you further whenever needed. We are ready to answer your call 24/7.We’ll also visit you regularly to learn about your needs.
Who we are
RICHI Machinery is one of the world’s leading suppliers of technology and services for the animal feed, aqua feed and pet food industries, also the largest pellet production line manufacturer in China.
Since 1995, RICHI’s vision to build a first-class enterprise, to foster first-class employees, and to make first-class contributions to society has never wavered.
In the past three decades, we have expanded our business to a wide range of areas, including animal feed mill equipment, aqua feed equipment, pet feed equipment, biomass pellet equipment, fertilizer equipment, cat litter equipment, municipal solid waste pellets equipment, etc.

1995
RICHI Established

2000+
Serving More Than 2000 Customers

120+
RICHI Employees

140+
Exported To 140 Countries