 0086-138 3838 9622
5 T/H Commercial Wood Pellet Plant in Zimbabwe
A completed 12,000 T/Y dry-sawdust fuel pellet project in Mashonaland East using two MZLH678 pellet mills, counterflow cooling and no thermal dryer.
RICHI MACHINERY
Project Overview
The 5 T/H commercial wood pellet plant in Zimbabwe is built around a rare simplification: the customer buys clean sawdust that is already close to the pelleting moisture and particle-size window. That allows the line to omit a large dryer, wood chipper and hammer-mill section while keeping the annual production target at about 12,000 T/Y of 8 mm industrial fuel pellets.
The plant operates one 8-hour shift for about 300 days per year, giving 2,400 scheduled hours. At 12,000 T/Y, the required average output is exactly 5 T/H. Ten employees cover receiving, line operation, cooling and packing, maintenance, warehouse work and administration. Completed fixed investment is approximately US$155,000, including an imported equipment package of about US$85,000 plus freight, local electrical work, installation, dust control and site integration.
The main technical condition is feedstock discipline. Sawdust from furniture and secondary wood-processing operations normally arrives around 7–9% moisture and about 1–3 mm particle size. That is dry enough to avoid a thermal dryer, but it can be too dry for stable compression if fed without control. The pellet-mill feeders therefore allow small moisture adjustment before the two MZLH678 presses when incoming material falls below the preferred operating window. This makes the sawdust pellet plant in Zimbabwe highly dependent on receiving discipline: the same simplified equipment list would be unsuitable for green sawmill residue, bark-heavy waste or mixed offcuts. The raw-material contract is therefore part of the engineering design, not just a purchasing document.
5 T/H
capacity
$155,000
investment
Zimbabwe
location
Biofuel
project type
RICHI MACHINERY
The Project Was Possible Because the Sawdust Arrived Prepared
The customer had an established timber-trading background and access to furniture-industry residues around Harare and Mashonaland East. The opportunity was not simply “cheap sawdust.” It was sawdust that had already passed through kiln-dried lumber production and mechanical dust collection, so both moisture and particle size were much closer to what a pellet press needs.
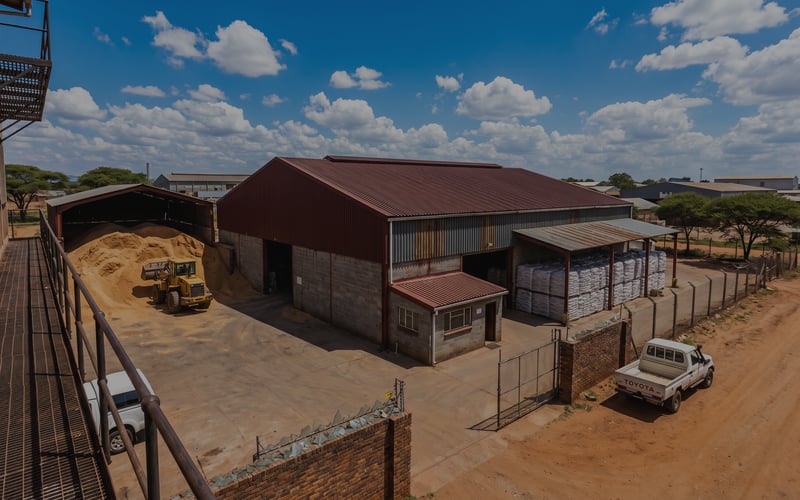
An existing 2,653 m² industrial building reduced the civil-work burden. The site already had a concrete floor, steel structure, water access and grid power, giving enough space for raw-material storage, a two-press pellet section, cooling, packing and finished-product warehousing without constructing a new factory shell.
The customer’s engineering question was whether a 5 T/H commercial wood pellet plant in Zimbabwe could run on furniture-factory sawdust without installing the size-reduction and drying sections found in a conventional green-wood pellet line.
Feedstock samples showed a consistent fine particle profile and about 7–9% moisture. That justified a simplified route, but only with strict receiving inspection, magnetic protection and the ability to add a small amount of moisture before pelleting when the driest loads created excessive die friction.
The finished design therefore uses two parallel MZLH678 pellet mills, a receiving protection stage, counterflow cooling, final screening and a central baghouse. The plant avoids equipment it does not need, but it does not skip the quality-control stages required after a 5 T/H hot pelleting process.
RICHI MACHINERY
One Feedstock Still Requires Supplier-by-Supplier Control
The customer contracts several furniture factories and sawmills within a practical trucking radius of Harare. Multiple suppliers reduce dependence on one workshop, but every load is checked for moisture, oversize particles and contamination before it enters the storage and pelleting system.
| Raw Material | Annual Input (tons) | As-Received Moisture | Cost Basis | Source |
|---|---|---|---|---|
| Clean furniture-grade sawdust | 12,030 | 7–9% | Approx. US$28/ton | Furniture factories and sawmills around Harare |
The process accepts only clean untreated sawdust. Painted wood, glued board waste, treated timber and mixed demolition residue are outside the raw-material boundary. The customer pays more for this pre-dried feedstock than for wet sawmill residue, but avoids the capital, fuel and maintenance burden of a dryer.
About 12,030 T/Y of incoming sawdust supports approximately 12,000 T/Y of finished pellets. The small difference is consistent with screening loss, dust recovery, startup loss and moisture equalization. Collected clean fines are returned to production where suitable, while used oil and maintenance waste are kept in the dedicated hazardous-waste area. Storage turnover is also planned around the one-shift schedule: at roughly 40 tons of finished output per operating day, the 700 m² raw-material zone provides a workable buffer without encouraging very long residence times for dry sawdust. That matters because even pre-dried material can pick up moisture if roof drainage, wall sealing or floor isolation is poor.
RICHI MACHINERY
Skipping the Dryer Only Works With a Dry-Sawdust Contract
Most wood pellet projects need drying when sawdust arrives from green logs or outdoor storage. This project has a different supply chain: furniture factories use dried lumber, and their extraction systems generate residue that is already close to the required moisture range.
The dryer-free route depends on three controls:
How it works:
- Only clean sawdust from approved furniture and wood-processing suppliers is accepted
- Receiving staff check moisture because loads at 7% and 11% do not behave the same in the pellet die
- Covered storage protects the dry-sawdust advantage before the material reaches production
The completed 5 T/H commercial wood pellet plant in Zimbabwe therefore has no thermal dryer or hot-air furnace. This reduces capital and fuel consumption, but it does not mean moisture can be ignored. Very dry sawdust may need a small controlled water addition at the pellet-mill feed system to stabilize compression and reduce die friction.
The commercial trade-off is clear: the customer pays more per ton for dry, clean sawdust, but avoids the equipment, fuel, floor area and operator attention required by a drying system. Whether that strategy is cheaper must be checked from actual local delivered prices rather than a universal savings figure.
RICHI MACHINERY
Two MZLH678 Pellet Mills Match the 5 T/H Annual Target
| Equipment | Quantity | Power | Function |
|---|---|---|---|
| Wood pellet mills | 2 × MZLH678 | 200 kW each | Main pelleting, about 2.5–3.0 T/H per machine |
| Receiving screen + magnetic protection | 1 set | Project-matched | Reject oversize material and protect pellet mills from metal |
| Counterflow cooler + pellet screener | 1 set | Project-matched | Cool hot pellets and remove loose fines before packing |
| Conveyors + bucket elevator | 1 system | Approx. 8–12 kW total | Feed and finished-product transfer |
| Baghouse filter | 1 | 11 kW | Central dust collection at pelleting and screening points |
| Exhaust stack | 15 m | — | Treated process-air discharge |
Main equipment package (EXW Qingdao): approximately US$85,000
The wheel loader was purchased locally in Harare so routine service and tyres could be sourced without importing a standard mobile machine. The imported package focuses on the two pellet mills, cooling/screening, conveying, protection and dust-control equipment.
Shipping: The main equipment shipment moved from Qingdao to Beira Port in Mozambique and then inland toward Harare because Zimbabwe is landlocked. The project freight basis includes approximately US$5,200 sea freight, about US$2,800 for the inland rail leg and about US$600 for final trucking. These logistics costs are part of the completed-project investment rather than the US$85,000 equipment price.
RICHI MACHINERY
The Existing 2,653 m² Building Leaves Room for Storage and Maintenance
The project reuses a former industrial building on a 2,653 m² property. Instead of filling the structure with unnecessary preprocessing equipment, the layout dedicates large areas to keeping dry sawdust protected, cooling and packing the finished pellets, and maintaining access around two high-load pellet mills.
| Area | Size (m²) | Function |
|---|---|---|
| Raw material storage | 700 | Covered dry-sawdust storage on the receiving side |
| Pelleting area | 400 | Two MZLH678 presses, cooler, screen and dust collection |
| Finished goods warehouse | 300 | Bagged 8 mm pellets awaiting dispatch |
| Office | 60 | Administration, production records and sales |
| Circulation and other | 1,193 | Receiving, bagging, aisles, maintenance and utility access |
The ten-person plant uses a septic system for domestic wastewater; no process wastewater is generated by the dry pellet route. The electrical connected load is approximately 440–480 kW once the two 200 kW pellet mills, cooler, screen, baghouse and conveyors are included. Annual electricity demand is planned at roughly 900,000–1,050,000 kWh depending on actual press load and operating days.
RICHI MACHINERY
A Short Process Still Needs Cooling and Screening
The plant is mechanically simpler than a green-wood pellet factory, but it is not just two pellet presses and a bag. Receiving control, moisture adjustment, cooling, screening and dust collection are all required for stable 5 T/H commercial operation. The installed MZLH capacity is deliberately slightly higher than the published line rating. Two 2.5–3.0 T/H presses can provide 5–6 T/H nameplate capacity, but the factory is sold and operated around a sustained 5 T/H balance because cooler load, screen performance, bagging rate and raw-material variation also determine real throughput.
Step 1 – Material receiving and protection
Dry sawdust moves from the 700 m² storage area through a receiving screen and magnetic protection. Loads containing oversize chunks, metal or visibly contaminated wood are isolated. Moisture is checked before the feed system; the driest material can receive a small controlled water addition before pelleting.
Step 2 – Pelleting
Two wood pellet extruder machines operate in parallel as MZLH678 presses. Each unit is rated at about 2.5–3.0 T/H, giving 5–6 T/H installed capacity. The plant publishes 5 T/H as its sustained line rating, producing 8 mm pellets for industrial heat while leaving practical margin for die condition and feedstock variation.
Both presses are required for full 5 T/H operation, but the parallel configuration allows limited production if one unit is stopped for die or roller service. Pellet formation relies on clean wood fiber and natural lignin; no routine chemical binder is required.
Step 3 – Cooling screening and bagging
Fresh pellets leave the dies hot and enter a counterflow cooler before they are screened. Loose fines are separated and recoverable clean material is recycled. The finished 8 mm pellets are then packed mainly in 25 kg woven bags or prepared for larger industrial orders. At 5 T/H, natural belt cooling alone is not used as the finished-product temperature-control system.
RICHI MACHINERY
Why the Plant Can Bypass Chipping and Hammer Milling
Most wood pellet production lines need wood chipper machines and wood pellet hammer mills because the raw material starts as logs, offcuts or coarse chips. This Zimbabwe project receives dust-collection sawdust that is already close to the required size.
The normal incoming particle range is about 1–3 mm. A safety screen and receiving inspection remove oversize material rather than regrinding every ton. This saves power and maintenance, but it also means supplier quality becomes part of the process specification.
Loads with pieces above the accepted size are rejected or handled separately instead of being forced through the pellet mills. The factory therefore saves the capital of a full grinding section while retaining the basic protection equipment needed for a commercial line.
RICHI MACHINERY
Dust Control Is Small in Equipment Count Not in Importance
The simplified process still generates dust at transfer, pelleting, cooling and screening points. A central baghouse with collection hoods serves the wood granulator machine discharge and finished-pellet handling areas.
Project dust-control basis:
- One central baghouse filter
- Approximate design airflow: 5,000 m³/h
- Exhaust stack height: 15 m
- Nominal collection efficiency used in the project calculation: about 95%
Annual particulate balance used for the project:
- Estimated total dust generation: about 12 T/Y
- Estimated baghouse capture: about 11.4 T/Y
- Estimated uncaptured / fugitive fraction within the workshop control area: about 0.6 T/Y
Captured clean fines are returned to the sawdust stream in controlled quantities. Housekeeping, filter inspection and sealed transfer points remain necessary because a high collection percentage does not eliminate settled dust around equipment.
Local environmental compliance should be checked against the project’s actual permit conditions and operating measurements. The case therefore keeps the equipment and calculated dust-control basis without claiming a blanket regulatory exemption or guaranteed compliance margin.
RICHI MACHINERY
Zimbabwe Gives the Project a Real Industrial Heat Use Case
Tobacco curing is an important heat-consuming activity in Zimbabwe, and wood-energy efficiency has long been part of the sector’s forestry and energy discussions. That makes densified biomass a technically relevant fuel option where the curing system, combustion equipment and delivered pellet cost are suitable. Other industrial and institutional heat users can provide additional demand outside the tobacco season. The commercial wood pellet plant in Zimbabwe is therefore positioned as an industrial-fuel project rather than a household-stove project. Buyers need consistent 8 mm fuel, predictable moisture and stable deliveries; the producer needs enough contracted demand to justify operating both pellet mills instead of carrying idle installed capacity.
The customer targets buyer groups rather than relying on one named sales contract:
- Tobacco-curing and agricultural-processing operations using solid-fuel heat systems
- Factories around Harare and Mashonaland East with compatible boilers or furnaces
- Institutional heat users that can store and feed bagged 8 mm pellets safely
Capacity expansion should follow contracted dry-sawdust supply and verified off-take. Adding another press before enlarging cooling, bagging, storage and electrical capacity would simply move the bottleneck to another section.
Renewable-energy and forestry policies can influence project economics, but incentives should be checked against current Zimbabwean rules and applicant eligibility. The completed factory is therefore presented on its process and market logic, not on an assumed tax benefit.
RICHI MACHINERY
The Main Operating Risk Is Losing the Dry-Feedstock Advantage
Once the plant began operating, the most important routine controls were moisture at receiving, pellet-mill load, cooler discharge temperature and bagging speed.
Controls that protect the simple process:
- Keep dry sawdust under cover so the line does not become a hidden dryer project during the rainy season
- Use two MZLH678 presses so full output is shared and limited production can continue during scheduled service
- Maintain the receiving screen and magnet even though no full crusher or hammer-mill section is installed
Items requiring regular attention:
- Use a moisture meter on every supplier group and add only controlled conditioning water when feedstock is too dry
- Keep the packing rate aligned with the 5 T/H cooler/screener output so finished pellets do not accumulate hot or exposed
- Stock one appropriate spare die and critical roller parts for each MZLH678 press
The simplified process lowers the number of machines, but it does not remove the need for power planning. With about 440–480 kW connected load and close to one million kWh of annual electricity use, stable grid supply and electrical protection remain important for a two-press commercial plant.
RICHI MACHINERY
RICHI Scope Focused on a Direct-Sawdust Pellet Route
For this 5 T/H commercial wood pellet plant in Zimbabwe, the engineering scope deliberately excludes a dryer and full grinding section while strengthening receiving control, pelleting, cooling and dust management.
- Process design – Direct-sawdust receiving, moisture conditioning, parallel pelleting, cooling, screening and bagging layout.
- Equipment package – Two wood pellet presses, receiving protection, cooler, screener, conveyors and baghouse.
- Installation supervision – Alignment, electrical interfaces, dust ducting, cooler setup and commissioning checks.
- Operator training – Moisture control, die/roller adjustment, pellet temperature, screening and dust-system maintenance.
- Spare parts kit – Die and roller wear parts, belts, bearings, cutting parts and filter bags.
The operating documentation also covers receiving acceptance, daily inspection and troubleshooting so the simplified line does not become dependent on one experienced operator.
RICHI MACHINERY
A Simple Zimbabwe Pellet Plant Starts With a Strict Sawdust Specification
For another 5 T/H commercial wood pellet plant in Zimbabwe, the first design decision should be whether the feedstock is truly dry and fine enough to justify deleting the dryer and grinding section. A supplier statement is not enough; moisture and particle size need to be measured across multiple loads.
- Pay for usable dry matter, not only a low wet-ton price. Dry furniture sawdust can justify a simpler factory when the supply is consistent.
- Keep the process simple only where the raw material allows it. Removing a dryer or hammer mill is an engineering decision, not a universal cost-saving rule.
- Match sales to compatible heat users. Tobacco curing and industrial boilers can be relevant markets, but combustion equipment and delivered fuel cost must be checked.
- Protect availability with critical spares. Two pellet mills only provide redundancy when dies, roller parts and filter consumables are available on site.
The finished project works because the feedstock condition and the equipment list match each other: 12,030 T/Y of clean dry sawdust, about 12,000 T/Y of 8 mm pellets, a true 5 T/H annual capacity requirement, two MZLH678 presses and no unnecessary thermal drying. A different Zimbabwe biomass pellet plant using wet sawmill residues would need a different process entirely, including drying and likely grinding. That distinction is important for buyers comparing project prices: the lower equipment count here is a result of feedstock quality, not a universal specification for every 5 T/H biomass line.
For a site assessment or wood pellet making equipment configuration, provide the annual dry-sawdust tonnage, moisture and particle-size ranges, working hours, building plan and target heat users. Those inputs allow the wood pellet plant construction scope to be matched to the real material instead of copied from a full green-wood process.
● RICHI MACHINERY
RICHI Service
● Consulting
Customer Consultation
We want to have a deep understanding of your industrial process, to know your exact needs of feed, wood, biomass, fertilizer or other pellet processing.
● Design
biomass Pellet Plant Design
Based on your unique situation and industrial process, we will tailor complete pellet plant you need, and inform you of every additional detail that could facilitate operation, minimize total cost.
● Manufacturing
Equipment Manufacturing
The critical components of the of the complete pellet production line equipment are built in our own workshops in Asia. Additional equipment is manufactured by our worldwide network of reliable partners.
● Testing
Quality Inspection & Testing
Before leaving the factory, all equipment will be inspected by the quality inspection department. We can also provide customers with testing services from a single machine to a complete pellet plant system, and provide you with real actual data for “worry-free use.”
● Delivery
Equipment Delivery
In equipment boxing and packaging, we adopt professional packaging and modular solutions to ensure the safe and non-destructive delivery of pellet plant equipment.
● Installation
Installation & Commissioning
Whether you choose your own subcontractor for the erection phase or you want to install everything together with us, a Richi supervisor will be around to make sure everything is mounted in a safe and thorough way.
● Training
Staff Training
We provide comprehensive training for the technicians of each project. We can also continue to provide support for the technicians during latter project operation.
● After-sales
Project Follow-Up
When everything is up and running our Richiers will help you further whenever needed. We are ready to answer your call 24/7.We’ll also visit you regularly to learn about your needs.
Who we are
RICHI Machinery is one of the world’s leading suppliers of technology and services for the animal feed, aqua feed and pet food industries, also the largest pellet production line manufacturer in China.
Since 1995, RICHI’s vision to build a first-class enterprise, to foster first-class employees, and to make first-class contributions to society has never wavered.
In the past three decades, we have expanded our business to a wide range of areas, including animal feed mill equipment, aqua feed equipment, pet feed equipment, biomass pellet equipment, fertilizer equipment, cat litter equipment, municipal solid waste pellets equipment, etc.

1995
RICHI Established

2000+
Serving More Than 2000 Customers

120+
RICHI Employees

140+
Exported To 140 Countries