

 0086-138 3838 9622
750 KG/H Biomass Pellet Plant in Greece
A compact Central Macedonia project converting dry furniture sawdust and baled cereal straw into 8 mm mixed biomass fuel pellets.
RICHI MACHINERY
Project Overview
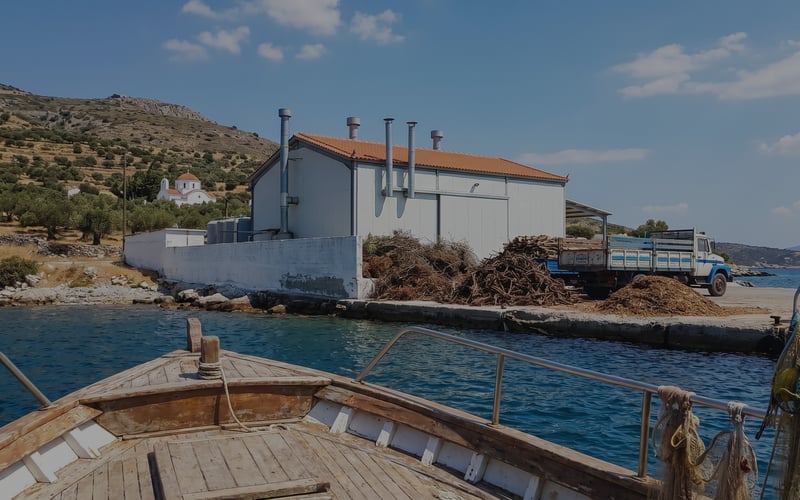
This 750 kg/h biomass pellet plant in Greece was commissioned in early 2024 for a client in Central Macedonia, approximately 40 km west of Thessaloniki. The customer already had an industrial building and access to two dry biomass streams: sawdust from furniture production and baled wheat and barley straw from nearby agricultural operations.
The biomass pellet plant was planned for about 1,500 tons of finished pellets per year. It operates one 8-hour shift per day for 250 days, giving 2,000 planned production hours. That annual target corresponds to an average finished-product rate of 750 kg/h, while the selected pellet mill has additional nameplate capacity so the line does not have to operate at its theoretical maximum every hour.
The project is small, but it is not a stripped-down pellet press installation. The final configuration includes straw preparation, fine grinding, controlled feedstock blending, pelleting, cooling, final screening, dust collection and bagging. Because both raw materials arrive at roughly 10–12% moisture, the line does not include a thermal dryer. This kept the plant compact enough for the client’s existing 2,000 m² site and 1,600 m² building.
750 KG/H
target output
1,500 T/Y
finished pellets
Greece
location
US$58,000
equipment investment
RICHI MACHINERY
Why This Small Greek Project Uses Two Feedstocks
The client had spent more than a decade in agricultural trading before investing in pellet production. That background gave him access to cereal growers, while the Thessaloniki-area furniture sector provided a second, more consistent material stream. Rather than build the project around one seasonal residue, the customer combined year-round furniture sawdust with contracted straw collected after the wheat and barley harvest.
This choice reduced dependence on a single supplier, but it also changed the process design. Sawdust is already fine and flows relatively easily. Baled straw is light, elastic and fibrous, so it first needs bale opening and coarse cutting before fine grinding. The two materials also differ in ash, silica, bulk density and die behavior. They cannot simply be tipped into the same hopper and treated as mechanically identical biomass.
The line was therefore sized as a flexible mixed-biomass system rather than as a miniature wood-only plant. The customer can adjust the sawdust-to-straw ratio according to raw-material availability and the fuel specification required by a particular buyer, while the basic downstream pelleting route remains unchanged.
RICHI MACHINERY
Raw Material Supply and Cost Basis
The supply network covers three furniture factories and around ten agricultural suppliers within an approximately 50 km collection radius. At project startup in 2023–2024, the customer was purchasing sawdust and straw at the following project-specific prices; they should not be treated as current Greek biomass quotations.
| Raw Material | Annual Input | As-Received Moisture | Startup Cost | Source |
|---|---|---|---|---|
| Furniture sawdust | 1,000 tons | 10–12% | US$25/ton | Three furniture factories |
| Wheat and barley straw | 510 tons | 10–12% | US$15/ton | Local farms and baling suppliers |
| Total project basis | 1,510 tons | About 10–12% | About US$21.50/ton weighted average | Multiple local suppliers |
The annual material balance is based on about 1,510 tons of incoming biomass and about 1,500 tons of finished pellets. Actual weight loss changes with incoming moisture, dust extraction, screening rejects and fines recycle. The small quantity of screened fines is returned to the biomass pellet production line where product quality permits.
Straw procurement is more seasonal than sawdust procurement, so the customer does not attempt to hold an entire year’s straw inventory inside the 550 m² warehouse. Baled straw is purchased in batches, kept dry, and replenished against production demand. This keeps storage requirements realistic for the available building area.
RICHI MACHINERY
Why the Line Does Not Need a Dryer
Dryer selection is based on incoming material condition, not on a rule that every biomass pellet production line must include thermal drying. In this project, the sawdust comes mainly from processing kiln-dried furniture lumber and the straw is purchased as dry bales. Project testing showed both streams at roughly 10–12% moisture.
That moisture level makes a no-dryer configuration practical, but only if the client protects the raw materials after purchasing them. Straw bales are stored under cover, sawdust is kept off wet floors, and incoming loads are checked before they enter the production queue. Material that has absorbed rainwater cannot simply be processed because the plant has no dryer to correct it.
The simplified route reduces initial equipment, heat-source requirements, fuel consumption and fire-management complexity. It also means moisture control shifts upstream into purchasing and storage. For this customer, that trade-off made sense because the existing raw-material network could already supply dry biomass.
RICHI MACHINERY
Finished Pellet and Certification Boundary
The mixed product is produced as an 8 mm biomass fuel pellet for customers whose combustion equipment can accept pellets containing herbaceous biomass. Because straw is intentionally blended with wood sawdust, this product should not be marketed as an ENplus-certified wood pellet. ENplus applies to wood pellets, while mixed or non-woody pellet products fall under a different fuel-classification route such as ISO 17225-6.
If the customer wants to serve a premium wood-pellet market later, the same site can run a separate wood-only production campaign, but the raw-material eligibility, segregation, quality testing and certification requirements would have to be handled independently. Straw cannot remain in an ENplus wood-pellet formulation simply because the finished diameter is the same.
- Mixed-biomass product: 8 mm sawdust-and-straw fuel pellets.
- Primary use: industrial or suitably designed commercial heating systems able to handle higher-ash herbaceous content.
- Packaging: 15 kg bags for smaller customers and 500 kg bulk bags for commercial users.
- Binder practice: no routine binder addition; blend ratio, moisture and die compression are used to maintain pellet formation.
- Wood-only option: possible as a separate production campaign if market and certification requirements justify it.
RICHI MACHINERY
Capacity Plan for 1,500 Tons per Year
The annual target is tightly linked to the working schedule: 1,500 tons divided by 2,000 planned hours equals 750 kg/h. That is the required average finished output, not the correct nameplate rating for the pellet mill. Selecting a machine with exactly 750 kg/h theoretical capacity would leave almost no allowance for feedstock variation, die wear, cleaning or minor interruptions.
| Planning Item | Project Value |
|---|---|
| Finished pellet target | About 1,500 T/Y |
| Working days | 250 days/year |
| Shifts | 1 shift/day |
| Hours per shift | 8 hours |
| Planned operating time | 2,000 hours/year |
| Required average output | 750 kg/h |
| Pellet mill selection | MZLH420, 90 kW, with operating reserve |
Pelleting is handled by one MZLH420 with a 90 kW main motor. Its 1.0–1.2 T/H biomass capacity provides operating reserve above the required 750 kg/h average output, helping the line absorb changes in straw proportion, bulk density, die resistance and routine maintenance conditions.
RICHI MACHINERY
Process Flow for Sawdust and Baled Straw
The two feedstocks do not enter the line in the same physical form, so the front end is split before they meet at fine grinding and controlled blending.
- Straw receiving and bale opening: dry wheat and barley straw is unloaded under cover and opened in manageable batches. Sawdust bypasses this stage.
- Straw coarse cutting: long fibers are shortened to approximately 20–30 mm so they can feed continuously instead of wrapping around downstream shafts.
- Fine grinding: pre-cut straw and sawdust are ground to a practical 3–5 mm range. Sawdust that already meets the required size can be screened and routed with less grinding duty.
- Metering and blending: the two ground materials are fed at a controlled ratio rather than mixed by loader estimation alone. The blend is adjusted for raw-material availability and the intended fuel specification.
- Pelleting: the mixed material enters the biomass pellet press. The die produces 8 mm pellets, with feed rate and compression settings adjusted because straw behaves differently from clean wood sawdust.
- Cooling: fresh pellets leave the die hot and must be cooled before storage. The cooler removes process heat and stabilizes the product for screening and packaging.
- Final screening: loose fines are separated from saleable pellets and suitable fines are recycled to the process.
- Bagging: cooled pellets are packed in 15 kg retail bags or 500 kg bulk bags according to the customer order.
The line uses no routine binder addition. Pellet formation depends on the sawdust fraction, straw condition, moisture, grinding quality, feed rate and die compression. When the raw-material ratio changes substantially, the operator rechecks pellet durability and fines before returning the line to normal production settings.
RICHI MACHINERY
Main Equipment Configuration
| Process Stage | Equipment | Model / Power | Qty | Function |
|---|---|---|---|---|
| Straw preparation | Bale opener and straw cutter | About 15–22 kW project class | 1 set | Open bales and shorten long cereal straw before fine grinding |
| Fine grinding | Biomass hammer mill | 22 kW project basis | 1 | Prepare 3–5 mm sawdust and straw material |
| Metering | Feed bins and dosing conveyors | Project-matched | 1 set | Control sawdust-to-straw ratio before pelleting |
| Pelleting | Biomass Pellet Mill | MZLH420, 90 kW | 1 | Form 8 mm mixed biomass fuel pellets |
| Cooling | Counterflow pellet cooler | Matched to small line | 1 | Reduce pellet temperature before screening and packing |
| Screening | Pellet screen | Matched to line capacity | 1 | Separate loose fines from finished product |
| Packaging | Weighing and bagging machine | 1.5 kW project basis | 1 | Pack 15 kg or 500 kg products |
| Dust control | Pulse-jet baghouse | 3.7 kW project basis | 1 system | Collect fine dust from grinding and transfer points |
| Conveying | Screw, belt and bucket conveying equipment | About 1.5 kW per small drive where applicable | Multiple | Transfer material between process stages |
The equipment contract value was approximately US$58,000 before international freight and local project costs. This 2023 project price should not be used as a current quotation for another 750 kg/h plant because steel prices, electrical scope, automation, packaging requirements and shipping conditions change.
RICHI MACHINERY
Using the Existing 1,600 m² Building
The client did not build a new factory shell. An existing steel-frame industrial building with a concrete floor already provided grid power, municipal water and sewer access. Reusing this building was one of the main reasons the plant could be completed within the US$118,000 fixed-investment level.
| Building Area | Size | Use in the Project |
|---|---|---|
| Production area | 900 m² | Straw preparation, grinding, blending, pelleting, cooling and packaging |
| Warehouse | 550 m² | Zoned storage for dry sawdust, straw bales and finished pellets |
| Office and QC area | 150 m² | Administration, purchasing, sales and production records |
| Total built area | 1,600 m² | Within a 2,000 m² site |
The warehouse is intentionally managed as turnover space rather than long-term annual storage. Straw bales occupy much more volume per ton than sawdust, so supply scheduling matters as much as floor area. Raw material and finished bags are separated into marked zones to reduce contamination and keep forklift routes clear.
RICHI MACHINERY
Utilities and Five-Person Operation
With no dryer or furnace, electricity is the dominant process utility. The 90 kW pellet mill is the largest individual load, followed by grinding, straw preparation, dust extraction, cooling and conveying. The existing grid connection was therefore checked against starting current and simultaneous motor demand before commissioning rather than being judged only by the previous building use.
Water demand is low because the process does not use wet conditioning as a primary production step. Municipal water serves staff facilities, cleaning and fire protection, with limited process adjustment only when required by the actual material condition.
- One operator supervises the main production line and control points.
- One worker handles straw receiving, bale opening and raw-material movement.
- One worker manages packaging, pallet or bulk-bag movement and warehouse turnover.
- One employee covers routine maintenance, moisture checks and basic product QC.
- One employee handles purchasing, dispatch, customer orders and administration.
These duties overlap in practice because the plant runs one shift rather than operating as a large continuous factory. The staffing level remains appropriate only while material receiving and packaging stay reasonably mechanized.
RICHI MACHINERY
Dust Control and Environmental Measures
The project’s environmental documentation identified fine dust as the main air-control issue. The pulse-jet baghouse serves the grinding and fine-material transfer area, while covered storage and housekeeping control dust from sawdust piles and straw handling.
| Environmental Item | Project Design Basis |
|---|---|
| Estimated dust generated | About 2.08 T/Y in the project calculation |
| Dust collected / filtered | About 2.058 T/Y, with suitable collected fines returned to production |
| Estimated fugitive dust | About 0.021 T/Y in the design calculation |
| Main control system | Single pulse-jet baghouse with local extraction points |
| Raw-material control | Covered indoor storage and protected sawdust piles |
These are project design estimates, not a substitute for operating measurements or permit limits. The plant also requires routine removal of settled biomass dust from motors, electrical cabinets, beams and floors because a small line still handles combustible fine material. Waste oil, worn filter bags and maintenance waste are kept separate from biomass feedstock and finished pellets.
RICHI MACHINERY
Shipping from Qingdao to Central Macedonia
The main equipment was packed into two 40-foot containers. The shipment left Qingdao on September 15, 2023 and reached the Port of Thessaloniki on October 28, 2023. From the port, the equipment moved by road to the client’s site in Central Macedonia.
| Logistics Item | 2023 Shipment Detail |
|---|---|
| Container quantity | Two 40-foot containers |
| Sea freight | About US$4,200 |
| Inland trucking | About US$600 |
| Freight and inland total | About US$4,800 |
The short inland distance from Thessaloniki port helped keep local transport straightforward. The figures above belong to the 2023 shipment and are retained as project history only; freight rates for a new Greek project need to be recalculated when the equipment is ready to ship.
RICHI MACHINERY
Fixed Investment of the Completed Project
The completed project fixed investment was approximately US$118,000. The machinery contract accounted for about US$58,000, while the remaining investment covered freight and the local work required to convert the existing building into an operating pellet facility.
| Cost Category | Project Treatment | What It Covered |
|---|---|---|
| Main equipment package | About US$58,000 | Preparation, grinding, pelleting, cooling, screening, dust control, packaging and conveying equipment |
| International freight and inland trucking | About US$4,800 | Two containers to Thessaloniki plus inland delivery |
| Electrical adaptation | Included in fixed investment | Power distribution, cabling and connection work for the equipment load |
| Foundations and building modifications | Included in fixed investment | Equipment bases, production zoning and installation preparation inside the existing building |
| Installation and commissioning | Included in fixed investment | Mechanical erection, testing and operator handover |
| Total fixed investment | About US$118,000 | Completed-project basis; normal working capital is handled separately |
The existing building is essential context for this number. A greenfield 750 kg/h project requiring land purchase, a new workshop, a larger transformer, fire-water construction or a dryer would have a very different capital profile even if the pellet capacity were the same.
RICHI MACHINERY
Commissioning Lessons from a Mixed-Biomass Line
The first operating months highlighted issues that are easy to underestimate when a small pellet plant handles straw as well as wood. Straw is lighter and more fibrous than sawdust, and its mineral content can increase wear. A small moisture meter, spare die and disciplined bale storage have more operating value than their purchase price suggests.
- Dry raw material justified removing the dryer, but moisture still has to be measured and controlled.
- Baled straw needs a preparation machine selected for fibrous material, not a generic wood chipper chosen only by motor power.
- Straw content changes die load and wear, so spare dies and rollers should be included in the maintenance plan.
- A 750 kg/h annual average should be supported by a pellet mill with reserve capacity rather than a machine already at its maximum rating.
- Mixed-biomass pellets need a market that accepts their ash and combustion characteristics; they should not be sold as certified wood pellets.
The plant layout leaves room for later capacity expansion. If the customer adds a second biomass fuel pellet machine, the expansion also needs a capacity check for hammer milling, dosing, cooling, dust extraction, electrical supply and finished-product handling. Adding pelleting capacity alone would simply move the bottleneck elsewhere.
RICHI MACHINERY
Project Timeline
The project moved quickly because the building and utilities were already in place. The engineering work focused on adapting the equipment to two different dry feedstocks and arranging the line within the existing workshop rather than constructing a new plant from the ground up.
- August 2023: confirm sawdust and straw availability, moisture, sample behavior and annual production target.
- Process design: define the no-dryer route, straw preparation, blending, pellet diameter and workshop arrangement.
- Equipment manufacturing: complete the production package, electrical matching and factory inspection.
- September 15, 2023: dispatch the main equipment from Qingdao in two 40-foot containers.
- October 28, 2023: receive the shipment at the Port of Thessaloniki and arrange inland delivery.
- Late 2023 to early 2024: complete local installation, electrical work, dust piping, trial production and operator training.
- Early 2024: commission routine one-shift production using the client’s actual sawdust and straw supply.
RICHI MACHINERY
RICHI Scope for the Greece Project
RICHI supplied the processing concept and equipment package around the customer’s existing building, local feedstock and 1,500 T/Y production objective.
- Raw-material evaluation for furniture sawdust and cereal straw.
- Process design for a dry-feedstock line without thermal drying.
- Straw preparation, hammer milling, dosing, pelleting, cooling, screening, bagging and dust-control equipment.
- Workshop layout and equipment-interface drawings for local installation.
- Installation supervision and commissioning support.
- Operator training covering material ratio, die changes, moisture checks and routine maintenance.
- Initial spare-parts planning for dies, rollers, bearings, belts and filter bags.
- Technical support for later adjustments or expansion planning.
RICHI MACHINERY
Planning a Small Biomass Pellet Project in Greece?
This project shows where a compact biomass line can make sense: the customer already has a suitable building, the raw materials are dry before they reach the factory, supply comes from more than one local source, and the finished-fuel market can accept a sawdust-and-straw pellet rather than requiring certified wood pellets.
For another project, the first questions should be different from “Which pellet mill is cheapest?” We need to know whether your straw arrives loose or baled, how much sawdust is available every month, the highest moisture after storage, the required pellet diameter, the combustion system used by your buyers, the number of operating hours, and the real dimensions of the building.
Send RICHI your raw-material photos, moisture range, annual supply quantities, site drawing and target product. We can use those conditions to size the process and determine whether your project needs drying, how much straw preparation is required, and which equipment should carry the production reserve. For investment planning, you can also review the scope of a complete biomass pellet project before comparing quotations.
● RICHI MACHINERY
RICHI Service

● Consulting
Customer Consultation
We want to have a deep understanding of your industrial process, to know your exact needs of feed, wood, biomass, fertilizer or other pellet processing.
● Design
biomass Pellet Plant Design
Based on your unique situation and industrial process, we will tailor complete pellet plant you need, and inform you of every additional detail that could facilitate operation, minimize total cost.

● Manufacturing
Equipment Manufacturing
The critical components of the of the complete pellet production line equipment are built in our own workshops in Asia. Additional equipment is manufactured by our worldwide network of reliable partners.

● Testing
Quality Inspection & Testing
Before leaving the factory, all equipment will be inspected by the quality inspection department. We can also provide customers with testing services from a single machine to a complete pellet plant system, and provide you with real actual data for “worry-free use.”

● Delivery
Equipment Delivery
In equipment boxing and packaging, we adopt professional packaging and modular solutions to ensure the safe and non-destructive delivery of pellet plant equipment.

● Installation
Installation & Commissioning
Whether you choose your own subcontractor for the erection phase or you want to install everything together with us, a Richi supervisor will be around to make sure everything is mounted in a safe and thorough way.

● Training
Staff Training
We provide comprehensive training for the technicians of each project. We can also continue to provide support for the technicians during latter project operation.

● After-sales
Project Follow-Up
When everything is up and running our Richiers will help you further whenever needed. We are ready to answer your call 24/7.We’ll also visit you regularly to learn about your needs.

Who we are
RICHI Machinery is one of the world’s leading suppliers of technology and services for the animal feed, aqua feed and pet food industries, also the largest pellet production line manufacturer in China.
Since 1995, RICHI’s vision to build a first-class enterprise, to foster first-class employees, and to make first-class contributions to society has never wavered.
In the past three decades, we have expanded our business to a wide range of areas, including animal feed mill equipment, aqua feed equipment, pet feed equipment, biomass pellet equipment, fertilizer equipment, cat litter equipment, municipal solid waste pellets equipment, etc.

1995
RICHI Established

2000+
Serving More Than 2000 Customers

120+
RICHI Employees

140+
Exported To 140 Countries



