 0086-138 3838 9622
3–4 T/H Wood Pellet Plant in Denmark
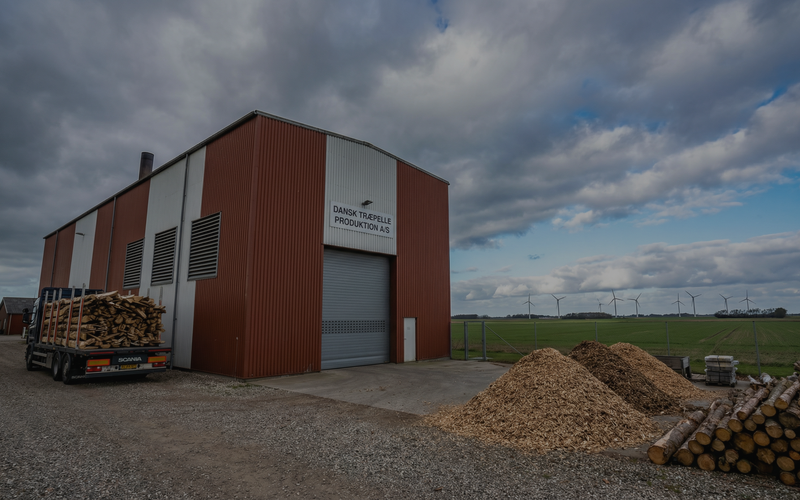
A Central Denmark project producing about 8,000 T/Y of heating pellets from dry furniture and sawmill residues with two MZLH520 pellet mills and no thermal dryer.
RICHI MACHINERY
Two Pellet Mills Carry the Whole Annual Production Plan
This 3–4 T/H wood pellet plant in Denmark was commissioned for a small regional producer in Central Denmark, around 40 km west of Aarhus. The project turns clean dry offcuts and sawdust from furniture factories and sawmills into heating pellets. The line is sized around an annual sales program of about 8,000 tons rather than around a large export terminal or continuous three-shift factory. That distinction keeps storage, staffing and packaging proportional to the customer’s regional business model.
The biomass pellet plant operates one 8-hour shift for about 300 days per year, or 2,400 scheduled hours. Producing 8,000 T/Y requires an average of roughly 3.33 T/H, so the final pelleting section uses two MZLH520 units rated at about 1.5–2.0 T/H each. Five employees cover receiving, line operation, packing, warehouse work and basic maintenance. Completed fixed investment is approximately US$142,000.
The key decision was to keep the process compact without under-sizing it. Two wood pellet mills provide 3–4 T/H of installed pelleting capacity, while the dry feedstock avoids a rotary dryer and furnace. The project still includes fine grinding, cooling, screening, dust collection and packing because a no-dryer line is only simple when every remaining stage is correctly matched.
3–4 T/H
capacity
$142,000
investment
Denmark
location
Biofuel
project type
RICHI MACHINERY
The Building Was Fixed Before the Equipment List Was
The customer already had a small agricultural and trading business in Central Denmark and wanted to add pellet production without developing a new industrial site. The available opportunity came from nearby furniture factories and sawmills that could supply dry clean wood residues in relatively regular form. The project therefore behaves more like a regional wood waste pellet plant in Denmark than a primary-forest processing complex.
An existing 1,800 m² ground-floor factory provided concrete floors, grid electricity, municipal water and sewer connection. The building favored a single-level process with short transfer routes, limited vertical lifts and a compact warehouse. Reusing the site kept the fixed investment proportionate to an 8,000 T/Y business.
The practical engineering question was not whether two pellet mills could be installed; it was whether two presses could sustain the annual tonnage without creating a bottleneck in grinding, cooling or bagging.
Incoming material samples were typically 8–10% moisture and came from kiln-dried wood. Clean offcuts still needed chipping and hammer milling, while fine sawdust could bypass unnecessary coarse reduction. Painted, laminated and chemically treated wood was excluded from the fuel stream.
The resulting wood pellet plant construction in Denmark uses two MZLH520 presses in parallel. That gives enough installed capacity for the 3.33 T/H annual average while retaining limited redundancy when one press is stopped for die or roller service.
RICHI MACHINERY
Dry Feedstock Supply Replaces a Dryer but Not Quality Control
The customer arranged supply from furniture factories and sawmills within roughly 50 km. That sourcing radius suits a dry-feedstock wood pellet plant in Denmark because transport remains manageable and suppliers can be audited for moisture, contamination and particle form. For a sawdust pellet plant in Denmark, dry bulk density and delivery frequency are especially important because warehouse volume can become the constraint before annual tonnage does.
| Raw Material | Annual Input (tons) | As-Received Moisture | Cost (USD/ton) | Source |
|---|---|---|---|---|
| Clean wood offcuts and sawdust | Approx. 8,200–8,400 accepted | 8–10% | Contract-specific | Furniture factories and sawmills |
The wider supplier network can offer up to about 8,900 tons in a year, but not every delivered ton is automatically accepted for pelleting. Loads outside the agreed moisture, cleanliness or particle-size window are segregated. This prevents cheap non-conforming wood from increasing ash, dust or wear in the finished product.
About 8,200–8,400 T/Y of accepted dry feedstock supports roughly 8,000 T/Y of saleable pellets after normal moisture adjustment, screening loss and recoverable fines recycle. That dry-matter balance is consistent with the no-dryer configuration and avoids assigning hundreds of tons to unexplained “moisture loss.” At 8,000 T/Y over 2,400 hours, the average required rate is about 3.33 T/H, which is why the plant cannot be treated as a true 3 T/H line.
Packaging is selected by customer channel rather than fixed around one bag size. Retail orders can use smaller bags, while commercial users can receive larger bulk bags or other agreed formats, reducing unnecessary packaging handling.
RICHI MACHINERY
The No-Dryer Route Works Because Moisture Risk Is Moved Upstream
Many wood pellet production lines need thermal drying because sawdust arrives directly from green lumber or primary sawmilling. This project purchases residues that have already passed through dry manufacturing environments.
Why no dryer? Accepted material is generally around 8–10% moisture. The customer pays attention to covered storage and supplier handling so rain or outdoor stockpiling does not turn a dry-feedstock design into a wet-feedstock problem.
Why two mills? Two MZLH520 presses provide 3–4 T/H of installed capacity. That is enough for the 8,000 T/Y program while keeping the line more maintainable than an oversized single-machine layout with no operating flexibility.
The commercial value of the no-dryer design comes from avoiding equipment, furnace fuel, hot-gas ducting and a larger environmental-control package. Those savings only remain valid while feedstock contracts continue to deliver genuinely dry clean wood.
RICHI MACHINERY
Two MZLH520 Presses Set the 3–4 T/H Capacity
| Equipment | Quantity | Power | Function |
|---|---|---|---|
| Wood chipper machine | 1 | 37 kW | Reduce larger dry offcuts before fine grinding |
| Wood pellet hammer mill | 1 | 55 kW | Prepare about 3–5 mm pellet feed |
| Wood granulator machine | 2 × MZLH520 | 132 kW each | Main pelleting, about 1.5–2.0 T/H per unit |
| Baghouse filter | 1 | 7.5 kW | Dust collection from preparation and transfer |
| Exhaust stack | 15 m | — | Treated-air discharge subject to site permit |
| Conveyors | Assorted | Project matched | Transfer plus compact cooling/screening connection |
Equipment package (EXW basis): approximately US$95,000
Shipping: The main machinery moved in two 40-foot containers from Qingdao to Port of Aarhus, Denmark before short-distance inland delivery. The project basis retains about US$5,200 for sea freight and about US$500 for local trucking.
RICHI MACHINERY
The 1,800 m² Building Keeps Raw and Finished Product Under One Roof
The single-story factory is compact enough that long vertical conveying is unnecessary. Raw wood, preparation, pelleting and finished-product dispatch are arranged in sequence so forklifts do not repeatedly cross the operator work zone.
| Area | Size (m²) | Function |
|---|---|---|
| Production workshop | 1,800 total building | Chipping, grinding, pelleting, cooling and packing |
| Raw material storage | Within 1,800 | Covered dry wood buffer separated from finished goods |
| Finished goods storage | Within 1,800 | Cooled pellets awaiting dispatch |
Municipal water and sewer are used mainly for staff and cleaning because the production process has no wet stage or steam system. The five-person team therefore creates only a small domestic wastewater load, while dust and fire prevention remain the main site-management priorities. Electrical planning is dominated by the two 132 kW pellet mills plus grinding, aspiration, conveying and cooling, so transformer and cabling capacity still need to be checked even in a no-dryer plant.
RICHI MACHINERY
Dry Wood Still Passes Through Four Controlled Production Stages
The Denmark wood pellet production line is short, but each stage protects the two pellet presses from a different feedstock risk.
Step 1 – Crushing
Larger dry offcuts are reduced to manageable chips before the hammer mill. Fine sawdust can bypass unnecessary coarse chipping when it already meets the feed condition.
Step 2 – Grinding
The hammer mill reduces prepared wood toward a stable 3–5 mm fraction. Screen condition and aspiration are checked because excessive fines waste power while oversize fibres increase die-load variation.
Step 3 – Pelleting
Ground material feeds two wood pellet presses configured as MZLH520 units. Each contributes about 1.5–2.0 T/H, giving 3–4 T/H of installed pelleting capacity. Finished diameter can be selected around 6 or 8 mm according to the heating customer and die specification.
Compression heat activates the natural lignin in the wood, so routine chemical binder addition is unnecessary. Fresh pellets are cooled and screened before packing; sending hot product directly into bags would create condensation and durability problems that do not disappear simply because the line has no dryer.
Step 4 – Bagging
Finished pellets are packed according to confirmed distributor or heating-customer orders. Packing throughput is checked against both presses so the bagging area does not become the limit when the pelleting section approaches its upper range.
RICHI MACHINERY
Dust Control Matters More When the Feedstock Is Already Dry
The project uses one centralized pulse-jet baghouse on the dry preparation and transfer section. Dry wood at 8–10% moisture can generate fine airborne dust during chipping, grinding and conveying, so aspiration is treated as part of production reliability rather than as a cosmetic housekeeping system.
System control points:
- Pulse-jet baghouse serving the main dry-dust generation points
- Differential-pressure and filter condition checks used to maintain stable suction
- Exhaust arrangement and stack height retained according to the approved site configuration
Operating practice:
- Recoverable clean dust can return to the process when it meets the raw-material specification
- Housekeeping prevents dry fines from accumulating around motors, bearings and electrical equipment
The chipper and hammer mill remain enclosed, and raw-material storage is separated from finished product. Fire prevention, grounding and dust removal are checked together because dry-fibre handling creates both product-loss and safety risks.
RICHI MACHINERY
Denmark Is a Mature Pellet User Not an Empty Market
Denmark already consumes substantial quantities of wood pellets in district heating, combined heat and power and private heating. Danish Energy Agency data show wood pellets remain a material part of both transformation-sector and household wood-fuel use. That gives this heating pellet plant in Denmark a real market context, but it also means a small producer has to compete on feedstock quality, delivery reliability and customer service rather than assuming demand alone guarantees sales.
- Wood pellets remain part of Denmark’s established woody-biomass energy system
- Commercial and district-heating users create demand beyond household bagged-pellet sales
- Quality and traceability matter in a mature market where buyers can compare multiple suppliers
- Regional delivery around Jutland can suit an 8,000 T/Y producer better than dependence on long-distance export
The customer therefore treats Denmark as the primary sales base and cross-border Germany as an optional channel tied to confirmed contracts. The plant’s size is better matched to regional distribution than to speculative commodity export.
RICHI MACHINERY
Commissioning Identified the Bottlenecks Outside the Pellet Mills
Early operation showed that the two-press concept was not the difficult part. Stable output depended on how quickly material could be prepared, cooled and packed around those presses. Because the line is staffed for one shift, short stoppages are easier to absorb than in a 24-hour plant, but repeated bottlenecks still reduce annual output quickly when the production target is 8,000 tons.
What worked as intended:
- Parallel MZLH520 presses provide maintenance flexibility; one unit can continue limited production while the other is stopped.
- The dry-feedstock route removes dryer fuel and thermal-control duties, keeping the five-person operating model realistic.
- The single-building layout makes short material routes and visual inspection easier for a small team.
What limits further growth:
- Packing speed needs to rise if retail bags become a larger share of sales; a second press alone would not solve that bottleneck.
- Chipping and grinding should be checked against peak offcut volume because dry sawdust and solid offcuts do not require the same preparation load.
- Critical dies, rollers and bearings should be stocked per press so a small spare-parts inventory does not become the reason for extended downtime.
RICHI MACHINERY
The Supplied Scope Was Built for a Dry Feedstock Business
For this 3–4 T/H complete wood pellet plant in Denmark, the supplied scope focused on converting already-dry residues without adding unnecessary thermal equipment. The same approach would apply to a biomass pellet plant in Denmark only when the proposed raw materials remain clean wood; agricultural residues or wetter forest biomass would require a different process basis:
- Process design – Single-level two-press layout matched to the existing 1,800 m² building.
- Equipment package – Chipper, hammer mill, two MZLH520 presses, conveying, cooling/screening and dust control.
- Installation supervision – Mechanical alignment, conveying interfaces, aspiration checks and commissioning support.
- Operator training – Feedstock inspection, moisture checks, die service, motor-load monitoring and safe dust-system operation.
- Spare parts kit – Wear parts and filter consumables selected for two parallel MZLH520 pellet mills.
RICHI MACHINERY
For Denmark Check Dry-Ton Supply Before Buying Pellet Capacity
If you are planning a wood pellet plant in Denmark, start with accepted dry feedstock and annual operating hours. A nominal 3 T/H line would not fully support an 8,000 T/Y target in 2,400 hours, which is why this project uses 3–4 T/H of installed pelleting capacity. A similar wood pellet production line in Denmark should also be checked against grinding, cooling and packing capacity before the press count is finalized.
- Size the presses from annual output. Two MZLH520 units provide enough margin for the 3.33 T/H average without forcing either machine to run continuously at its upper limit.
- Protect the no-dryer assumption. Supplier moisture, covered storage and receiving checks are operating requirements, not optional paperwork.
- Sell into a defined regional channel. Denmark has an established pellet market, so differentiation comes from reliable quality and delivery rather than unsupported premium-price claims.
- Plan cooling and packing with the same care as pelleting. A simple line fails if hot product or slow bagging stops both presses.
The project works because capacity, dry feedstock, building size and staffing remain aligned. Expansion should follow confirmed additional residue supply and sales—not the assumption that another pellet mill automatically creates another market. The current one-shift format also leaves a clear option to increase operating hours before changing every major machine, provided labor, utilities and buyer demand support that step.
For a similar wood pellet production line in Denmark, send annual dry-wood tonnage, moisture range, offcut size, working hours, building dimensions and expected bag/bulk split. Those figures determine whether a two-press no-dryer configuration is appropriate.
● RICHI MACHINERY
RICHI Service
● Consulting
Customer Consultation
We want to have a deep understanding of your industrial process, to know your exact needs of feed, wood, biomass, fertilizer or other pellet processing.
● Design
biomass Pellet Plant Design
Based on your unique situation and industrial process, we will tailor complete pellet plant you need, and inform you of every additional detail that could facilitate operation, minimize total cost.
● Manufacturing
Equipment Manufacturing
The critical components of the of the complete pellet production line equipment are built in our own workshops in Asia. Additional equipment is manufactured by our worldwide network of reliable partners.
● Testing
Quality Inspection & Testing
Before leaving the factory, all equipment will be inspected by the quality inspection department. We can also provide customers with testing services from a single machine to a complete pellet plant system, and provide you with real actual data for “worry-free use.”
● Delivery
Equipment Delivery
In equipment boxing and packaging, we adopt professional packaging and modular solutions to ensure the safe and non-destructive delivery of pellet plant equipment.
● Installation
Installation & Commissioning
Whether you choose your own subcontractor for the erection phase or you want to install everything together with us, a Richi supervisor will be around to make sure everything is mounted in a safe and thorough way.
● Training
Staff Training
We provide comprehensive training for the technicians of each project. We can also continue to provide support for the technicians during latter project operation.
● After-sales
Project Follow-Up
When everything is up and running our Richiers will help you further whenever needed. We are ready to answer your call 24/7.We’ll also visit you regularly to learn about your needs.
Who we are
RICHI Machinery is one of the world’s leading suppliers of technology and services for the animal feed, aqua feed and pet food industries, also the largest pellet production line manufacturer in China.
Since 1995, RICHI’s vision to build a first-class enterprise, to foster first-class employees, and to make first-class contributions to society has never wavered.
In the past three decades, we have expanded our business to a wide range of areas, including animal feed mill equipment, aqua feed equipment, pet feed equipment, biomass pellet equipment, fertilizer equipment, cat litter equipment, municipal solid waste pellets equipment, etc.

1995
RICHI Established

2000+
Serving More Than 2000 Customers

120+
RICHI Employees

140+
Exported To 140 Countries