

 0086-138 3838 9622
2–3 T/H Wood Pellet Plant in Italy
A Lombardy retrofit upgrading a partial pellet workshop into a 6,000 T/Y line with seasonal drying, one MZLH678 press, cooling and stronger dust/noise control.
RICHI MACHINERY
This Project Started as a Retrofit Not a Greenfield Plant
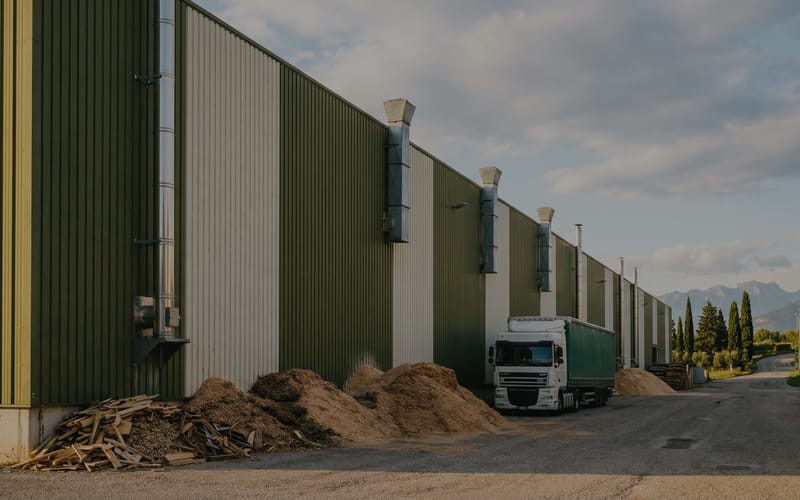
This 2–3 T/H wood pellet plant in Italy was completed as a retrofit in Lombardy, around 60 km east of Milan. The customer already had part of the material-preparation and drying equipment, but the original workshop layout, dust extraction and noise control were not suitable for a stable 6,000 T/Y heating-pellet operation. That retrofit history gives the page a different engineering basis from a new-build biomass pellet plant in Italy.
The biomass pellet plant operates one 8-hour shift for about 300 days per year, giving 2,400 scheduled hours. A 6,000 T/Y output requires an average of 2.5 T/H, so the final pelleting section is based on one MZLH678 rated at approximately 2.5–3.0 T/H with a 200 kW main motor. Ten employees cover receiving, preparation, operation, packing, maintenance and site support. Completed fixed investment is approximately US$175,000.
The distinctive engineering work was not simply adding more equipment. The retrofit had to relocate noisy preparation work, rebalance dust extraction, retain a seasonal dryer where it still added value, add proper pellet cooling, and simplify the pelleting section around one correctly sized press. The result is a compact wood pellet factory using existing assets without carrying forward the original bottlenecks.
2–3 T/H
capacity
$175,000
investment
Italy
location
Biofuel
project type
RICHI MACHINERY
The Existing Workshop Had Three Problems Before Expansion
The customer already occupied a 1,824 m² former industrial building and had installed a crusher, screening equipment, a small seasonal dryer and basic pelleting machinery. The retrofit was triggered when production growth exposed layout, noise and dust-control weaknesses that could not be solved by simply extending operating hours. Reusing the building still made economic sense, so the engineering priority was to correct the weak points without discarding usable assets.
Three issues shaped the engineering scope:
First: The crusher was too close to the building edge and transferred vibration into the structure, making noise control difficult during normal operation.
Second: The original dust collection and duct routing were not balanced for the combined crusher, screen, dryer and pelleting loads.
Third: The customer wanted a reliable 6,000 T/Y production plan without turning the retrofit into a second full greenfield investment.
The engineering objective became a practical one: retain useful existing equipment, remove the process bottlenecks and rebuild the pellet section around a capacity that actually matches 6,000 T/Y over one 8-hour shift.
A site review in Lombardy was therefore used to map material flow, noise sources, dust pickup points, dryer use, electrical demand and the available production/warehouse space before the final retrofit package was fixed.
RICHI MACHINERY
The Retrofit Solved Noise Dust and Capacity in Different Ways
Problem 1 – Noise at the preparation side.
The crusher location transmitted vibration toward the building edge and left little separation between high-impact size reduction and the rest of the workshop.
The fix: The crusher was moved toward the interior process area, vibration-isolation pads were added, and blade condition became part of scheduled maintenance. The objective was to reduce structural vibration and boundary noise without reducing crushing capacity.
Problem 2 – Dust collection and exhaust routing.
The existing filters and duct branches were not well balanced for the combined dry preparation and seasonal drying loads.
The fix: A third pulse-bag filter was added, duct branches were rebalanced and the exhaust arrangement was modified to fit the site’s approved environmental configuration. Filter pressure drop and pickup-point suction are now checked during routine operation.
Problem 3 – Partial process flow.
The old workshop had material-preparation and drying assets, but the line still lacked a clean capacity logic between preparation, pelleting, cooling and packing.
The fix: We completed the wood pellet production line around one MZLH678 biomass pellet mill, matched conveying and a proper cooling stage. The 2.5–3.0 T/H press covers the 2.5 T/H average required by the 6,000 T/Y plan.
RICHI MACHINERY
6,300 Tons of Mixed Wood Feedstock Close the Annual Mass Balance
The plant sources clean residues from furniture factories, sawmills and woodworking shops within roughly 50 km of the Lombardy site. Using three material forms gives the customer supply flexibility, but each stream enters the line differently. For a sawdust pellet plant in Italy, fine sawdust can move directly toward classification, while denser offcuts first consume crushing capacity.
| Raw Material | Annual Input (tons) | As-Received Moisture | Cost (USD/ton) | Source |
|---|---|---|---|---|
| Wood shavings | 900 | 10–12% | Contract-specific | Furniture factories |
| Sawdust | 1,800 | 12–15% | Contract-specific | Local sawmills |
| Wood offcuts | 3,600 | 15–18% | Contract-specific | Sawmills and woodworking shops |
| Total | 6,300 | Variable by stream | Contract basis |
At about 6,300 T/Y of accepted feedstock, the plant can produce roughly 6,000 T/Y of saleable pellets after seasonal moisture removal, screening loss and fines recycle. This closes the project mass balance without the contradictory 7,000-ton ingredient table that would otherwise overstate annual consumption. Dividing 6,000 tons by 2,400 scheduled hours gives the 2.5 T/H average that determines the final MZLH678 size.
Shavings and dry sawdust can move directly toward fine preparation, while larger offcuts require crushing. The existing natural-gas dryer is retained for wetter winter material, with annual gas use around 100,000 Nm³ on the project basis. Cleaner summer lots can bypass full thermal duty when moisture is already suitable.
RICHI MACHINERY
Seasonal Drying Is More Practical Than Running a Dryer All Year
Most incoming material is close to the pelleting moisture window, but winter storage and wetter offcut lots can reach about 18–20%. A small seasonal dryer therefore remains useful even though the plant does not need year-round thermal drying.
The rotary drum operates mainly during the wetter season and is bypassed for suitably dry material. This lowers gas demand while preserving the ability to stabilize moisture before the MZLH678 when supplier conditions change.
Dryer operating basis:
- Type: Rotary drum, direct heating
- Heat source: Natural-gas furnace matched to the seasonal drying duty
- Natural gas consumption: approximately 100,000 Nm³/year on the project basis
- Operating period: mainly winter and wet-weather production rather than year-round use
The dryer exhaust is handled under the site’s approved emission arrangement. Using natural gas reduces solid-fuel handling and ash, but it does not remove the need to check exhaust temperature, particulate carryover and permit conditions for the actual installation.
RICHI MACHINERY
One MZLH678 Replaces the Old Two-Press Capacity Logic
| Equipment | Quantity | Power | Function |
|---|---|---|---|
| Crusher | 1 | 55 kW | Reduce clean wood offcuts before fine preparation |
| Screening machine | 1 | 2.2 kW | Classification plus connection to cooling stage |
| Rotary drum dryer | 1 | 7.5 kW | Seasonal moisture correction |
| Natural gas furnace – 1.5t/h | 1 | — | Heat source for seasonal dryer |
| Biomass wood pellet machines | 1 × MZLH678 | 200 kW | Main pelleting, about 2.5–3.0 T/H |
| Belt conveyors | 2 | 1.5 kW each | Material transfer between retrofit sections |
| Wheel loader | 1 | Diesel | Raw material handling |
| Pulse baghouse filters | 3 | 7.5 kW each | Dust collection for preparation, drying and pelleting |
| Exhaust stack (1#) | 15 m | — | Process-dust exhaust under site permit |
| Exhaust stack (2#) | 15 m | — | Seasonal dryer exhaust |
Equipment package (EXW basis): approximately US$105,000
The wheel loader was sourced locally in Italy, while the imported package concentrated on the process equipment and retrofit components that directly affect pellet quality and plant compliance.
Shipping: The imported retrofit package moved in three 40-foot containers from Qingdao to Port of Genoa, Italy before inland trucking to Lombardy. The project basis retains about US$5,200 of sea freight and about US$1,200 for the final inland leg.
RICHI MACHINERY
The 1,824 m² Workshop Had to Be Re-Zoned Around Noise and Material Flow
The former industrial building provides 1,824 m² of usable area. Instead of replacing it, the retrofit separates raw-material storage, high-noise preparation, seasonal drying, pelleting/cooling and finished-product handling so forklifts and operators do not repeatedly cross the same work zones. The result is a compact wood pellet plant retrofit in Italy where layout changes deliver as much operational value as the new press itself.
| Area | Size (m²) | Function |
|---|---|---|
| Raw material storage | 650 | Shavings, sawdust and offcuts with lot separation |
| Production area | ~1,000 | Crushing, screening, seasonal drying, MZLH678 and cooling |
| Finished goods storage | 150 | Cooled bagged pellets separated from raw material |
| Office | 24 | Administration, production records and sales |
RICHI MACHINERY
The Retrofit Creates One Clear Route Through Existing Equipment
The completed Italy wood pellet production line combines retained preparation assets with a new capacity logic built around one 2.5–3.0 T/H pellet mill.
Step 1 – Raw material receiving
Shavings, sawdust and clean offcuts arrive by truck and are stored by material form and moisture. Offcuts are directed to crushing while suitable fine material can bypass unnecessary size reduction.
Step 2 – Crushing
Clean offcuts are reduced before screening. The crusher is located and isolated to limit structural vibration while still allowing loader access for maintenance and feeding.
Step 3 – Screening
Prepared material is classified so oversize pieces return to size reduction and acceptable feed moves toward either seasonal drying or direct pelleting.
Step 4 – Drying– Winter only
Wetter seasonal lots pass through the rotary dryer from roughly 18–20% toward the pelleting range. Drier shavings and sawdust can bypass full thermal duty, reducing gas use and unnecessary moisture removal.
Step 5 – Pelleting
Prepared material enters the wood pellet press configured as one MZLH678. The 200 kW press provides about 2.5–3.0 T/H, matching the 2.5 T/H average needed for the 6,000 T/Y annual target. The line can produce 6 mm or 8 mm pellets according to the sales specification.
Pellet quality is controlled through particle size, moisture, feed rate and die condition. Natural wood lignin provides binding under compression; routine chemical binder addition is unnecessary for the accepted clean-wood feedstock.
Step 6 – Cooling and bagging
Fresh pellets enter a compact cooling stage before packing. Retail and bulk-bag formats can be handled according to order mix, but hot pellets are not sent directly into storage.
Step 7 – Dust collection
Three pulse baghouse filters serve the crusher, screen, dryer transfer points and wood pellet extruder machine area. Clean recoverable fines can return to production when they meet the feedstock specification.
RICHI MACHINERY
Italy Rewards Quality but Does Not Remove the Need for Cost Control
Italy has one of Europe’s largest residential wood-pellet markets and a well-developed distribution network. AIEL’s pellet industry group reports large volumes of certified product moving through the Italian market, confirming that heating demand is established rather than hypothetical. For this heating pellet plant in Italy, that supports regional sales but also creates strong competition on quality, packaging, delivery and traceability.
- Premium heating channels place strong emphasis on consistent pellet quality and certification where applicable
- Biomass-heating incentives and policies can change over time, so investment should not rely on one fixed subsidy percentage
- Regional distributors, retailers and heating-system users provide several sales channels within northern Italy
The project is therefore positioned around customer types rather than unverified named contracts:
- Pellet traders and regional distributors able to take repeat bulk or bagged volumes
- Hardware and heating retailers requiring reliable seasonal supply
- Commercial and residential users served through local distribution partners
Any future expansion should first confirm additional dry feedstock, cooling/packing capacity and electrical headroom. Adding another wood pellet mill before those constraints are checked would recreate the imbalance that the retrofit was designed to remove.
RICHI MACHINERY
The Most Useful Lessons Came From Correcting an Existing Workshop
Because this was a retrofit, commissioning focused on whether each correction actually changed daily operation rather than on demonstrating a new factory from zero. The operator had to learn a new material-routing logic, a larger single press and revised dust-control checks while still working inside the same building. That makes the operating transition as important as the mechanical installation.
What improved the plant:
- Relocating and isolating the crusher reduced vibration transfer and made the preparation area easier to manage.
- Rebalanced extraction and an additional filter improved dust capture across several process sources instead of relying on one overloaded duct route.
- One correctly sized MZLH678 simplified pelleting capacity around the actual 6,000 T/Y production plan.
What should be checked before the next expansion:
- Permit, environmental and utility requirements should be reviewed before equipment is moved or new capacity is added.
- Packing labor can become restrictive if retail bags increase, so an automatic scale may add more value than more press capacity.
- Any additional press requires a fresh review of grinding, cooling, electricity and raw-material supply; demand alone is not enough.
RICHI MACHINERY
The RICHI Scope Focused on Retrofit Risk
For this 2–3 T/H wood pellet plant engineering project in Italy, the supplied work centered on integrating retained assets with the new pelleting and environmental-control configuration. The project scope had to distinguish what was worth keeping from what would continue to restrict a 6,000 T/Y wood pellet production line in Italy:
- Site assessment – Material-flow review, noise-source mapping, dust-system inspection and utility checks.
- Retrofit design – Crusher relocation, vibration isolation, seasonal-dryer routing and revised material flow.
- Additional equipment – MZLH678 pelleting, cooling integration, extra filtration and conveyor modifications.
- Installation supervision – Mechanical alignment, ductwork balancing, startup checks and retrofit sequencing.
- Operator training – Moisture control, dust-filter inspection, press loading, cooling and maintenance routines.
- Compliance documentation – Technical project data prepared for the customer’s local permitting and environmental review process.
RICHI MACHINERY
For an Italian Retrofit Audit the Existing Line Before Adding Machines
If you are considering a wood pellet plant retrofit in Italy, start with the equipment already on site, actual feedstock moisture, building layout and environmental-control gaps. The lowest-cost retrofit is the one that keeps useful assets without preserving the bottlenecks attached to them. A greenfield wood pellet plant in Italy would not necessarily use the same seasonal dryer or workshop zoning.
- Do not size expansion from demand alone. Annual output, working hours and the retained preparation equipment must all support the proposed pellet capacity.
- Noise control begins with machine placement and maintenance. Vibration isolation, blade condition and distance from sensitive boundaries can matter as much as enclosure.
- Stack height is site-specific. Do not copy one number from another factory; exhaust design has to follow the actual permit, building geometry and emission source.
- Natural-gas drying still needs engineering control. Cleaner combustion does not eliminate the need to manage dryer carryover, temperature and approved exhaust conditions.
- Certification is not created by the pellet mill. Premium heating-pellet claims require quality testing, traceability and the producer’s own certification process where applicable.
The value of this project is the retrofit logic: a seasonal dryer, mixed dry wood residues and an existing building were retained, while capacity, dust control, cooling and material flow were rebuilt around a consistent 6,000 T/Y target. That approach also keeps the US$175,000 completed investment proportionate to the scale of the project instead of turning a medium retrofit into a full factory replacement.
For a similar Italian retrofit, send the existing equipment list, raw-material moisture by season, annual target, building drawing, available electrical supply and current dust/noise-control arrangement. Those inputs determine what should be retained, relocated, replaced or added.
● RICHI MACHINERY
RICHI Service

● Consulting
Customer Consultation
We want to have a deep understanding of your industrial process, to know your exact needs of feed, wood, biomass, fertilizer or other pellet processing.
● Design
biomass Pellet Plant Design
Based on your unique situation and industrial process, we will tailor complete pellet plant you need, and inform you of every additional detail that could facilitate operation, minimize total cost.

● Manufacturing
Equipment Manufacturing
The critical components of the of the complete pellet production line equipment are built in our own workshops in Asia. Additional equipment is manufactured by our worldwide network of reliable partners.

● Testing
Quality Inspection & Testing
Before leaving the factory, all equipment will be inspected by the quality inspection department. We can also provide customers with testing services from a single machine to a complete pellet plant system, and provide you with real actual data for “worry-free use.”

● Delivery
Equipment Delivery
In equipment boxing and packaging, we adopt professional packaging and modular solutions to ensure the safe and non-destructive delivery of pellet plant equipment.

● Installation
Installation & Commissioning
Whether you choose your own subcontractor for the erection phase or you want to install everything together with us, a Richi supervisor will be around to make sure everything is mounted in a safe and thorough way.

● Training
Staff Training
We provide comprehensive training for the technicians of each project. We can also continue to provide support for the technicians during latter project operation.

● After-sales
Project Follow-Up
When everything is up and running our Richiers will help you further whenever needed. We are ready to answer your call 24/7.We’ll also visit you regularly to learn about your needs.

Who we are
RICHI Machinery is one of the world’s leading suppliers of technology and services for the animal feed, aqua feed and pet food industries, also the largest pellet production line manufacturer in China.
Since 1995, RICHI’s vision to build a first-class enterprise, to foster first-class employees, and to make first-class contributions to society has never wavered.
In the past three decades, we have expanded our business to a wide range of areas, including animal feed mill equipment, aqua feed equipment, pet feed equipment, biomass pellet equipment, fertilizer equipment, cat litter equipment, municipal solid waste pellets equipment, etc.

1995
RICHI Established

2000+
Serving More Than 2000 Customers

120+
RICHI Employees

140+
Exported To 140 Countries



