

 0086-138 3838 9622
Rice Straw Pellet Processing Line for Heating Fuel in Cambodia
RICHI MACHINERY
Project Overview
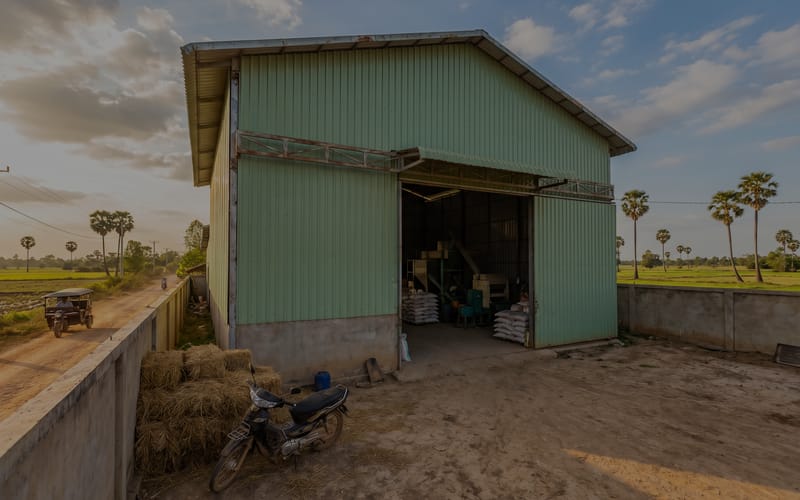
A biomass-fuel startup developed this Rice Straw Pellet Processing Line for Heating Fuel in Cambodia in Battambang Province to convert baled rice straw into an industrial solid fuel for rice mills, food processors, dryers and other small boiler users. The project is based on one seasonal agricultural residue rather than a mixed-biomass recipe, so straw collection, covered storage, ash control and boiler compatibility are the main design issues.
Finished output is approximately 9,000 T/A. The plant operates about 300 days per year for 10 production hours per day, which requires an average saleable output of 3 T/H. One MZLH678 biomass pellet mill with a 200 kW main motor is configured around this project duty, giving the annual plan a direct capacity match without using an undersized 75–90 kW machine.
The feedstock plan uses about 9,800 T/A of baled rice straw at roughly 14–16% weighted receiving moisture. After removal of soil, stones, metal, excess fines and around 450–550 tons of water during conditioning, pelletizing and cooling, the line produces approximately 9,000 T/A of finished fuel pellets at about 9–11% moisture.
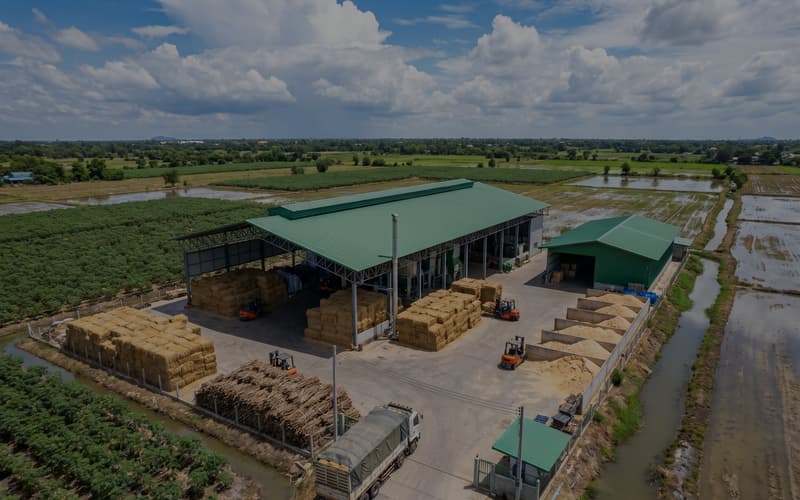
The completed project represents a fixed total investment of USD 328,000, including a USD 228,000 RICHI equipment package. The operating site is approximately 3,200 m² with about 1,500 m² of covered production and straw storage. This remains a compact Battambang project, but it provides enough protected space for several days of bulky baled straw, mechanical cooling, truck access and fire separation.
3T/H
capacity
$328,000
investment
Cambodia
location
Biofuel
project type
RICHI MACHINERY
Why Cambodia? (Market Context for Rice Straw Pellets)
Cambodia has a strong rice-residue base. FAO’s 2026 country brief forecasts 2025 aggregate paddy production at about 14.6 million tonnes, roughly 17% above the five-year average. Battambang is one of the country’s important rice-producing provinces, and the 2024 Cambodia Agriculture Survey reported some of the country’s strongest aromatic-paddy yields there.
That does not mean all straw is available for pellets. Some remains in fields, some is used for livestock or soil cover, and collection cost can rise sharply when fields are small or distant. The project therefore contracts baled straw within a practical radius and buys on delivered moisture and cleanliness rather than assuming a national straw-to-paddy ratio automatically becomes factory supply.
| Target Customer | Why Rice-Straw Pellets May Fit | Commercial Check |
|---|---|---|
| Rice mills and dryers | More uniform fuel feeding than loose straw | Boiler grate, ash removal and delivered cost |
| Food / agro-processing boilers | Dry standardized solid fuel | Fuel trial and emissions/ash handling |
| Small industrial steam users | Higher bulk density than loose straw | Storage, feeding and clinker behavior |
| Biomass traders | Densified product for regional resale | Moisture, ash and contracted volume |
Household heating is not treated as a main market in Cambodia’s climate. The commercial route is industrial thermal energy, where customers already burn rice husk, wood, coal or other fuels and may value a denser, more consistent product.
Cambodia’s Ministry of Mines and Energy reported that biomass contributed about 0.92% of installed renewable electricity capacity in 2025. Biomass is therefore part of the country’s energy system, but this project does not assume power-sector demand or a government pellet subsidy; regional industrial boilers remain the base market.
RICHI MACHINERY
Raw Materials: Rice Straw
The commercial feedstock is 100% rice straw, but the purchasing specification is stricter than simply accepting any post-harvest bale. Rice straw carries silica naturally and can also pick up soil, sand, stones and metal during harvesting and baling, all of which raise ash and equipment wear.
| Raw Material Parameter | Project Purchasing Range | Reason |
|---|---|---|
| Annual gross straw intake | Approx. 9,800 T/A | Supports about 9,000 T/A finished pellets |
| Receiving moisture | Normally about 12–18% | Limits drying load and biological deterioration |
| Bale form | Small/medium square or compact rectangular bales | Reduces transport volume and handling loss |
| Visible soil / sand | Low; contaminated bales rejected | Controls ash, die wear and clinker risk |
| Mold / decay | Not accepted | Protects storage and fuel consistency |
At about 15% average moisture, 9,800 tons of straw contains roughly 8,330 tons of dry matter. Finished pellets at 9,000 T/A and about 10% moisture contain about 8,100 tons of dry matter. The difference provides a realistic allowance for soil/mineral removal, foreign material, screening loss and unrecoverable fines.
The plant does not depend on every farmer delivering straw at exactly 10–15% moisture. Dry-season bales may enter preparation directly, while wetter lots are held under cover with forced ventilation or routed through limited pre-drying before grinding. Straw that arrives excessively wet or moldy is rejected.
- Moisture is measured with a calibrated meter, not only by hand feel.
- Baling wire, metal, stones and plastic are removed before size reduction.
- Very dirty straw is not blended down with clean straw to hide high ash.
- Supplier contracts define maximum moisture and contamination.
- Harvest-season purchasing is staged so the factory does not need to store the full annual requirement on site.
A full-size straw dryer is not included in the first-stage project because the procurement strategy is based on field-dried baled straw. If future supply shifts toward wetter feedstock, a dedicated drying module must be sized from actual tonnes of water evaporation.
RICHI MACHINERY
The Site and Building
The operating site is approximately 3,200 m² in Battambang Province. About 1,500 m² is covered, while the remaining area provides truck circulation, fire separation, bale unloading and limited short-term outdoor handling. This is still a compact project for 9,000 T/A, but it avoids forcing a 3 T/H straw line into a 666 m² property.
| Zone | Approx. Area | Main Use |
|---|---|---|
| Covered baled-straw storage | 650 m² | Several days of protected feedstock |
| Preparation / grinding | 300 m² | Bale breaking, cutting and hammer milling |
| Pelletizing / cooling / screening | 300 m² | MZLH678, cooler and screener |
| Packing / finished-product buffer | 150 m² | FIBC / bagged pellet dispatch |
| Electrical / QC / maintenance / office | 100 m² | Controls, moisture/ash sampling and spares |
| Roads / fire access / unloading / utility space | Balance of site | Truck turning and safe separation |
The 8 m building height is sufficient for bale feeding, elevators, day bins, MZLH678, counterflow cooler and screening equipment. The project does not need a tall tower or large storage silos.
Because baled straw has low bulk density, the site cannot economically hold months of feedstock. The customer contracts farmers, baling teams and collection points to hold part of the seasonal inventory, then schedules deliveries into the covered factory buffer.
Finished pellets are kept as short dispatch inventory. The line is designed for regular industrial shipments rather than using valuable covered space as a long-term product warehouse.
RICHI MACHINERY
Equipment Configuration
The equipment package is simple but fully commercial. It adds the handling and cooling stages needed for 3 T/H continuous output instead of relying on workers to carry ground straw, shovel hot pellets and cool product on the floor.
| Section | Main Equipment | Project Configuration |
|---|---|---|
| Bale receiving | Bale breaker / straw feeder | Controlled feed into cutting section |
| Primary size reduction | Straw cutter / crusher | Shortens long fibrous straw before hammer milling |
| Fine grinding | Hammer mill + aspiration | Approx. 4 T/H prepared-straw duty |
| Protection | Magnetic separator + coarse contamination screen | Removes ferrous metal and oversize debris |
| Buffering | Small day bin + variable feeder | Stabilizes pellet-mill feed |
| Pelletizing | 1 × MZLH678 straw pellet machine | 200 kW; configured around 3 T/H project duty |
| Pelletizing reference | Rice straw pellet making machine | MZLH ring-die route for industrial straw fuel |
| Cooling | Counterflow cooler | Matched to 3 T/H output |
| Screening | Pellet screener + fines return | Controls loose fines before packing |
| Packing | Semi-automatic FIBC / bagging station | Industrial bulk bags plus 25–50 kg option |
| Dust control | Cyclone + bag-filter aspiration | Grinding, transfer and screening points |
| Controls | Compact PLC / MCC | Interlocks, alarms and overload protection |
The fixed RICHI equipment package is USD 228,000. The completed USD 328,000 investment also covers the building adaptation, electrical service, foundations, fire equipment, local steelwork, installation, commissioning and initial spare parts.
The line does not include a thermal dryer, but it does include mechanical conveying and cooling. At 3 T/H, those two functions provide more value than trying to save capital through constant manual shoveling.
MZLH678 is used because its biomass-duty size matches the dry prepared-straw requirement. The plant does not claim that a 75–90 kW ring-die machine can produce 3 T/H of rice-straw pellets continuously.
RICHI MACHINERY
Process Flow
The process is designed around baled straw rather than loose powder. Controlled bale opening, fiber cutting and fine grinding are necessary before stable ring-die pelletizing.
Step 1: Raw Material Receiving and Storage
Baled straw arrives by truck and is unloaded into the covered receiving/storage zone. Each lot is recorded by supplier and checked for moisture, mold and visible soil contamination. Several days of straw are held on site; the wider seasonal inventory remains with contracted suppliers or collection points.
Step 2: Grinding (Hammer Milling)
Bales are opened mechanically and the straw first passes through a cutter so long stems do not wrap around the hammer-mill feed system. The hammer mill then reduces the prepared fiber to a few-millimeter particle distribution suitable for ring-die feeding. Screen size is selected from actual fiber behavior rather than fixed permanently at 6 mm.
Step 3: Buffer Storage
Ground straw enters a day bin with level indication and a variable-speed discharge feeder. The buffer separates intermittent grinding from continuous pelletizing and eliminates manual shoveling into the pellet mill.
Step 4: Pelletizing
Prepared straw enters the MZLH678 biomass fuel pellet machine. The normal product is 8 mm industrial fuel pellet. Feed moisture, die compression and roller gap are established during commissioning from actual Battambang straw, because silica, particle size and moisture affect both output and die wear.
The biomass pellet press does not use one universal 5:1 compression ratio or a fixed 180 RPM die speed for every straw source. The operating point is selected from motor load, pellet durability, fines and temperature.
Step 5: Cooling
Hot pellets discharge directly into a compact counterflow cooler. Mechanical cooling brings product temperature close to ambient before screening and storage. Floor spreading for four to six hours is not used because it occupies space, increases contamination risk and creates inconsistent cooling during humid weather.
Step 6: Bagging
Cooled pellets pass through a screener and clean fines are returned in a controlled proportion. Industrial customers can receive FIBC, while smaller boiler users can use 25–50 kg bags. Mechanical transfer into the bagging station replaces manual shoveling.
Batch records link supplier, incoming moisture, pellet-mill settings and finished moisture/ash results so buyers can see whether a high-ash lot came from raw-material contamination or normal rice-straw mineral content.
RICHI MACHINERY
Utilities and Consumption
Electricity is the main purchased utility because the first-stage line has no thermal dryer. The largest load is the 200 kW MZLH678, followed by straw cutting, hammer milling, aspiration, cooling and conveying.
| Utility | Practical Annual Planning Range | Engineering Basis |
|---|---|---|
| Electricity | Approx. 1.05–1.25 million kWh/year | Pelletizing, grinding, cutting, fans, cooling and conveying |
| Electrical service | Approx. 500–630 kVA | Supports MZLH678 plus preparation and auxiliaries |
| Process heat | None in first stage | Procurement based on field-dried straw |
| Fresh / domestic water | Approx. 120–180 m³/year | Staff use and dry-process housekeeping |
| Process water | Minimal | Only controlled moisture correction when required |
| Loader / forklift fuel | Approx. 2,000–3,000 L/year | Bale and product handling |
The production basis is 300 days per year and 10 operating hours per day. At 9,000 T/A, average finished output is 3 T/H. Electricity is therefore monitored per finished tonne so changes in straw moisture, hammer condition or die wear can be identified quickly.
A workforce of about 8–10 people is appropriate for bale receiving, straw preparation, pelletizing, cooling/screening, packing, forklift work, maintenance/QC and supervision. The project is labor-conscious but not dependent on family members carrying every tonne by hand.
Power tariffs and supply arrangements are project-specific. The plant does not use a fabricated residential-versus-industrial tariff comparison in the operating case; the customer confirms the actual industrial connection and utility contract before commissioning.
RICHI MACHINERY
How RICHI Customized This Line for Ultra-Low Budget
The project remains cost-controlled, but ‘low budget’ is interpreted as removing unnecessary systems rather than removing essential process functions. The design omits thermal drying because the straw is purchased dry, while retaining conveying, cooling and screening because they directly affect continuous 3 T/H operation.
- One MZLH678 is used instead of several small pellet mills.
- Supplier moisture specifications replace the need for a full thermal dryer.
- A bale opener/cutter prevents long straw from overloading the hammer mill.
- A day bin and metered feeder replace manual shoveling into the pellet mill.
- A counterflow cooler eliminates floor cooling and shortens release time.
- Semi-automatic FIBC/bag filling limits packaging labor without requiring a robotic system.
Operator training focuses on bale inspection, moisture measurement, cutter/hammer-mill wear, magnetic separation, MZLH die and roller settings, cooler airflow, lubrication and safe startup/shutdown.
The client keeps critical spare parts for the die, rollers, hammer-mill screens, belts and bearings. For a one-mill project, planned spares and maintenance are more economical than purchasing an idle second pelletizing line.
The plant can add a dryer later if supplier moisture rises materially, but that expansion would be engineered from actual water evaporation rather than simply adding a small heater to the existing flow.
RICHI MACHINERY
Product Specifications
The finished product is an industrial rice-straw fuel pellet. It is not marketed as a low-ash wood pellet, because rice straw naturally contains more silica and mineral matter and may behave differently in combustion systems.
| Property | Practical Project Target | Buyer Relevance |
|---|---|---|
| Diameter | 8 mm main | Industrial feeding compatibility |
| Length | Typically 15–35 mm | Conveying and dosing |
| Moisture | About 8–12% | Storage stability and useful energy |
| Bulk density | Typically about 500–600 kg/m³ | Transport and storage |
| Ash | Often high; source-dependent | Ash removal and slagging risk |
| Net calorific value | Typically about 13–15 MJ/kg | Delivered-energy comparison |
| Mechanical durability / fines | Contract / batch target | Handling loss and feeder reliability |
| Chlorine / alkalis | Tested for sensitive boilers | Corrosion and deposit formation |
Rice straw can exceed 10% ash depending on variety, harvest method and soil contamination. The customer therefore sells to boilers able to handle agricultural-residue ash and does not promise wood-pellet ash levels.
Durability and calorific value are released from batch testing rather than fixed at one claimed number such as 92–94% PDI or 14.5–15 MJ/kg for every harvest.
The page does not use a fixed May 2025 selling price or a simplified cost-per-MJ comparison. Firewood, rice husk, electricity and diesel prices change, and combustion efficiency differs between boiler systems.
RICHI MACHINERY
Market Outlook for Rice Straw Pellets in Cambodia
Cambodia’s paddy output gives rice straw pellet producers a large theoretical feedstock base, but the bankable market is much smaller than the residue total. FAO forecasts about 14.6 million tonnes of paddy for 2025, while Battambang’s strong rice productivity keeps the project close to a concentrated agricultural supply area.
The most realistic customers are industrial heat users that need a standardized fuel and can manage agricultural ash. Raw rice husk remains a strong competitor because many rice mills already have access to it at low cost, so pellets must earn their price through better handling, storage, metering or combustion consistency.
| Commercial Challenge | Project Response |
|---|---|
| Rice husk is already cheap at mills | Target users that value densification and controlled feeding |
| Straw collection is seasonal | Contract balers and supplier-side covered storage |
| Rice straw has high ash | Match customers with appropriate grates and ash handling |
| Transporting bales is expensive | Keep collection radius close to Battambang |
| Customers may prefer firewood | Run combustion trials and compare delivered heat cost |
| Export needs tighter specifications | Treat export as secondary to domestic industrial sales |
Cambodia’s Ministry of Mines and Energy reports biomass as part of the national renewable-energy mix, but the project does not assume utility co-firing demand. Its base case remains local and regional industrial heat.
The project does not rely on unsupported estimates such as a 5,000–10,000 T/A national pellet market, five to ten competitors, a 60% breakeven rate or guaranteed 15–20% operating margins. Sales expansion follows contracted customers and actual utilization.
RICHI MACHINERY
Why a Rice Straw Pellet Line Makes Sense for Small Entrepreneurs
A rice-straw pellet line can suit a small entrepreneur when the plant is located close to rice production, straw arrives dry enough for economical processing and the target boilers are able to handle agricultural-residue ash.
The largest cost-saving opportunity is not eliminating every auxiliary machine; it is avoiding unnecessary drying. Buying properly field-dried straw can remove a major thermal system from the first-stage investment, but moisture still has to be measured and wet-season supply managed.
The second advantage is single-feedstock simplicity. Operators do not need to change recipes between wood, husk and stalks, although supplier-to-supplier differences in moisture, soil and silica still require quality control.
At 3 T/H, however, manual transfer and floor cooling are no longer sensible ways to save capital. A bale opener, short conveyors, a day bin and counterflow cooler reduce labor and make commercial output more predictable.
The 3,200 m² site is also deliberately moderate. It is large enough for protected straw and truck access but still relies on supplier-side seasonal inventory rather than building a huge warehouse that a small Cambodian business would struggle to finance.
For another biomass pellet project, RICHI first checks bale form, moisture by harvest season, collection radius, ash contamination, industrial power, customer boiler type and storage days before finalizing the process.
Equipment can be shipped from Qingdao to Sihanoukville Autonomous Port and then moved inland by road to Battambang. PAS identifies Sihanoukville as Cambodia’s main deep-sea port; in the second quarter of 2025 alone it handled more than 317,000 TEU, confirming adequate container infrastructure for imported machinery.
RICHI scope covers engineering, manufacture, factory inspection, export packing, installation guidance, commissioning and operator training. A project of this scale can typically be implemented in about 5–7 months when site work and electrical preparation proceed in parallel with equipment manufacture.
Additional project equipment references include biomass pellet mill; straw pellet plant.
● RICHI MACHINERY
RICHI Service

● Consulting
Customer Consultation
We want to have a deep understanding of your industrial process, to know your exact needs of feed, wood, biomass, fertilizer or other pellet processing.
● Design
biomass Pellet Plant Design
Based on your unique situation and industrial process, we will tailor complete pellet plant you need, and inform you of every additional detail that could facilitate operation, minimize total cost.

● Manufacturing
Equipment Manufacturing
The critical components of the of the complete pellet production line equipment are built in our own workshops in Asia. Additional equipment is manufactured by our worldwide network of reliable partners.

● Testing
Quality Inspection & Testing
Before leaving the factory, all equipment will be inspected by the quality inspection department. We can also provide customers with testing services from a single machine to a complete pellet plant system, and provide you with real actual data for “worry-free use.”

● Delivery
Equipment Delivery
In equipment boxing and packaging, we adopt professional packaging and modular solutions to ensure the safe and non-destructive delivery of pellet plant equipment.

● Installation
Installation & Commissioning
Whether you choose your own subcontractor for the erection phase or you want to install everything together with us, a Richi supervisor will be around to make sure everything is mounted in a safe and thorough way.

● Training
Staff Training
We provide comprehensive training for the technicians of each project. We can also continue to provide support for the technicians during latter project operation.

● After-sales
Project Follow-Up
When everything is up and running our Richiers will help you further whenever needed. We are ready to answer your call 24/7.We’ll also visit you regularly to learn about your needs.

Who we are
RICHI Machinery is one of the world’s leading suppliers of technology and services for the animal feed, aqua feed and pet food industries, also the largest pellet production line manufacturer in China.
Since 1995, RICHI’s vision to build a first-class enterprise, to foster first-class employees, and to make first-class contributions to society has never wavered.
In the past three decades, we have expanded our business to a wide range of areas, including animal feed mill equipment, aqua feed equipment, pet feed equipment, biomass pellet equipment, fertilizer equipment, cat litter equipment, municipal solid waste pellets equipment, etc.

1995
RICHI Established

2000+
Serving More Than 2000 Customers

120+
RICHI Employees

140+
Exported To 140 Countries



