 0086-138 3838 9622
4–5 T/H organic waste pellet production line in Brazil
Two pellet presses connect straw, wood, bamboo and branch residues with industrial fuel production in São Paulo State. Wet straw and branches pass through a drum dryer, while material already at the moisture target can bypass drying after suitable particle preparation.

RICHI MACHINERY
A completed mixed-residue fuel plant in São Paulo
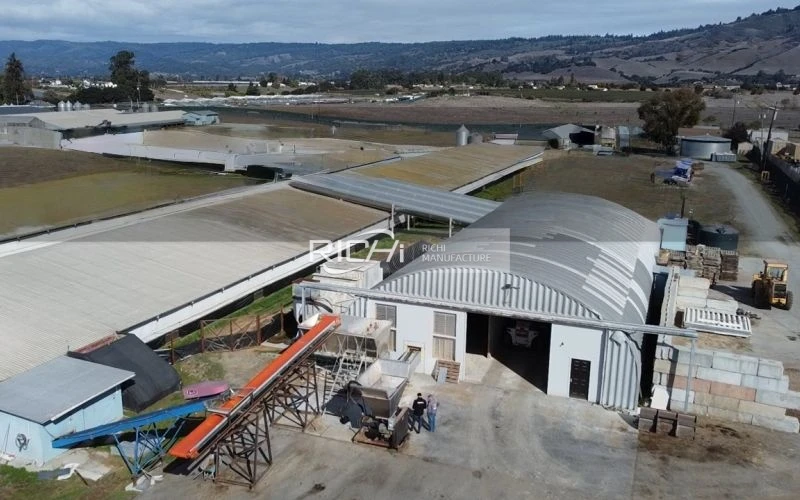
This organic waste pellet production line in Brazil was completed for a renewable-resource company in São Paulo State. The forming section belonged to the 4–5 T/H class, with a nominal operating point of 4.5 T/H. Its annual production programme was 20,000 tonnes of pellet material.
The incoming-material account covered crop straw, wood chips, bamboo chips and branches. Their moisture levels differed substantially, so the preparation route separated material needing water removal from material already near the press-feed moisture target. Size preparation remained necessary for coarse pieces on either route.
The finished product was biomass pellet fuel for industrial heat users. The wood and bamboo scope depended on clean, untreated material with an identifiable origin. Painted, treated, bonded or unidentified demolition debris was outside the stated fuel recipe.
The owner combined existing buildings with a new steel workshop on the same site. Preparation, drying, pelletizing, cooling and packing occupied the production route. A dedicated fine-material warehouse supported feed handling, while finished pellets were held within the production workshop before dispatch.
The wood pellet production line operation had 18 staff and a 280-day working year. Its daily line window ran from 08:00 to 24:00, giving 16 scheduled hours per day. Staff were recruited around the site, with lunch provided and no on-site dormitory.
4–5 T/H
forming capacity
US$360,000
project investment
Brazil
location
Industrial fuel pellets
project type
RICHI MACHINERY
Site area and the three main buildings
The organic waste pellet production line in Brazil occupied a 9,188 m² site. Total building floor area was 4,511.59 m²: 668 m² in two existing buildings, 3,743.59 m² in the new workshop, and 100 m² for the guard room and other facilities.
Land and building allocation
| Area measure | Project figure | Scope |
|---|---|---|
| Project site | 9,188 m² | Whole site area |
| Existing buildings combined | 668 m² | Buildings 1 and 2 |
| New workshop | 3,743.59 m² | Building 3 floor area |
| Guard room and other facilities | 100 m² | Additional building area |
| Total building floor area | 4,511.59 m² | Existing and new combined |
| Parking provision | 22 spaces | Site parking allocation |
Building functions and production space
| Building | Floor area | Function |
|---|---|---|
| Building 1 west | 294.32 m² | Fine raw-material storage |
| Building 2 north | 373.68 m² | Office canteen and staff facilities |
| Building 3 east | 3,743.59 m² | Production and finished-product holding |
Building 2 had two floors, while the new steel workshop was single-storey. The floor-area total combined the buildings’ usable levels. Process layout used the workshop’s preparation, drying, forming and finishing zones alongside the existing storage and office functions.
RICHI MACHINERY
Annual pellet production and internal fuel use
The 20,000-tonne programme covered pellet material produced from the four feedstock groups. The furnace also had a 600-tonne annual pellet-fuel allowance, mainly from material unsuitable for the sale specification but suitable for that furnace. Internal fuel withdrawal reduced the amount available for external delivery.
| Pellet account | Annual figure | Meaning |
|---|---|---|
| Production programme | 20,000 tonnes | Whole-site pellet-material objective |
| Furnace fuel allowance | 600 tonnes | Internal withdrawal |
| External availability calculation | 19,400 tonnes | Programme less own fuel |
The external-availability figure is a planning balance at the stated production and furnace-fuel allowances. It precedes opening and closing product stocks and other adjustments. Product dispatched to buyers and pellets consumed within the plant occupy separate lines in the annual account.
RICHI MACHINERY
Equipment from coarse preparation to bagging
The biomass pellet production line had one shredder, one crusher, a three-pass drum dryer and two main pellet presses. Cooling, screening and weighing followed forming. The equipment schedule below keeps the preparation, thermal, forming and finishing duties in their respective sections.
Coarse and fine preparation
| Preparation equipment | Quantity | Function |
|---|---|---|
| Vibrating conveyor | 1 | Present incoming material |
| Shredder | 1 | Reduce coarse feed |
| Transfer conveyors | 6 | Move material between duties |
| Feed inverter | 1 | Control preparation feed |
| Crusher | 1 | Prepare finer particles |
| Process fan | 1 | Support conveying airflow |
| Cyclone | 1 | Separate entrained particles |
| Discharge airlock | 1 | Discharge collected material |
| Bag collector | 1 | Collect suitable fines |
| Pipeline set | 1 | Connect the air circuit |
Drying equipment
| Drying equipment | Quantity | Function |
|---|---|---|
| Conveyors | 2 | Transfer the wet stream |
| Feed inverter | 1 | Regulate dryer feed |
| Feeding fan | 1 | Serve dryer feeding |
| Three-pass drum dryer | 1 | Dry suitable wet feed |
| Process fan | 1 | Move drying air |
| Cyclone | 1 | Separate drying-stage particles |
| Discharger | 1 | Release dried material |
| Discharge airlock | 1 | Control collected-material discharge |
| Thermal-line protective device | 1 | Furnace-line accessory |
| Hot-air duct and furnace | 1 set | Provide drying heat |
Pellet forming equipment
| Forming equipment | Quantity | Function |
|---|---|---|
| Feed conveyor | 1 | Supply the forming section |
| Level controls | 2 | Monitor material level |
| Rectangular holding bin | 1 | Hold prepared feed |
| Press feeders | 2 | Feed the two presses |
| Press support frames | 2 | Support press assemblies |
| Biomass pellet mill | 2 | Compress prepared biomass |
| Automatic lubrication units | 2 | Lubricate the presses |
| Air and particle-handling units | 3 | Serve forming-stage airflow |
| Flat conveyor | 1 | Transfer formed pellets |
Cooling and screening equipment
| Cooling equipment | Quantity | Function |
|---|---|---|
| Steep-angle conveyor | 1 | Lift pellets to cooling |
| Cooler | 1 | Cool freshly formed pellets |
| Fan | 1 | Provide cooling airflow |
| Cyclone | 1 | Separate entrained particles |
| Level controls | 2 | Monitor cooler material levels |
| Product screen | 1 | Separate the finished stream |
Packing equipment
| Packing equipment | Quantity | Function |
|---|---|---|
| Steep-angle conveyor | 1 | Transfer product downstream |
| Packing-stage mixer | 1 | Downstream material handling |
| Level controls | 2 | Monitor material holding |
| Packing scale | 1 | Weigh product for packing |
RICHI MACHINERY
Feedstock quantities moisture and service allowances
The four raw-material streams totalled 24,108 tonnes annually on the procurement basis. Production used no added adhesive for the stated recipe. Moisture figures described the incoming streams; the drying target was about 15% before the wet material joined the pelletizing route.
| Incoming material | Annual allowance | Moisture basis |
|---|---|---|
| Crop straw | 2,476 tonnes | 30% |
| Wood chips | 6,316 tonnes | About 15% |
| Bamboo chips | 6,316 tonnes | About 15% |
| Branches | 9,000 tonnes | 45% |
| Total incoming biomass | 24,108 tonnes | Four-stream procurement account |
RICHI MACHINERY
How the wet and drier material routes joined
Receiving established which material needed coarse preparation and which needed drying. Both routes supplied particles suitable for the same forming section. The shared finishing route then cooled and screened the pellets before weighed packing and movement into product storage.
Receive and divide the raw-material streams
Straw entered the material account at 30% moisture and branches at 45%. Wood and bamboo chips were budgeted at about 15%. The drier material could bypass the dryer after its particle condition was suitable; large chips still required size reduction before pressing.
Shred coarse feed before fine preparation
The vibrating conveyor and shredder handled suitable coarse feed before the crusher. The stated preparation range was 3–8 mm. That range described size reduction, with the final particle distribution assessed against the die and material behaviour before the feed entered the presses.
Cyclone separation discharged prepared particles through the connected collection and transfer equipment. Suitable collected fines returned to the production route. Returned fines remained an internal flow and did not represent an additional supply of purchased dry material.
Dry the straw and branch stream
The wood chip dryer took heat from the pellet-fired hot-air furnace. Straw and branches formed the wet drying branch under the stated material account. The three-pass drum provided the drying path before this material joined the drier feed for pelletizing.
The wet branch comprised 11,476 tonnes annually at its incoming moisture levels. Drying it to 15% moisture gives about 7,863 tonnes of prepared material and removes about 3,613 tonnes of water. These are calculated annual quantities with dry solids retained, before preparation or handling losses.
Wood and bamboo contributed a further 12,632 tonnes at the same 15% reference moisture without this drying load. Together, the two branches gave about 20,495 tonnes of prepared feed on the calculation basis. Actual finished weight also followed forming losses, internal use and stock movement.
| Annual drying calculation | Approximate quantity | Moisture basis |
|---|---|---|
| Straw after drying | 2,039 tonnes | 15% |
| Branches after drying | 5,824 tonnes | 15% |
| Combined wet-branch prepared feed | 7,863 tonnes | 15% |
| Water removed | 3,613 tonnes | Dry-solids balance |
| Drier wood and bamboo feed | 12,632 tonnes | 15% reference |
| All prepared feed | 20,495 tonnes | Before processing losses |
Over 4,480 scheduled hours, this wet-stream calculation averages about 2,562 kg/h entering the dryer and 807 kg/h of water removal. These calendar averages provide an annual-load reference. The required peak drying rate follows the actual dryer hours and the material being fed.
Feed two presses from prepared material
Each ring die pellet machine compressed prepared particles into fuel pellets. Two presses shared the forming duty; feeders and automatic lubrication were provided for each. The stated product diameter was 8–10 mm, with the die opening and finished specification selected for the receiving industrial fuel system.
Cool before final product handling
Freshly formed pellets passed to the cooler before screening and packing. Cooling reduced heat in the product and helped it reach a suitable storage condition. The finishing section’s conveyor, fan, cyclone and level controls supported this stage as part of the shared product route.
Screen weigh and store the pellets
The screen separated product according to the finishing requirement. Accepted pellets passed to weighed packing and finished-product holding. Suitable returns re-entered production, while any material allocated to furnace fuel was withdrawn and accounted for separately.
RICHI MACHINERY
A north entrance with production on the east side
The site entrance was on the north side, near the office building and parking provision. Building 1 on the west held fine raw material. The new eastern workshop contained size reduction, drying, pelletizing, cooling, packing and finished-product holding in process order.
RICHI MACHINERY
Why the company chose a shared residue-pellet operation
Process four identifiable residue streams
The owner worked with agricultural processing residues and recoverable woody material. A shared preparation and fuel-pellet route gave accepted material a defined production destination. Receiving still needed to identify each stream so that the line could apply the appropriate size and moisture preparation.
The four-stream account also made storage and processing requirements visible. Branches carried more incoming water than the wood and bamboo allowance, while straw had its own handling characteristics. Procurement weight therefore translated into different drying loads and prepared-feed quantities.
Supply fuel for industrial heat applications
The customer’s commercial direction included heat users in food processing, sugar production and chemical industries. Fuel acceptance followed each buyer’s specification and equipment. Those sectors described intended outlets for suitable product without establishing a particular buyer’s order volume.
Industrial customers needed the declared feedstock, pellet dimensions and handling condition to suit their fuel system. Moisture, ash, fines and fuel value were specification items for the offered product. Results depended on the supplied mix and the product lot.
Define the recoverable wood and bamboo scope
Recovered wood and bamboo were useful only when their material history and condition suited the recipe. Sorting and receiving kept clean, untreated material distinct from coated, treated, bonded or mixed debris. The feed specification defined what could enter the fuel route.
Fit the annual programme into productive hours
Productive running time determined whether the calendar could cover the annual programme. The scheduled line window allowed 4,480 hours. Dryer availability, press loading and finishing capacity all affected how much of that window became accepted production.
| Annual operating measure | Calculated time | Condition |
|---|---|---|
| Scheduled line window | 4,480 hours | 16 hours for 280 days |
| 20,000 tonnes at 4.5 T/H | About 4,444 hours | Productive forming time |
| 20,000 tonnes at 5 T/H | 4,000 hours | Upper-class rate scenario |
| Calendar allowance at 5 T/H | 480 hours | For interruptions and other duties |
The 5 T/H scenario is a capacity-planning check rather than a measured annual result. At 4.5 T/H, only about 36 hours remain in the full calendar before interruptions. Reliable annual delivery therefore depends on the productive rate actually sustained with the selected material.
Account for fuel consumed within the plant
The hot-air furnace used pellet fuel, including an allowance for suitable off-specification material. Keeping this withdrawal visible connected production with the dryer’s own fuel demand. Startup also required a suitable fuel supply before fresh pellets became available from the line.
Electricity water and furnace-fuel allowances
The existing electricity connection served the line, with an annual planning allowance of 1.6 million kWh. Supply water came from the well and tap-water provision. Personnel water and the furnace collection circuit had separate annual allowances.
| Service allowance | Annual figure | Account boundary |
|---|---|---|
| Electricity | 1.6 million kWh | Whole-line planning allowance |
| Personnel water | 252 m³ | Staff facilities |
| Process collection water | 420 m³ | Furnace collection circuit |
| Combined water allowance | 672 m³ | Personnel plus process |
| Pellet fuel for drying | 600 tonnes | Internal furnace use |
The energy figures were operating allowances. Electricity depended on the presses, preparation drives, fans and other auxiliaries at their actual loads. The furnace’s pellet consumption was a separate heat input, drawn from suitable fuel stock and recorded as an internal withdrawal.
For an organic waste pellet production line in Brazil, give RICHI the quantities and moisture of each residue stream, its physical form and the intended industrial pellet specification. Include the dryer-fuel requirement and operating calendar so that preparation, two-press forming and external product availability fit the same production account.
● RICHI MACHINERY
RICHI Service
● Consulting
Customer Consultation
We want to have a deep understanding of your industrial process, to know your exact needs of feed, wood, biomass, fertilizer or other pellet processing.
● Design
organic waste Pellet Plant Design
Based on your unique situation and industrial process, we will tailor complete pellet plant you need, and inform you of every additional detail that could facilitate operation, minimize total cost.
● Manufacturing
Equipment Manufacturing
The critical components of the of the complete pellet production line equipment are built in our own workshops in Asia. Additional equipment is manufactured by our worldwide network of reliable partners.
● Testing
Quality Inspection & Testing
Before leaving the factory, all equipment will be inspected by the quality inspection department. We can also provide customers with testing services from a single machine to a complete pellet plant system, and provide you with real actual data for “worry-free use.”
● Delivery
Equipment Delivery
In equipment boxing and packaging, we adopt professional packaging and modular solutions to ensure the safe and non-destructive delivery of pellet plant equipment.
● Installation
Installation & Commissioning
Whether you choose your own subcontractor for the erection phase or you want to install everything together with us, a Richi supervisor will be around to make sure everything is mounted in a safe and thorough way.
● Training
Staff Training
We provide comprehensive training for the technicians of each organic waste pellet production line in Brazil project. We can also continue to provide support for the technicians during latter project operation.
● After-sales
Project Follow-Up
When everything is up and running our Richiers will help you further whenever needed. We are ready to answer your call 24/7.We’ll also visit you regularly to learn about your needs.
Who we are
RICHI Machinery is one of the world’s leading suppliers of technology and services for the animal feed, aqua feed and pet food industries, also the largest pellet production line manufacturer in China.
Since 1995, RICHI’s vision to build a first-class enterprise, to foster first-class employees, and to make first-class contributions to society has never wavered.
In the past three decades, we have expanded our business to a wide range of areas, including animal feed mill equipment, aqua feed equipment, pet feed equipment, biomass pellet equipment, fertilizer equipment, cat litter equipment, municipal solid waste pellets equipment, etc.

1995
RICHI Established

2000+
Serving More Than 2000 Customers

120+
RICHI Employees

140+
Exported To 140 Countries